

R-Type EDM Chucks Deliver High-Performance Precision for EDM Applications
As a reliable industrial supplier of R-Type EDM Chucks, JWGRIP delivers robust long-service-life pneumatic chucks, manual chucks and multi-station clamping modules for mold makers, electrode processing contractors and EDM workshop buyers seeking steady clamping repeatability in continuous spark erosion operations. Core functional parts receive in-factory cryogenic treatment and precision lapping to reduce thermal deformation from long-time spark discharge and preserve stable locating performance under cyclic loading. Beyond EDM clamping hardware, JWGRIP also develops EROWA Compatible EDM Workholding and Wire EDM Workholding Fixtures, satisfying full-range clamping demands from electrode preparation to wire-cut finishing.
Many mold processing facilities underestimate how much unstable chuck performance can erode final part quality. In daily EDM production, operators frequently replace electrodes and workpieces; ordinary clamping structures easily suffer from position offset after multiple disassembly. Tiny positioning deviation will be amplified in spark machining, resulting in uneven spark gap, flawed mold cavity surfaces and increased rework rate. Without dedicated chucks designed for dielectric-rich EDM environments, workshops cannot give full play to high-end EDM machine potential, even if they invest heavily in advanced spark erosion equipment.
What distinguishes purpose-built clamping hardware from general-purpose fixtures used inside EDM machines?
Standard mechanical vices or simple clamping blocks are made for CNC milling environments, and they lack protection against dielectric fluid immersion, carbon residue accumulation and pulse-induced thermal fluctuation.
In contrast, R-Type EDM Chucks are fully optimized for the unique working conditions of spark erosion.
The R-Type D150 Pneumatic EDM Chuck delivers fast, force-balanced pneumatic locking for frequent electrode swap-outs, while R-Type D75 MacroStd CNC Manual EDM Chuck suits low-volume prototype jobs where air supply is unavailable on-site. The R-Type 9-in-1 Pneumatic EDM Chuck supports multi-electrode simultaneous positioning, greatly cutting total machining cycle time for complex cavity molds.
Sealed internal structures block dielectric fluid and carbon debris from entering precision fitting gaps, reducing wear on internal locating components. Every clamping action reproduces the original datum, so operators avoid repeated indicator checking and time-consuming electrode re-alignment between different spark tasks.
Process Advantages
Many factories spend far more time swapping and calibrating electrodes than actual spark-erosion cutting. Adopting standardized chucks helps shift most setup work outside the EDM machine enclosure. Workers can complete electrode pre-clamping and offset measurement on auxiliary benches, then transfer the whole assembly onto the machine-mounted chuck in seconds. Pneumatic variants such as R-Type D150 Pneumatic EDM Chuck and R-Type 9-in-1 Pneumatic EDM Chuck minimize manual twisting and tightening, lowering human error sources. If your production line mixes prototype orders and mass mold projects, you can match manual-style R-Type D75 MacroStd CNC Manual EDM Chuck and R-Type D100 Manual EDM Chuck according to batch characteristics. This set of hardware can cooperate with R--Type Electrode Holders to form a complete electrode handling workflow, and it can also interconnect with quick-change components from Quick Change Workholding System when building semi-automated mold-making cells.
Core Product Strengths
Specially sealed internal construction resists dielectric fluid, carbon dust and machining residue contamination for long-term stable EDM operation.
Dual selection of pneumatic drive and manual mechanical locking adapts to automated production lines and small-batch manual workshops respectively.
Micron-level repeat positioning accuracy reduces electrode offset and avoids defective mold cavity surfaces triggered by datum shift.
Compatible with mainstream electrode holders and locating plates, enabling seamless connection with existing workshop fixture inventory.
Product Composition Overview
JWGRIP’s clamping hardware portfolio covers pneumatic multi-station models and compact manual variants to fit diverse EDM production flows.
High-efficiency pneumatic products include R-Type D150 Pneumatic EDM Chuck and R-Type 9-in-1 Pneumatic EDM Chuck, mainly oriented toward high-frequency electrode replacement scenarios in large-scale mold workshops; these models rely on stable air pressure input to realize uniform clamping force across multiple stations. Manual series contains R-Type D75 MacroStd CNC Manual EDM Chuck and R-Type D100 Manual EDM Chuck, ideal for laboratories, prototype workshops and sites without stable compressed-air supply. All chucks belong to the complete R-Type EDM Workholding System product ecosystem. When users need to expand electrode mounting capacity, they can pair these chucks with R-Type Centering Plates for datum extension, or adopt supporting modules from EROWA Compatible EDM Workholding to realize cross-system fixture sharing.
Typical Application Scenarios
These clamping units are widely deployed in plastic injection mold manufacturing, die-casting mold processing, precision stamping die production and custom electrode batch preparation work. They fit sinker EDM machines for cavity machining, and serve as core locating units for mold insert, gear electrode and complex texture electrode clamping. Whether you are retrofitting old sinker EDM equipment or constructing brand-new intelligent mold-making workshops, properly configured chucks can compress electrode replacement cycles and stabilize final surface quality of mold cavities. They are frequently selected by automotive mold suppliers, consumer-electronics mold factories and precision tooling manufacturers.
Selection Guide
First evaluate your actual production mode: mass continuous mold-making with frequent electrode changes tends to benefit more from pneumatic-driven R-Type EDM Chucks such as R-Type D150 Pneumatic EDM Chuck or R-Type 9-in-1 Pneumatic EDM Chuck. Prototype-oriented job shops with fewer swap-ins can choose cost-effective manual options including R-Type D100 Manual EDM Chuck.
Next confirm electrode sizes, maximum clamping load and installation space on your EDM machine worktable. Do not ignore the on-site air-supply condition: pneumatic versions require stable, dry compressed-air sources.
If you plan to connect with existing fixture resources, verify compatibility with R-Type Electrode Holders and locating plates in advance. If you face confusion about parameter matching, JWGRIP’s product documentation offers detailed dimension tables and installation reference guides for on-site technical reference.
Why Work With JWGRIP?
Every chuck body, locating taper and locking assembly undergoes strict multi-process inspection before delivery. High-hardness alloy steel raw materials plus cryogenic treatment relieve internal stress generated during machining, so positioning accuracy will not decay rapidly after thousands of clamping cycles.
Besides standard stocked models, we accept customized modification for special installation dimensions, clamping force parameters and anti-corrosion surface treatment to satisfy unique mold-making requirements. We provide dimension drawings, installation manuals and maintenance tips to help workshop staff carry out daily inspection and component replacement. Correct routine maintenance will greatly extend service life of these precision clamping units and keep your sinker-EDM production running steadily for years.




- View as
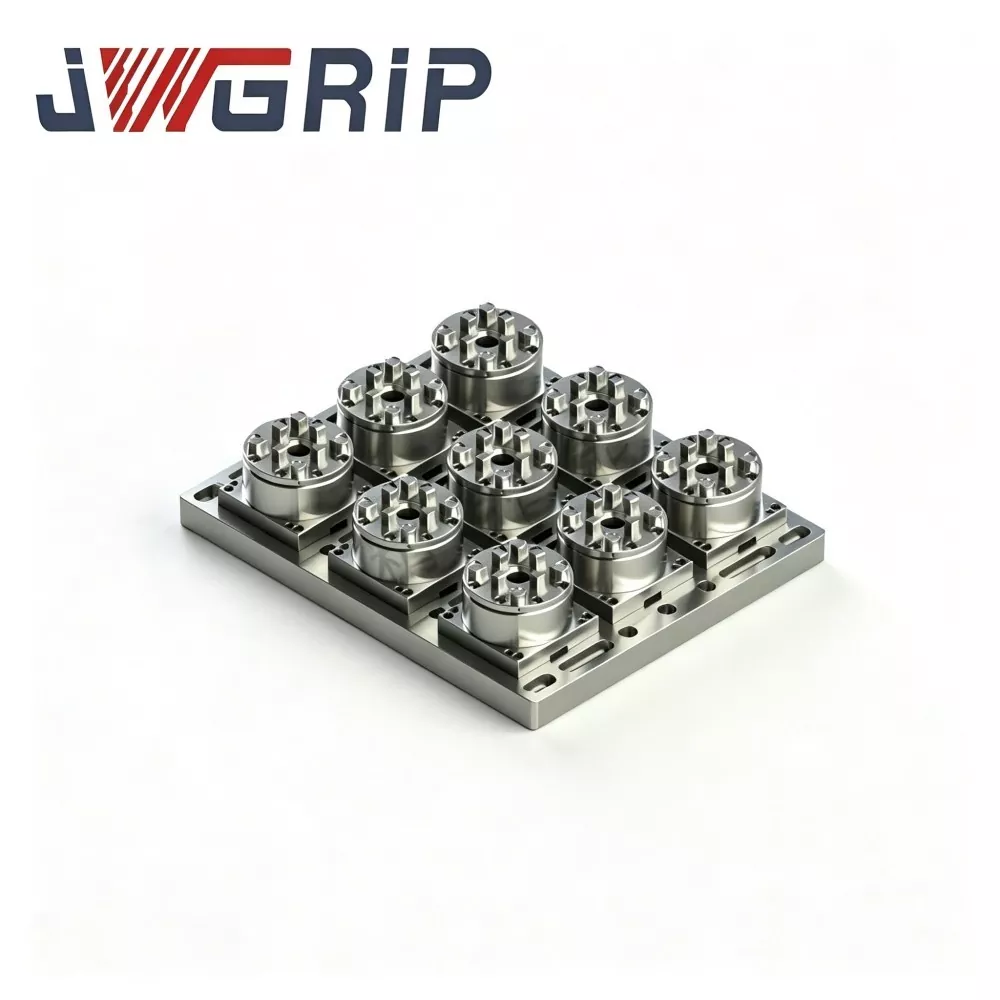
R-Type 9-in-1 Pneumatic EDM Chuck
JWGRIP is the professional manufacturer and supplier of R-Type 9-in-1 Pneumatic EDM Chuck in China, providing Factory Direct service with standard models fully in Stock to serve global precision machining and mold manufacturing enterprises. It is an all-in-one integrated quick-change pneumatic workholding system professionally designed for EDM and precision machining flexible production scenarios. It integrates nine sets of different electrode holder configurations into a single chuck body, eliminating the need for purchasing, storing and managing multiple discrete EDM chucks and independent clamping accessories.
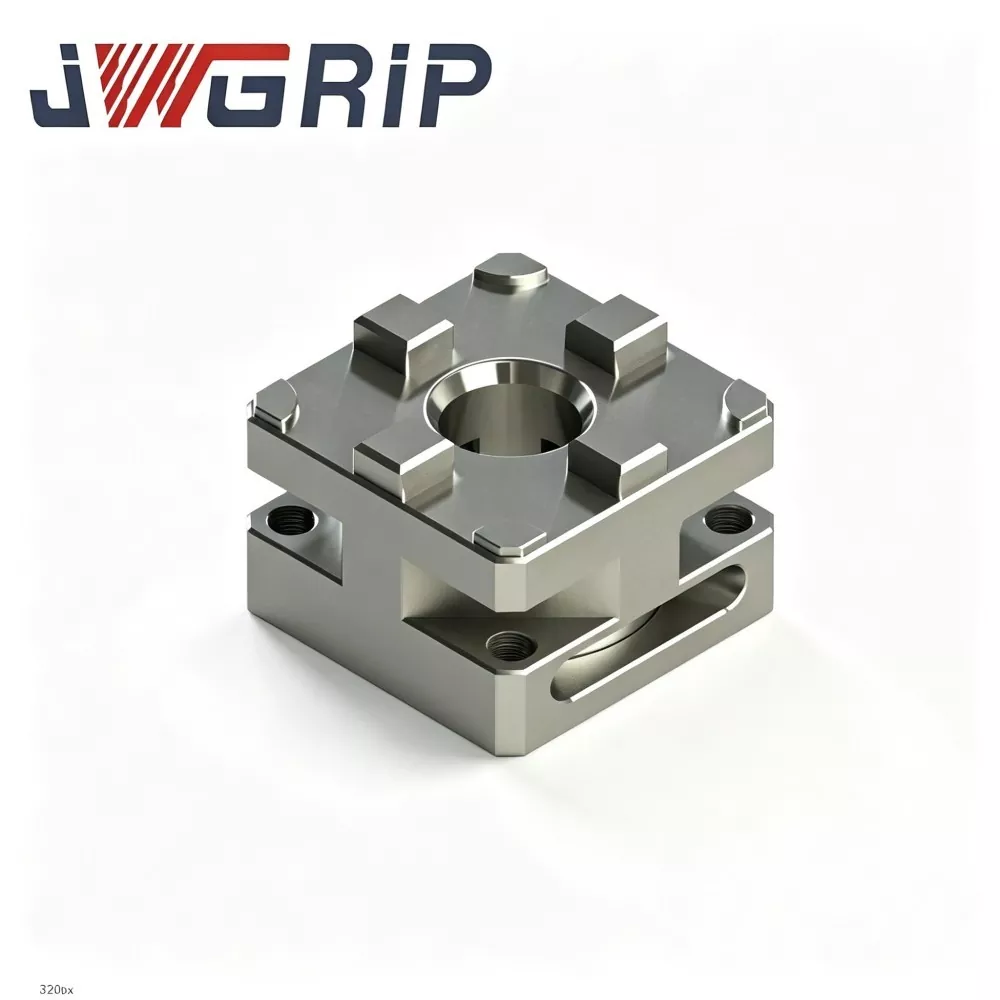
R-Type D100 Manual EDM Chuck
JWGRIP is the professional manufacturer and supplier of R-Type D100 Manual EDM Chuck in China, with standard models fully in Stock and supporting global Bulk Order for project tender submission and batch trial-run procurement. It is a high-precision integrated manual datum clamping fixture specially designed for sinker EDM, die-making and multi-station electrode presetting workshops. Adopting all-mechanical locking structure without pneumatic air source dependence, it integrates stable manual clamping performance and high-precision concentricity positioning function into a single unit.
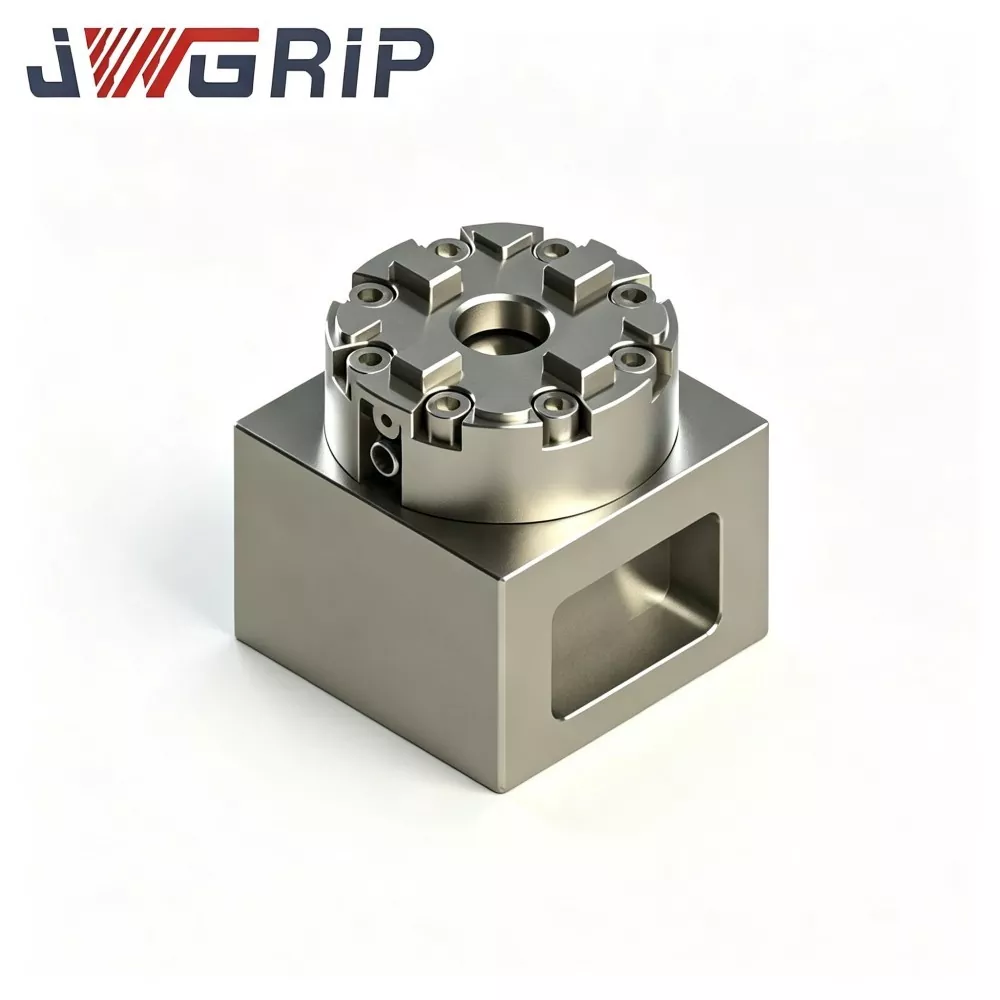
R-Type D75 MacroStd CNC Manual EDM Chuck
JWGRIP is the professional manufacturer and supplier of Customized R-Type D75 MacroStd CNC Manual EDM Chuck in China, providing Factory Direct supply to support global volume bidding projects and spot consignment business. It is a high-precision integrated manual clamping fixture complying with MacroStd dimensional standards, specially engineered for sinker EDM, wire-cut EDM and professional mold electrode manufacturing workshops. Integrating anti-corrosion hardened steel structure and unified precision positioning benchmark into a single compact unit, it eliminates tedious repeated dial indicator calibration and cumulative positioning errors of traditional clamping tools.

R-Type D150 Pneumatic EDM Chuck
JWGRIP is the Professional manufacturer and supplier of R-Type D150 Pneumatic EDM Chuck in China, with standard specifications fully in Stock to support global framework agreement cooperation and consignment order deployment. It is a high-efficiency integrated pneumatic clamping fixture professionally customized and developed for die-sinker EDM, wire-cut EDM and precision mold electrode machining scenarios. It integrates optimized internal air circuit structure and high-precision positioning clamping unit into a single device, eliminating tedious manual alignment and repeated calibration procedures required by traditional fixtures.
JWGRIP is a professional R-Type EDM Chucks manufacturer and supplier in China. We warmly welcome you to wholesale high quality products at competitive price from our factory.




