

Customized Wire EDM Workholding Fixtures for Precision Machining Applications
As an experienced developer and fabricator of Wire EDM Workholding Fixtures, JWGRIP delivers independent technical development for adaptive wire-cut clamping jigs, adjustable positioning brackets and anti-distortion support assemblies dedicated to submerged precision die-cutting processes. JWGRIP’s hardware lineup also includes R-Type EDM Workholding System and CNC Self-Centering Vises, solving various fixture-matching challenges for cross-process precision manufacturing.
Many precision workshops underestimate how much finished-part failure originates from unsuitable fixture hardware for submerged wire-cut operations. Unlike conventional CNC milling, wire EDM runs continuously under deionized dielectric water flushing. Poor fixture material selection will trigger rusting, scale accumulation and clamping-force decay over long cutting cycles. Thin-wall, fragile or irregular-outline workpieces easily suffer micro-deformation under uneven squeezing force or strong water-jet impact.
Have you ever thought about how many qualified parts get discarded simply because unstable holding conditions instead of machine-tool parameter errors? Operators spend plenty of working hours correcting reference readings after re-mounting workpieces, which compresses actual effective cutting duration. That is exactly why purpose-built Wire EDM Workholding Fixtures become irreplaceable hardware for high-quality wire-cut mass-production and prototype tasks.
Typical Hidden Fixture-Related Issues
Common general-purpose vises lack anti-corrosion material treatment. After long-time immersion in dielectric fluid, locating faces get pitted and scaled, bringing invisible positioning drift for subsequent batches.
Excessive local clamping stress squeezes thin-walled blanks. Even minor elastic deformation will rebound after part release, generating out-of-tolerance dimension and flatness errors for high-precision components.
Without unified reference interfaces, operators have to redo full-indicator calibration every time workpieces get dismounted and reinstalled. Repeated manual centering creates cumulative human-introduced deviation.
When parts need sequential processing across milling, sinker EDM and wire-cut stations, ordinary jigs cannot keep consistent datum transferring between different machine platforms. Extra re-alignment work lowers overall workshop throughput.
Core Advantage
Wire EDM Workholding Fixtures adopt non-magnetic, anti-corrosion stainless-steel base material. Key locating surfaces go through ultra-fine grinding treatment, resisting dielectric-water erosion and debris adhesion in long-cycle submerged processing. Drain-off slot design reduces residual liquid retention and simplifies daily fixture cleaning.
Multi-point distributed clamping structure helps spread contact pressure evenly. It avoids local stress concentration so that thin and easily-deformed workpieces can be secured firmly without obvious squeezing distortion.
Modular combination layout supports flexible assembling. Users can mix vises, adapter seats, V-type clamping holders and beam pallet sets according to workpiece outline, no need for full new custom jigs for every new-coming part.
Selected fixture variants reserve compatible datum interfaces, enabling datum sharing with R-Type EDM Workholding System. Workpieces can circulate between sinker EDM and wire-cut equipment, retaining original locating reference without complete re-probing.
Main component modules
JWGRIP’s wire-cut fixture portfolio contains three inter-connected secondary-level modules, covering direct clamping, rotary-vise holding and auxiliary supporting requirements:
1. Wire EDM Chucks
Representative items: Wire EDM Vise for Precision Workholding, Pneumatic Chuck for Wire EDM Workholding, Unoset Adapter with RSM 50 Pallet Set for Wire EDM, Wire EDM Chuck for Precision Workholding.
These chucks act as core direct-clamping units installed on wire-cut machine worktable. Manual models fit small-batch trial-production; pneumatic-driven versions realize steady automatic clamping for repeated-batch tasks. Multi-direction adjustable structures compensate installation offset for complex-geometry blanks.
2. Wire EDM Vises
Representative items: TP Unoset Vee Vise for Wire EDM, 0-100mm Rotatable Wire EDM Vise, R-Type Wire EDM Super Vise 0-77mm, Unisis Square Pallet Set for Wire EDM Workholding.
Rotatable vise bodies permit angular adjustment without repeated re-clamping. V-groove inner profiles suit cylindrical and round-bar stock. Square pallet sets expand mounting space for medium-large multi-component combined clamping assignments.
3. Wire EDM Fixture Accessories
Representative items: WEDM Adapter for Wire EDM Workholding, Wire EDM Round Clamp Holder, Beam Pallet Set for Wire EDM Workholding, WEDM Reference Element for Precision Workholding.
This accessory group delivers auxiliary positioning, transition connection and benchmark-setting functions. Beam-style pallet sets offer large-span supporting space for extra-long thin parts; reference elements supply repeatable benchmark origin for frequent part-swap scenarios.
How to screen proper wire-cut fixture combinations matching your actual workshop conditions?
1.Should you pick manual or pneumatic wire EDM chucks?
Manual chucks are cost-effective for low-frequency batch change. If you run high-volume repeated-part orders and pursue stable clamping output, pneumatic chucks deserve priority consideration.
2.What fixture structure fits thin-wall fragile components?
Prioritize multi-point distributed-contact vises instead of narrow-edge point-type clamping, to minimize workpiece squeezing deformation.
3.Do you need angle adjustment during cutting procedures?
Rotatable wire EDM vises release you from repeatedly loosening and re-locking whole-set jigs for angular modification.
4.Are you planning cross-equipment part transfer among milling, sinker EDM and wire-cut?
You had better choose fixtures with unified datum interfaces. At this moment you may also refer to our CNC Self-Centering Vises for your cross-machine fixture-unification planning.
Process Advantages
Critical contact and locating components adopt special anti-corrosion non-magnetic stainless-steel raw material. After precise grinding and surface passivating disposal, fixtures sustain stable performance under long-time dielectric-water immersion.
Every finished set undergoes flatness inspection, clamping-force verification and repeat-mounting accuracy testing before leaving factory. Interchangeability among modular accessories gets fully validated.
We provide custom-tailored modification service: change clamping span, add special drainage slots, build non-standard transition brackets according to customer samples or technical drawings.
Our technical team accumulates abundant practical experience cooperating with mold labs, medical-part manufacturers and precision tool-making enterprises. We do not merely supply off-the-shelf catalogue goods; we analyze your real-world cutting constraints and propose matched fixture configuration suggestions.
Typical practical application scenarios
Precision mold insert and die component wire-cut processing under dielectric-water environment.
Thin-wall, fragile, cylindrical and irregular-shaped high-precision component production.
Multi-angle contour cutting tasks requiring rotary angle adjustment without workpiece dismounting.
Cross-station production workflow where workpieces circulate among milling, sinker EDM and wire-cut machine tools.
Small-batch prototype laboratories and high-mix-low-volume precision-part manufacturing workshops.



- View as
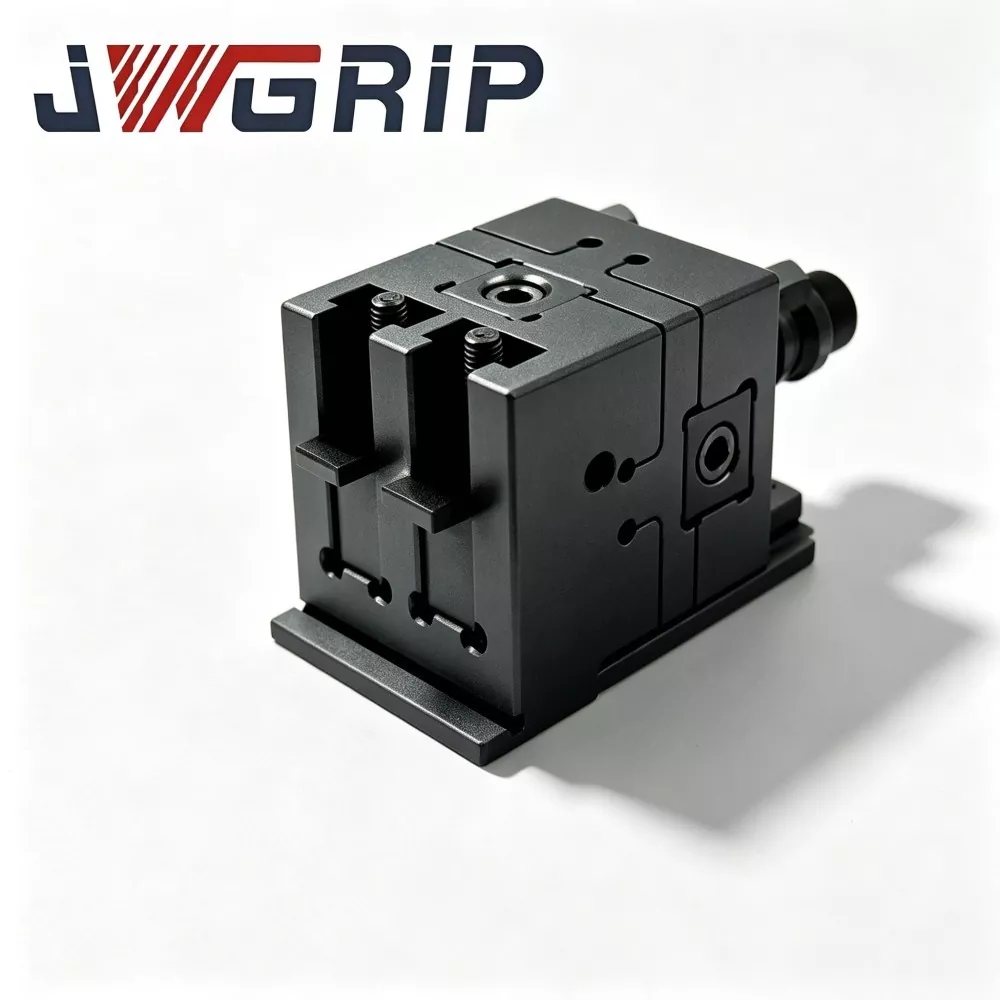
0-100mm Rotatable Wire EDM Vise
JWGRIP is the manufacturer and supplier of the Professional 0-100mm Rotatable Wire EDM Vise in China. It is high-precision workholding hardware purpose-engineered for multi-angle, taper-profile and spatial-inclined-cavity submerged wire-cut tasks. Made of thermally stabilized pre-hardened alloy steel, it adopts high-resolution rotary indexing platform and multi-point rigid position-locking mechanism, supporting continuous angular adjustment within 0-100mm clamping range. It firmly locks arbitrary rotary positions with high structural rigidity and maintains excellent angular repeatability under long-term dielectric fluid splashing and humid submerged conditions.
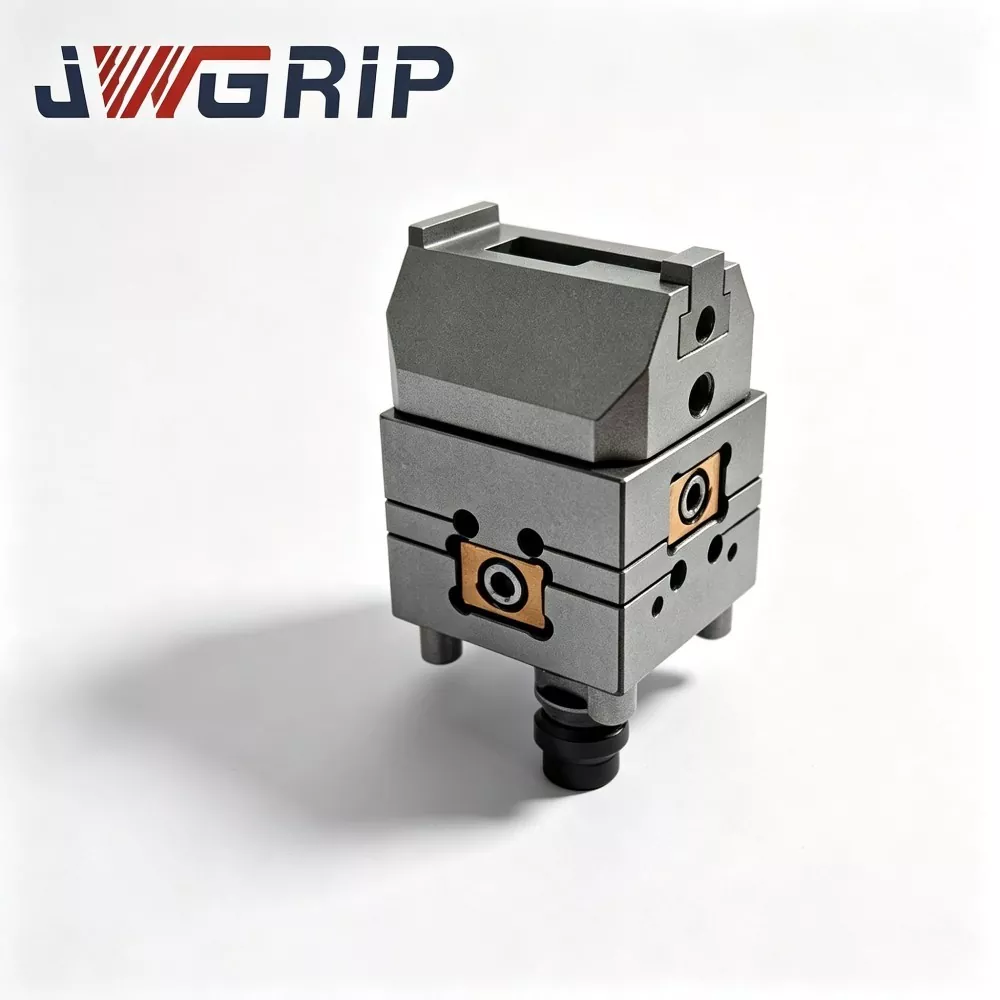
TP UnoSet Vee Vise for Wire EDM
JWGRIP is the manufacturer and supplier of the TP UnoSet Vee Vise for Wire EDM in China. It is a specialized self-centering workholding fixture engineered for submerged wire-EDM mass-production of round bar, shaft-type and eccentric cylindrical blanks. Built with cryogenically-stabilized pre-hardened alloy-steel material, it merges precision-ground dual-V-groove locating feature and native Unoset quick-change interface as one compact unit. It mounts directly to any Unoset-compatible wire-EDM worktable without extra intermediate adapters.

Wire EDM Chuck for Precision Workholding
JWGRIP is the Professional manufacturer and supplier of Wire EDM Chuck for Precision Workholding in China, providing Factory Direct supply and professional OEM modification services for global high-mix low-volume mold subcontract workshops. It is a quick-change integrated clamping fixture specially optimized for frequent-job-switch wire-cut EDM flexible production environments. It integrates precision quick-locating interface and professional submerged anti-corrosion structure into a single device, eliminating tedious full dialing and repeated re-calibration procedures required by traditional fixed clamping fixtures during order switching.
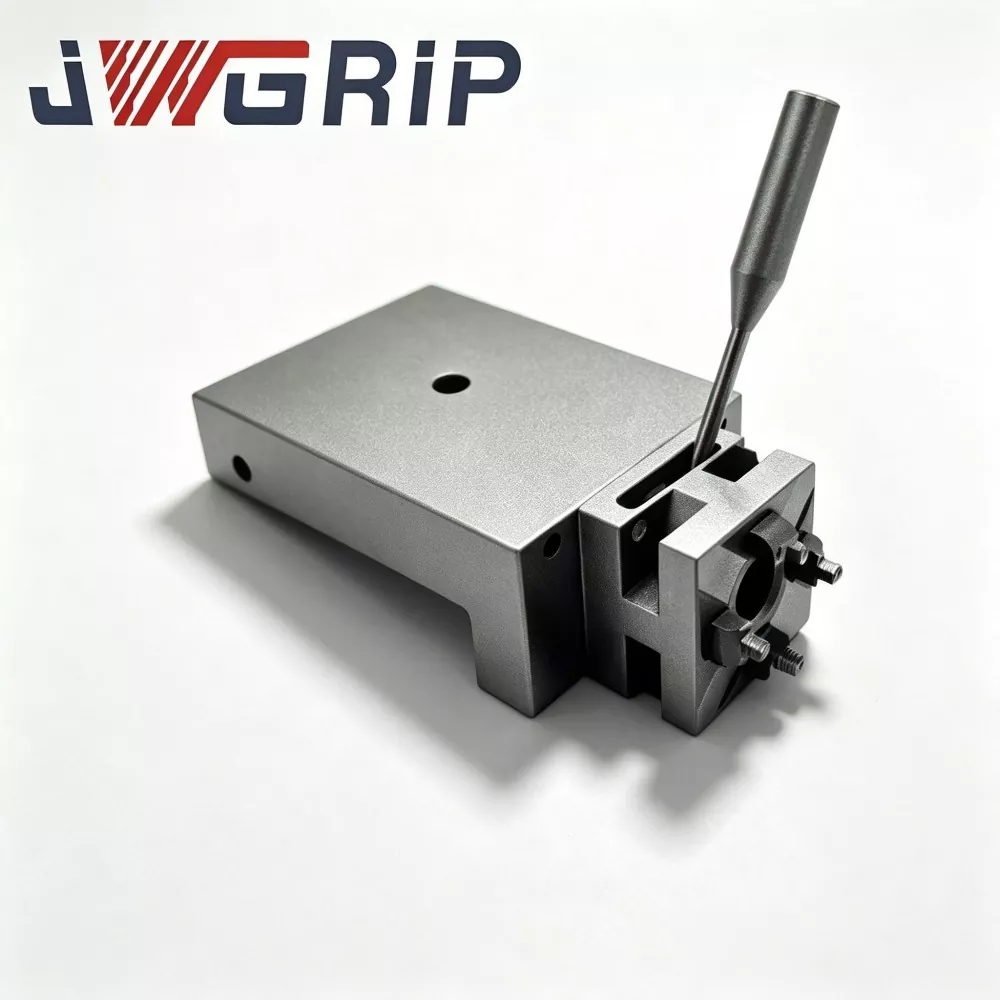
UnoSet Adapter with RSM 50 Pallet Set for Wire EDM
JWGRIP is the professional manufacturer and supplier of UnoSet Adapter with RSM 50 Pallet Set for Wire EDM in China, with standard complete sets fully in Stock and supporting global Bulk Order for mold factory equipment renovation and mixed fixture system upgrading projects. It is an integrated cross-system fixture conversion solution specially designed for wire EDM old equipment retrofitting and multi-standard fixture interconnection scenarios. It integrates Unoset-standard transition adapter and matched RSM 50 locating pallet into a complete set, accurately filling the dimensional and datum gap between Unoset machine interface and RSM 50 fixture system.
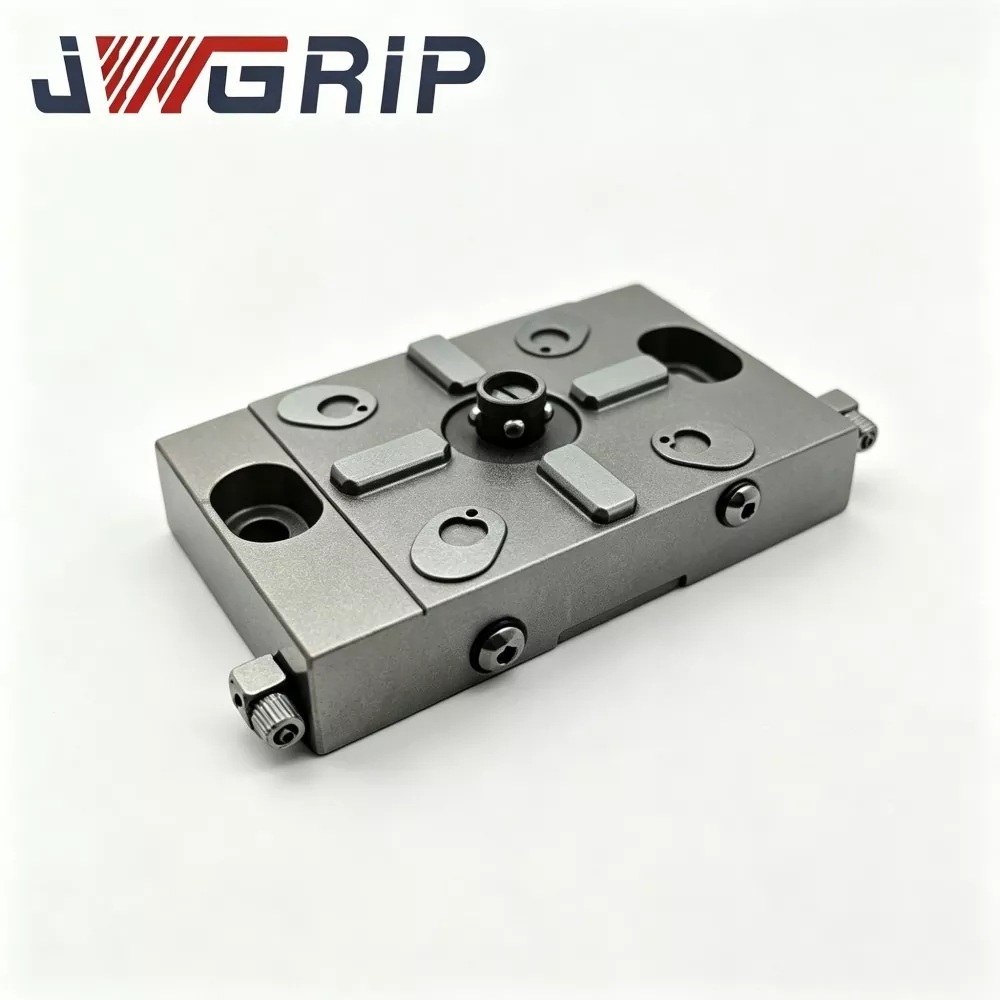
Pneumatic Chuck for Wire EDM Workholding
JWGRIP is the professional manufacturer and supplier of Pneumatic Chuck for Wire EDM Workholding in China, providing Factory Direct supply and Customized OEM structural modification for global automated submerged wire-cut production lines. It is a professional anti-corrosion integrated pneumatic clamping fixture specially designed for fully submerged wire EDM unmanned machining scenarios. It integrates exclusive air-channel anti-contamination structure and high-stability pneumatic locking performance into a single device, eliminating the common defects of ordinary dry-type pneumatic chucks such as fluid infiltration, piston jamming and clamping force attenuation in underwater environments.

Wire EDM Vise for Precision Workholding
JWGRIP is the professional manufacturer and supplier of Wire EDM Vise for Precision Workholding in China, with standard models fully in Stock and supporting global Bulk Order for professional submerged wire-cut production workshops. It is a high-rigidity integrated professional clamping fixture specially optimized for full-submersion wire EDM precision machining scenarios. It integrates cryogenically stabilized material performance and jaw anti-deflection reinforced structure into a single unit, effectively solving the problems of jaw tilting, uneven clamping and micro-deviation of ordinary general-purpose vises in long-term submerged working environments.
JWGRIP is a professional Wire EDM Workholding Fixtures manufacturer and supplier in China. We warmly welcome you to wholesale high quality products at competitive price from our factory.




