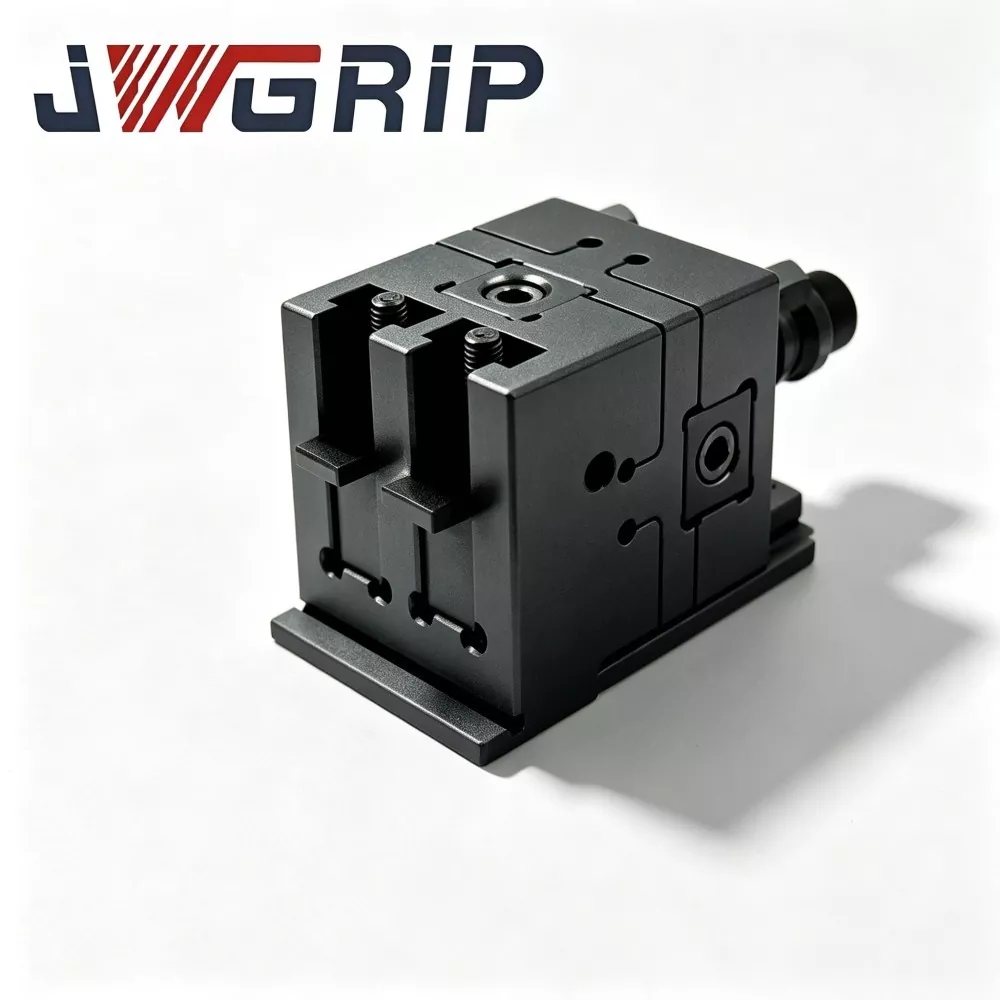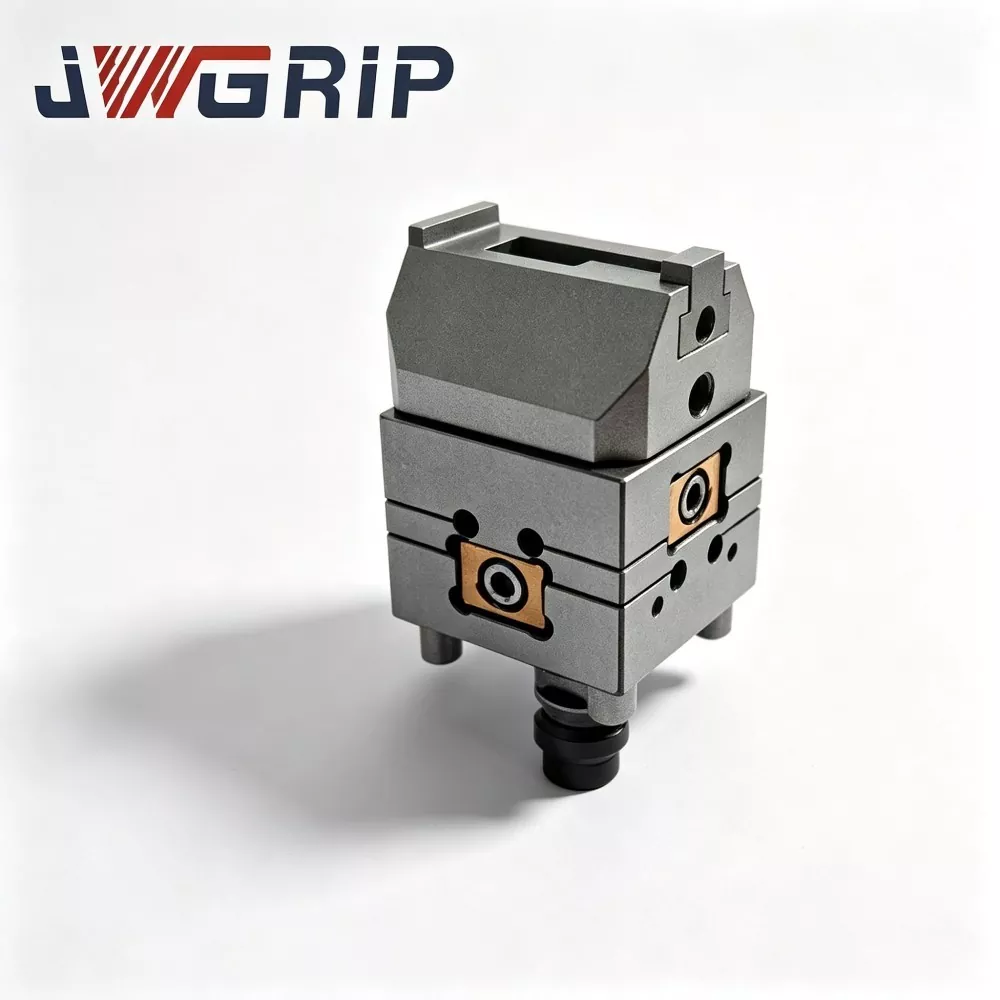
TP UnoSet Vee Vise for Wire EDM
JWGRIP is the manufacturer and supplier of the TP UnoSet Vee Vise for Wire EDM in China. It is a specialized self-centering workholding fixture engineered for submerged wire-EDM mass-production of round bar, shaft-type and eccentric cylindrical blanks. Built with cryogenically-stabilized pre-hardened alloy-steel material, it merges precision-ground dual-V-groove locating feature and native Unoset quick-change interface as one compact unit. It mounts directly to any Unoset-compatible wire-EDM worktable without extra intermediate adapters.
This high-precision wire EDM Vee Vise is manufactured from premium cryogenically stabilized pre-hardened alloy steel, with optimized rigid anti-deformation structure and professional anti-corrosion treatment tailored for long-term dielectric fluid submerged working conditions. The upgraded dual-V-groove geometric design enables accurate mechanical self-centering for various cylindrical workpieces, effectively tolerating minor raw material roundness deviation and maintaining ultra-stable concentric reference during long-duration multi-batch wire-cut cycles.
Different from traditional flat-jaw vises and ordinary loose V-blocks that rely on manual alignment and easily produce human errors and batch inconsistency, it features uniform clamping force distribution and excellent sludge erosion resistance. It avoids V-groove wear, positioning micro-shift and clamping instability caused by long-time submerged operation, greatly shortening fixture setup time and stabilizing dimensional accuracy and profile consistency of shaft parts.
Widely applicable to batch wire-cut processing of mold core pins, ejector pins, eccentric cam blanks and carbide round bars, TP UnoSet Vee Vise for Wire EDM supports standard mass supply and ODM customized modification of V-groove angles, opening ranges and mounting interfaces, providing reliable unmanned workholding solutions for modern automated cylindrical blank production cells.
Existing Bottlenecks
Many precision mold-component and tool-making workshops undertake high-volume wire-EDM orders for pin shafts, ejector pins, core pins, eccentric cam blanks and carbide round bars. Cylindrical work-pieces bring persistent practical work-holding difficulties.
· Conventional flat-jaw vises grip round blanks via two parallel flat surfaces. Minor ovality or out-of-round defects on raw stock shift workpiece central axis every time re-clamping happens. Operators spend substantial working hours re-checking concentricity for each new round-bar blank.
· Under high-volume batch-production conditions, repeated manual centering introduces variable human error. Even slight concentric offset yields inconsistent cam profiles, uneven wall-thickness on pin-style parts and non-conforming finished components.
Numerous commercially-available V-block fixtures lack standardized Unoset quick-change interface.
· Operators must perform full datum dial-in after each fixture installation and cannot share pre-established machine datum with existing Unoset tooling inventory.
· Certain simple V-block products show insufficient anti-corrosion capability under long-term dielectric-fluid immersion. Repeated batch-processing causes wear or corrosion on locating V-groove surfaces due to accumulated wire-cut sludge.
Core Design
JWGRIP TP UnoSet Vee Vise for Wire EDM is specially developed to resolve the above-mentioned cylindrical-blank work-holding bottlenecks. Different from flat-jaw vises and discrete loose V-blocks, this integrated unit combines precision self-centering dual-V-groove locating geometry and native Unoset interface.
1. Drawing on abundant shaft-part batch-production field data accumulated from JWGRIP ODM projects, multiple prototype versions complete thousands-cycle round-bar clamping aging test under simulated submerged-tank conditions before formal mass-production launch.
2. Operators mount this vise directly onto Unoset-equipped work-tables. Cylindrical blanks rest inside dual-V-groove to realize mechanical self-centering. Pre-existing Unoset fixture datum can be inherited without rebuilding the full reference chain.
3. Apart from standard specifications, JWGRIP ODM service delivers customized V-groove parameters and modified mounting interfaces for special shaft-blank automated production-lines.
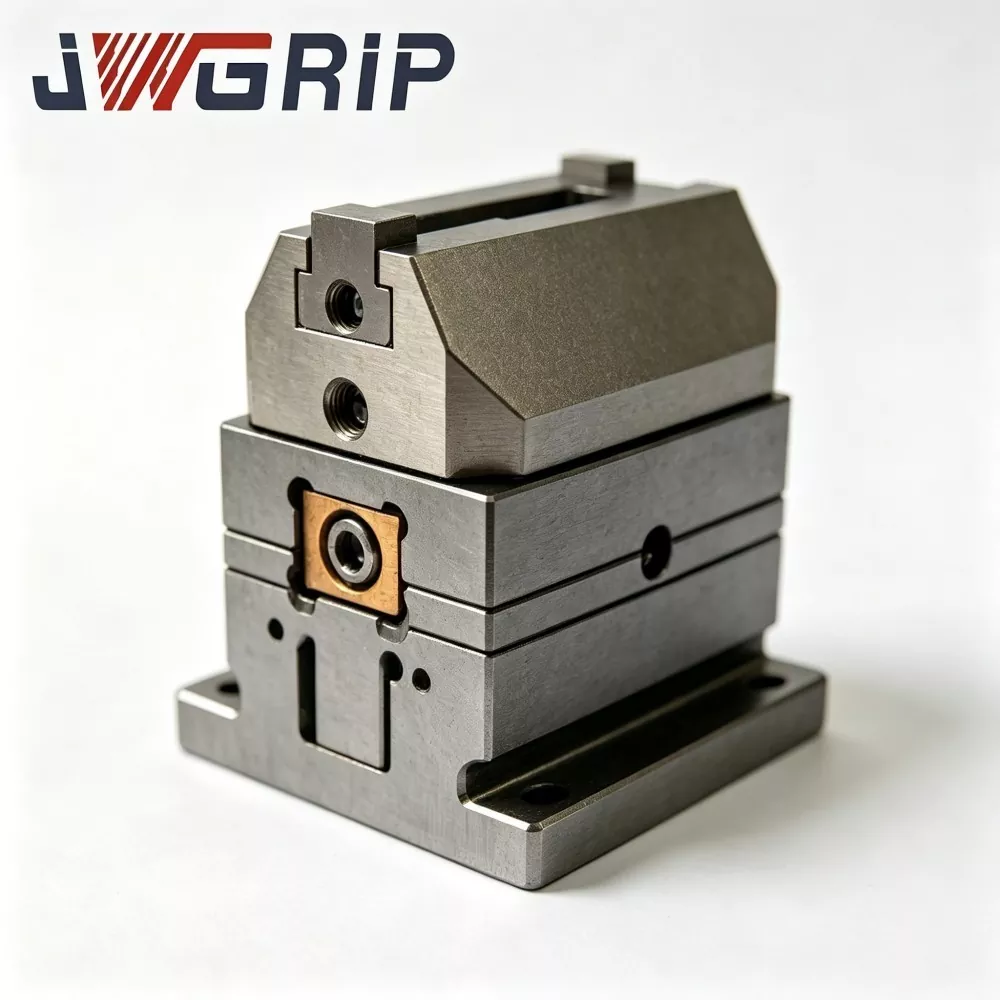
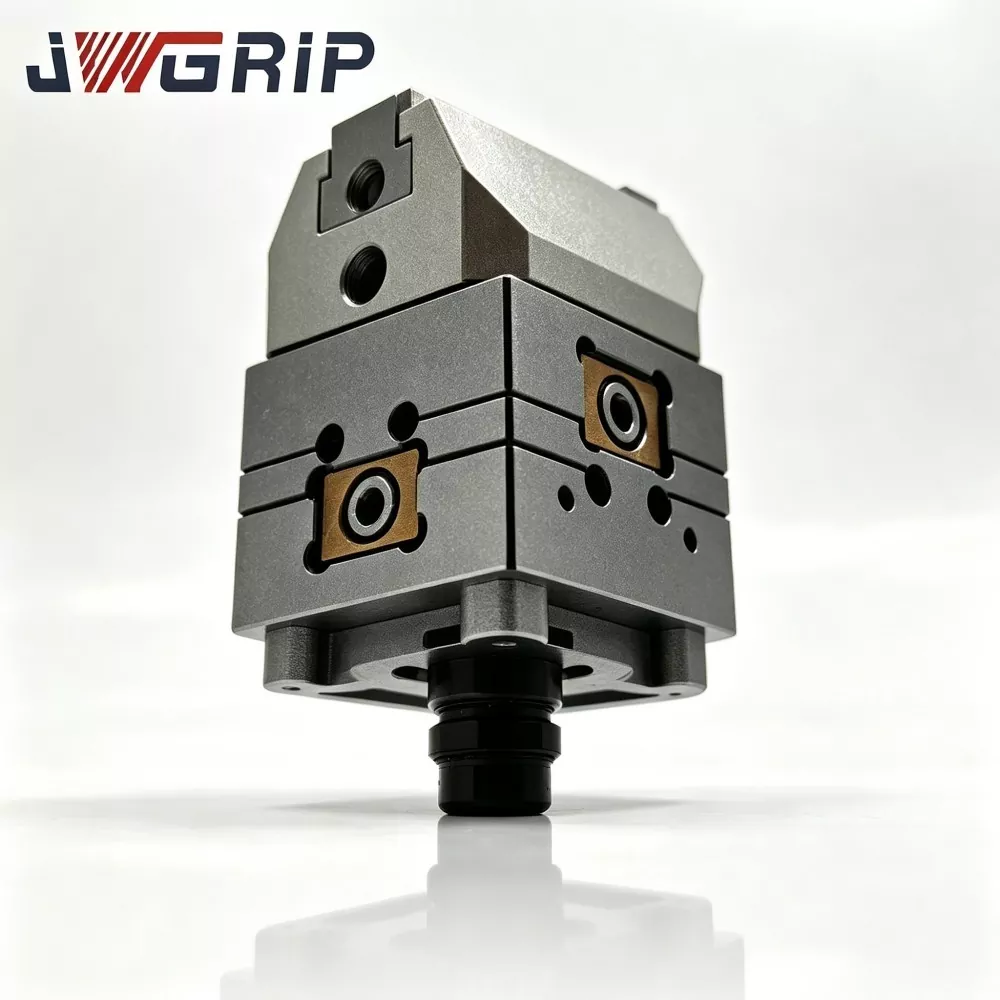
Geometric Realization
JWGRIP TP UnoSet Vee Vise for Wire EDM adopts symmetric dual-V-groove locating principle targeting cylindrical blanks. Two groups of inclined V-shaped working faces constitute angular locating supports. When cylindrical round-bar is placed onto dual-V inclined surfaces, gravity plus clamping force push cylinder to slide along inclined planes until stable three-point contact status is achieved. The geometric axis of cylindrical workpiece automatically converges toward theoretical central position defined by V-groove geometry.
Functional Boundary
Important functional boundary clarifications:
This mechanical self-centering acts upon outer-diameter cylindrical surfaces. It compensates limited-range out-of-roundness error of raw bar stock, yet cannot correct inherent eccentricity between outer circle and inner hole on pre-machined hollow-shaft parts.
The Unoset interface transfers this V-groove central datum into wire-EDM machine Unoset work-table datum-chain. Operators still need simple probe verification after fixture installation. Mechanical self-centering works as auxiliary locating means and cannot fully replace probe-based measuring compensation for final high-precision wire-cut manufacturing.
Core Performance Highlights
1. Symmetric Precision-ground Dual-V-groove Self-centering Structure Comparative batch-clamping lab test data shows: under identical round-bar outer-diameter tolerance scope, JWGRIP TP Unoset Vee Vise cuts manual concentric-setting time by approximately 61 % versus conventional flat-jaw vises for successive round-bar batches. V-groove working-surfaces receive ultra-precision grinding to guarantee stable three-point contact condition.
2. Cryogenically-stabilized Alloy-steel Main-body Main-body undergoes cryogenic treatment plus multi-round stress-relief tempering. Within workshop ambient-temperature 15-32 ℃, main-body datum-plane flatness variation ≤0.0028 mm, restraining thermal-deformation risk under temperature-fluctuating wire-EDM-tank conditions.
3. Plasma-nitrided V-groove Locating Surfaces V-groove inclined functional surfaces complete local plasma-nitriding hardening, surface hardness reaches HV840-950. It improves wear-resistance against wire-cut carbon powder and metal-particle erosion over long-time submerged batch-production. Whole-unit passivation anti-rust finish resists dielectric-fluid splash-triggered corrosion.
4. Native Unoset Standard Interface Bottom locating and locking features strictly comply with Unoset specifications. It realizes datum inheritance with existing Unoset fixture library on wire-EDM equipment and avoids repeated full-scale datum reconstruction work.
5. Adjustable Clamping-stop Configuration Fitted with removable adjustable axial stop-block, it controls axial position of round-bar blanks and facilitates batch-production of parts with consistent length dimension.
6. Flexible ODM Custom-engineering Capacity As ODM-capable manufacturer, JWGRIP can adjust V-groove included-angle, effective opening width, variant Unoset interface and stop-block layout according to customer technical drawings for special shaft-blank automated-cell demands.
7. Complete Serial-number Traceability Every finished JWGRIP TP Unoset Vee Vise carries laser-etched unique serial number. Full inspection datasets covering V-groove geometric accuracy, datum-flatness and self-centering repeat-test records are archived for enterprise-oriented quality management.
Complete Production Craft
1. Incoming raw-material composition & hardness inspection
2. CNC rough-milling for main-body and V-groove blank
3. Cryogenic stabilization treatment
4. Multi-round stress-relief tempering
5. Semi-finish machining
6. Symmetric dual-V-groove forming
7. V-groove slope local plasma-nitriding hardening
8. Multi-face ultra-precision grinding (V-groove faces, bottom Unoset datum plane)
9. Unoset locating-pin & locking-hole finish-machining
10. Adjustable stop-block component processing
11. CMM multi-item geometric-profile scanning
12. Round-bar self-centering repeat-simulation test
13. Laser serial-number marking
14. Whole-unit anti-rust passivation
15. Final visual + dimensional recheck
16. Finished-product warehousing
Installation Guide
1. Prior to mounting JWGRIP TP Unoset Vee Vise onto wire-EDM Unoset work-table, fully clean machine Unoset locating features and vise-bottom Unoset datum-surface; clear away wire-cut sludge, metal chips and dielectric-fluid residues. Trapped foreign particles cause vise-body tilt and spoil locating datum.
2. Tighten Unoset locking-bolts at recommended torque value; over-torque fastening brings micro-warping on main-body datum-plane.
3. Thoroughly clean dual-V-groove slopes before placing round-bar work-piece; remove tiny hard-particles staying inside V-groove valley, particles will impair self-centering accuracy.
4. Gently place cylindrical blank onto dual-V-groove, adjust removable axial stop-block to constrain bar axial position, then complete clamping movement. Never hammer-strike round-bar to force seating.
5. After clamping completion, perform simple probe verification for workpiece central position before executing formal wire-cut program. Mechanical self-centering cannot fully substitute probe-based coordinate fine-compensation.
6. After tank-production work finishes: take vise out when necessary, thoroughly rinse dual-V-groove to wash-off sludge debris, dry all reference-surfaces completely for storage.
Solution Evaluation
Three mainstream work-holding alternatives for wire-EDM cylindrical shaft-blanks:
ordinary flat-jaw vise, loose separate V-block without Unoset interface, JWGRIP TP UnoSet Vee Vise for Wire EDM.
1. Centering efficiency: Flat-jaw vise demands manual re-dial-indicating for every new bar. Discrete V-blocks deliver V-type locating yet lack Unoset datum inheritance. Our integrated vise combines dual-V-groove self-centering and native Unoset quick-change interface, shortening overall setup time for shaft-part batches.
2. Submerged-environment durability: Many loose V-blocks only receive ordinary quenching; V-slope suffers fast wear under wire-cut-sludge erosion. JWGRIP V-groove applies plasma-nitriding hardening plus whole-unit passivation anti-rust finish to extend service-life inside tank-working scenarios.
3. Datum-chain continuity: Flat-vise and separate V-blocks cannot inherit Unoset fixture datum; each installation triggers full datum-rebuilding. Built-in Unoset interface on JWGRIP vise shares machine-side Unoset reference with rest on-site tooling library.
4. Inspection standard: A great many suppliers only perform simple dimensional spot-check. Each JWGRIP unit completes CMM V-groove profile scanning plus round-bar self-centering repeat-simulation test. ODM custom-orders also receive dedicated-feature validation.
5. Custom-realization capacity: Numerous factories merely sell fixed-standard-size V-blocks / vises. Supported by mature ODM workflow, JWGRIP adjusts V-groove angle, applicable bar-diameter scope and variant Unoset interface for special shaft-blank automated-cell projects.
FAQ
Q1: Can JWGRIP TP UnoSet Vee Vise for Wire EDM fully eliminate concentric error originating from raw-stock bar out-of-roundness?
A: Dual-V-groove self-centering mechanism can absorb limited-magnitude raw-stock out-of-roundness. It cannot counteract heavy oval-shape deformation on severely defective bar blanks. Probe coordinate fine-verification after clamping remains mandatory for high-precision shaft-part assignments.
Q2: Can this vise realize positioning correction for hollow-shaft parts carrying large inherent eccentricity between outer-circle and inner-hole?
A: JWGRIP TP Unoset Vee Vise accomplishes positioning relying on workpiece outer-cylindrical surface. It reproduces existing outer-circle geometric center and cannot amend pre-existing eccentricity between outer-circle and inner-hole of hollow-shaft blanks.
Q3: If non-standard V-groove angle, special bar-diameter scope or variant Unoset interface is needed, can you provide ODM custom-engineering?
A: Yes. Please submit complete technical-drawings with clear requirements covering V-groove included-angle, applicable round-bar diameter scope, mounting-interface dimension and tolerances. Our engineering-department will finish manufacturability assessment and issue formal quotation feedback within 12 working-days.
Q4: Which failure modes fall under product-warranty scope?
A: JWGRIP TP UnoSet Vee Vise for Wire EDM belongs to high-precision submerged-environment work-holding fixture for wire-EDM. Warranty covers manufacturing-origin defects existing at time-of-delivery such as out-of-spec V-groove geometry and datum-flatness non-conformity. Damages brought by hammer-impact, foreign-particle jamming, dielectric-fluid-sludge erosion and normal cyclic-usage-wear are excluded out-of-warranty terms.
Hot Tags: TP UnoSet Vee Vise for Wire EDM
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.