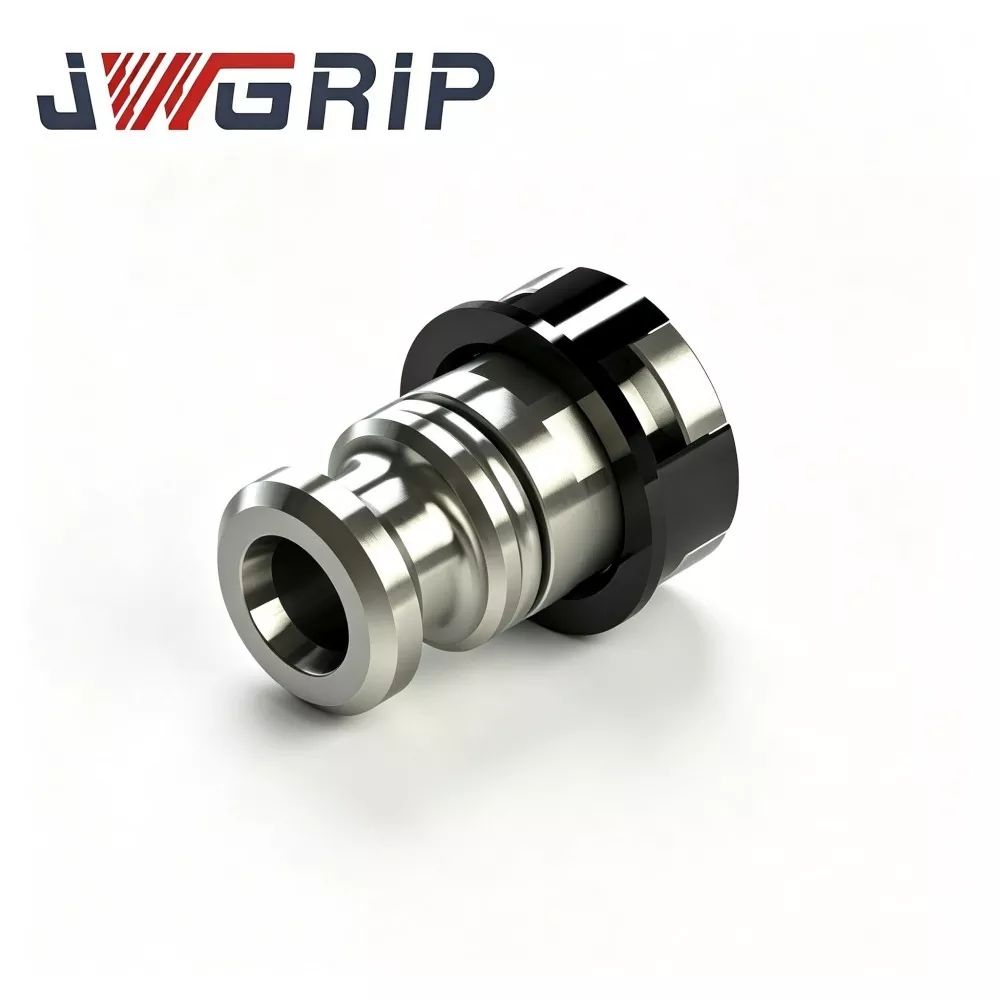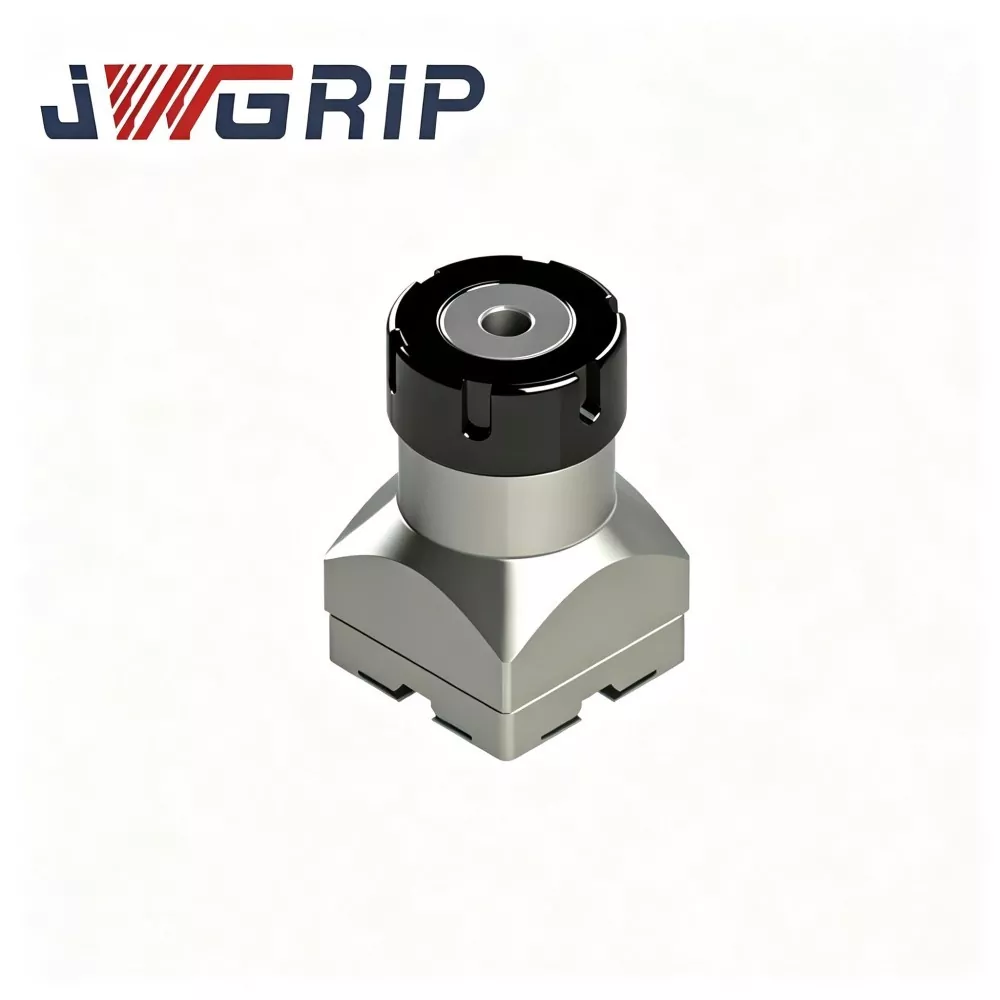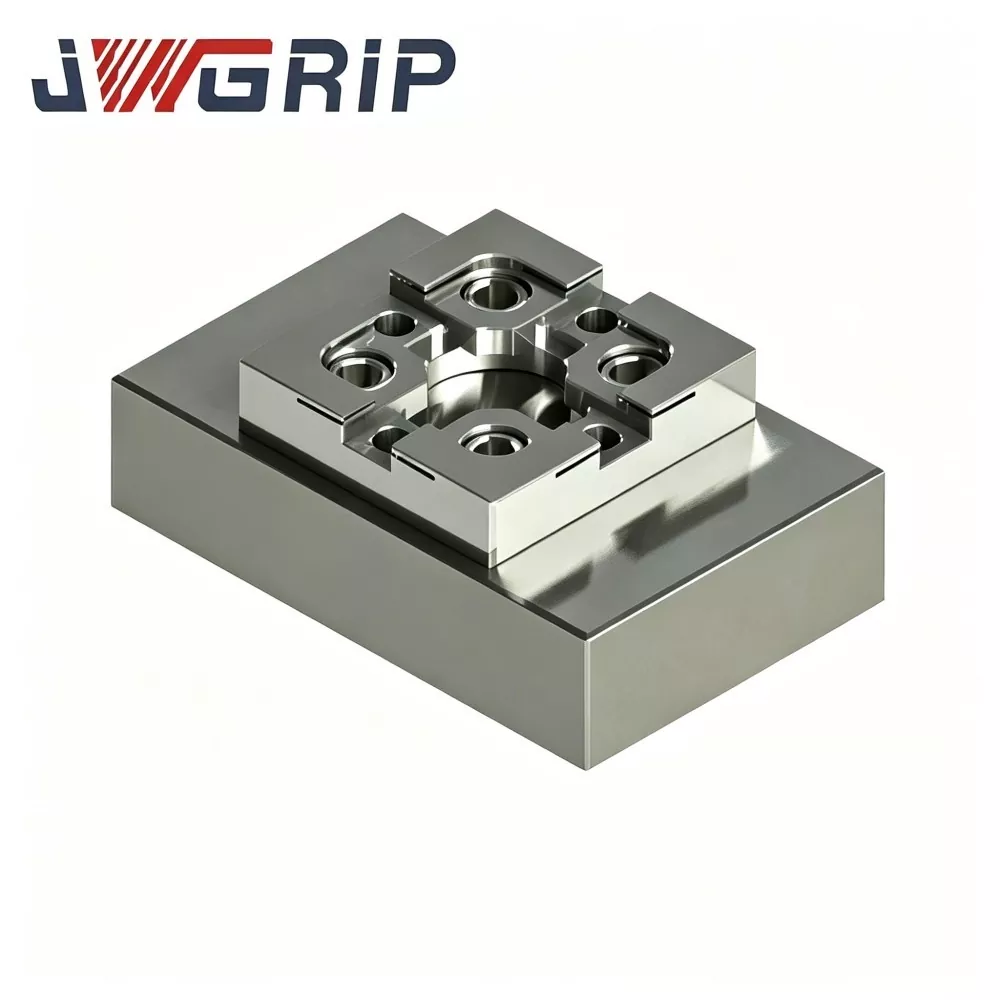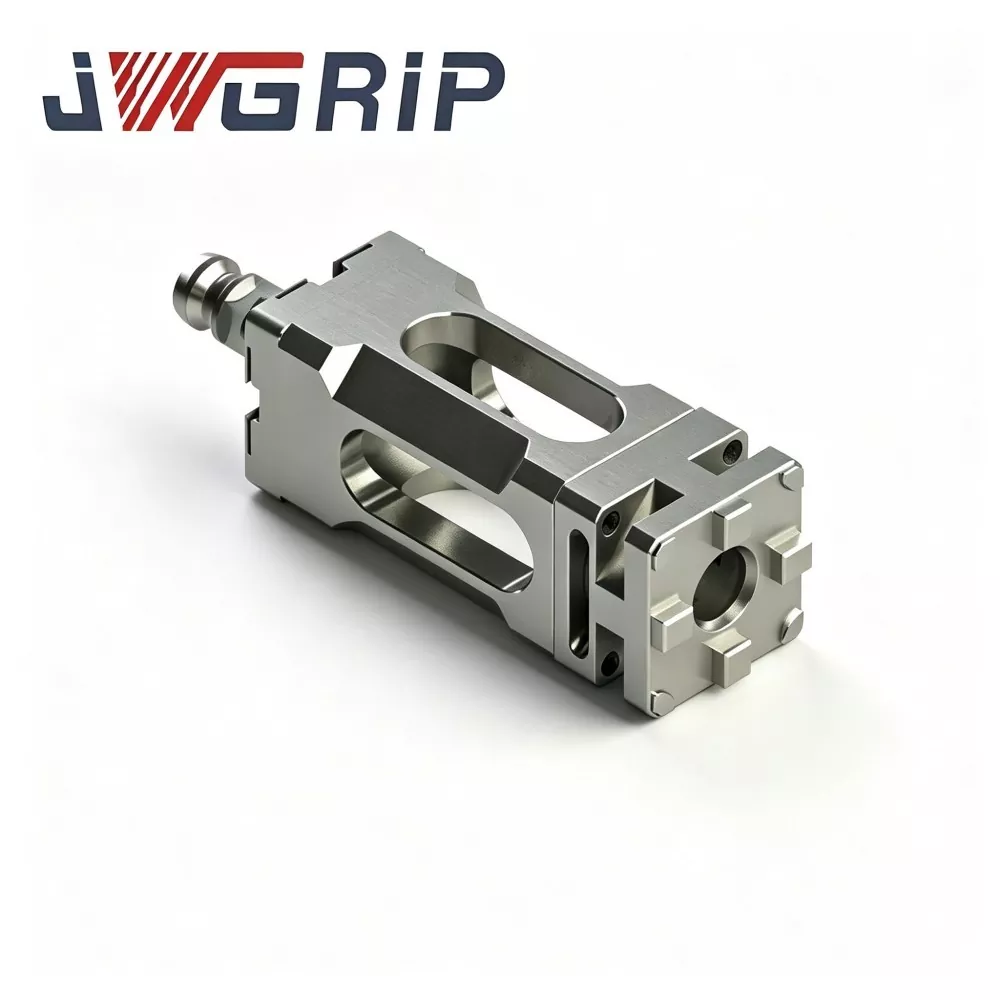
R-Type Extension Rod for EDM Electrode Holder
JWGRIP is the professional manufacturer and supplier of R-Type Extension Rod for EDM Electrode Holder in China, providing Customized dimensional modification service with multiple standard specifications fully in Stock. It is a professional high-precision EDM tooling extension component specially designed for complex die-mold sinker machining deep cavity processing scenarios. It integrates high-rigidity structural design and ultra-precision coaxial positioning performance into a single integrated rod body, perfectly solving the problem of insufficient working stroke of standard electrodes in deep cavity machining.
This high-performance R-Type EDM Electrode Extension Rod adopts integrated high-strength high-alloy tool steel blank, processed through complete stress-relieving heat treatment and high-precision outer circle cylindrical grinding technology. It features excellent concentricity, ultra-low runout and outstanding structural rigidity, effectively suppressing electrode vibration and deflection caused by pulse discharge impact during high-speed EDM machining.
Different from ordinary extension rods with insufficient heat treatment and poor stability, R-Type Extension Rod for EDM Electrode Holder maintains long-term stable positioning accuracy after cyclic operation, without electrode position drift and cavity surface quality damage. It safely extends the effective working distance of electrodes, greatly reducing repeated tool-setting times and mold rework probability. Widely applicable to deep rib processing, sunken texture machining and complex cavity molding of precision molds, it provides stable and efficient auxiliary tooling support for modern mold EDM sinker production.
Practical Machining Pain Points
In modern mold-making sinker-EDM workshops, deep-recessed feature processing brings multiple practical obstacles:
· Standard-size electrodes fail to reach inner forming areas of deep-cavity mold structures. Shops have to fabricate extra-long one-piece electrodes. Such electrodes tend to vibrate and deflect under pulse-discharge impact, resulting in bad surface texture and dimensional deviation on finished mold cavities.
· Conventional low-cost extension-rod products lack sufficient heat-treatment procedures. After long-time cyclic operation, large run-out appears, which shifts electrode position and ruins cavity surface finishing.
JWGRIP optimizes this extension rod for above-mentioned pain-points:
1. One-piece high-strength high-alloy tool-steel blank is adopted. Complete stress-relieving heat-treatment removes internal residual stress.
2. Outer-circle and connecting reference surfaces are finished by high-precision cylindrical grinding to guarantee coaxiality between upper and lower connecting interfaces.
3. Enhanced structural rigidity suppresses electrode vibration during spark-discharge. Working length can be safely extended without sacrificing positioning accuracy.
4. Compatible with most mainstream EDM electrode holders and supports flexible combination for various cavity-depth requirements. Frequent repeated tool-setting operations get avoided, stabilizing machining consistency for deep ribs, concave textures and intricate cavities.
5. Besides standard dimensions, drawing-driven customized dimensional modification is available for special-depth electrode application scenarios.
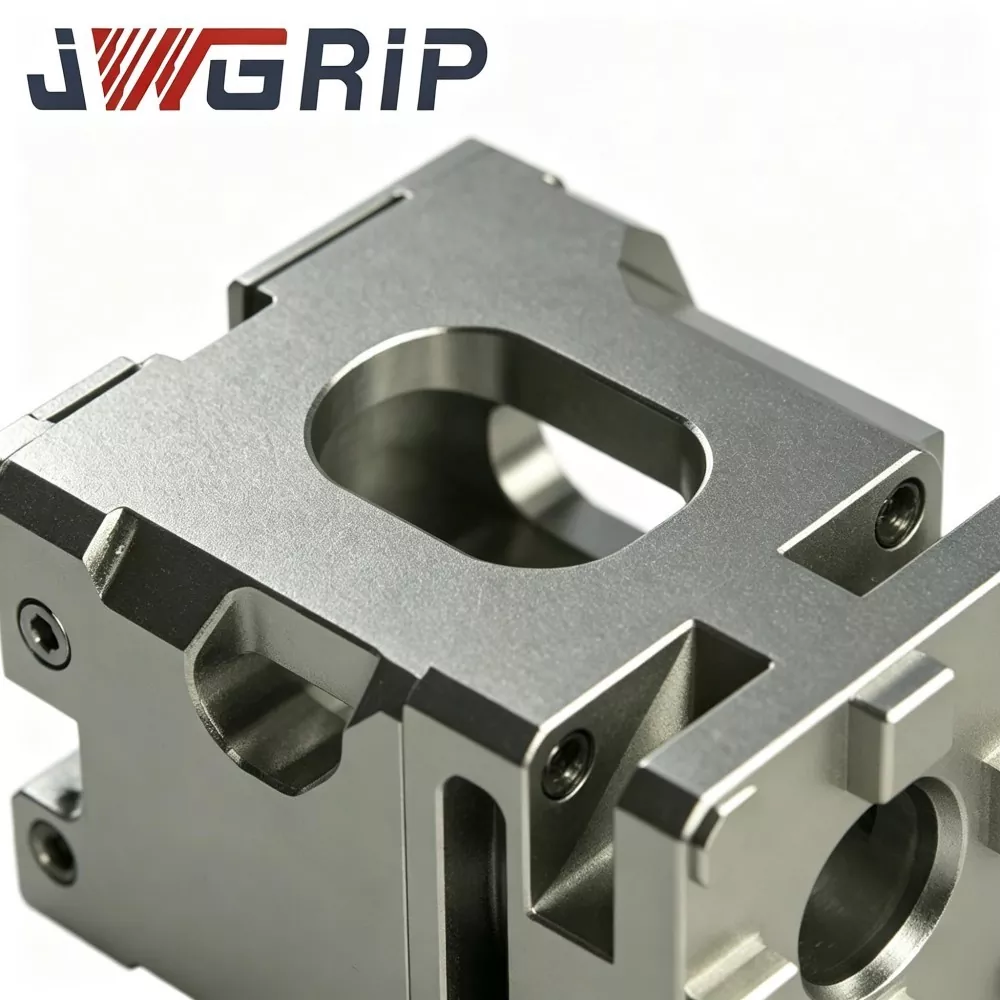
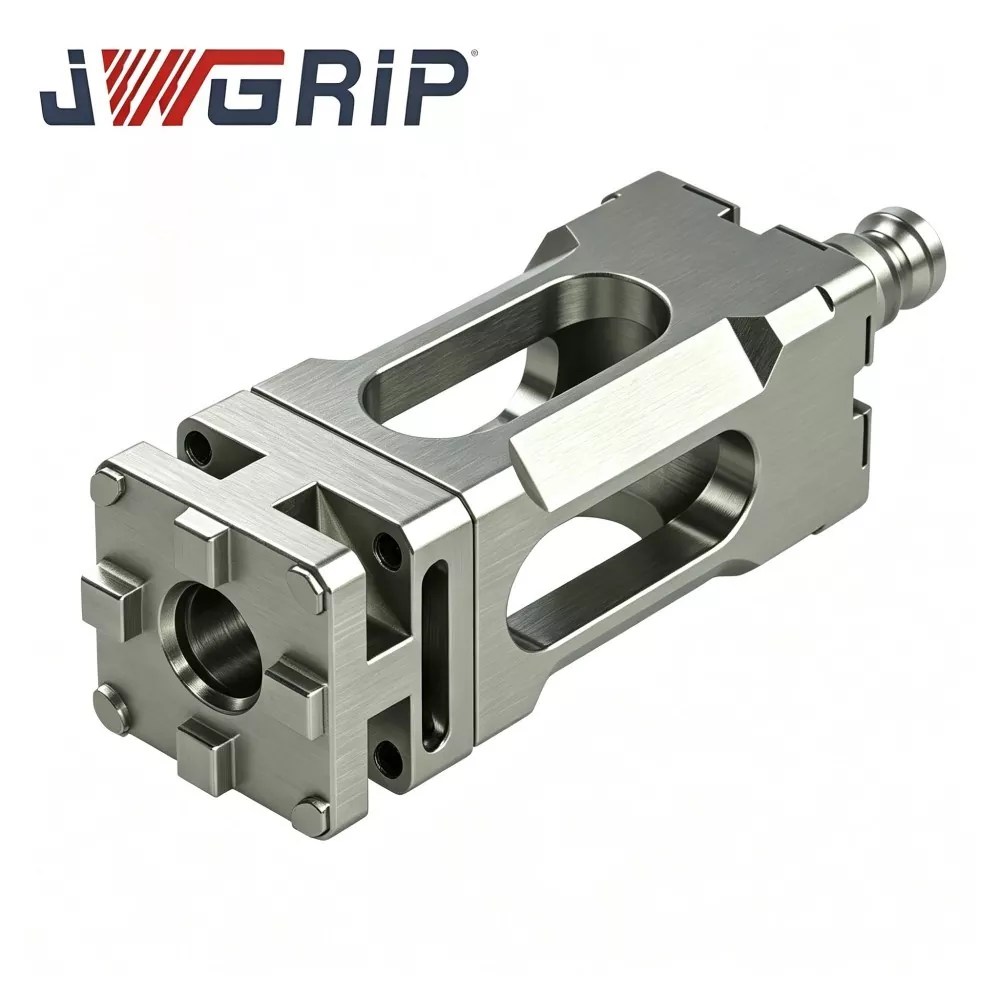
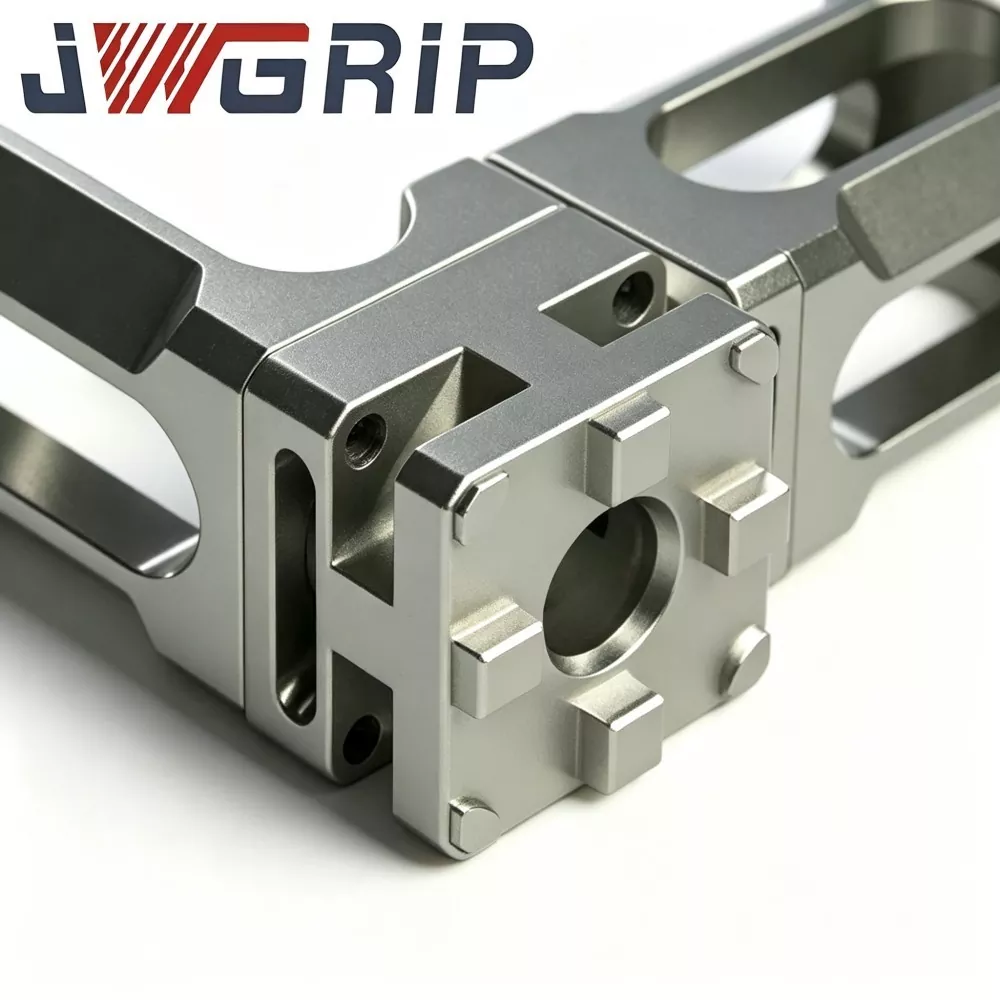
Structural Characteristics
JWGRIP R-Type Extension Rod for EDM Electrode Holder functions as precision intermediate connecting spacer for sinker-EDM equipment:
1. It installs between EDM electrode holder and working electrodes including copper, graphite and copper-tungsten materials.
2. When processing deep mold cavities, narrow ribs and sunken features, this rod raises electrode mounting datum and extends electrode outreach so electrodes can reach hard-to-access machining zones.
3. Unlike simple straight lengthening sleeves, R-type transition-fillet structural layout optimizes stress distribution under discharge vibration, lowering bending-deformation and run-out-drift risks.
Core Functional Performances
1. Rigorous Concentricity & Run-out Control Outer-circle grinding process is applied for finished parts. Total run-out is strictly controlled ≤0.002 mm. Low run-out prevents uneven spark gap and eliminates abnormal over-erosion defects on mold-cavity surfaces.
2. Optimized R-type Mechanical Construction Transition-fillet design reduces local stress concentration. Under continuous EDM pulse-discharge vibration, the rod maintains stable structural rigidity and is less susceptible to bending deformation compared with ordinary straight-type lengthening sleeves.
3. Mature Alloy-steel & Heat-treatment Technology High-alloy tool-steel material with quenching-and-tempering heat-treatment achieves surface hardness HRC 42-46. Surface anti-oxidation treatment mitigates corrosion risk caused by EDM dielectric fluid, improving service-life under long-term workshop conditions.
4. Broad Universal Interface Compatibility Interface dimensions comply with mainstream EDM electrode-holder industrial standards. It fits most sinker-EDM machine-tool brands on market; users need not purchase special modified holders.
5. Flexible Dimensional Custom-ization Solution Full range of mainstream standard lengths in stock. Outer diameter, connecting thread and overall length can be adjusted per customer drawings or physical samples to solve non-standard deep-cavity machining challenges.
6. Stable Batch-to-batch Interchangeability Dimension and batch number are marked on each single unit. Replacement spare parts keep consistent assembly precision for mass-production mold workshops.
Application Scenarios
JWGRIP R-Type Extension Rod for EDM Electrode Holder is widely deployed for sinker-EDM tasks inside mold-making factories:
· Plastic injection mold: deep gate inserts, deep thin-wall cavities, deep-rib feature machining. Household-appliance mold factories adopt this rod for deeply sunken textured cavities and avoid electrode self-collision.
· Die-casting mold: deep-recessed logos, characters and complex slide-insert spark-erosion processing.
· Precision stamping mold: small deep-hole EDM machining for stamping-die inserts.
· Medical & optical mold: high-precision micro-cavity which demands stable concentricity under extended outreach condition.
Production Workflow & Quality Rules
Each production batch of JWGRIP R-Type Extension Rod for EDM Electrode Holder follows standardized full-process control: Raw-material incoming inspection → CNC preliminary machining → heat-treatment → precision outer-circle grinding → thread finishing → concentricity & run-out test → surface anti-oxidation treatment → final dimensional re-inspection → warehousing.
· All key dimensional data are recorded inside batch inspection reports.
· Our factory holds ISO 9001 quality-management-system certification. Third-party material test reports can be provided upon client request.
· All run-out inspection measuring instruments go through periodic calibration to secure measurement accuracy.
Why Partner With JWGRIP
1. Practical EDM-tooling Development Experience Our engineering team has long-term experience in EDM accessory development. We focus on real-site mold-shop pain-points rather than only executing theoretical drawing parameters.
2. Strict Full-batch Run-out Screening Many low-cost competitors skip full-batch concentricity testing and cause unstable spark gaps. Every finished JWGRIP extension-rod passes run-out inspection before shipment.
3. Fast Custom-project Response For non-standard dimension requests, engineering team completes drawing review within 12 working-days and delivers feasible technical feedback. Standard-spec items can be delivered within 10-15 working-days.
4. Complete After-sales Technical Back-up Technical-support team provides installation guidance and troubleshooting advice when customers encounter assembly or machining anomalies.
5. Traceable Batch-management Mechanism Every single rod carries clear batch marking. Once machining abnormalities emerge, production-and-inspection records can be quickly traced for technical root-cause analysis.
Product Packaging
1. Single-unit packing: Each JWGRIP R-Type Extension Rod for EDM Electrode Holder is protected by anti-scratch protective sleeve first, then placed inside individual plastic tool-case to avoid impact damage in transit.
2. Bulk-order packing: Carton box filled with foam cushioning material.
3. Logistics service: Cooperate with professional international freight forwarders for sea-freight and air-freight arrangements.
4. Attached documents: Packing list and batch-inspection documents can be enclosed with goods upon request.
FAQ
Q1: Will JWGRIP R-Type Extension Rod bring obvious vibration during high-speed EDM discharge?
A1: Under correct clamping status, optimized R-type structure plus ≤0.002 mm run-out restrain vibration. Excessive vibration usually comes from improper clamping torque, bent electrode or over-long total outreach. We recommend the total outreach (rod + electrode) should not exceed 150 mm for stable machining output.
Q2: Can this extension-rod work with heavy graphite electrodes?
A2: R-Type Extension Rod for EDM Electrode Holder supports graphite-electrode usage. For large-size heavy graphite electrodes, you must evaluate spindle load and total outreach. Excessive weight accelerates holder-thread wear and degrades machining accuracy.
Q3: My connecting-thread dimension is non-standard. Can you make customized R-Type Extension Rod?
A3: Yes. Please provide technical drawing or physical sample, mark thread specs, overall length, outer diameter and concentricity tolerance requirements. Our engineers will confirm manufacturability and formal quotation.
Q4: What is the warranty policy for this extension-rod?
A4: This belongs to precision consumable tooling. Warranty covers manufacturing-originated defects such as out-of-spec run-out on delivered goods. Damage caused by collision, wrong clamping torque and overload usage is not covered by warranty.
Hot Tags: R-Type Extension Rod for EDM Electrode Holder, Manufacturer, Supplier
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.