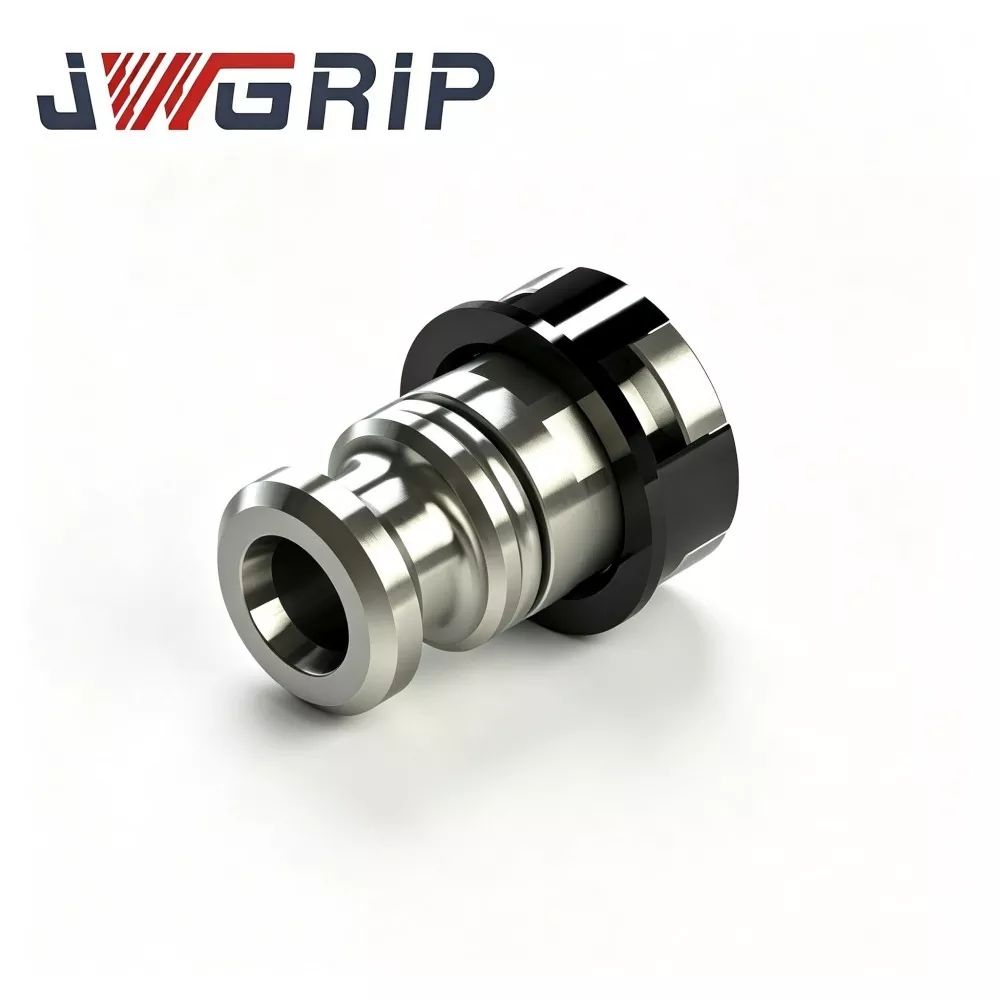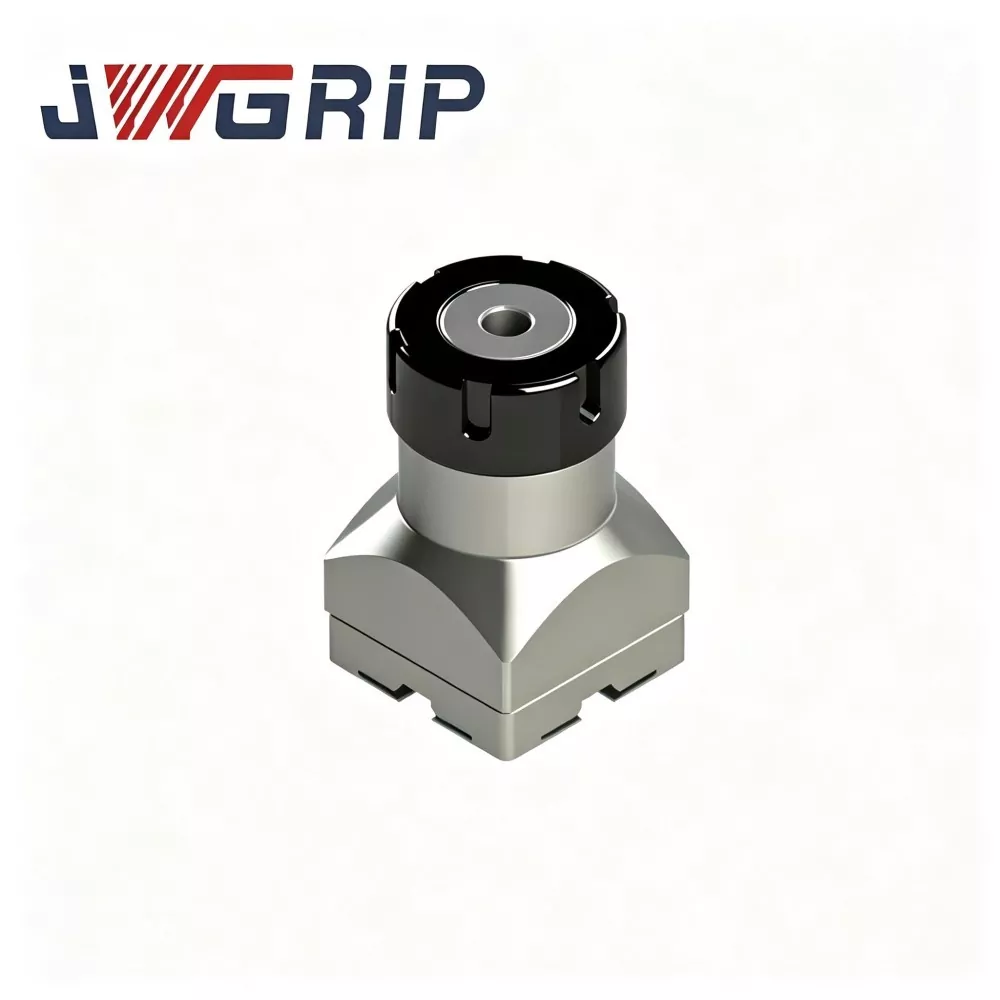
R-Type ER32 Collet for EDM Electrode Holder
JWGRIP is the professional manufacturer and supplier of R-Type ER32 Collet for EDM Electrode Holder in China, providing Factory Direct supply and mature OEM modification service for global sinker EDM mold-making enterprises. It is a high-performance EDM-specific elastic clamping accessory specially optimized for spark erosion machining working conditions. Integrating optimized R-type force balance structure and high-precision elastic clamping performance into a single unit, it solves the common defects of ordinary general-purpose collets such as uneven stress and easy precision attenuation.
This advanced R-Type ER32 Collet is made of premium high-grade spring steel material, processed through multiple precision turning, internal hole honing and complete cyclic stress-relieving heat treatment. It features stable clamping force retention, excellent roundness accuracy and reliable elastic fatigue resistance under long-term continuous EDM pulse discharge shock. The optimized R-type structural profile realizes uniform force transmission on the inner hole surface, effectively minimizing electrode run-out error during clamping. It is universally applicable to copper, graphite and copper-tungsten electrodes, perfectly adapting to long-run mold cavity precision machining scenarios.
Different from ordinary collets that are prone to roundness distortion and clamping force attenuation after repeated opening and closing cycles, R-Type ER32 Collet for EDM Electrode Holder avoids electrode micro-slippage, spark gap imbalance and mold cavity dimensional deviation. Supporting standard spot supply and customized modification of inner bore tolerance, groove parameters and surface finishing, it provides stable, high-precision and durable clamping solutions for modern precision mold EDM processing workshops.
Production Pain Points
In daily sinker-EDM mold-making production, ordinary off-the-shelf ER collets create several common manufacturing headaches:
Simplified raw-material and cutting-heat-treatment workflows lead to roundness distortion and clamping-force attenuation after frequent elastic open-close cycles.
Under continuous pulse-discharge impact, electrodes produce micro-slip and run-out drift. Spark gap becomes uneven, bringing inconsistent cavity texture, dimensional deviation and scrap risk for high-value mold electrodes.
JWGRIP optimizes R-Type ER32 Collet targeting above-mentioned pain-points:
1. High-grade spring-steel raw-material plus multi-round stress-relieving heat-treatment eliminates internal residual stress generated in turning and honing, preventing permanent deformation in long-term elastic cyclic work.
2. Optimized R-type contour design distributes clamping force evenly over whole inner-hole surface. It performs stably for soft-copper, brittle-graphite and high-density copper-tungsten electrodes.
3. Matches existing mainstream ER32 electrode-holder bodies, avoiding excessive fixture-renewal investment.
4. Standard specifications are in stock; OEM modification for inner-bore tolerance, groove structure and surface treatment is available for special-diameter electrodes and harsh working-conditions.
5. Effectively lowers electrode-slippage and run-out risks, stabilizes spark-gap status during long-time cavity-machining tasks.
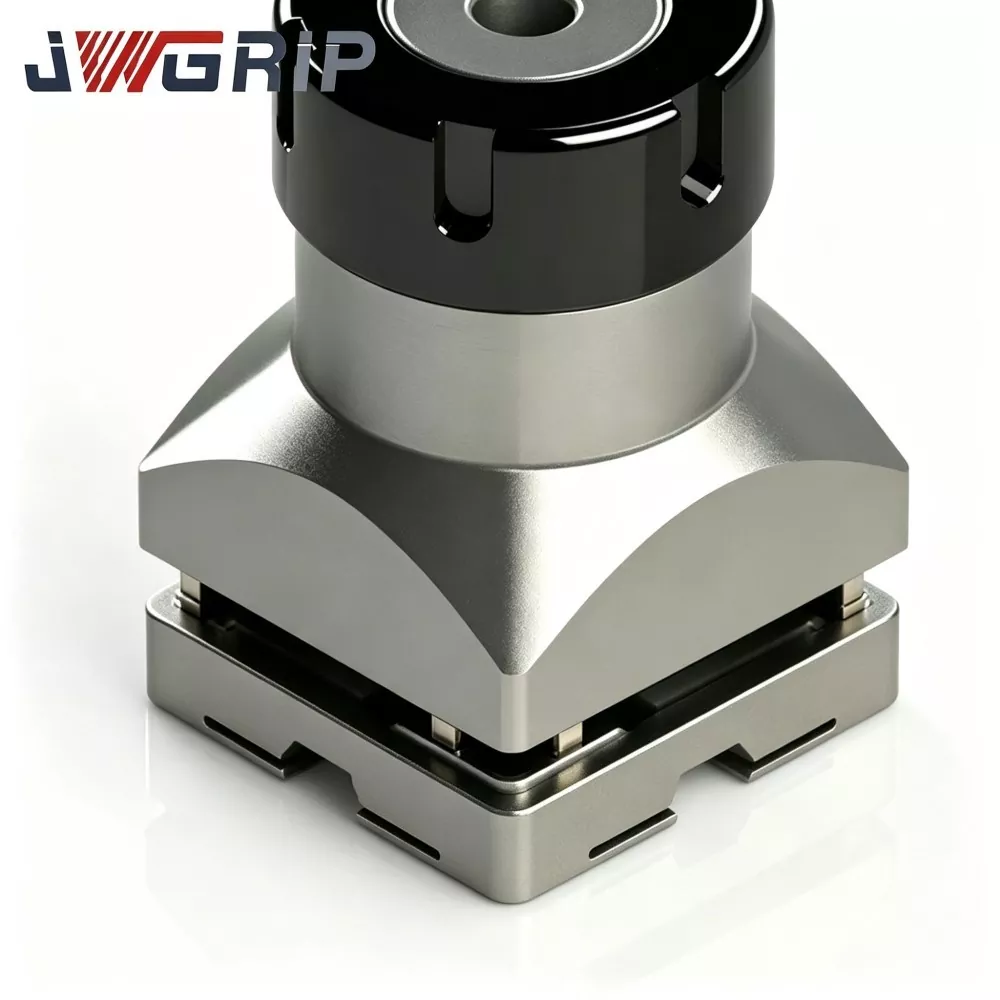
Structural Features
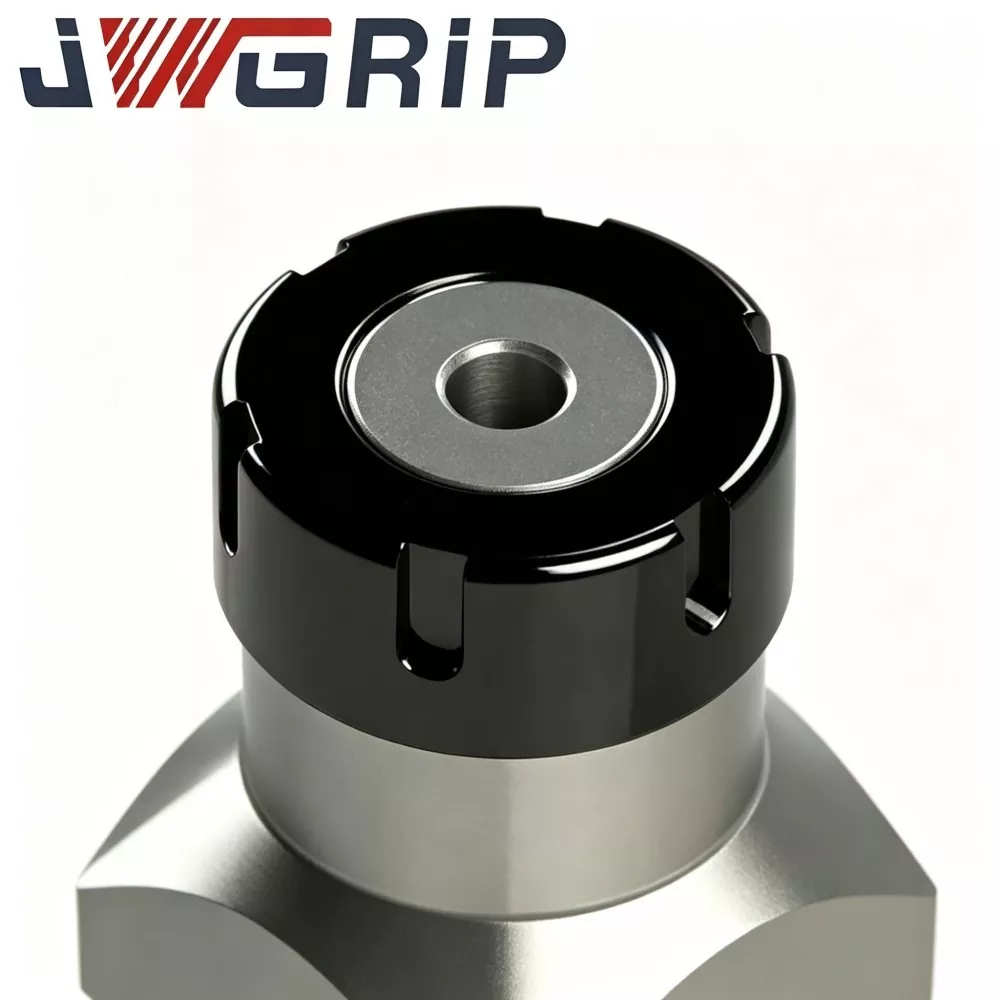
JWGRIP R-Type ER32 Collet for EDM Electrode Holder is a high-precision elastic clamping component exclusively engineered for sinker-EDM electrode-holder assemblies:
1. Installed inside ER32 holder nut and holder main-body. When holder nut is tightened, it delivers uniform circumferential squeezing force to lock round-shank electrodes in preset position.
2. Conventional universal ER32 collets are originally designed for CNC-milling spindles; they are not optimized for EDM-specific conditions: continuous pulse vibration, dielectric-fluid splashing and frequent electrode swapping.
3. Improved R-type slit-groove layout redistributes elastic stress across collet body, reduces local stress concentration and improves elastic-recovery performance after repeated open-close cycles, maintaining low run-out under continuous EDM operation.
Application scope: It is a core consumable for plastic-injection-mold, die-casting-mold, precision-stamping-die, medical-part-mold and optical-component-mold workshops. It clamps round-shank copper, graphite and copper-tungsten EDM electrodes. Direct drop-in installation without extra mechanical alteration. OEM drawing-based modification is supported for non-standard electrode-shank dimensions.
Key Technical Performances
1. Optimized R-Type Slit-groove Distribution Structure Compared with ordinary ER32 collets, rearranged R-type slit-groove layout balances elastic-stress distribution. During electrode-shank clamping, each section generates homogeneous squeezing force, avoids local electrode-shank deformation and suppresses total assembly run-out of electrode clamping unit.
2. Carefully-selected Spring-steel Raw-material Adopts special spring-steel instead of ordinary carbon-steel. After precise quenching, tempering and multi-stage stress-relieving thermal cycles, it keeps stable elasticity after hundreds of clamp-release cycles and resists permanent plastic deformation.
3. High-precision Inner-hole Honing Craft Inner clamping bore goes through fine honing. Excellent inner-hole roundness and surface smoothness reduce abrasion marks on electrode shanks during repeated swapping, and prevent micro-particle accumulation which would worsen positioning deviation.
4. Good Dielectric-fluid Corrosion Resistance Special surface anti-corrosion treatment slows chemical erosion from long-term contact with EDM dielectric fluid. It lowers rust risk inside humid EDM-tank environment and extends service life.
5. Wide Compatibility with Standard ER32 EDM Holders Follows basic ER32 outer-dimension standards, fits most commercial ER32-form EDM electrode-holder bodies and clamping nuts. End-users need not replace existing holder hardware.
6. Flexible Factory-direct & OEM Custom-ization Standard clamping-diameter specifications cover mainstream electrode-shank sizes. OEM can adjust inner-bore tolerance, slit-groove depth, outer-dimension fine-tuning and surface-treatment according to customer drawings or physical samples.
7. Reliable Batch-to-batch Consistency Every production lot carries multi-item sampling inspection. Key dimension, clamping run-out and hardness data are recorded in batch-inspection files, guaranteeing stable performance for volume-purchase mold-making enterprises.
Complete Production Workflow
Every batch of JWGRIP R-Type ER32 Collet follows strictly-controlled full-step manufacturing workflow:
① Raw-material incoming inspection
② CNC precision turning for outer contour
③ slit-groove milling
④ high-precision inner-hole pre-machining
⑤ multi-stage heat-treatment (quenching, tempering, stress-relief)
⑥ inner-hole fine honing
⑦ deburring & edge finishing
⑧ surface anti-corrosion treatment
⑨ multi-dimensional performance testing
⑩ batch sorting & finished-goods warehousing.
Quality-control Specifications
Production is performed under ISO 9001 quality-management-system standards.
Core test items: dimension measurement, hardness verification, clamping run-out detection, elastic-fatigue simulation test.
All measuring tools get periodic metrological calibration to secure test-result authenticity and repeatability.
Batch-inspection reports are archived for each lot; material certificates and partial third-party test records can be supplied upon client request.
Operational & storage suggestion:
Store collets in separated anti-collision tool-box compartments. Keep away from dampness, metal chips and hard scratching before installation. Clean inner-bore thoroughly before each mounting. Chips or dielectric-fluid residue inside bore will seriously degrade clamping precision.
Why Choose JWGRIP
1. EDM-specialized Tooling R&D Background Engineering team accumulates rich experience on sinker-EDM clamping-accessory development. We do not simply copy milling-type collet designs; product optimizations derive from massive front-line mold-technician feedback.
2. Full-batch Performance Screening Before Shipment Many competitors only perform spot sampling inspection. Every finished JWGRIP R-Type ER32 Collet passes clamping-run-out detection before delivery to filter non-conforming units.
3. Stable Factory-direct Supply & Mature OEM Process Standard-spec goods maintain stable delivery. For dimension-modified or special-surface-requirement orders, engineering team reviews OEM drawings within 12 working-days and gives feasibility feedback. Standard lead-time:10-15 working-days; OEM lead-time is confirmed according to drawing complexity.
4. Application-oriented Professional Technical-support When customers encounter abnormal clamping, excessive run-out and other on-site assembly troubles, technical-support team provides practical installation guidance and troubleshooting based on real EDM-workshop experience.
5. Complete Batch Traceability Mechanism Each production lot carries independent batch marking. If unexpected machining-related problems occur, original production-parameters and inspection-records can be quickly retrieved for root-cause technical analysis.
FAQ
Q1: Can JWGRIP R-Type ER32 Collet realize zero run-out after installation?
A1: Zero run-out cannot be achieved by any elastic-collet assembly. Under standard test-condition with matched holder and qualified test-bar, assembled run-out is controlled ≤0.003 mm. Actual machine-mounted total run-out is also affected by electrode-shank roundness, surface condition, nut-tightening torque and holder-body wear. Keep mating components in good condition for best clamping-accuracy.
Q2: Is this collet suitable for heavy-weight large-diameter graphite electrodes?
A2: R-Type ER32 Collet for EDM Electrode Holder supports graphite-electrode clamping. For large-size heavy graphite electrodes, evaluate spindle load and tightening-torque. Excessive weight or over-tightening accelerates collet elastic-fatigue and shortens service-life. Match electrode weight with collet clamping-capacity in real-world production.
Q3: Can you make OEM when clamping inner-diameter or slit-groove parameters differ from standard ER32?
A3: Yes. Please provide complete technical drawings or physical samples, mark clamping-bore dimension, tolerance, slit-groove specs, hardness target and surface-treatment requirements. Engineering department will evaluate manufacturability and issue formal quotation.
Q4: What items are covered under warranty?
A4: This is high-precision wearing consumable tooling. Warranty applies to manufacturing-originated defects such as out-of-spec run-out at time of shipment. Damage caused by scratch, overload clamping, improper torque, chip-jamming and long-term fatigue-wear from production usage is excluded from warranty.
Collet-selection Guide & Daily-workshop Operation Tips
1. Select nominal clamping-diameter as close as possible to real electrode-shank dimension. Do not use one collet for an excessively wide size range; large dimension gap creates uneven clamping pressure and higher run-out value.
2. Before formal mold production, fully clean collet inner-bore, holder-nut cavity and electrode-shank surface to remove metal chips and dielectric-fluid residue.
3. After assembly, perform run-out inspection by dial-indicator before spark-erosion processing. This pre-check greatly lowers mold-cavity scrap risk caused by clamping-component deviation.
4. For multi-machine mold-shops, prepare multiple collets corresponding to frequently-used electrode-shank sizes. Discard heavily-worn collets. Replace immediately if elastic weakening, permanent deformation or surface cracks are observed during routine inspection, even if theoretical service-life is not reached.
5. Implement classified storage and regular condition-check for collet stock to sustain stable EDM machining consistency for long-run serial-production projects.
Hot Tags: R-Type ER32 Collet for EDM Electrode Holder
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.