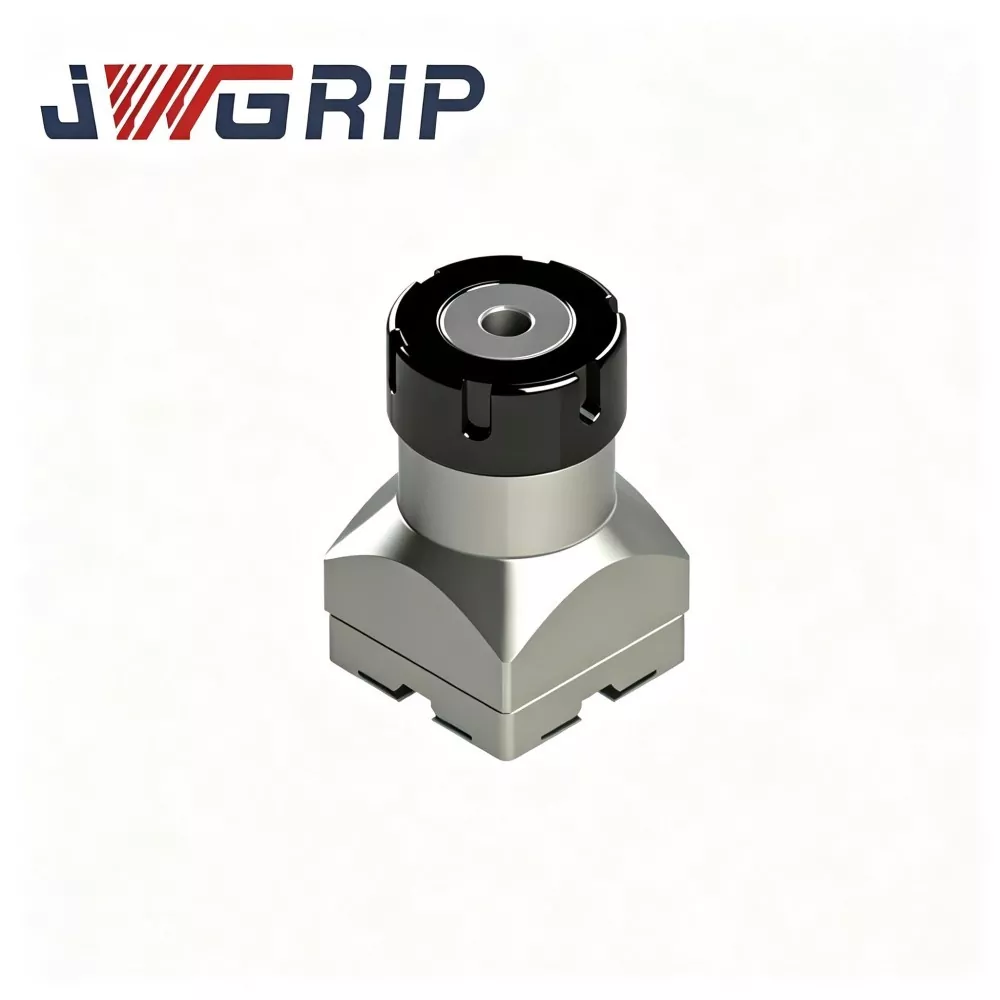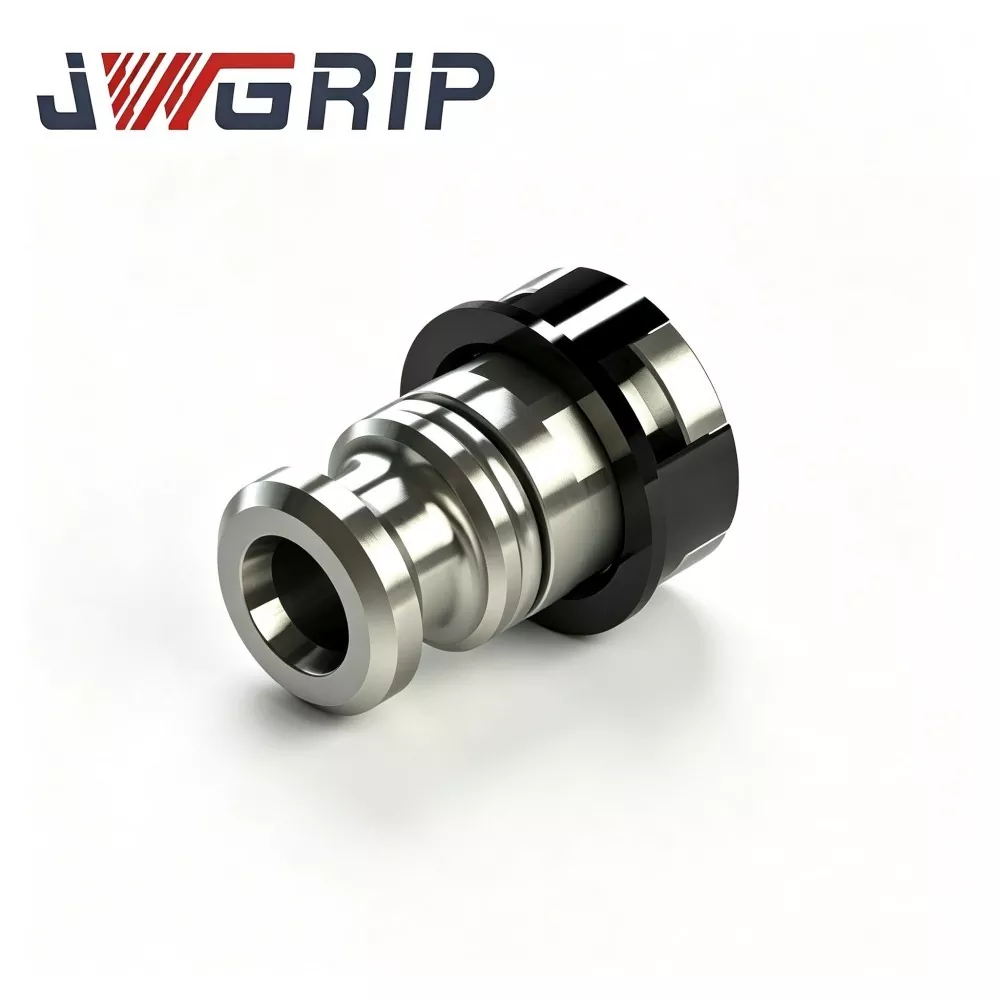
R-Type Pneumatic Drawbar for EDM Electrode Holder
JWGRIP is the professional manufacturer and supplier of R-Type Pneumatic Drawbar for EDM Electrode Holder in China, with standard specifications fully in Stock and accepting global Bulk Order for automated intelligent mold workshop projects. It is a high-reliability integrated pneumatic pulling component specially designed for unmanned automated sinker EDM production lines. It integrates optimized R-type stress-balanced force transfer structure and high-hardness anti-corrosion mechanical performance into a single device, eliminating tension attenuation, local stress concentration and easy wear defects of traditional straight-body drawbars.
This advanced R-Type Pneumatic Drawbar is constructed from high-strength alloy steel, processed through ultra-precision grinding and professional nitrogen hardening surface treatment, featuring excellent surface hardness, abrasion resistance and dielectric fluid erosion resistance. The upgraded R-type force transfer structure achieves uniform stress distribution during repeated clamping and releasing cycles, effectively reducing internal component fatigue wear and avoiding pulling force drift caused by long-term high-frequency pneumatic operation and EDM pulse vibration.
R-Type Pneumatic Drawbar for EDM Electrode Holder maintains stable and consistent pulling tension throughout mass unmanned production, minimizing electrode micro-displacement and spark gap deviation, and greatly improving mold cavity surface machining consistency. It effectively shortens electrode swap cycle time, reduces manual intervention and equipment calibration downtime.
Widely applicable to intelligent lights-out EDM manufacturing workshops, it supports standard batch supply and customized OEM modification of pulling force parameters, thread dimensions and mounting interfaces, providing stable and high-efficiency core connection solutions for automated EDM production cells.
Production Pain-points
Modern lights-out mold-making workshops encounter typical bottlenecks caused by ordinary pneumatic drawbars:
After thousands of automatic cycles, pull-force drifts and creates hidden electrode-loosening risk. Premature internal-part wear forces frequent production shutdown for maintenance.
Poor surface anti-corrosion performance leads to component jamming after long-time immersion in EDM dielectric fluid. Unexpected stoppages interrupt unattended machining and cause scrap on complex-cavity workpieces.
JWGRIP optimizes R-Type Pneumatic Drawbar for these real-site challenges:
1. High-strength alloy-steel body receives precision grinding and gas nitriding hardening, improving surface hardness, wear-resistance and dielectric-fluid corrosion-resistance.
2. Refined R-type force-transfer transitional-shoulder redistributes mechanical stress during repeated clamping-release strokes, mitigates internal-component fatigue and extends service-life.
3. Sustains steady pulling-tension across continuous automatic cycles, minimizing electrode positioning drift and securing consistent spark-erosion results.
4. Well-matched with mainstream automatic EDM electrode-holder assemblies, simplifies electrode-swap workflow and reduces manual intervention.
5. Drawing-based OEM modification for tension parameters, thread dimensions and mounting structures supports personalized automated-cell requirements.
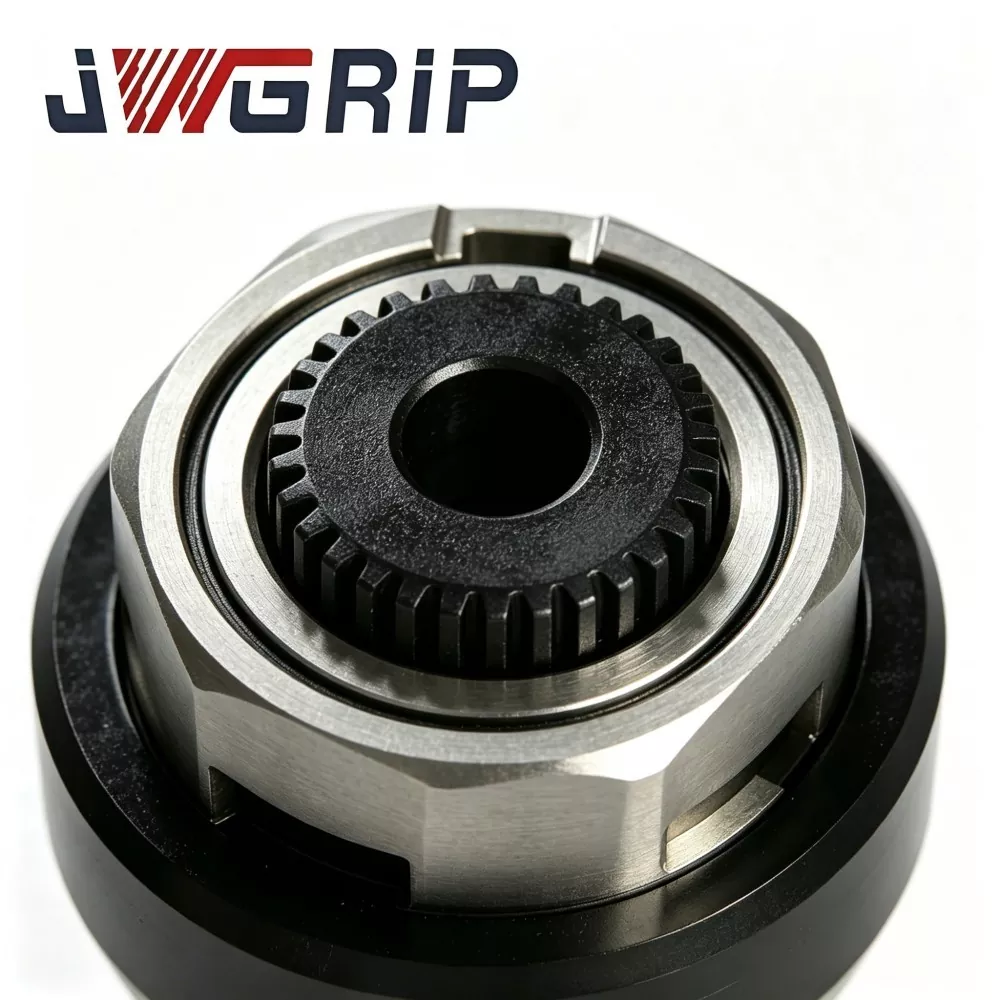
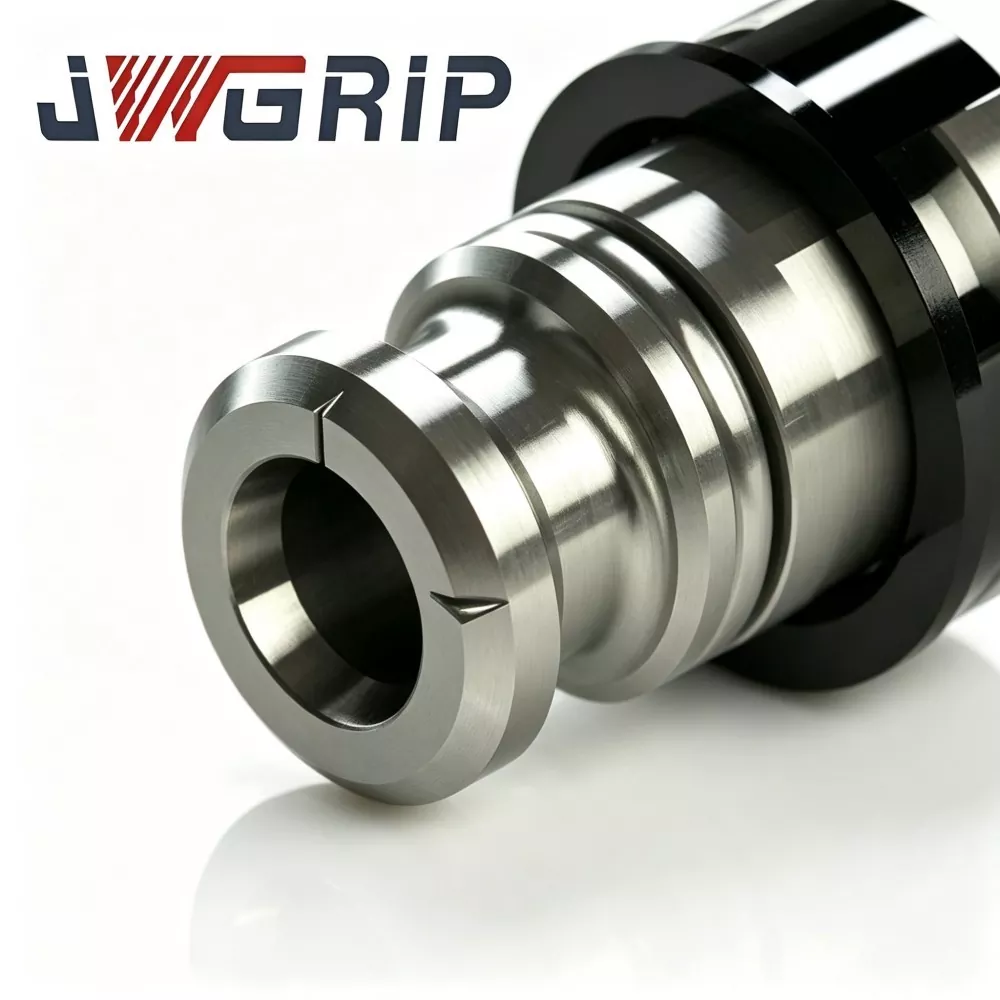
Working Mechanism
JWGRIP R-Type Pneumatic Drawbar connects between pneumatic drive cylinder and inner locking mechanism of EDM electrode holder, converting cylinder linear thrust into axial pulling-tension for electrode clamping:
1. Forward compressed-air input → pull stroke: R-type rounded-shoulder evenly transfers axial force onto holder internal locking components, compressing collet assembly and firmly clamping electrode shank.
2. Reversed-direction ventilation → backward movement: pre-load tension gets released, collet springs open for electrode removal.
Core R-type structural improvement:
Conventional straight-shoulder drawbars produce sharp stress peaks under cyclic impact; micro-deformation accumulates and alters output pulling-force.
R-type rounded transitional shoulder spreads stress over larger contact area, slowing fatigue deformation of drawbar body and thread joints. Stable axial tension can be maintained even after hundreds-of-thousands clamp-release cycles under partial dielectric-fluid submerged environment.
Technical Performances
1. R-Type Stress-dispersion Transitional-shoulder Construction Specially rounded-shoulder profile avoids sharp-angle stress concentration. Under equal air-pressure input, local stress value reduces by about 27 % compared with conventional straight-shoulder drawbars. Thread crack risk and body micro-deformation possibility are greatly lowered.
2. Gas-nitriding Surface-hardening Treatment High-alloy steel substrate undergoes precise gas-nitriding process; surface hardness reaches HV 850-950. Excellent wear-resistance and dielectric-fluid corrosion-resistance fit long-term partial immersion inside EDM working tank.
3. Accurately Calibrated Stable Pull-force Output Every finished unit is individually calibrated. Within rated air-pressure range, pull-force fluctuation is controlled within ±5 %. Reliable tension prevents electrode loosening during high-energy pulse discharge for deep-cavity machining.
4. High-precision Thread & Mounting Datum Thread section and mounting reference surface are precision-ground. Coaxiality between thread and drawbar main-body ≤0.004 mm. Eccentric load during reciprocating motion gets eliminated, lowering extra abrasion on matched holder inner components.
5. Broad Compatibility With Automatic EDM Holders Fits most commercially-available automatic EDM electrode-holder assemblies. Only minor mechanical adjustment is needed during retrofitting; full holder-set replacement is not mandatory.
6. Flexible OEM Custom-modification Capacity For special-retrofit projects, OEM service supports adjustment of thread specs, overall length, R-shoulder dimension and rated pull-force threshold according to customer drawings or physical samples.
7. Validated Long-cycle Fatigue Resistance Each production lot runs accelerated fatigue test simulating automatic electrode-change cycles. Qualified samples complete no less than 300 000 pull-release cycles without obvious performance degradation.
Operating Specifications
Even high-grade JWGRIP R-Type Pneumatic Drawbar for EDM Electrode Holder will age rapidly without proper workshop maintenance. Practical do-and-don’t rules are summarized from massive after-sales records.
Correct daily maintenance routines
1. Keep compressed-air source dry and clean; install air filter-regulator unit to block water vapor and oil sludge entering moving clearances.
2. Visual inspection every 7-10 working days: check thread surface and R-shoulder for scratch, corrosion or micro-crack.
3. During holder periodic overhaul, apply special EDM-tooling anti-corrosion grease on sliding-fit zones; ordinary general-purpose lubricant may dissolve in dielectric fluid and shall not be used.
4. If machine halts production over one week, retract drawbar out of submerged zone and perform anti-rust protection.
Operations strictly to be avoided
1. Exceed rated air-pressure: long-term input pressure over 0.7 MPa produces overload tension and causes permanent deformation on R-shoulder and thread sections.
2. Run without air-source filtration: moisture and impurity particles abrade mating clearances and trigger drawbar jamming.
3. Force assembly by hammer or striking tools: impact knocks ruin coaxial accuracy; invisible micro-cracks expand under cyclic load and bring sudden breakdown.
4. Continue running after detecting pull-force abnormality; may cause electrode dropping and mold-cavity crash, resulting in costly workpiece scrap.
Core Competitive Strengths
Most competing pneumatic drawbars adopt simple straight-shoulder structure without stress-optimized R-transition and only carry out basic dimensional checking instead of independent fatigue-cycle sampling test.
1. Structural gap: Competitor straight-shoulder drawbars concentrate stress at sharp corners; fatigue failure occurs after 80 000-150 000 cycles. JWGRIP R-type rounded-transition disperses stress; qualified samples pass ≥300 000 pull-release cycles.
2. Surface-treatment gap: Many manufacturers only apply conventional quenching without nitriding; parts corrode quickly under dielectric-fluid contact. Our gas-nitriding layer greatly improves wear-resistance and anti-corrosion under partial-immersion conditions.
3. Testing-standard gap: Many suppliers merely check dimensions. JWGRIP implements piece-by-piece pull-force calibration plus sampling accelerated-fatigue test to screen hidden defects before shipment.
4. Custom-service gap: Numerous factories only supply fixed standard sizes. Supported by export-oriented production capacity, JWGRIP OEM service realizes non-standard interface redesign for special-brand EDM-machine retrofit projects.
Packaging Specs
● Single-unit packing: Each qualified JWGRIP R-Type Pneumatic Drawbar is thoroughly cleaned, sprayed with anti-rust oil and sealed inside shock-resistant individual plastic tool-case, preventing scratch and thread bruise in transit.
● Bulk-order packing: foam-filled carton outer-package for sea-freight or air-freight shipment.
Logistics Options
● Logistics: cooperate with professional international freight forwarders.
● Attached documents: packing list and batch-inspection report copies can be enclosed in cargo or supplied as digital files.
FAQ
Q1: Can JWGRIP R-Type Pneumatic Drawbar for EDM Electrode Holder eliminate all electrode-loosening risks in automatic EDM production?
A1: This drawbar greatly stabilizes axial pull-force, yet electrode loosening can originate from other factors: insufficient/fluctuating air-source pressure, heavily-worn collet, deformed electrode shank, contaminated mating surfaces. When slipping happens, inspect the whole holder assembly systematically instead of only replacing drawbar.
Q2: Can I raise air-pressure above rated value for larger clamping pull-force?
A2: Not recommended. Excessive air-pressure brings overload tension and causes permanent micro-deformation on R-shoulder and threads. Even if clamping-force rises temporarily, service-life drops sharply and fracture risk increases. Choose higher-rating model or contact us for OEM solution if higher pull-force is required.
Q3: Do you support OEM if thread dimension or overall length differs from standard?
A3: Yes. Submit complete drawings or physical samples with clear specs for thread, total length, R-shoulder dimension, rated pull-force and surface-treatment. Engineering team finishes manufacturability assessment within 12 working-days and issues formal quotation.
Q4: What is covered under warranty?
A4: This is precision moving consumable tooling. Warranty applies to manufacturing-caused defects including out-of-spec coaxiality, non-conforming nitriding-layer and pull-force deviation at time of delivery. Damage caused by over-pressure operation, hammer-impact assembly, polluted air-source and long-term production fatigue-wear is excluded from warranty.
Hot Tags: R-Type Pneumatic Drawbar for EDM Electrode Holder, Manufacturer, Supplier
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.