

Professional Manufacturer of R-Type EDM Workholding System for Precision EDM Applications
As an experienced manufacturer specializing in R-Type EDM Workholding System, JWGRIP develops customized EDM chucks, electrode holders and centering plates through our in-house R&D team. This clamping platform is a quick-release tooling solution purpose-built for die-sinking EDM machines, automatic electrode changers and round-the-clock mold machining. Meanwhile, we also supply Zero Point Positioning System and Quick Change Workholding System for your broader CNC automation needs. Feel free to send an inquiry for a quotation and detailed specifications!
Where does electrode accuracy actually get lost?
Every mold shop knows that cavity quality depends on electrode accuracy. But accuracy is not created at the EDM machine — it is created, and often lost, long before. The usual loss points are: clamping deviation when the electrode blank is set on the CNC machine, measuring errors during inspection, deformation during handling, and position drift every time the electrode is changed on the EDM table.
Many workshops accept these losses as "normal production variation". In reality, they accumulate: a 0.01 mm offset at clamping, another 0.02 mm at changing, and soon the cavity wall no longer matches the 3D model — the mold goes for rework, and the electrode has to be re-cut.
How do professional mold shops prevent these accumulated losses? They do not rely on operator skill alone. They rely on a workholding system that keeps the electrode datum identical from the CNC electrode machine all the way to the EDM table.
Technological Process
CNC electrode machining: the electrode blank is clamped in an R-Type electrode holder. Because the holder centers the blank automatically, the milled electrode is concentric with the datum from the very first cut. For round graphite or copper electrodes, the R-Type ER32 Collet for EDM Electrode Holder keeps the shank firmly on axis.
Inspection and calibration: the finished electrode moves to the measuring station with its holder still attached. Using the R-Type CNC Calibration Block for EDM Workholding, the operator verifies the datum quickly, so every electrode carries a known and verified reference into the next step.
Roughing EDM: the electrode is locked into the chuck on the EDM machine. Because the chuck returns every electrode to the same reference, the roughing spark starts exactly where the program expects it, cycle after cycle.
Finishing EDM: When the roughing electrode is consumed the finishing electrode clamped on the same holder standard drops into the same datum.No re-probing, no re-zeroing, no guesswork. This is how cavity walls merge without steps and why finishing quality stays consistent even on late shifts.
Core Working Principle
An R-Type EDM Workholding System is a standardized quick-change workholding platform for die-sinking EDM. The R series covers chucks, holders, extension rods, collets and centering plates that all lock to one universal datum.
The core design separates clamping from locating: the datum is fixed on the machine, and the holder is clamped or released in seconds. Because every component shares the same reference, electrodes can be swapped quickly without re-probing or re-zeroing.
This is why the R-Type system is the standard choice for electrode work in mold shops, automatic electrode changers and robotic EDM cells.
Practical Strategies
How to cut changeover from minutes to seconds?
Use pneumatic quick-release chucks for frequent swaps. The R-Type D150 Pneumatic EDM Chuck releases and locks with one air signal, ideal for electrodes that are changed several times per shift.
How to keep the EDM machine cutting while you prepare the next electrode?
Pre-assemble electrodes on spare holders at the bench, then simply exchange the holder at the machine. The R-Type 9-in-1 Pneumatic EDM Chuck lets you prepare multiple electrodes in one setup, which is a real time-saver for multi-electrode cavity work.
How to make the system fit your existing workflow?
Start with one chuck and a set of holders for your most frequent electrode sizes, then expand the holder and centering plate families step by step.
Key Considerations
Do you machine large or small electrodes?
D150 and D100 chucks suit medium-to-large electrodes; compact holders with 54x54 or 70x70 centering plates fit smaller high-precision electrodes.
Manual or pneumatic?
Manual models offer reliability and low cost for conventional EDM; pneumatic models prepare you for automation and robotic electrode changing.
Planning to automate later?
Choose pneumatic chucks and zero-point pallets now so your future robot or pallet cell can connect without re-engineering.
Why choose JWGRIP?
JWGRIP is a professional EDM workholding manufacturer. Locating faces are precision ground and every chuck, holder and centering plate is inspected for repeatability before shipment, so components from different batches stay interchangeable.
We supply complete R-type sets — chuck, holder, extension rod, collet and centering plate — from one source, eliminating interface mismatch problems.
We support custom sizes and special geometries, and our engineers help you match components to your EDM machine model and electrode routine.
Typical application scenarios
Sinker EDM processing for injection molds, die-casting molds and stamping mold cavities.
Multi-electrode successive erosion processing requiring datum consistency between roughing and finishing procedures.
Mold processing workshops preparing to construct semi-automatic or fully-automatic EDM production cells.
Electrode pre-calibration work carried out on auxiliary CNC equipment.




- View as
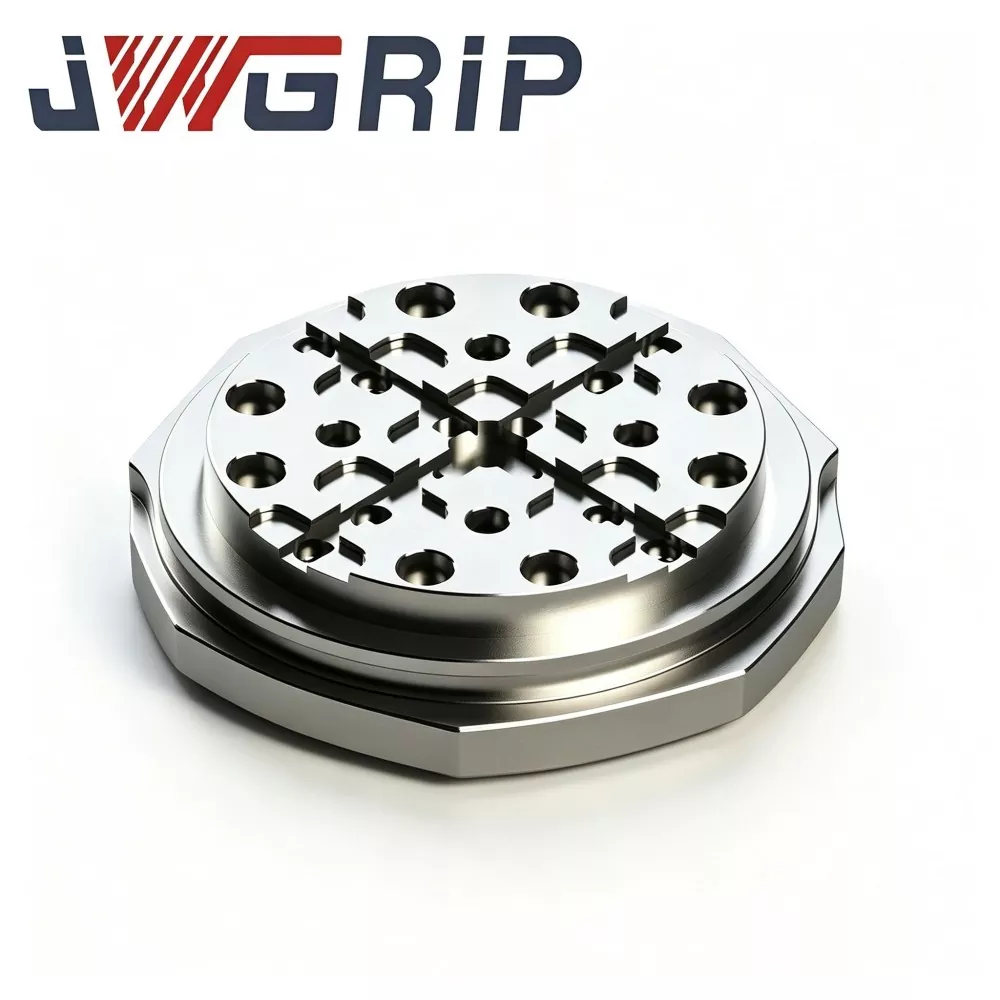
R-Type 156mm EDM Pallet for Zero Point Workholding
JWGRIP, experienced supplier delivering proven ODM solutions for high-precision EDM workholding hardware, offers rigid-construction R-Type 156mm EDM Pallet for Zero Point Workholding, a key purchasing component for sinker EDM cross-process transfer in medium-large mold-making plants. Made of stress-relieved pre-hardened alloy steel, it undergoes multi-cycle thermal stabilization, R-type transition-groove machining and full-face ultra-precision grinding. Equipped with chip-diversion drainage architecture for splashing EDM tank environments, its unique R-shaped stress-release groove spreads high local stress from repeated zero-point lock-unlock cycles and suppresses locating-datum-face micro-deformation after long-time cyclic operation.
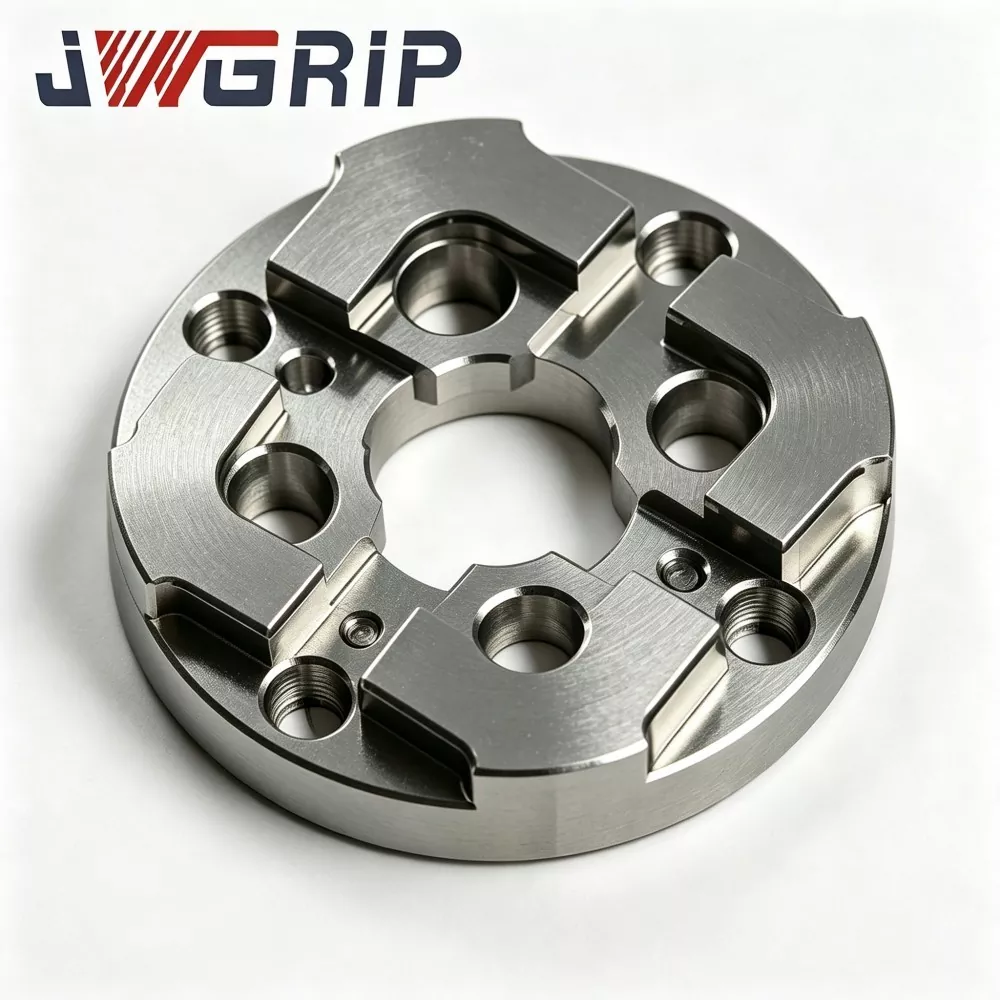
75mm EDM Zero Point Centering Plate
JWGRIP is the professional manufacturer and supplier of 75mm EDM Zero Point Centering Plate in China, providing Factory Direct supply and Customized structural adjustment for medium-large mold-making workshops worldwide. It is a high-stability integrated datum positioning fixture specially developed for sinker EDM zero-point fixture systems. It integrates reinforced anti-deformation structure and high-precision zero-point matching benchmark into a single unit, realizing fast datum restoration during frequent mold insert replacement and multi-electrode batch machining.

R-Type 54x54 EDM Centering Plate
JWGRIP is the professional manufacturer and supplier of R-Type 54x54 EDM Centering Plate in China, with standard specifications fully in Stock and supporting global Bulk Order for compact EDM machine and precision mold workshop projects. It is a wear-resistant high-precision integrated positioning benchmark fixture specially engineered for small-size sinker EDM equipment, mini electrode jigs and multi-cavity precision mold processing scenarios. It integrates optimized R-type transitional positioning shoulder structure and thermally stable mechanical performance into a single unit, eliminating the defects of easy extrusion wear and corner chipping of traditional right-angle miniature centering plates.
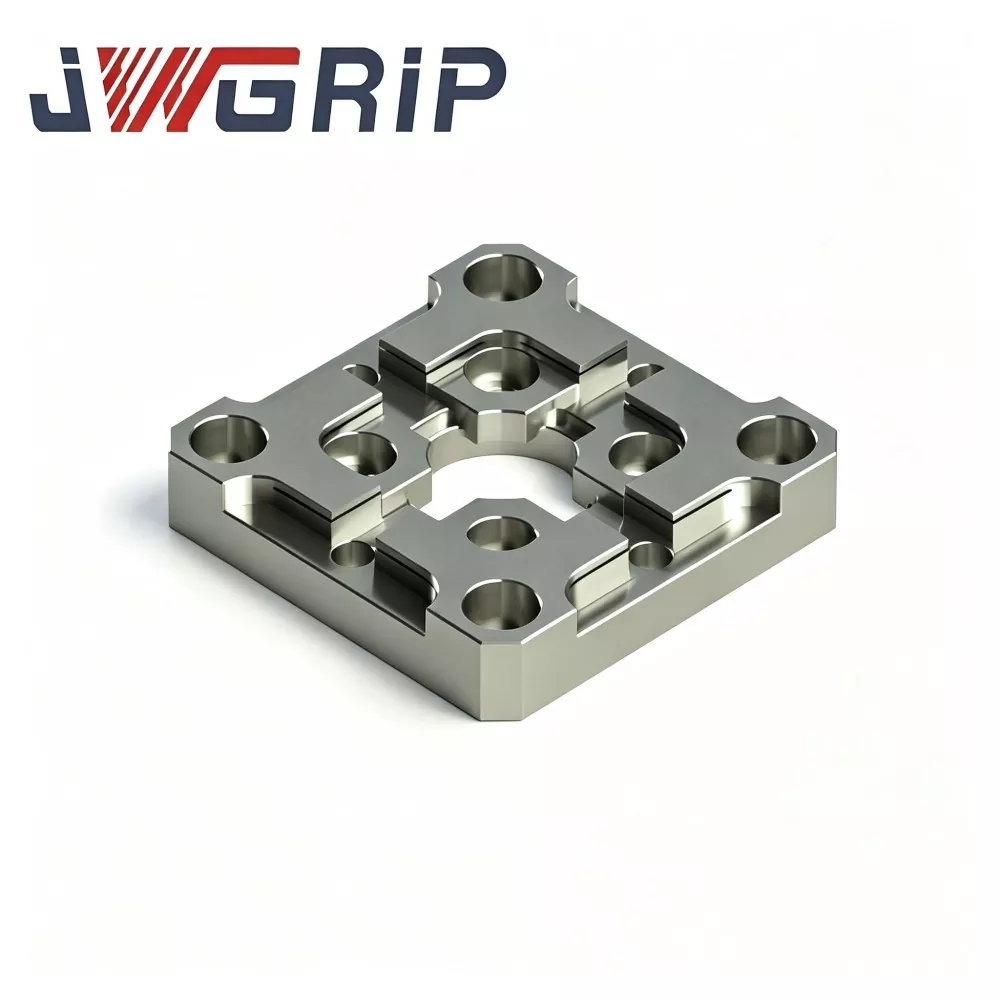
R-Type 70x70 EDM Centering Plate
JWGRIP is the professional manufacturer and supplier of R-Type 70x70 EDM Centering Plate in China, providing Factory Direct delivery and Customized structural modification to meet diverse EDM fixture layout demands. It is a high-precision integrated electrode positioning benchmark fixture specially optimized for sinker EDM mold-making workshops, focusing on rapid centering and repetitive electrode positioning tasks. It integrates stress-dispersed R-type inner chamfer transition structure and ultra-stable benchmark positioning performance into a single compact unit, effectively solving sharp-edge wear and reference drift defects of traditional flat centering plates.
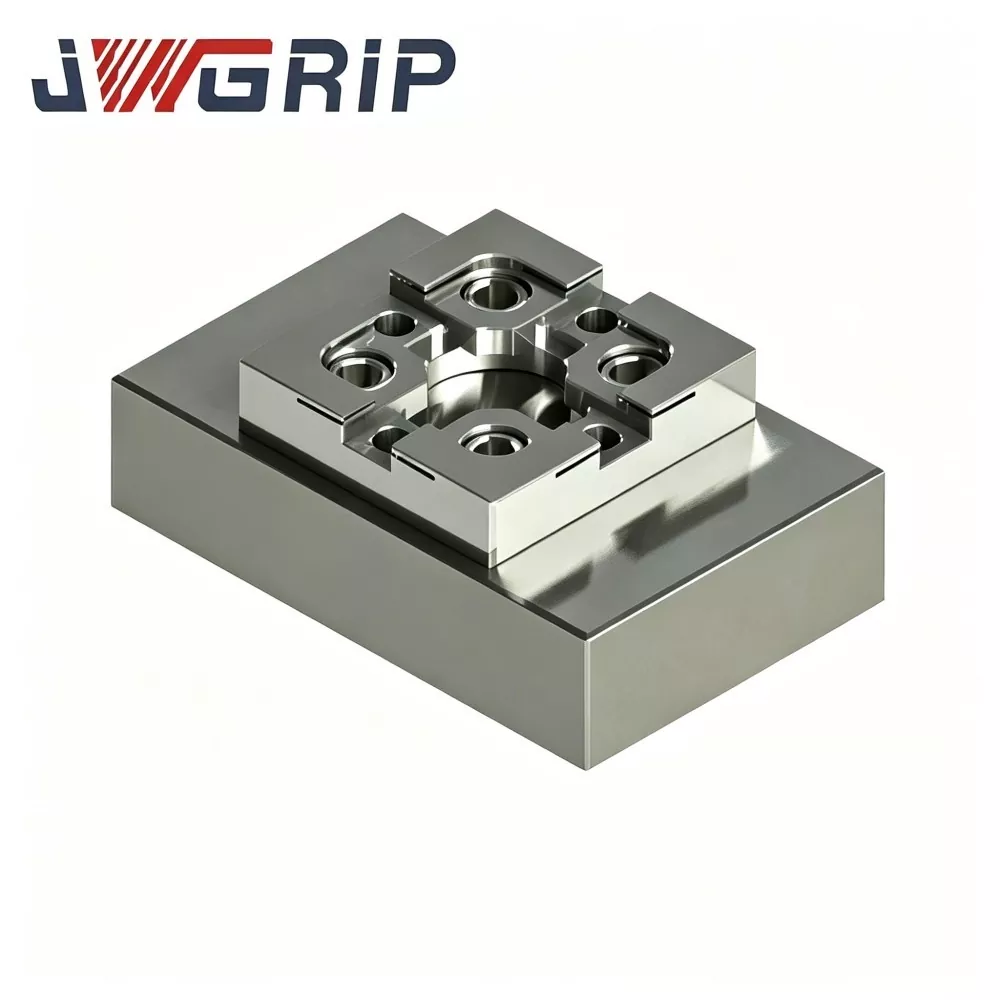
R-Type CNC Calibration Block for EDM Workholding
JWGRIP, a reliable factory-direct and professional exporter of precision EDM workholding accessories, supplies high-accuracy R-Type CNC Calibration Block for EDM Workholding, bulk order and drawing-based custom projects. Made of stabilized tool-steel with stress-relief aging, multi-face CNC milling and ultra-precision surface grinding, this calibration block maintains stable geometric tolerance under frequent temperature fluctuation and repeated probe contact. Unique R-type rounded reference-corner lowers sharp-edge wear risk and delivers repeatable coordinate offset data.
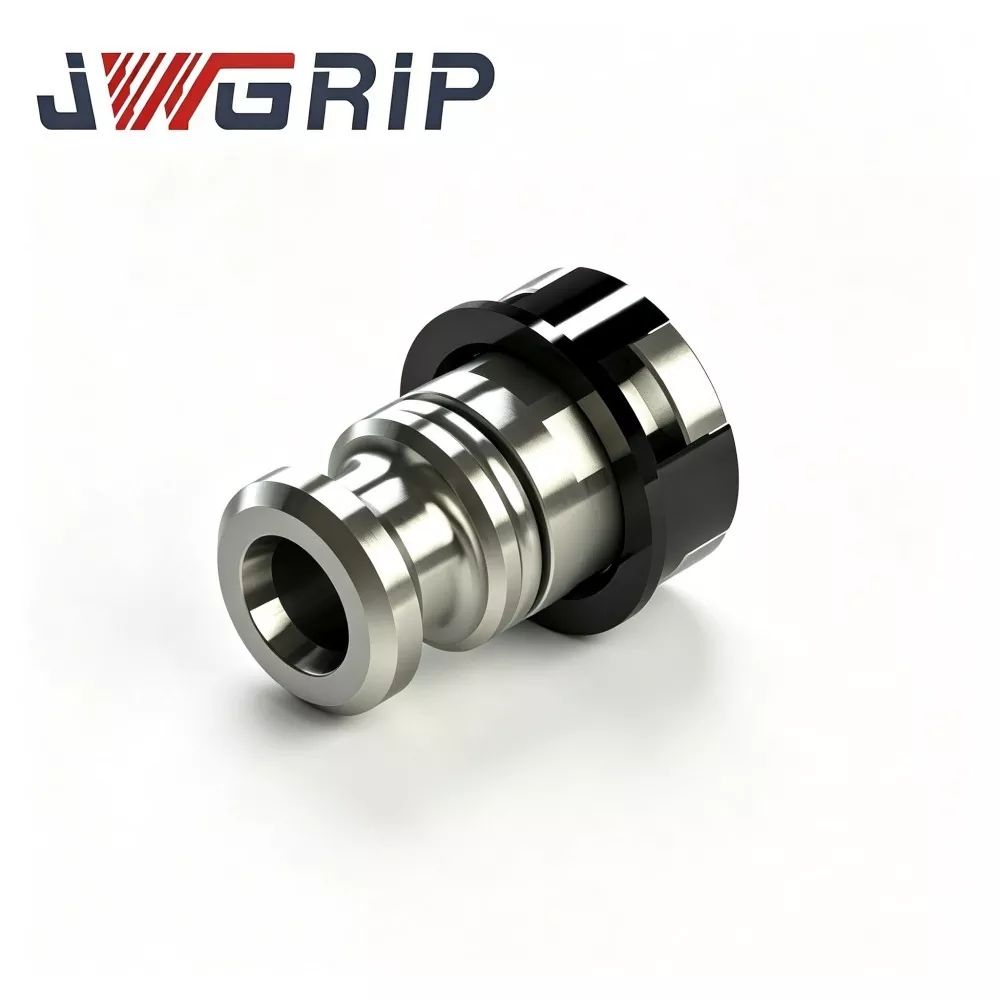
R-Type Pneumatic Drawbar for EDM Electrode Holder
JWGRIP is the professional manufacturer and supplier of R-Type Pneumatic Drawbar for EDM Electrode Holder in China, with standard specifications fully in Stock and accepting global Bulk Order for automated intelligent mold workshop projects. It is a high-reliability integrated pneumatic pulling component specially designed for unmanned automated sinker EDM production lines. It integrates optimized R-type stress-balanced force transfer structure and high-hardness anti-corrosion mechanical performance into a single device, eliminating tension attenuation, local stress concentration and easy wear defects of traditional straight-body drawbars.
JWGRIP is a professional R-Type EDM Workholding System manufacturer and supplier in China. We warmly welcome you to wholesale high quality products at competitive price from our factory.




