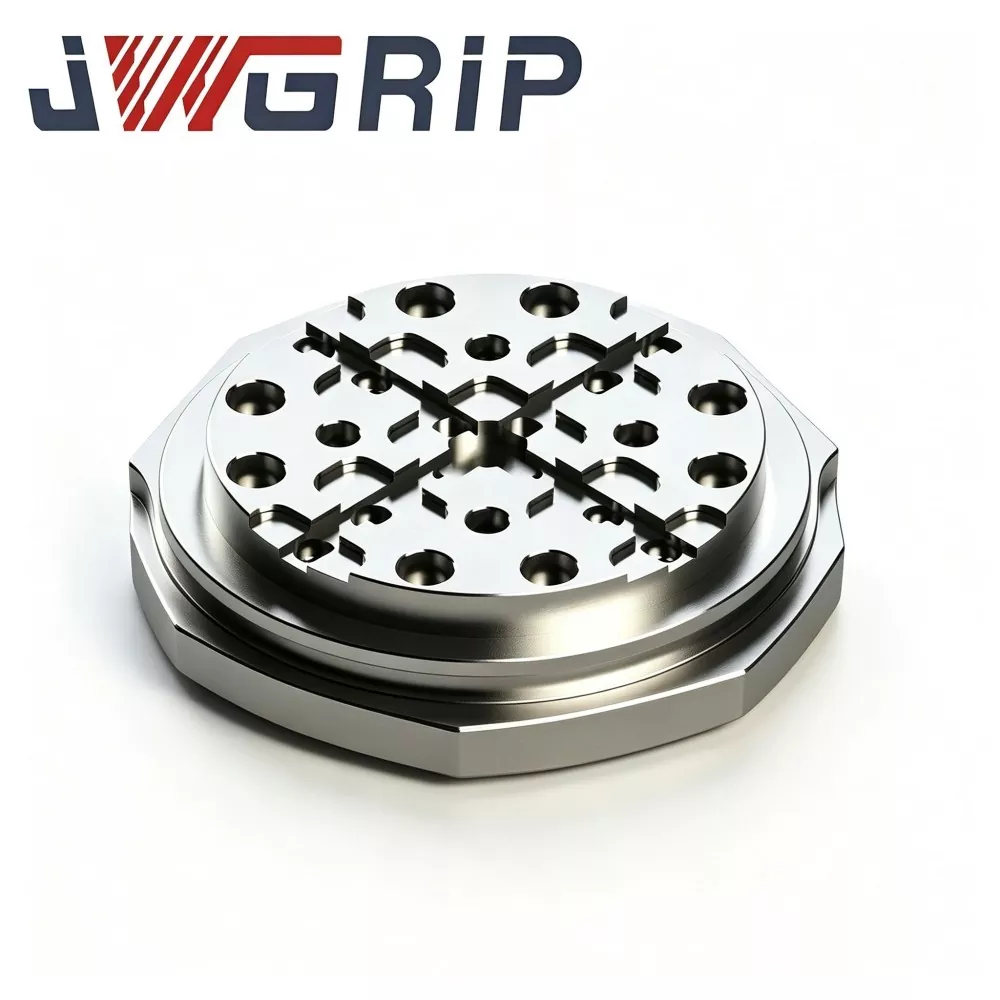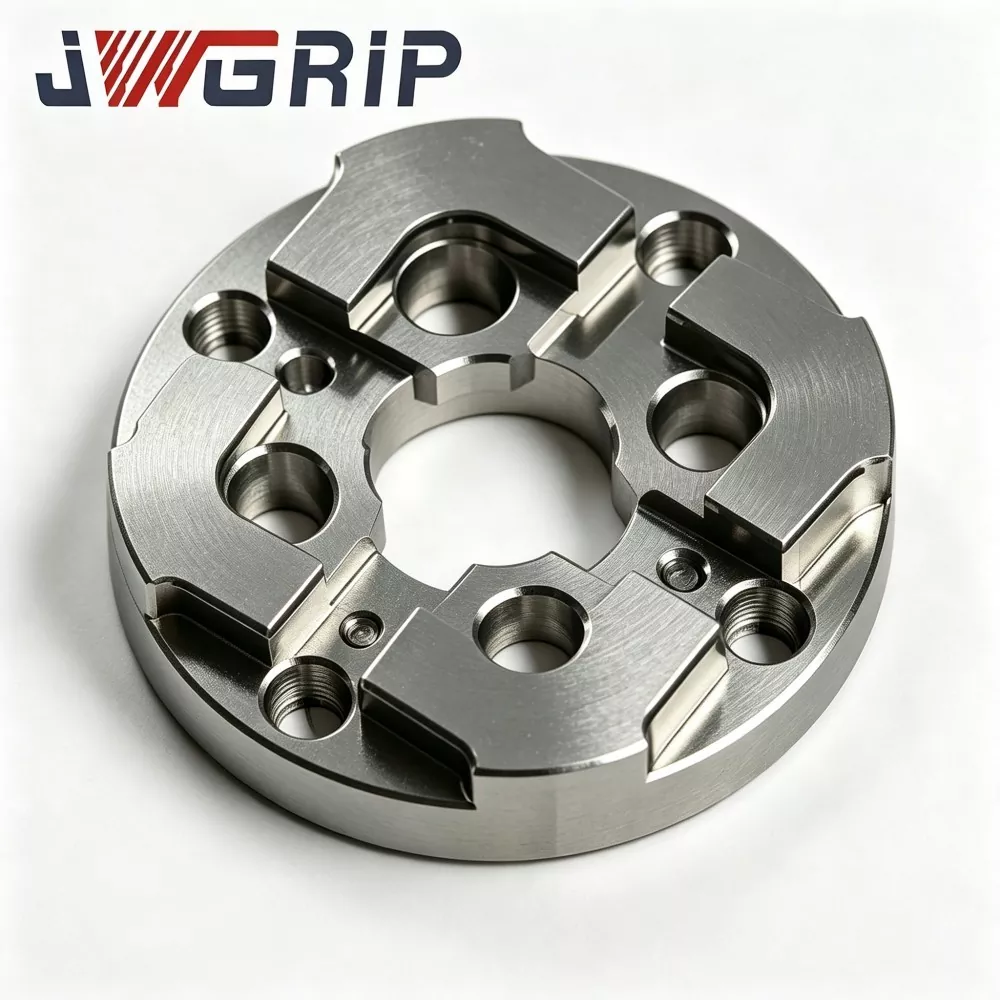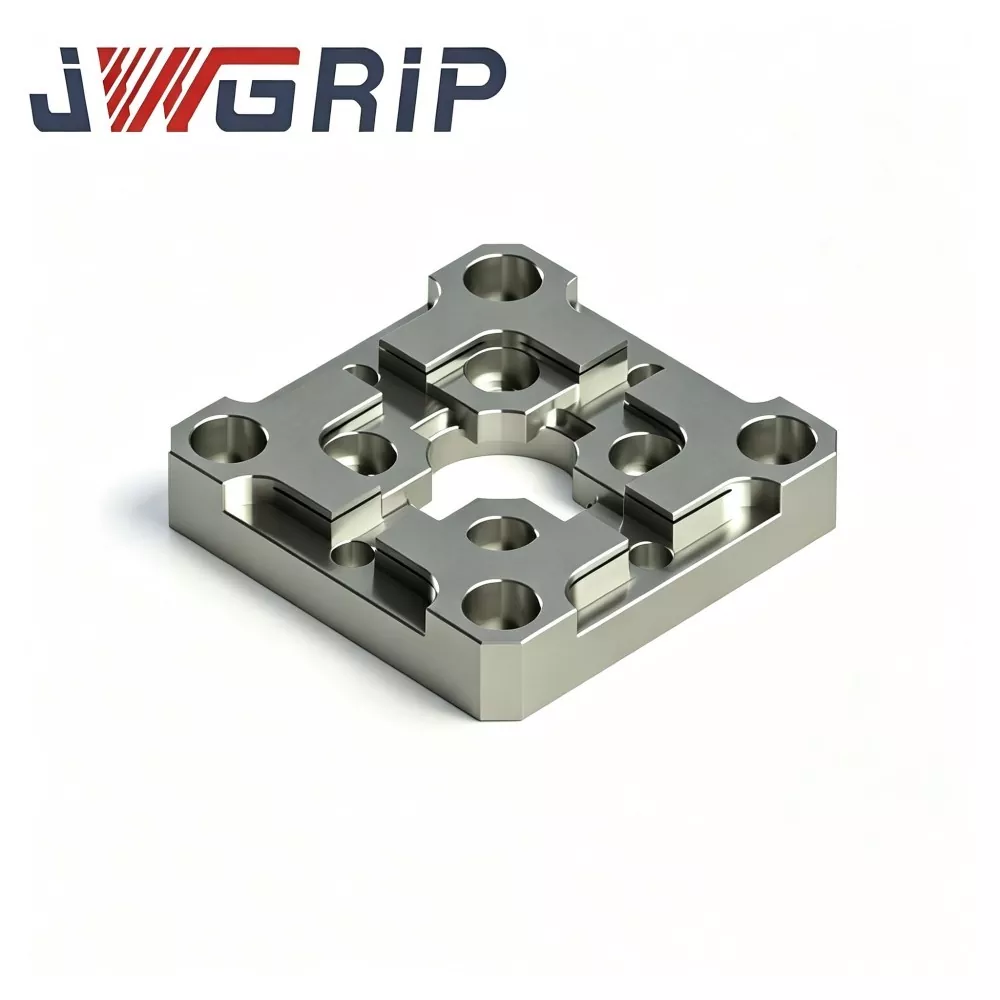
R-Type 70x70 EDM Centering Plate
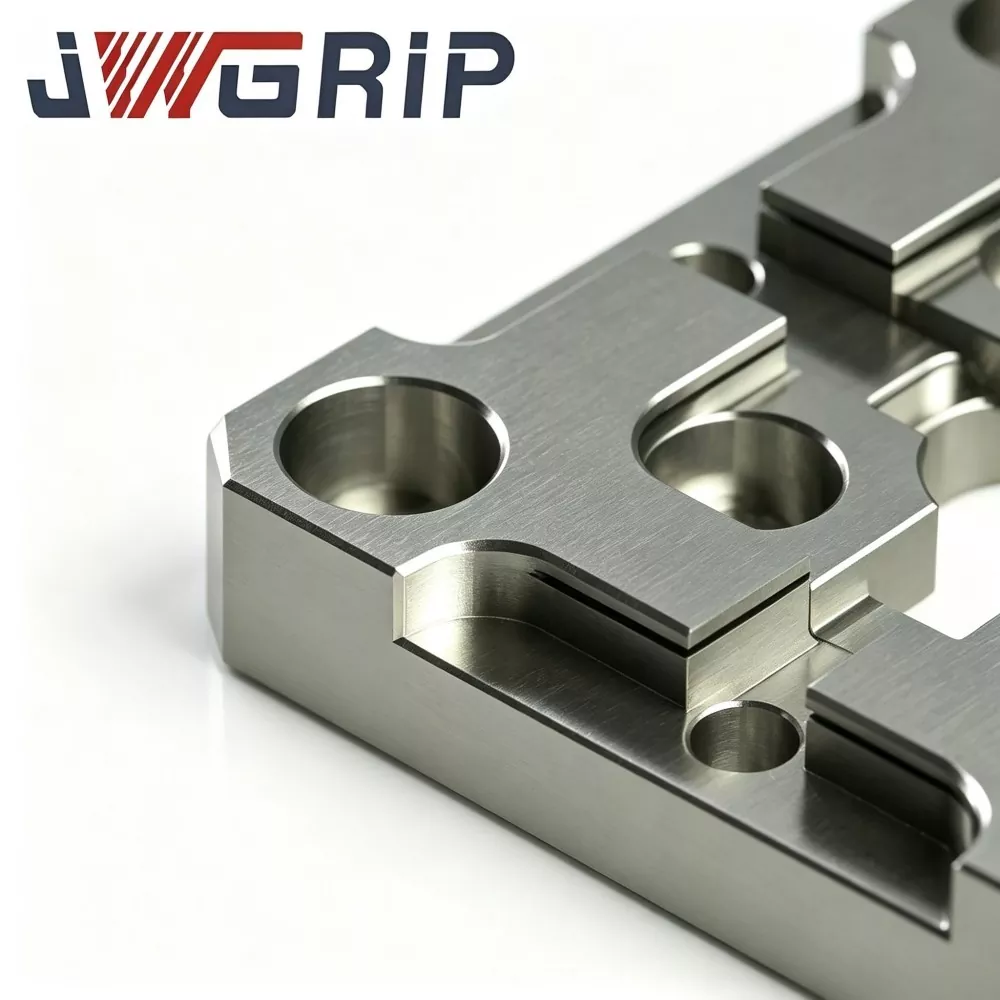
JWGRIP is the professional manufacturer and supplier of R-Type 70x70 EDM Centering Plate in China, providing Factory Direct delivery and Customized structural modification to meet diverse EDM fixture layout demands. It is a high-precision integrated electrode positioning benchmark fixture specially optimized for sinker EDM mold-making workshops, focusing on rapid centering and repetitive electrode positioning tasks. It integrates stress-dispersed R-type inner chamfer transition structure and ultra-stable benchmark positioning performance into a single compact unit, effectively solving sharp-edge wear and reference drift defects of traditional flat centering plates.
This high-repetition-accuracy EDM Centering Plate is manufactured from pre-stabilized alloy steel, adopting multi-step stress-relief treatment, professional surface hardening and ultra-precision double-face grinding technology to ensure excellent flatness and parallelism. The upgraded R-type chamfer transition structure disperses local contact stress during repeated fixture docking and loading-unloading cycles, effectively restraining positioning edge notch wear and long-term reference deformation. It eliminates cumulative positioning errors caused by frequent manual calibration and workshop temperature fluctuation, maintaining consistent electrode concentricity and stable spark gap in multi-cavity batch mold processing.
R-Type 70x70 EDM Centering Plate greatly simplifies electrode tool-setting procedures, shortens manual centering time, reduces human-induced positioning deviation for copper and graphite electrodes, and lowers mold rework rates. Supporting standard factory direct supply and drawing-based customization of hole layout and positioning boss size, it provides highly reliable benchmark guarantee for high-efficiency and high-consistency precision EDM mold production.
Prioritization scheme
Mold-making workshops running large-volume multi-electrode sinker-EDM jobs face hidden quality risks caused by conventional square-shoulder centering plates:
After hundreds of electrode-jig docking cycles, sharp inner corners produce indentation and partial abrasion. Subtle wear cannot be spotted by routine visual inspection, yet concentric reference drifts silently.
Deviation accumulates gradually. By the time problems are detected, several mold cavities have already been machined, resulting in high-value mold-insert scrap, poor spark-gap uniformity and uneven cavity side-wall erosion.
JWGRIP optimizes R-Type 70x70 EDM Centering Plate for these practical pain-points:
1. R-type smooth inner chamfer disperses docking contact stress and lowers indentation-type wear risk on positioning shoulders.
2. Pre-stabilized alloy-steel substrate with multi-round high-temperature aging largely eliminates internal residual stress and resists benchmark distortion caused by temperature fluctuation and continuous clamping impact.
3. Double-face ultra-precision grinding guarantees superior flatness and parallelism for stable mechanical-centering benchmark.
4. Simplifies manual centering procedures, reduces re-work rate and improves overall dimensional consistency for precision-mold EDM production.
5. Compact 70×70 outer dimension fits mainstream EDM fixture space; drawing-driven custom hole-pattern and positioning-boss modification are available for automatic electrode-change EDM-cell projects.
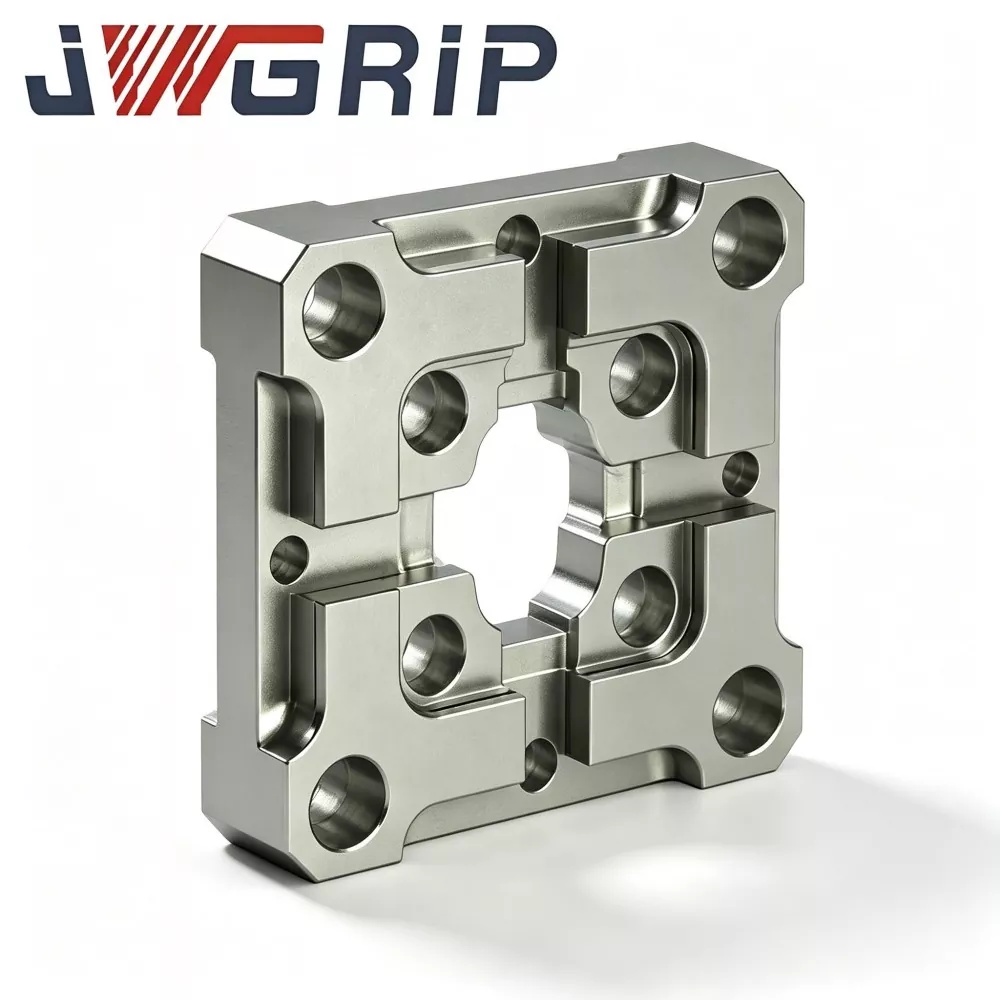
Working Principle
JWGRIP R-Type 70×70 EDM Centering Plate is a dedicated reference component for sinker-EDM electrode pre-positioning and concentricity calibration:
1. Mounted between EDM work-table and electrode-holder jig. It provides repeatable mechanical centering reference when swapping copper, graphite or copper-tungsten electrode jigs.
2. Conventional centering-plates adopt sharp-angled inner shoulders. Every docking impact concentrates stress on tiny corner zones and generates local plastic indentation after repeated pressing.
3. Core structural upgrade: smooth R-type inner chamfer transition expands effective contact area during jig docking, spreads pressing force over larger surfaces instead of narrow sharp corners, slowing indentation-wear and preserving original concentric benchmark for longer service cycles.
Important usage reminder: This plate delivers mechanical pre-centering only, and cannot replace final probe-based coordinate fine-calibration. After mechanical docking against this centering plate, operators still need to run probe compensation following standard EDM process specs. It is widely applied for injection-mold, die-casting-mold and precision stamping-insert EDM processing, especially suitable for batch-production workshops with frequent electrode swap. It can be installed on EDM work-table, zero-point chuck base or custom fixture support plate.
Key Technical Performance Characteristics
1. Optimized R-type Inner Chamfer Anti-wear Construction Comparative durability testing shows under identical docking-impact frequency, JWGRIP R-Type 70×70 EDM Centering Plate reduces local contact stress by approx.29 % compared with conventional sharp-shoulder centering plates, greatly lowering indentation and corner-notch risk caused by repeated jig pressing.
2. Multi-cycle Stress-relief Stabilization Alloy-steel substrate receives two-round high-temperature aging after rough-machining to remove most residual internal stress. Within workshop ambient-temperature 17-29 ℃, finished-plate flatness variation ≤0.0025 mm, preventing benchmark distortion induced by temperature drift.
3. Dual-sided Ultra-precision Grinding Top reference surface and bottom mounting datum are both ultra-precision ground. Flatness ≤0.002 mm; parallelism between top-bottom datum ≤0.003 mm. High parallelism supports alternative-surface usage by flipping the plate.
4. Localized Surface-hardening Treatment Key positioning-shoulder zones obtain special surface hardening, surface hardness reaches HRC 58-62. Strong anti-abrasion capability resists particle scratch and docking-impact marks; non-working zones retain proper substrate toughness to avoid whole-plate brittle fracture.
5. Dielectric-fluid-resistant Anti-corrosion Finish Whole outer-surface passivation anti-rust treatment. Resists long-time splashing EDM dielectric-fluid and humid workshop atmosphere, slowing oxidation and spot-rust occurrence.
6. Standard-size With Pre-processed Mounting Features Compact 70×70 outer footprint, pre-fabricated locating-pin holes and countersink screw holes. Direct installation fits most mainstream zero-point fixture interfaces without secondary machining.
7. Traceable Full-item Metrology Inspection Each finished unit carries laser-engraved unique serial-number. Complete inspection records covering flatness, parallelism and R-chamfer dimension are archived, supporting traceable quality-control for high-volume mold-making enterprises.
Complete Production Workflow
Each batch of JWGRIP R-Type 70x70 EDM Centering Plate strictly follows full-sequence manufacturing workflow:
Raw-material incoming chemical-composition & hardness inspection → CNC rough-milling → first-round high-temperature stress-relief aging → semi-finish machining → R-type inner-chamfer forming → secondary stress-relief aging → local surface-hardening → double-face precision grinding → pin-hole & countersink-hole finishing → CMM full-item geometric inspection → laser serial-number marking → anti-rust passivation → final visual re-check → finished-goods warehousing.
Production complies with ISO 9001 quality-management-system requirements.
Core measuring devices: coordinate-measuring-machine, surface-flatness interferometer, hardness-tester; all receive periodic official metrological calibration.
Every finished piece is attached with independent inspection report; material test certificates can be supplied per customer request.
Storage practical tip: Store centering plate inside dedicated shock-proof gauge box. Avoid heavy-object impact and metal-chip scratching. Even invisible micro-indentation will damage positioning accuracy. After each on-machine application, wipe positioning-shoulders and reference-surfaces completely with lint-free soft cloth before storage.
Correct assembly & operating workflow
1. Before installation, fully clean fixture-base mounting plane, locating-pin holes and centering-plate bottom datum; remove metal chips, carbon powder and dielectric-fluid residues. Trapped foreign particles will tilt plate and distort centering benchmark.
2. Fasten countersink screws following recommended torque. Over-torque creates local plate deformation and ruins flatness; insufficient torque causes plate shifting under docking impact.
3. Prevent heavy crash between electrode-jig and R-type positioning shoulders; adopt soft-contact docking mode for mechanical pre-centering.
4. After mechanical pre-centering, complete probe coordinate compensation per EDM-process specs. Never skip fine probing and rely purely on mechanical centering result for final machining.
5. Inspect positioning-shoulders under magnifying glass every 7-10 working-days; replace the plate immediately once indentation, scratch or notch is found.
Improper operations to be avoided
1. Mounting without cleaning mating surfaces: chips sandwiched produce hidden tilt deviation.
2. Violent hammer-aided docking: heavy impact generates invisible micro-indentation on positioning shoulders.
3. Over-torque screw fastening: induces internal stress and permanent geometric distortion of plate body.
4. Skip probe fine-calibration and take mechanical-centering output as final machining benchmark.
Why Select JWGRIP
1. Practical EDM work-holding R&D Experience Our engineering team accumulates abundant on-site feedback from mold technicians. Product iterations are optimized for real-shop bottlenecks instead of only theoretical drawing parameters.
2. Rigorous Full-unit Pre-shipment Inspection Many competitors merely adopt sampling dimensional check. Every JWGRIP R-Type 70×70 EDM Centering Plate completes CMM full-item geometric inspection to screen non-conforming parts before delivery.
3. Stable Lead-time For Standard & Custom Orders Standard-spec 70×70 products maintain production stock. For custom positioning-boss or hole-layout requirements, engineering team finishes drawing review within 12 working-days and confirms feasible schedule. Standard order lead-time:10-15 working-days.
4. Application-oriented Technical-support When customers meet assembly confusion or abnormal centering performance, technical-support team provides practical troubleshooting suggestions based on real EDM-workshop experience.
5. Complete Batch Traceability Management Each plate carries exclusive serial-number. Once positioning-related unexpected issues occur, original production parameters and inspection archives can be quickly retrieved for root-cause technical analysis.
FAQ
Q1: Can JWGRIP R-Type 70x70 EDM Centering Plate eliminate all centering deviation?
A1: It supplies stable mechanical pre-centering benchmark and cannot remove every source of deviation. Final probe-based coordinate compensation remains mandatory. Positioning error may also stem from worn electrode-jig, loose fixture mounting or electrode-shank deformation. Operators shall inspect whole jig-assembly periodically.
Q2: Is this centering-plate fit for frequent docking of heavy-weight large-size graphite-electrode jigs?
A2: It supports graphite-electrode-jig centering work. For extra-heavy assemblies, control docking contact force strictly and forbid violent impact. Even with R-chamfer optimization, excessive impact load still produces indentation damage on positioning shoulders.
Q3: Can you customize non-standard hole-pattern or special positioning-boss dimension?
A3: Yes. Please submit complete technical drawings with clear requirements for hole layout, positioning-boss geometry, flatness and parallelism tolerance. Engineering department evaluates manufacturability within 12 working-days and issues formal quotation.
Q4: Which damage conditions are excluded from warranty?
A4: This belongs to high-precision positioning work-holding component. Warranty covers manufacturing-originated defects upon delivery such as out-of-spec flatness, parallelism and hardness. Damage induced by collision, improper torque-installation, particle-scratch and normal service-wear is outside warranty coverage.
Hot Tags: R-Type 70x70 EDM Centering Plate
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.