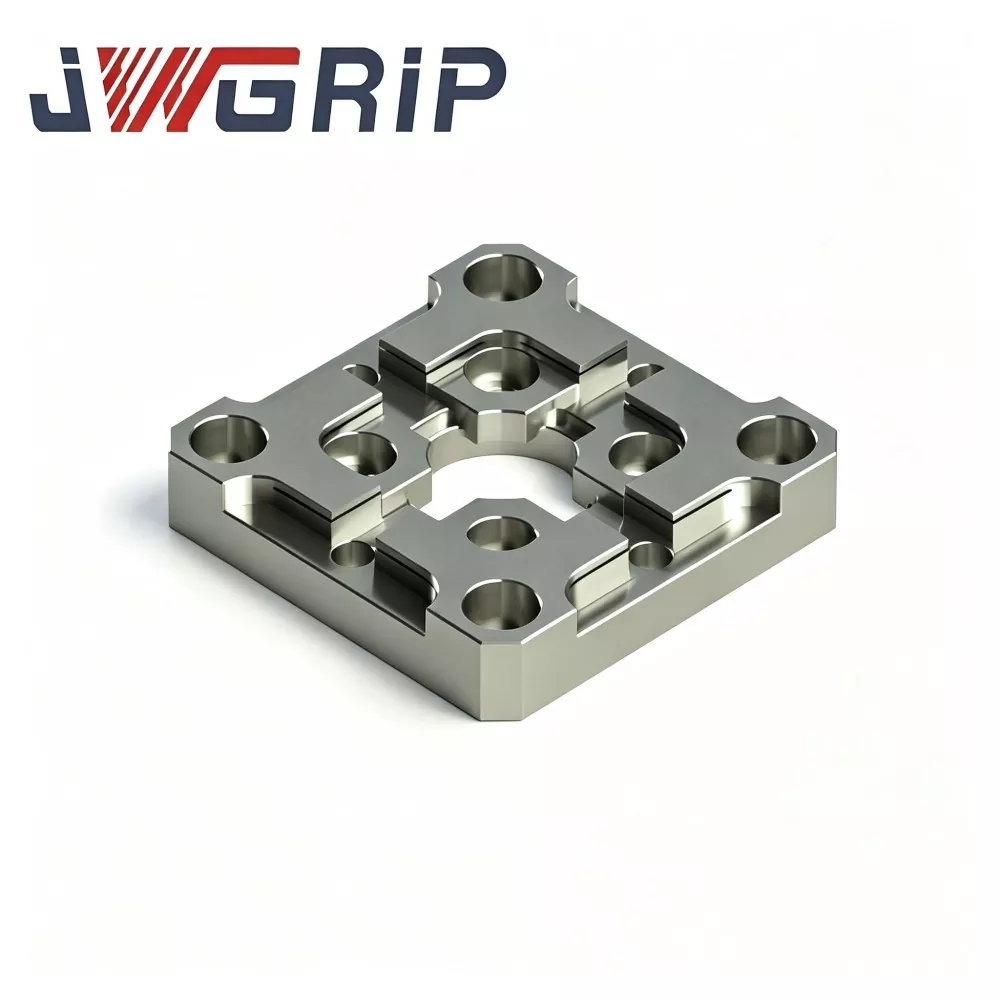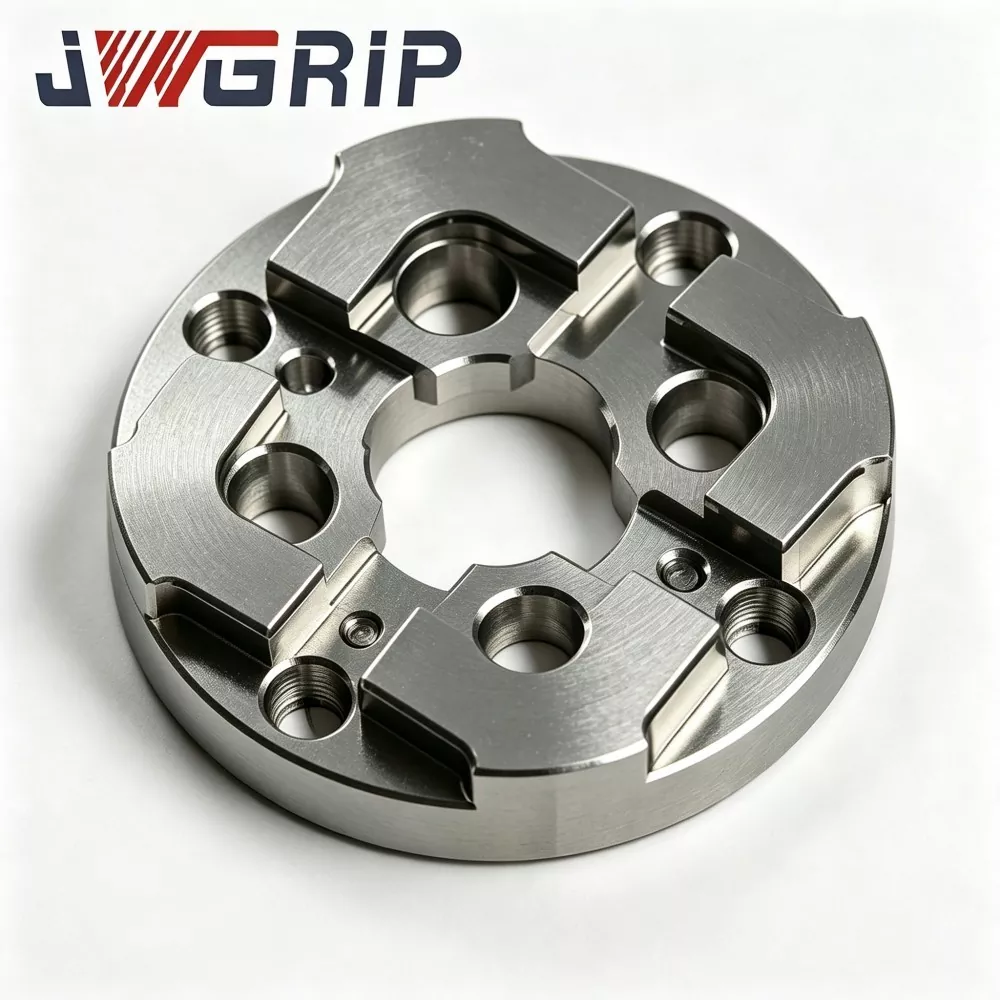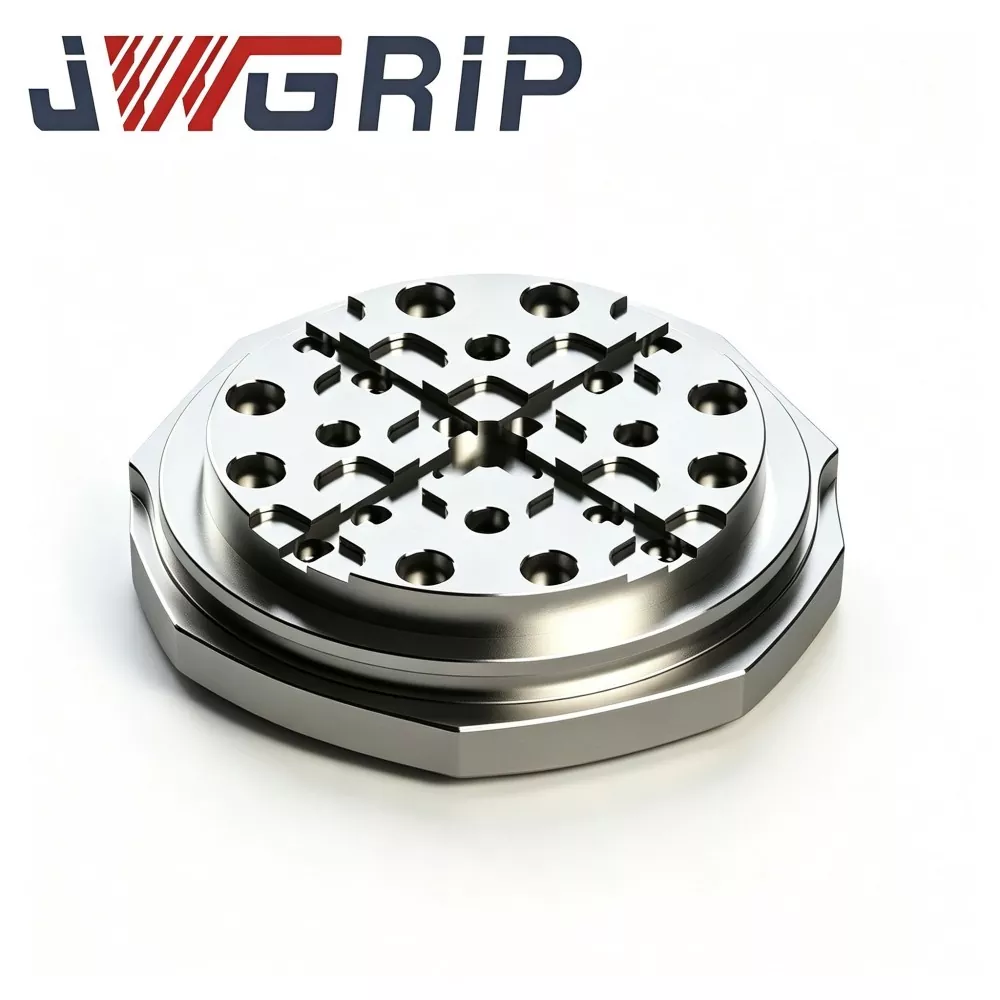
R-Type 156mm EDM Pallet for Zero Point Workholding
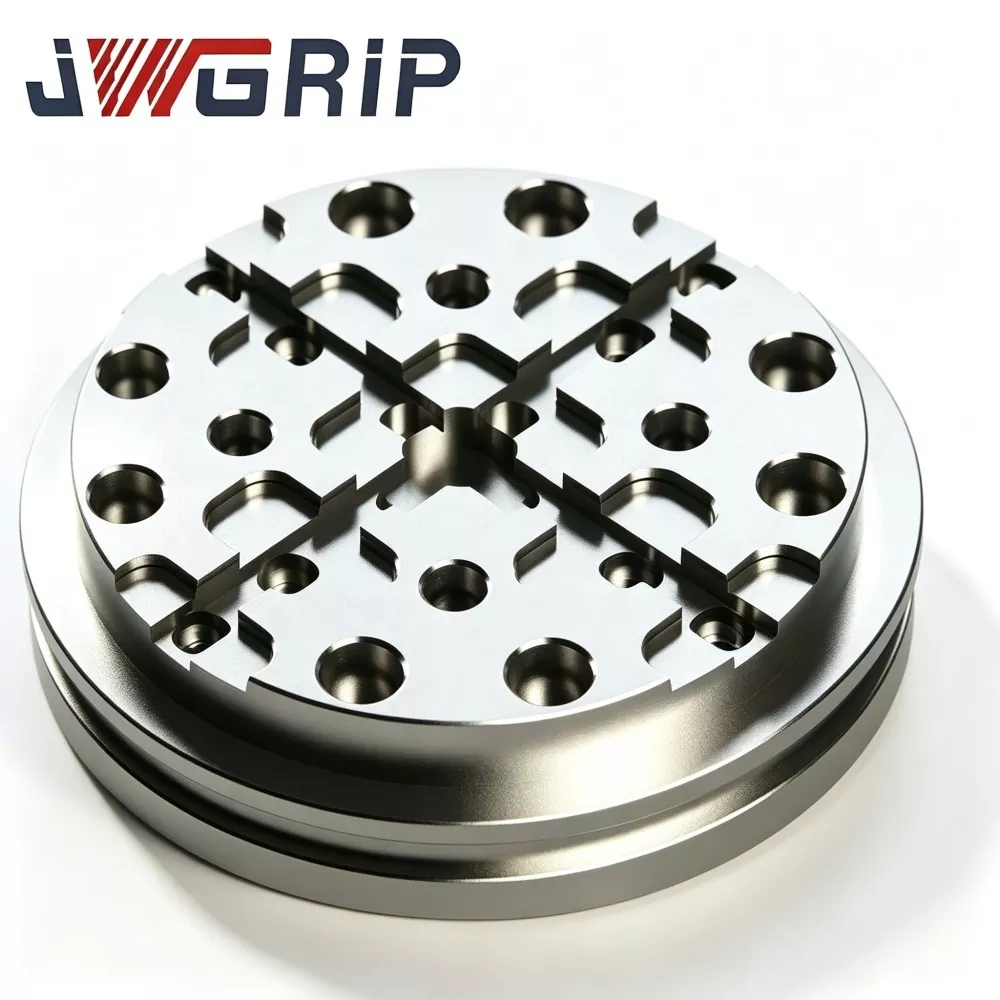
JWGRIP, experienced supplier delivering proven ODM solutions for high-precision EDM workholding hardware, offers rigid-construction R-Type 156mm EDM Pallet for Zero Point Workholding, a key purchasing component for sinker EDM cross-process transfer in medium-large mold-making plants. Made of stress-relieved pre-hardened alloy steel, it undergoes multi-cycle thermal stabilization, R-type transition-groove machining and full-face ultra-precision grinding. Equipped with chip-diversion drainage architecture for splashing EDM tank environments, its unique R-shaped stress-release groove spreads high local stress from repeated zero-point lock-unlock cycles and suppresses locating-datum-face micro-deformation after long-time cyclic operation.
Traditional mold-making workflows suffer benchmark shift and subtle datum deformation caused by frequent cross-station fixture exchanges. Conventional zero-point pallets with stiff right-angle grooves easily concentrate locking stress and lose flatness over cycles. Combined with continuous coolant splash and chip accumulation, ordinary pallets bring positioning failures and heavy manual-cleaning workload. This upgraded JWGRIP R-Type 156mm EDM Pallet for Zero Point Workholding solves such industry-wide drawbacks.
Thermally stabilized steel body removes internal residual stress, while optimized R-groove evenly distributes clamping impact. Built-in drainage and chip-evasion design copes with harsh EDM conditions, preserving steady datum flatness and repeat accuracy. It standardizes cross-station workpiece transfer, reduces auxiliary setup time, stabilizes multi-batch mold machining precision and delivers high-rigidity zero-point locating support for automated medium-large mold production lines.
Real Pain-points
Modern medium-to-large mold-making workshops adopt zero-point workholding to achieve offline fixture preparation and cross-station part transfer following lean-production concepts. Even so, many end-users keep facing tough practical troubles with ordinary universal zero-point pallets installed on sinker EDM machines.
· Conventional pallets feature sharp-angled inner-groove geometry. Under repeated zero-point pre-load, stress accumulates at sharp corners and slowly triggers datum-face micro-distortion.
· Most standard pallets lack dedicated chip & dielectric-fluid drainage features. Debris mixed with dielectric fluid piles up around locating holes. Air-blow cleaning cannot fully clear contaminants, which gradually ruin locating fit clearance and degrade repeat-positioning performance.
· When mold inserts flow from milling stations into EDM tanks, invisible positioning drift accumulates step-by-step, resulting in costly rework or scrap for high-value multi-cavity mold components.
Development Orientation
JWGRIP R-Type 156mm EDM Pallet for Zero Point Workholding is purpose-built to resolve the above-mentioned sinker-EDM zero-point workflow bottlenecks. Different from generic zero-point pallets only validated under dry laboratory conditions, our engineering team performed abundant field tests inside real-world EDM working-tank environments. Test conditions fully cover dielectric-fluid immersion, chip pollution and cyclic locking pre-load.
· Leveraging multi-year on-site feedback from global mold clients, multiple prototype iterations passed tens-of-thousands zero-point lock-unlock simulation cycles before mass-production launch.
· The pallet can be mounted directly onto mainstream zero-point base modules. Its 156 mm outer dimension fits clamping scenarios for medium-large mold inserts and heavy-weight electrode fixtures.
· Beyond standard specs, JWGRIP ODM service supplies customized structural features for retrofitted special-purpose automated EDM zero-point cells.
Functional Principle
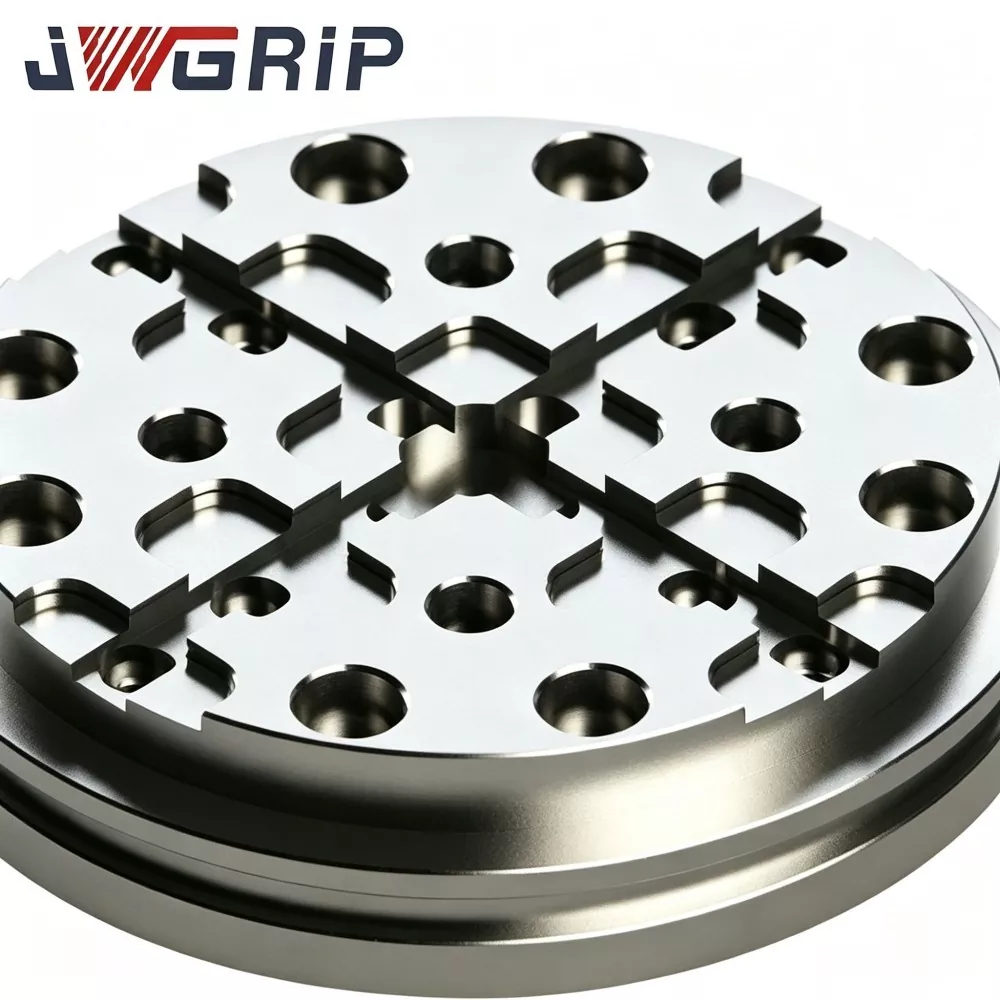
JWGRIP R-Type 156mm EDM Pallet for Zero Point Workholding acts as the load-carrying datum carrier within zero-point workholding ecosystem. It sits between zero-point locking modules and upper fixture plates / mold-insert jigs. After docking onto zero-point locating pins and completing pneumatic pull-lock action, unified mechanical datum gets established. It supports offline fixture assembly and fast cross-station workpiece hand-over without full dial-indicating work.
Ordinary zero-point pallets gather locking stress at sharp groove corners. After countless lock-unlock cycles, residual micro-plastic deformation accumulates and datum flatness drifts.
· The core upgrade of JWGRIP R-Type pallet lies in continuous smooth R-type transition-groove construction. R-curved profiles spread concentrated locking stress over broader groove-wall surfaces instead of narrow sharp-corner zones.
· Meanwhile integrated chip-diversion drainage channels guide EDM dielectric fluid and eroded chips away from locating-hole mating zones, lowering particle-contamination risks for precision-fit interfaces.
Core Product Advantages
1. R-Type Stress-Dispersed Groove Architecture Comparative cyclic-load lab testing shows: under identical zero-point pull-lock force, JWGRIP R-Type 156mm EDM Pallet cuts peak local stress by around 35 % compared with conventional sharp-groove zero-point pallets. R-Type 156mm EDM Pallet for Zero Point Workholding significantly suppresses datum-face micro-deformation risk after thousands of repeated lock-unlock cycles.
2. Multi-phase Thermal-stabilization Aging Pre-hardened alloy-steel substrate undergoes three-stage high-temperature stress-relief aging after rough-machining to eliminate most internal residual stress. Within real-world workshop temperature range 14-32℃, finished-pallet datum-surface flatness variation is controlled ≤0.0030 mm, resisting thermal distortion triggered by EDM tank temperature fluctuation.
3. Full-face Ultra-precision Grinding Treatment Bottom zero-point mating datum, upper fixture-mounting datum and locating-groove contact surfaces all receive ultra-precision grinding. Upper-datum flatness ≤0.0025 mm; top-to-bottom mating-datum parallelism ≤0.0040 mm. Stable parallelism guarantees datum consistency through repeated disassembly-reassembly cycles.
4. Built-in Chip-diversion Drainage System Purpose-built continuous drainage-groove paths divert dielectric fluid and eroded chips out from locating-pin hole zones, reducing particle-residue accumulation on precision-fit interfaces under submerged EDM working conditions.
5. Integrated Anti-corrosion Surface Finish Whole-pallet passivation anti-rust treatment is applied. It endures long-time splashing and partial immersion of EDM dielectric fluid and inhibits spot-rust formation inside humid EDM machine-tank environment.
6. Standard-compatible Locating-Interface & Flexible ODM Support Prefabricated locating-pin holes and locking-screw holes match mainstream 156-size zero-point module specs. JWGRIP can adjust hole layout, drainage-groove route and outer contour dimension following customer engineering drawings for special-purpose fixture-cell reconstruction projects.
7. Full-lot Traceable Quality-archive Mechanism Each finished pallet carries laser-etched exclusive batch serial number. Complete inspection datasets of flatness, parallelism and loaded-state deformation test results are archived for traceability, convenient for quality management for large-scale mold-making enterprises.
Manufacturing Process
Every JWGRIP R-Type 156mm EDM Pallet production batch strictly follows full-chain controlled manufacturing steps:
1. Incoming raw-material composition & hardness validation
2. CNC rough milling (including R-type transition-groove and drainage-channel features)
3. First-phase high-temperature stress-relief aging
4. Semi-finish machining
5. Secondary & tertiary thermal-stabilization aging
6. Locating-hole and locking-screw-hole forming
7. Double-sided plus groove-face ultra-precision grinding
8. CMM multi-item geometric-profile scanning
9. Simulated zero-point pull-load deformation test
10. Chip-diversion-groove burr-removal
11. Laser serial-number marking
12. Whole-pallet anti-rust passivation
13. Final visual + dimensional reinspection
14. Finished-product warehousing
JWGRIP plant implements ISO 9001 quality-management-system standards. Core metrology devices including coordinate-measuring-machine, flatness interferometer and zero-point load-simulation test bench get periodic official metrological calibration. Every finished pallet is delivered with independent inspection report. For ODM custom orders, material certification documents and partial third-party test records can be provided upon buyer request.
Maintenance Checklist
1. Before mounting JWGRIP R-Type 156mm EDM Pallet for Zero Point Workholding, fully clean zero-point-module top mating surface, pallet bottom datum, locating-pin-hole inner walls and chip-diversion-groove cavities. Remove metal chips, carbon-powder and dielectric-fluid residues. Foreign particles trapped between mating interfaces trigger pallet micro-warping under zero-point pull-lock pre-load.
2. Operate zero-point locking-modules strictly within manufacturer-specified rated air-pressure. Never feed over-rated air-pressure; excessive pull-load will result in permanent pallet geometric distortion.
3. After zero-point pull-lock completes, never skip probe-based coordinate fine-compensation. Mechanical zero-point datum cannot offset tiny assembly-clearance deviation.
4. Every 9-12 working-days: perform visual inspection for datum-surface scratches & indentations; check chip-diversion-groove for particle clogging; run periodic loaded-state repeat-positioning test.
5. After disassembly, clean all datum faces and drainage-grooves before placing into dedicated gauge-box. Do not stack heavy raw-workpieces directly on pallet upper-datum surface.
Competitive Edge
Many commercially-available 156-size zero-point pallets adopt sharp-angled inner-groove layout without R-type stress-release optimization. Numerous competitors omit special chip-diversion drainage-groove and cut thermal-stabilization aging cycles to lower production costs.
1. Stress-resistance: Competitor sharp-groove pallets tend to generate local micro-deformation after 7000-12000 zero-point lock-unlock cycles. JWGRIP R-Type pallet with R-shaped stress-release groove greatly reduces deformation risk under repeated pull-load cycles.
2. Anti-pollution performance: Most rival pallets have no built-in chip-diversion channels; EDM chips and dielectric residues accumulate near locating holes. Our integrated drainage-groove diverts contaminants away from precision-fit zones and reduces manual-cleaning burden.
3. Internal-stress control: Many competing products reduce aging procedures; residual-stress releases slowly under temperature cycling and causes late-phase flatness drift. JWGRIP multi-phase thermal-stabilization removes most residual-stress and sustains long-term geometric stability.
4. Inspection scope: Plenty suppliers only run partial-dimension sampling inspection. Every JWGRIP pallet completes full-item CMM geometric scanning. ODM modified pallets also receive special-feature validation.
5. Customization capability: Most factories can only supply fixed-standard-size pallets. With mature ODM workflow, JWGRIP can redesign outer contour, hole-layout and drainage-groove for special-reconstruction EDM zero-point-fixture-cell projects.
FAQ
Q1: Can JWGRIP R-Type 156mm EDM Pallet achieve zero-deformation over unlimited zero-point lock-unlock cycles?
A: Optimized R-type stress-release groove plus chip-diversion groove greatly mitigate deformation and particle-pollution risks. Absolute zero-deformation cannot be guaranteed after massive cyclic-load operation. Operators must maintain zero-point-modules running within rated air-pressure range and implement periodic loaded-state repeat-positioning inspection. Probe coordinate fine-compensation remains a mandatory production step.
Q2: Is this pallet capable of continuous ultra-heavy mold-insert payload?
A: JWGRIP R-Type 156mm EDM Pallet for Zero Point Workholding is engineered for medium-large mold-insert and electrode-fixture loads. For ultra-heavy-workpiece scenarios, users need to cross-check overall payload against zero-point-module rated load capacity. Surpassing rated payload accelerates pallet-interface wear and may trigger permanent deformation.
Q3: If non-standard outer contour, special hole-layout and custom drainage-groove path are needed, do you support ODM manufacturing?
A: Yes. Please submit complete technical drawings specifying outer outline, locating-hole arrangement, drainage-groove route and tolerance specs. Our engineering department will finish manufacturability assessment and send formal quotation within 12 working-days.
Q4: Which failure conditions fall under product-warranty coverage?
A: JWGRIP R-Type 156mm EDM Pallet belongs to high-precision zero-point-workholding load-bearing datum component. Warranty applies to manufacturing-origin defects existing upon delivery: out-of-spec flatness, parallelism and disqualified loaded-deformation-test index. Damages from over-pressure locking, heavy-impact collision, chip-abrasion and wear accumulated through long-term cyclic usage are excluded from warranty scope.
Hot Tags: R-Type 156mm EDM Pallet for Zero Point Workholding
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.