English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик
Why do many mold factories choose the R-type 9-in-1 pneumatic chuck in EDM processing
Article Abstract: Sinker EDM workshops commonly suffer from time-consuming electrode setup work, positioning deviation caused by assembling multiple discrete chucks, and low machine utilization for multi-electrode mold production. JWGRIP, a professional workholding solution provider, has launched the high-performance R-Type 9-in-1 Pneumatic EDM Chuck. Adopting an all-in-one monolithic base plate structure, this product eliminates cumulative splicing errors generated by combining scattered single chucks. This article explains the core design concept, real-world performance advantages, practical production value and typical application scenarios of this multi-station fixture. It illustrates how it greatly shortens electrode change-over time and delivers stable micron-level positioning accuracy for sinker EDM operations of multi-cavity molds, automotive molds and medical molds.
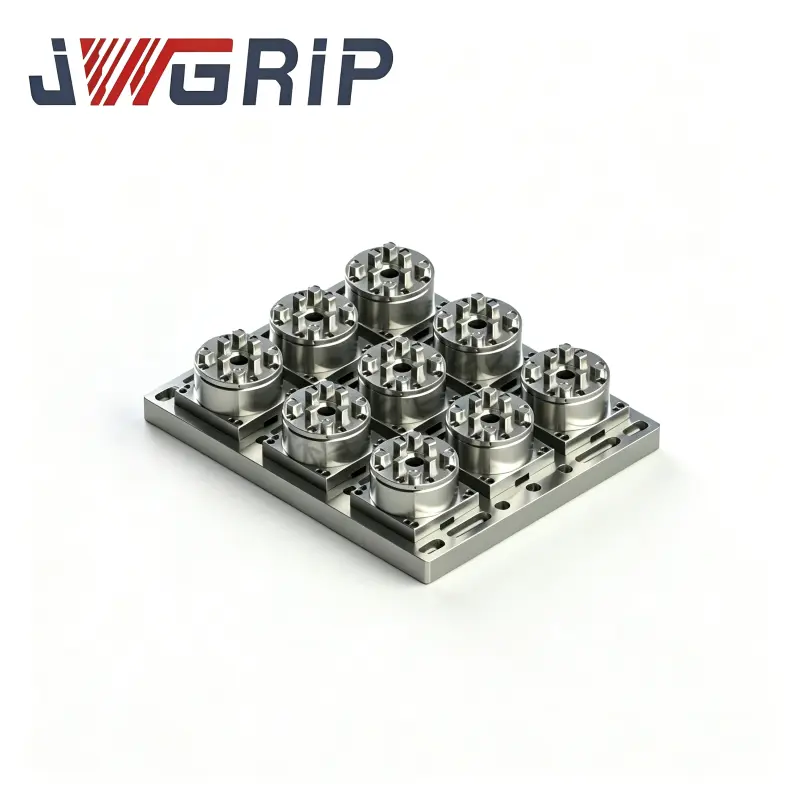
Table of Contents
1.What Is the Core Design Philosophy of JWGRIP R-Type 9-in-1 Pneumatic EDM Chuck?
2.How Does the R-Type 9-in-1 Pneumatic EDM Chuck Outperform Multiple Separate Single Zero-Point Chucks?
3.What Operational Advantages Does the R-Type 9-in-1 Pneumatic EDM Chuck Bring to Daily Production?
4.What High-Precision Manufacturing Scenarios Can the R-Type 9-in-1 Pneumatic EDM Chuck Perfectly Adapt To?
5.Frequently Asked Questions About R-Type 9-in-1 Pneumatic EDM Chuck
1. What Is the Core Design Philosophy of JWGRIP R-Type 9-in-1 Pneumatic EDM Chuck?
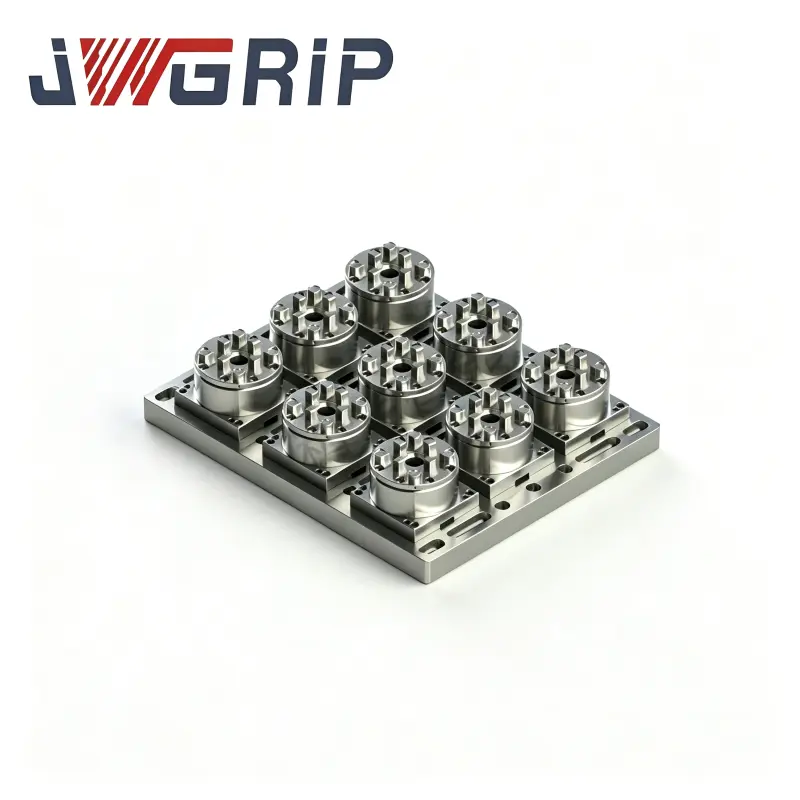
Developed by JWGRIP specifically for the pain points of multi-electrode sinker EDM machining, the R-Type 9-in-1 Pneumatic EDM Chuck breaks various limitations brought by assembling multiple scattered independent single zero-point chucks. Featuring an all-in-one monolithic base plate structure, it integrates nine independent pneumatic clamping stations, integrated manifold air control unit, high-precision positioning mechanism, hardened and ground steel, building an efficient multi-electrode quick-change workholding ecosystem.
Traditional solutions require installing, leveling and calibrating multiple loose single chucks one by one. In contrast, after the R-Type 9-in-1 chuck is mounted on the EDM machine table, it only needs one-time calibration. All nine clamping stations share the same base plate reference, thoroughly avoiding assembly cumulative tolerances caused by splicing. All key positioning surfaces go through overall quenching followed by high-precision grinding treatment. Operators can complete offline electrode presetting on external stations during machine processing cycles, so the machine will not sit idle waiting for tedious fixture calibration work.
2. How Does the R-Type 9-in-1 Pneumatic EDM Chuck Outperform Multiple Separate Single Zero-Point Chucks?
The table below compares core operating parameters and real-world production benefits between the R-Type 9-in-1 Pneumatic EDM Chuck and the conventional multiple separate single zero-point chucks solution, to intuitively show comprehensive performance improvements obtained by mold workshops.
| Performance Dimension | R-Type 9-in-1 Pneumatic EDM Chuck | Multiple Separate Single Zero-Point Chucks |
| Repeat Positioning Accuracy | ≤ ±0.002 mm, consistent across all nine clamping stations | ±0.003-0.010 mm, cumulative positioning error from multi-chuck splicing |
| Average Electrode Change-over Time | Seconds-level lock / unlock; offline pre-set, no repeated dial-gauge calibration | 15-30 minutes, each chuck needs independent leveling and re-calibration |
| Machine Non-Productive Setup Ratio | Reduce non-productive setup time by up to 80% | High idle ratio, lots of machine time wasted on fixture alignment |
| EDM Table Space Occupation | Compact monolithic layout, saves valuable table area | Large occupation when installing multiple chucks side-by-side |
| Spare-part Management Burden | One integrated unit, fewer spare accessories to manage | Large quantity of pull studs & spare parts for each individual chuck |
| Cross-Workflow Consistency | Unified reference for EDM sparking, CNC milling and CMM inspection | Reference deviation may occur between different single-chuck units |
3. What Operational Advantages Does the R-Type 9-in-1 Pneumatic EDM Chuck Bring to Daily Production?
Built on multi-station integrated architecture, the R-Type 9-in-1 pneumatic EDM chuck solves many long-standing pain points in sinker EDM mold shops.
Unified manifold pneumatic control: Nine clamping stations are driven by one shared air manifold switch. Operators can lock and release multiple groups of electrodes within seconds without adjusting each chuck separately. It reduces reliance on senior skilled technicians; even less-experienced technicians can stably complete multi-electrode clamping tasks.
One-time calibration without accumulated splicing error: The monolithic base plate guarantees unified datum for all nine positions. After one-time mounting and calibration on the EDM table, repeated leveling work is not required, completely eliminating tolerance stacking caused by assembling multiple discrete chucks.
Compact layout for optimized table-space utilization: The all-in-one design integrates nine clamping positions onto a single base plate. Unlike scattered independent chucks, it avoids fragmented table occupation. It reserves more space for workpiece placement and cable routing, prevents interference between fixtures, and fits most standard sinker EDM machine tables.
Powerful offline presetting capability supporting lights-out production: Electrodes can be assembled and adjusted on external presetting stations. Operators mount pre-aligned electrode groups onto the machine, realizing continuous batch machining and unattended lights-out production to maximize equipment output.
Strict quality control traceability: Every finished chuck undergoes full-range inspection on Zeiss CMM measuring machine before shipment. Official inspection reports can be provided upon customer request to achieve traceable quality control.
4. What High-Precision Manufacturing Scenarios Can the R-Type 9-in-1 Pneumatic EDM Chuck Perfectly Adapt To?
Multi-cavity plastic mold manufacturing: For multi-cavity mold insert processing requiring large batches of electrodes, the nine-station integrated layout can hold abundant electrode groups, shorten overall mold lead-time and prevent cumulative positioning drift.
Automotive precision mold production: Suitable for lamp housing, interior part molds with large electrode quantities. Fast electrode change-over helps mold shops cope with tight project delivery schedules.
Medical precision mold processing: For micro-cavities of medical molds, it maintains stable ±0.002 mm repeat positioning accuracy and lowers scrap risk caused by positioning drift during multi-electrode EDM operations.
5. Frequently Asked Questions About R-Type 9-in-1 Pneumatic EDM Chuck
Q1: Do I need to modify my sinker EDM machine to install the R-Type 9-in-1 pneumatic EDM chuck?
A1: No modification is required. JWGRIP provides standard mounting base plates compatible with mainstream sinker EDM models. It can be fixed on the original machine table with standard screws. No welding, cutting or on-site custom machining is needed. Normal installation can be finished within one hour.
Q2: What air pressure is required for the R-Type 9-in-1 pneumatic EDM chuck? Do I need extra pneumatic accessories?
A2: This chuck has a recommended working air pressure of 6 bar. The compressed air supply shall be dry and clean. An oil-water separator is recommended to filter moisture and impurities. Standard pneumatic connectors are included, so no complex extra pneumatic parts are required under normal conditions. If your workshop suffers unstable air pressure, a pressure regulating valve is suggested to guarantee consistent clamping force for all stations.
Q3: Will the R-Type 9-in-1 pneumatic EDM chuck get rusty and lose positioning accuracy under long-term exposure to EDM dielectric fluid?
A3: The key locating body of the chuck adopts quenched anti-rust alloy steel, and key positioning surfaces receive special hardening treatment for moderate resistance to EDM dielectric fluid. However, the chuck is not fully submersible-proof. Avoid continuous heavy flushing of pneumatic components by dielectric fluid during machining. Thoroughly remove EDM sludge and residual dielectric fluid and dry the unit after each job to sustain long-term positioning performance.
Q4: Can you provide non-standard customization based on my special EDM production requirements?
A4: Yes. Our engineering team supports custom modification for special mounting hole layout or special application conditions. Custom proposals and performance test reports will be delivered before shipment.
Q5: What daily maintenance work is required to keep long-term accuracy?
A5: Keep locating sealing surfaces clean, remove EDM carbon debris and metal chips. Maintain specified stable working air pressure. Periodically inspect pull-stud clamping condition. Simple routine cleaning can preserve its precision performance.
Conclusion
The JWGRIP R-Type 9-in-1 Pneumatic EDM Chuck adopts a monolithic multi-station structure, unified pneumatic actuation and stable micron-level positioning performance to solve these practical pain points in the manufacturing industry. It effectively improves clamping efficiency, table-space utilization and cross-process repeat positioning accuracy for mold-making.
If you want to cut non-productive setup hours or enhance multi-electrode machining stability, please share your machine specifications and regular production requirements and contact us our application engineering team. We will offer you targeted technical support and solution recommendations.
Related News
- Why Should You Choose a Compatible EROWA Uniholder 72 ER-035211 for High-Precision Workholding
- Why Do 5-Axis Job Shops Prefer Compact High Precision Self Centering Zero Point Vise with Hard Jaws
- How Can a 0-100mm Rotatable Wire EDM Vise Improve Precision and Machining Efficiency
- Is the TP UnoSet Vee Vise for Wire EDM the Ultimate Workholding Fix for Batch Cylindrical Shaft Parts Production
- Why Is the UnoSet Adapter with RSM 50 Pallet Set a Game-Changer for Modern Wire EDM Precision Manufacturing in 2026
- How Can a Wire EDM Chuck for Precision Workholding Improve Accuracy and Reduce Setup Time
Leave me a message
New Products
News Recommendations