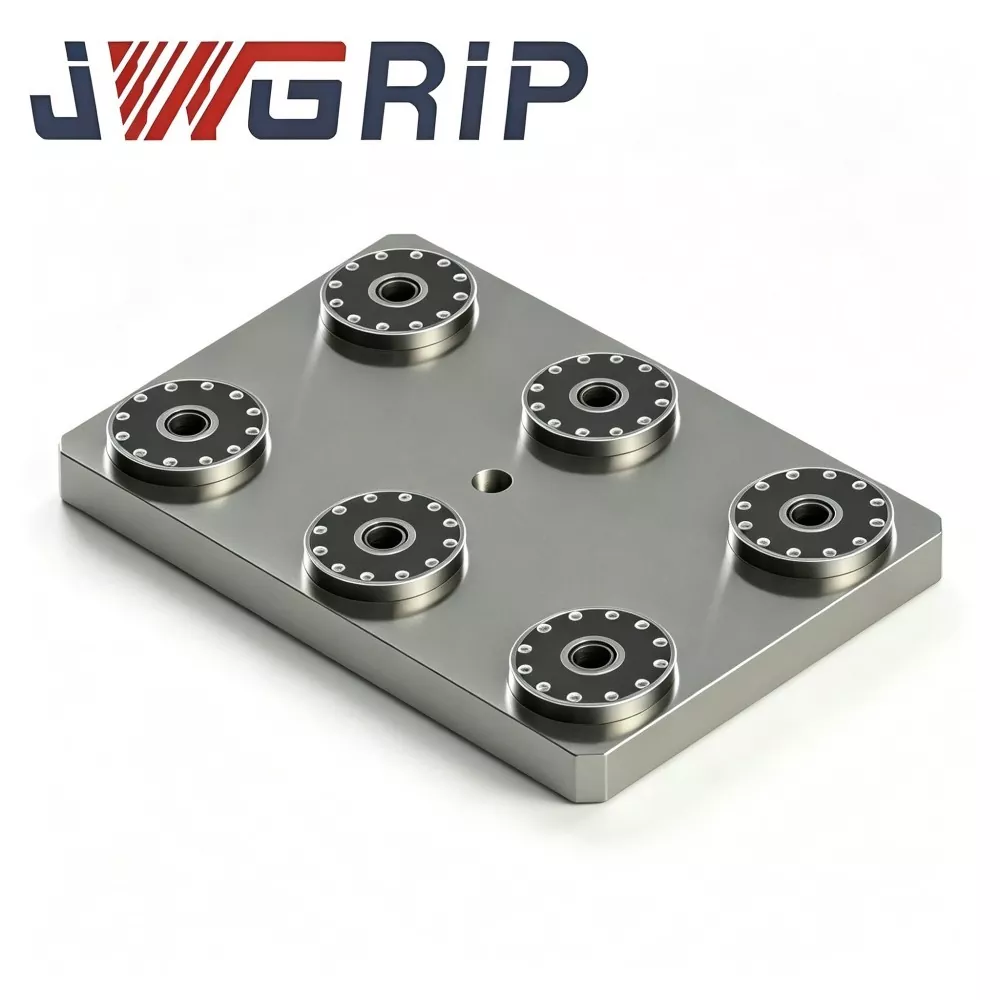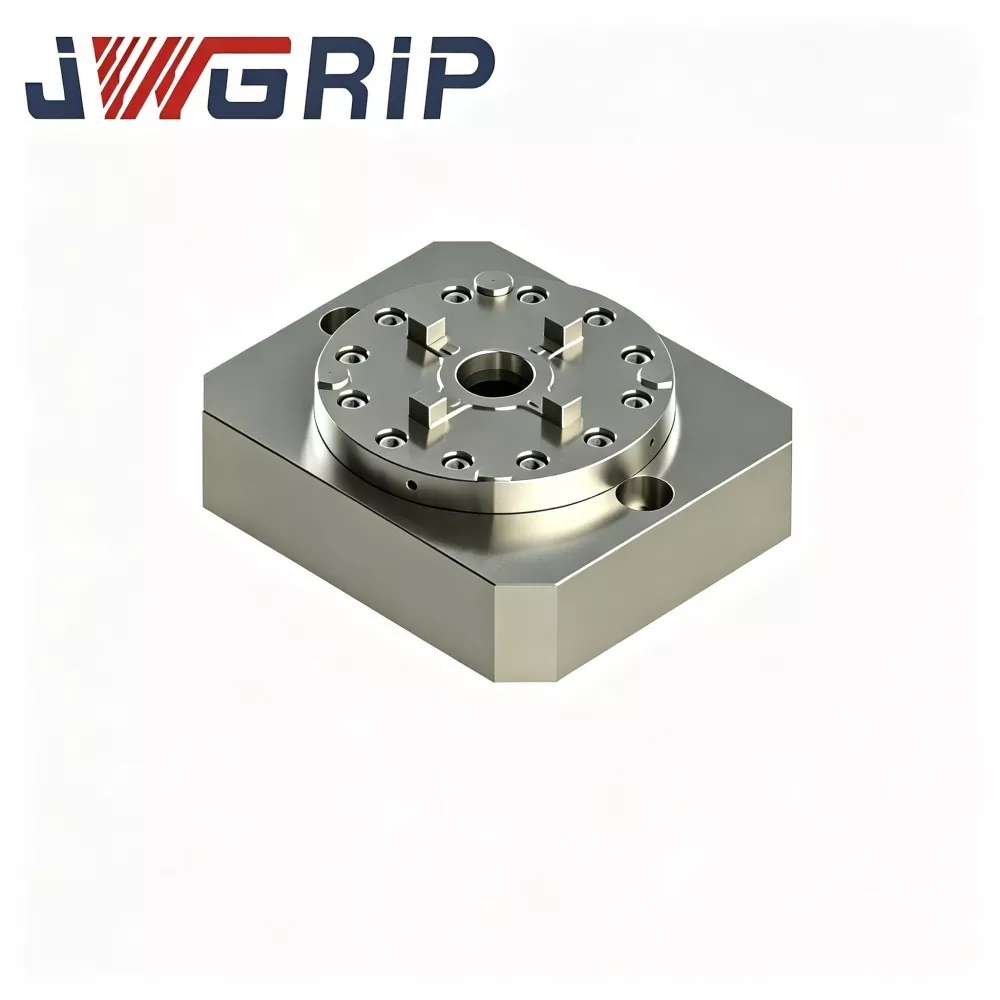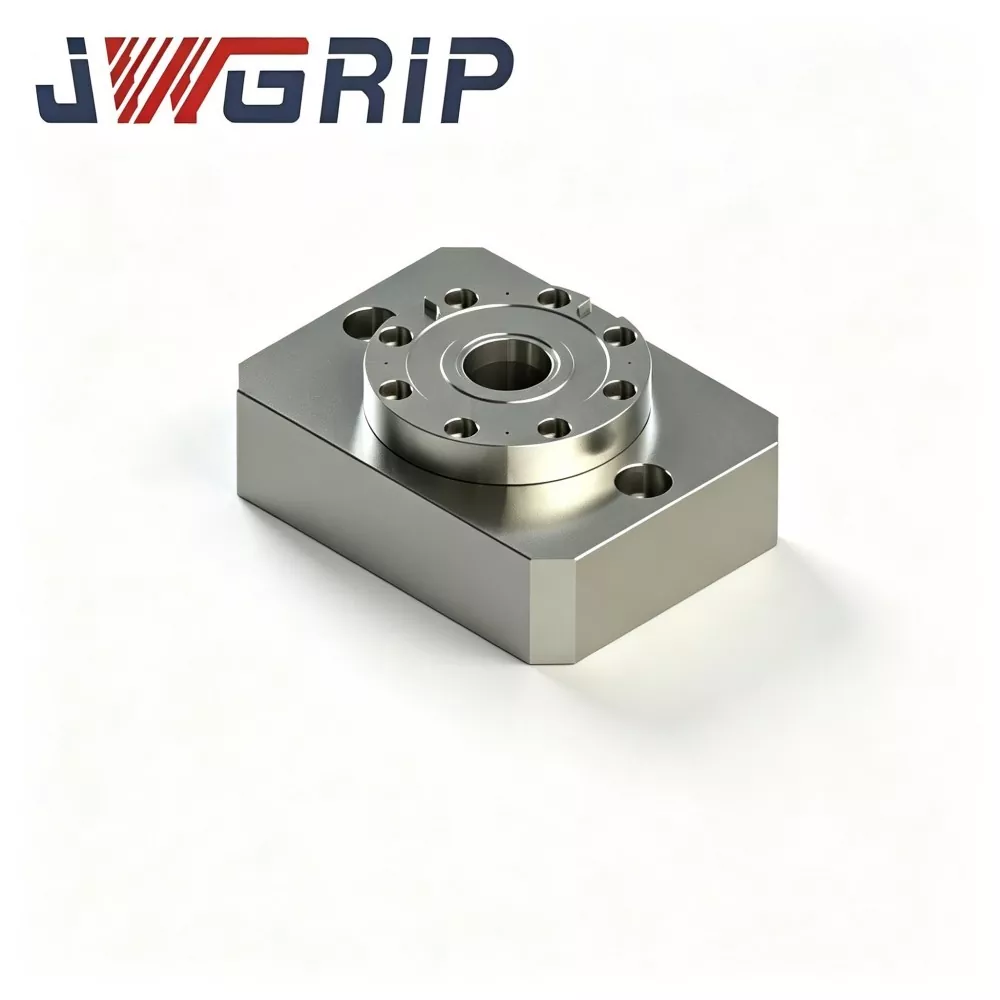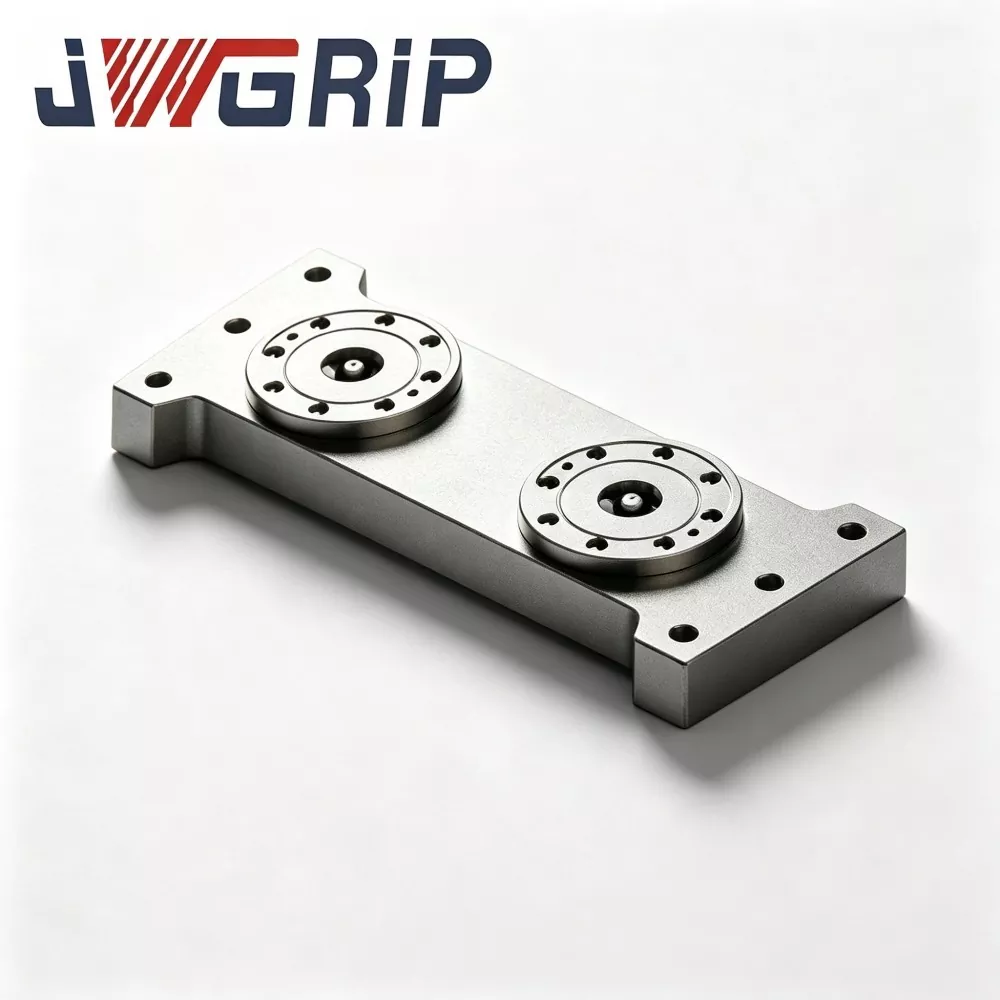
L-Type Zero Point Positioning Chuck Pallet
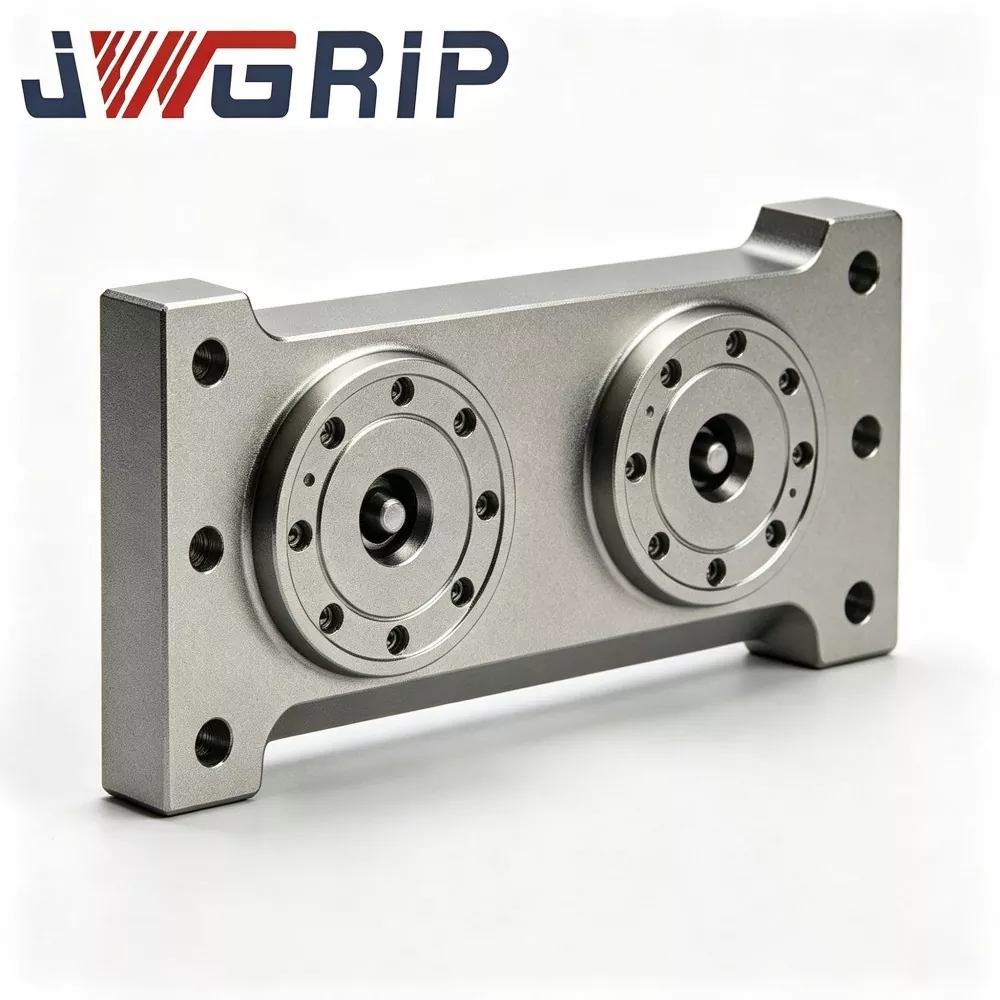
JWGRIP provides Professional L-Type Zero Point Positioning Chuck Pallet with Factory Direct sales service in China. As a core integrated fixture of the Zero Point Clamping Chuck series, this professional L-type zero point pallet is specially designed for flexible CNC machining production lines with space-limited equipment. It integrates vertical datum conversion structure and high-precision zero-point positioning components into one monolithic unit, eliminating the need for extra auxiliary adapter structures to realize vertical workpiece clamping and side feature machining.
Featuring an integrated L-shaped bent structure, the L-Type Zero Point Positioning Chuck Pallet arranges precision zero-point positioning bushing assemblies on the vertical reference surface to deliver standard 90-degree zero-point locating datum. The optimized vertical hanging installation mode effectively solves tool-fixture interference in side milling and lateral hole drilling, perfectly adapting to the machining demands of mold inserts and irregular bent parts with side key features.
This high-efficiency positioning pallet supports fast zero-point fixture swap, greatly shortening setup time and fitting high-mix-low-volume flexible production modes. It is compatible with manual fixture replacement for standalone machine operation and can cooperate with robotic grippers to achieve automatic loading and unloading of vertically hung fixtures. Widely applied in mold manufacturing and precision component processing, it delivers stable and high-precision positioning performance for space-constrained CNC machining scenarios.
Key Hardware Components
JWGRIP L-Type Zero-Point Positioning Chuck Pallet is forged from a single monolithic alloy-steel blank with no bolted spliced joints. The full assembly includes:
One-piece L-shaped main-body (horizontal mounting base + vertical locating riser)
Zero-point positioning bushing assemblies fitted on vertical riser
Internal pneumatic locking passages
Base mounting counter-sink holes
Protective cover plates for locating datum surfaces
Working process
1. Fasten the horizontal base of JWGRIP L-Type pallet securely onto the CNC machine-tool worktable.
2. Hang fixture bases pre-fitted with zero-point pull studs onto the vertical locating riser face.
3. Feed 0.5-0.7 MPa compressed air; built-in pneumatic passages actuate zero-point bushings to complete locking.
4. Position-confirmation signal outputs to the CNC system. The spindle faces workpiece side faces directly and executes side milling, lateral drilling and side cavity machining cycles.
5. Once machining finishes, release air pressure to unlock. Vertically hung fixtures can be removed for next-batch loading.
Engineering Design
Many competing L-shaped fixtures adopt split bolt-spliced construction. Repeated lateral cutting impact creates tiny gaps at joint interfaces and brings locating-accuracy drift.
JWGRIP adopts one-piece forging to eliminate spliced joint surfaces, delivering strong resistance against continuous lateral cutting impact.
After forging, alloy-steel blanks undergo dual stress-relief aging cycles to release residual stress from forging and CNC machining. Under side-clamping conditions, fixtures sustain persistent horizontal cutting force; unreleased internal stress would trigger gradual substrate deformation and degrade locating accuracy over long-term cyclic loads.
Positioning bushings are manufactured from high-hardness bearing steel. Inner bores receive quenching plus honing super-finishing to guarantee stable repeat-positioning accuracy on the vertical riser stations.
Production Advantages
1. 90° zero-point datum conversion solves side-machining interference on compact machines
On small-table machines, vertically hung workpieces face the spindle directly without large-angle spindle tilting. Tool-fixture collision risks are reduced, unlocking full machining capacity for compact-envelope equipment.
2. Joint-free monolithic forging withstands lateral cutting impact
Different from bolt-assembled right-angle fixtures, the one-piece forged structure removes joint-loosening risks. It maintains locating stability under sustained side-milling forces and lowers chatter marks and surface defects caused by micro fixture movement.
3. Retain zero-point quick-change benefits for side-feature setups
Vertical-riser zero-point bushings match industry-standard D20 zero-point pull studs. Existing fixture bases only need retrofitting with standard pull studs for vertical hanging. No manual indicating-and-alignment during fixture swap, drastically shortening setup time for side-feature machining.
4. Preserve valuable Z-axis travel for compact machines
Conventional horizontal clamping consumes Z-axis stroke. Vertical-hanging layout shifts workpieces toward Y-direction, saving limited Z-axis travel for small-footprint CNC equipment and making some previously stroke-limited parts manufacturable.
5. Fit both manual workshops and automation retrofits
Operators can replace vertical fixtures manually. Meanwhile vertical zero-point datum can pair with robot grippers to handle vertically oriented fixture bases for automatic loading-unloading. Old-machine upgrades can be completed without full-equipment replacement.
6. Chip-slope design lowers maintenance frequency for vertical-hanging setup
Inclined chip-slope surfaces surround the riser datum. Cutting chips slide downward and rarely get trapped inside positioning-bushing gaps, reducing cleaning workload under vertical side-clamping conditions.
Application Cases
JWGRIP L-Type Zero Point Positioning Chuck Pallet is widely deployed on compact vertical machining centers and small-size 5-axis machines for side-hole, side-cavity and side-slot feature machining.
Case 1: Mold-Making Workshop
This customer runs multiple compact vertical CNC machines for side-cavity machining of miniature mold inserts.
Before upgrade: split-type angle blocks plus vises were used for side clamping. Each fixture swap required manual indicating and alignment, taking 3-5 minutes every time. Bolt-joint angle blocks tended to loosen under cutting impact, generating frequent chatter marks on workpiece side surfaces.
After rolling out JWGRIP L-Type pallets: zero-point quick-change removes manual alignment work. Fixture-swap time drops to 7-10 minutes. One-piece L-shape improves rigidity against lateral cutting force. Chatter-mark defects are greatly suppressed, and pass-rate for mold-insert side-face surface roughness rises significantly.
Case 2: Precision-Component Processing Factory
The site operates small-size 5-axis machines with constrained internal working volume. A large share of workpieces require side-feature machining. With JWGRIP L-Type pallet’s vertical hanging solution, large-amplitude spindle tilting is no longer necessary. Spindle-collision probability goes down. Saved Z-axis stroke enables processing of parts that could not be finished previously due to stroke limits.
Complete Production Workflow
1. One-piece L-shape forging of alloy-steel blank
2. Rough-machining
3. First stress-relief aging
4. Semi-finishing
5. Secondary stress-relief aging
6. Super-precision grinding for datum faces
7. Bushing press-fitting
8. Pneumatic-circuit seal assembly
9. Air-tightness pressure-holding test
10. Multi-item accuracy inspection
11. Anti-rust protection treatment
12. Export-grade shock-proof packing
Inspection Checklist
Vertical-station repeat-positioning-accuracy test
90-degree right-angle geometric accuracy test
5-minute air-holding air-tightness test, max allowable pressure drop ≤0.02 MPa
Cyclic locking-unlocking functional verification
Every unit ships with factory-issued accuracy-inspection data sheet for customer fixture-equipment archiving.
Product Evaluation & Selection
Check available mounting space on machine-tool worktable. Calculate length-and-width footprint of L-type base to avoid collision with machine guard and spindle moving range.
Evaluate total weight of workpiece plus fixture base. Vertical hanging creates cantilever loading condition. Never exceed published maximum allowable cantilever load rating.
Confirm specifications of on-site zero-point pull studs. Standard version fits D20 pull studs. Custom bushing assemblies can be developed for alternative pull-stud sizes upon request.
For robot-automation integration: assess gripper reach toward vertically-oriented fixture bases. JWGRIP technical team can support feasibility evaluation.
Operation Precautions
Tighten mounting bolts for L-type horizontal base strictly according to torque-value requirements in JWGRIP user manual. This pallet bears cantilever lateral cutting force; insufficient bolt torque causes micro vibration of the whole unit and ruins machining accuracy.
Install oil-water filter at compressed-air inlet front-end. Moisture and impurities entering bushings trigger rusting and abrasion and lead to accuracy drift.
Spray dry-lubricant aerosol onto vertical-riser zero-point bushings after every cumulative 80-100 working hours. Liquid engine oil is strictly prohibited. Liquid oil traps downward-sliding metal chips and causes bushing-jamming failures.
At each shift-change, blow-clean vertical locating riser and bushings from top-down direction with compressed-air to clear accumulated sliding chips.
Avoid heavy impact hitting vertical locating riser face. Collision-induced riser deformation will almost permanently damage 90-degree right-angle accuracy and locating performance.
Strictly prohibit overload operation beyond rated cantilever load. Overload will bring permanent substrate deformation.
Packaging & Shipment
Packaging: Export-grade shock-proof solid-wood case with thick foam inner buffer. Special protective treatment is applied for vertical locating datum face to prevent collision damage in long-distance ocean-going transit.
Standard lead-time: 14-20 working days. A small number of standard SKUs are kept in stock for expedited shipment.
After-Sales Support
Warranty: 12-month full-unit warranty covers manufacturing defects excluding human-caused misuse or collision damage. Qualified claims enjoy free repair or spare-part replacement.
Technical resources: Online operation documents are provided. Paid remote technical support is available for bulk-volume order projects.
Custom modification service: riser height adjustment, pull-stud-spec alteration, multi-station layout design on vertical riser are supported.
Sample evaluation: Evaluation sample can be arranged; buyer shall bear sample freight cost.
FAQ
Q1: Can JWGRIP L-Type Zero Point Positioning Chuck Pallet be laid flat and used as an ordinary horizontal zero-point pallet?
A: It is purpose-built for vertical side-hanging clamping. Flat-lay usage is not recommended. The actual force-bearing mode deviates from substrate design specification and will easily exceed rated load capacity.
Q2: Will machining vibration occur under cantilever side-hanging clamping?
A: Within rated allowable load range, the one-piece forged substrate provides sufficient rigidity. Noticeable chatter will happen if combined workpiece-and-fixture weight exceeds cantilever-load rating. Total-weight calculation is mandatory during product-selection phase.
Q3: Can my existing zero-point fixture bases be used on the vertical riser of this L-type pallet?
A: Fixture bases equipped with standard D20 zero-point pull studs can be hung directly without fixture remanufacturing.
Q4: Is JWGRIP L-Type pallet compatible with 5-axis CNC machines?
A: It works with small-size 5-axis machines. Complete interference assessment covering fixture-pallet-spindle-tilt motion must be completed at selection stage.
Procurement Decision Insight
Many users of compact-envelope CNC machines face tricky side-feature-machining challenges. Low-cost conventional angle blocks lack zero-point quick-change capability and bring long setup time. Ordinary horizontal zero-point pallets cannot achieve 90-degree vertical datum conversion.
JWGRIP L-Type Zero Point Positioning Chuck Pallet combines high-rigidity one-piece L-shaped forging structure and zero-point quick-change system. It solves core fixture bottlenecks for side-feature machining on space-limited machine tools, delivering tangible practical value for mold-making and irregular-precision-part side-processing applications.
Hot Tags: L-Type Zero Point Positioning Chuck Pallet
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.