English
- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик
High-Performance Wire EDM Fixture Accessories for Precision Machining Operations
As a full-range fixture supplier of Wire EDM Fixture Accessories, JWGRIP manufactures high-precision alignment seats, V-type clamping holders, bridge adapter plates and reference guide components for mold repair workshops, job-shop operators and fixture procurement specialists troubled by fixture compatibility gaps and insufficient locating reference points in daily wire-cut production. All accessories adopt anti-rust treated alloy steel, with fine-ground key mating surfaces to maintain flatness and parallelism under long-term circulating-water immersion.
These auxiliary components solve connection bottlenecks between main clamps and machine tables, improving hardware adaptability for special-shaped, ultra-thin or over-hanging workpieces. JWGRIP also delivers Wire EDM Vises and R-Type EDM Workholding System, helping users build complete combined workholding chains for wire-cut and sinker EDM processes.
Many wire-cut workshops only invest budgets on main clamping bodies such as vises and chucks, ignoring the supporting auxiliary parts that determine overall fixture adaptability. Even high-performance main clamps cannot handle special-structure workpieces without matched auxiliary accessories. When processing ultra-thin blanks, tall over-hanging parts or parts requiring offset installation, operators often have to make makeshift spacer blocks, simple brackets or temporary locating supports on site.
These self-made makeshift parts lack strict flatness control and anti-corrosion treatment. Under long-term water flushing and chip accumulation, homemade spacers easily deform, rust or trap fine particles, which will tilt workpieces and introduce invisible locating errors. Many generic accessories sold on the market adopt general-purpose dimensional standards, failing to match existing vises and chucks perfectly, resulting in assembly clearance and unstable datum during wire-cut submerged processing.
What value can standardized auxiliary locating components bring to day-to-day wire-cut mass-production and prototype-making tasks?
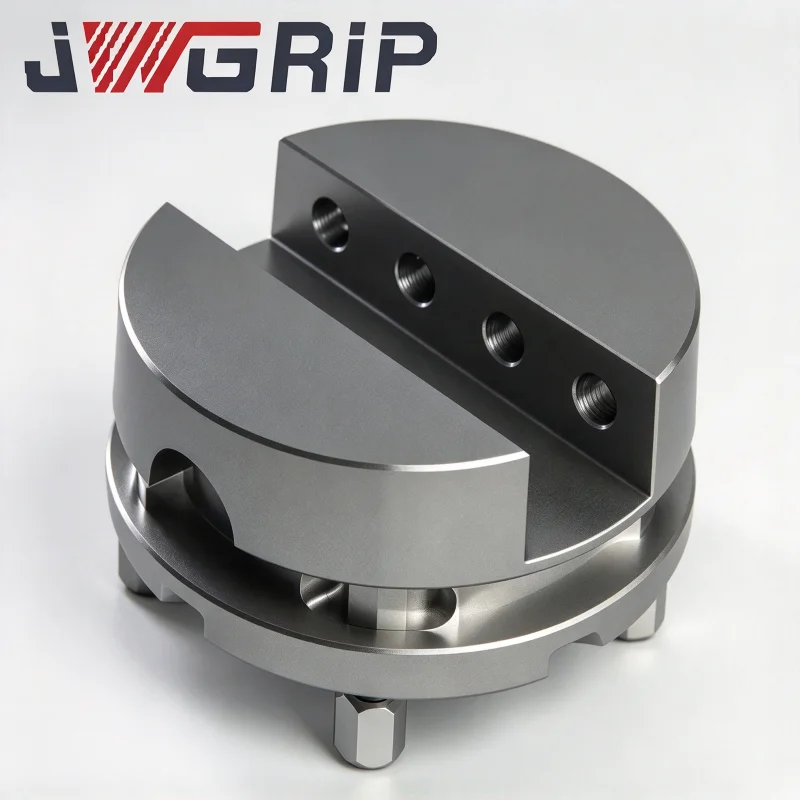
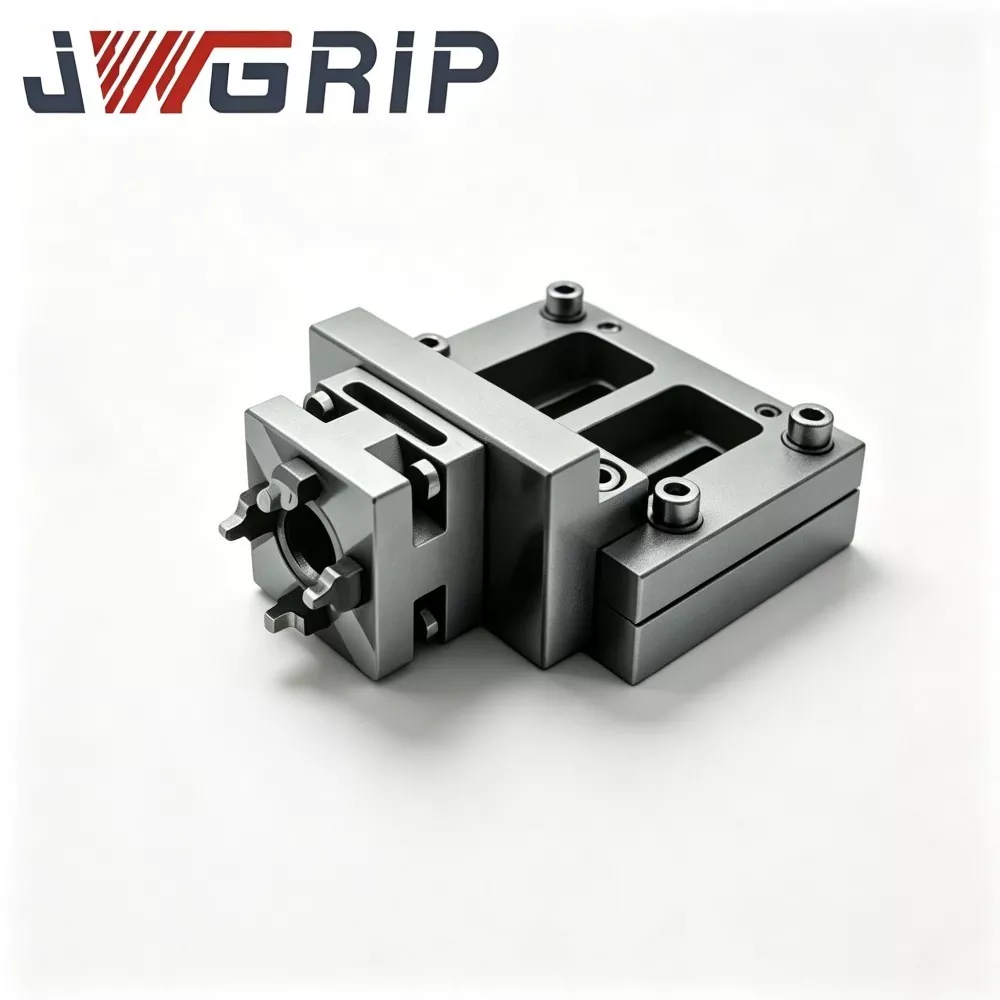
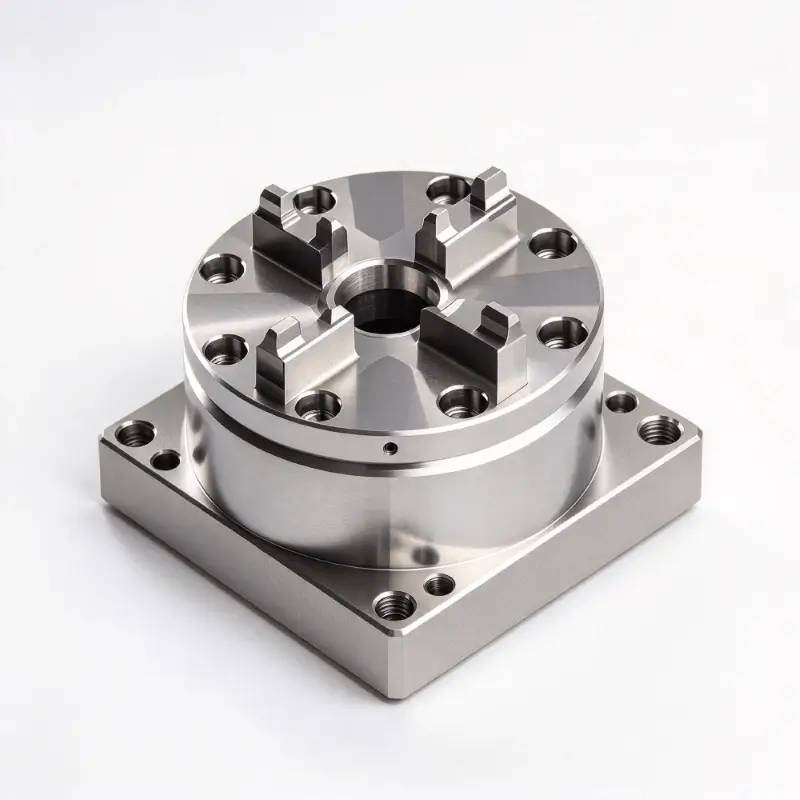
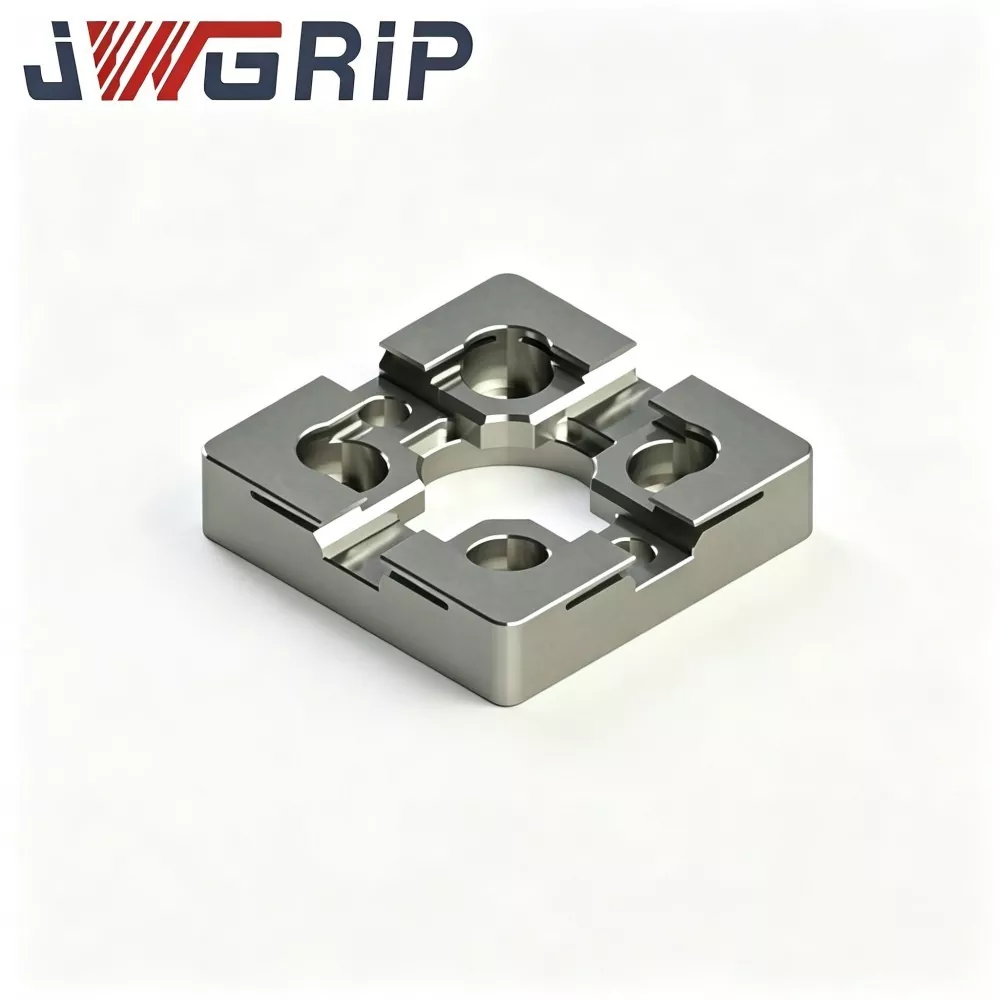
Temporary self-made shims and simple brackets can only satisfy extremely low-requirement processing. They cannot offer repeatable datum transfer or stable offset installation under cyclic water immersion. In contrast, Wire EDM Fixture Accessories are purpose-built auxiliary modules for wire-cut submerged operating scenarios. The WEDM Adapter for Wire EDM Workholding acts as a multi-direction alignment seat for fast position correction without repeated indicator calibration. The Wire EDM Round Clamp Holder provides reliable V-shaped supporting and clamping for shaft-like and circular work-pieces.
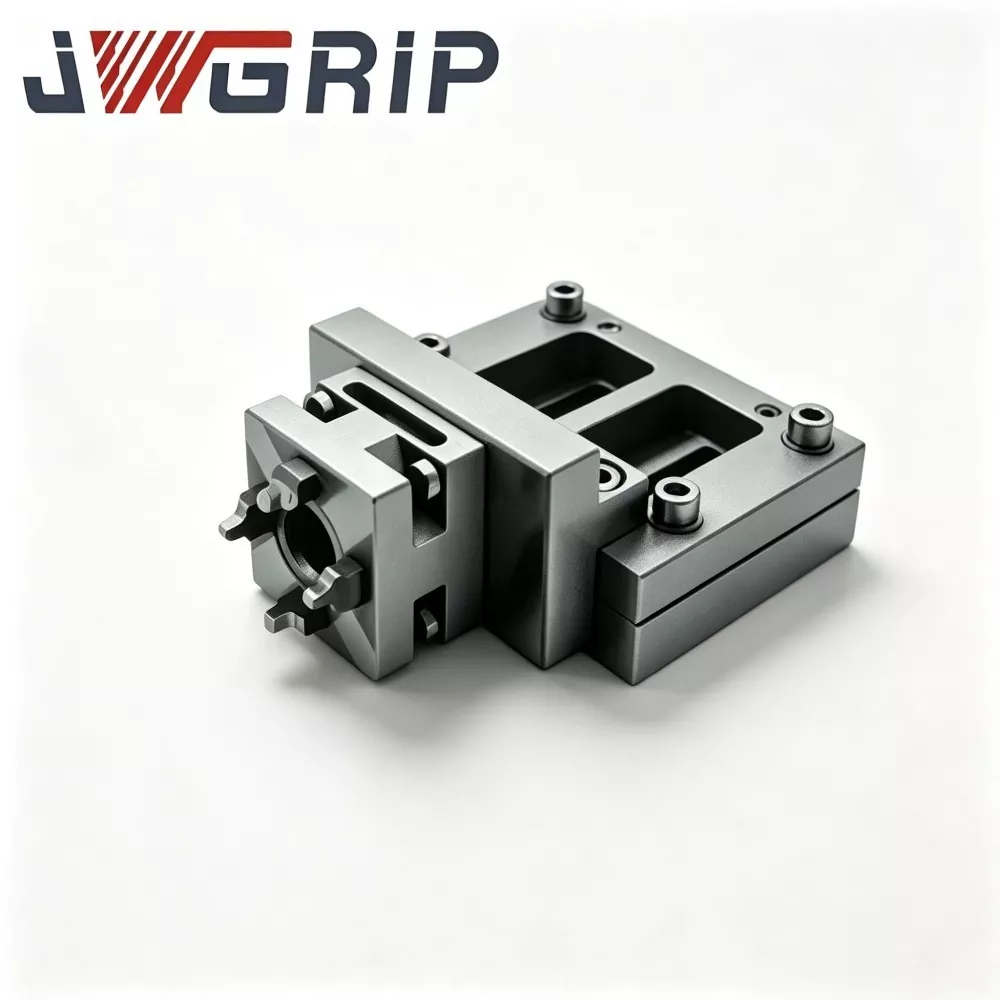
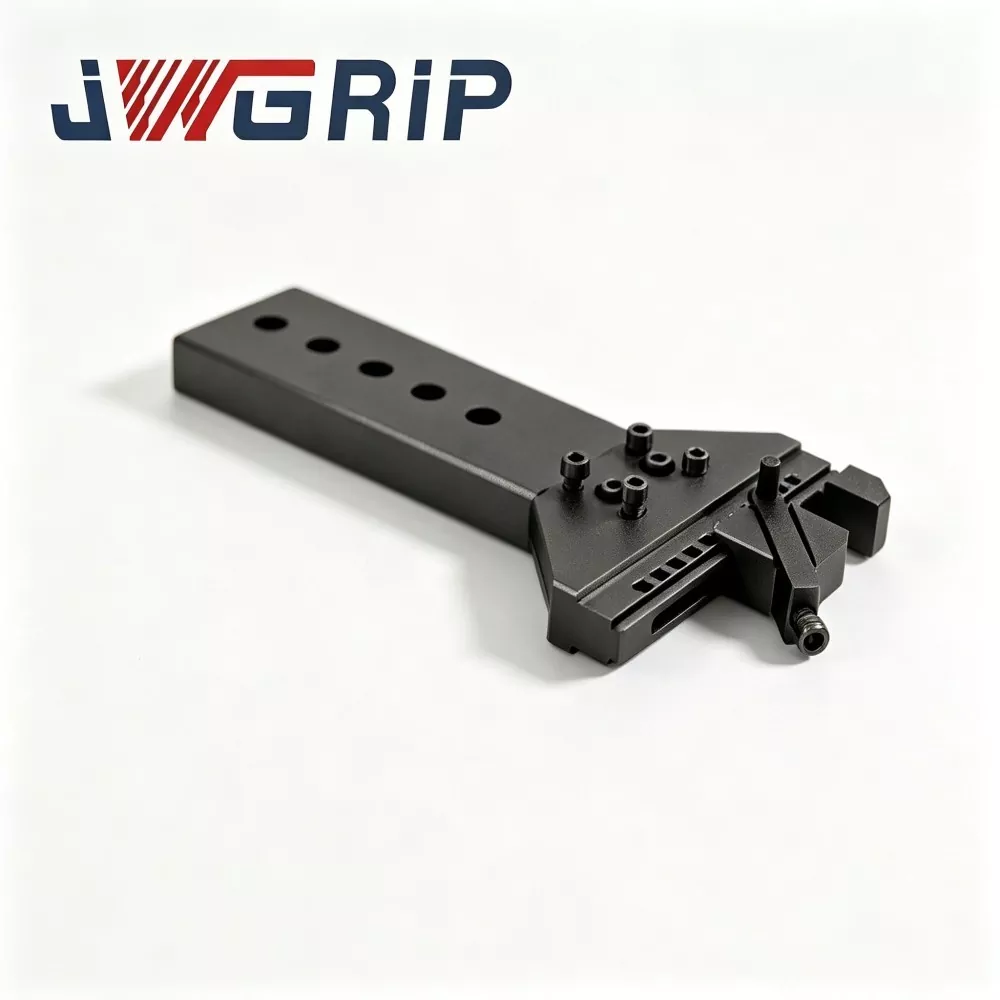
The Beam Pallet Set for Wire EDM Workholding lifts the whole fixture assembly, reserving sufficient bottom space for brass-wire penetration when processing tall or over-hanging blanks. The WEDM Reference Element for Precision Workholding serves as benchmark reference rail, helping operators quickly confirm datum position before formal cutting starts. All accessories undergo unified precision grinding and anti-corrosion surface treatment. Standardized mounting holes guarantee interchangeability with mainstream main-body clamping hardware. With these auxiliary modules, workshops no longer rely on makeshift handmade parts, and locating repeatability remains consistent across different batches of wire-cut jobs.
How can factories reduce makeshift on-site fabrication of spacer blocks and auxiliary brackets in high-mix wire-cut production?
High-mix and small-batch orders dominate most wire-cut job-shops. Workpieces vary greatly in height, profile shape and installation requirements. If every special-shaped workpiece requires operators to produce temporary supporting parts, plenty of working hours will be consumed by fixture preparation rather than real cutting progress.
Wire EDM Fixture Accessories allow operators to combine different auxiliary modules on external setup benches. Multi-direction alignment seats, V-type clamp holders, bridge pallet sets and reference rails can be freely assembled according to workpiece height, shape and offset requirements. After completing combination, adjustment and inspection outside the machine, the whole fixture stack can be mounted onto Wire EDM Vises or other main clamping bodies in one step. There is no need for on-site cutting, grinding or fitting of temporary spacer blocks.
If workshops hope to realize unified datum across multi-process workflows, these accessories can cooperate with modules from Quick Change Workholding System, achieving fast transfer of assembled fixture groups between pre-setting platforms and wire-cut machine worktables. This working pattern cuts manual makeshift-part production time and lowers hidden risks caused by uncalibrated homemade supports.
Core Product Strengths
Pre-manufactured standardized auxiliary modules replace makeshift handmade spacer blocks, avoiding locating deviation caused by poor flatness of self-made parts.
Diversified functional modules cover multi-direction alignment, circular-part clamping, fixture height lifting and datum reference checking for complex wire-cut workpieces.
Anti-rust surface treatment plus precision-ground mating surfaces maintain stable performance under long-term circulating-water immersion and chip accumulation.
Modular combination design supports flexible assembly and matching with mainstream vises, chucks and pallet-type clamping bodies inside wire-cut workshops.
Product Module Overview
JWGRIP auxiliary component portfolio includes alignment adapters, circular clamping holders, bridge-type lifting pallets and datum guide parts to solve various fixture matching difficulties in wire-cut production.
WEDM Adapter for Wire EDM Workholding is a multi-direction alignment seat, simplifying workpiece position correction and reducing repeated dial-indicator work. Wire EDM Round Clamp Holder delivers stable V-type clamping for round shafts, pin parts and cylindrical mold components. Beam Pallet Set for Wire EDM Workholding lifts the entire fixture assembly; it creates bottom clearance so that brass wire can pass freely for tall, over-hanging and deep-profile workpieces.
WEDM Reference Element for Precision Workholding works as benchmark guide rail for fast datum confirmation before cutting. All these components belong to the complete Wire EDM Workholding Fixtures product ecosystem. When subsequent sinker-EDM processing is required for mold parts, users can select matched components from R-Type EDM Workholding System, continuing to use consistent locating references across different processing stations.
Typical Application Scenarios
These auxiliary fixture components find wide application in precision stamping die maintenance, connector part processing, medical miniature component manufacturing and custom prototype wire-cut subcontracting. They are compatible with medium-speed and high-speed wire-cut equipment, solving fixture matching problems for over-hanging parts, shaft-shaped blanks, offset-installation workpieces and parts needing fast datum checking. Whether renovating old wire-cut production lines or building flexible high-mix processing cells, properly-selected auxiliary accessories eliminate homemade spacer-block risks and improve overall locating stability of the whole fixture group. They are widely adopted by mold repair workshops, prototype-focused job-shops and enterprises undertaking diverse customized wire-cut orders.
Practical Guidance
First analyze workpiece structural features: over-hanging or tall workpieces need height-lifting solutions such as Beam Pallet Set for Wire EDM Workholding. Shaft-type circular blanks should be matched with Wire EDM Round Clamp Holder. Workpieces requiring frequent position correction can adopt WEDM Adapter for Wire EDM Workholding to simplify alignment operations.
Second check dimensional compatibility with your existing main-body clamping hardware including vises and chucks. Evaluate your production mix: high-mix prototype workshops benefit more from full sets of combinable auxiliary modules.
If you plan to realize cross-station fixture circulation, confirm interface compatibility with Quick Change Workholding System modules in advance. When facing confusion about module combination schemes, you may refer to JWGRIP application case documents and dimension tables to select suitable accessories based on workpiece height, shape and installation constraints.
Usage and Maintenance Notes
Metal chips, carbon particles and circulating-water sludge will accumulate on reference planes and mounting holes during continuous wire-cut production. Regular cleaning of mating surfaces, positioning holes and supporting edges prevents particle-triggered tilting and hidden locating deviation. Avoid hammering or heavy knocking on precision ground reference surfaces; impact will generate indentations leading to permanent accuracy loss.
After daily production, rinse each accessory completely, wipe away water stains and apply anti-rust protection. Store disassembled auxiliary modules on dedicated storage racks to prevent surface scratches. Inspect flatness and mounting hole conditions periodically for frequently-used accessories; retire components with obvious indentations, corrosion pits or deformed mounting holes. Standardized maintenance habits preserve datum quality of auxiliary components and reduce hidden fixture-caused defects for high-mix wire-cut batches.
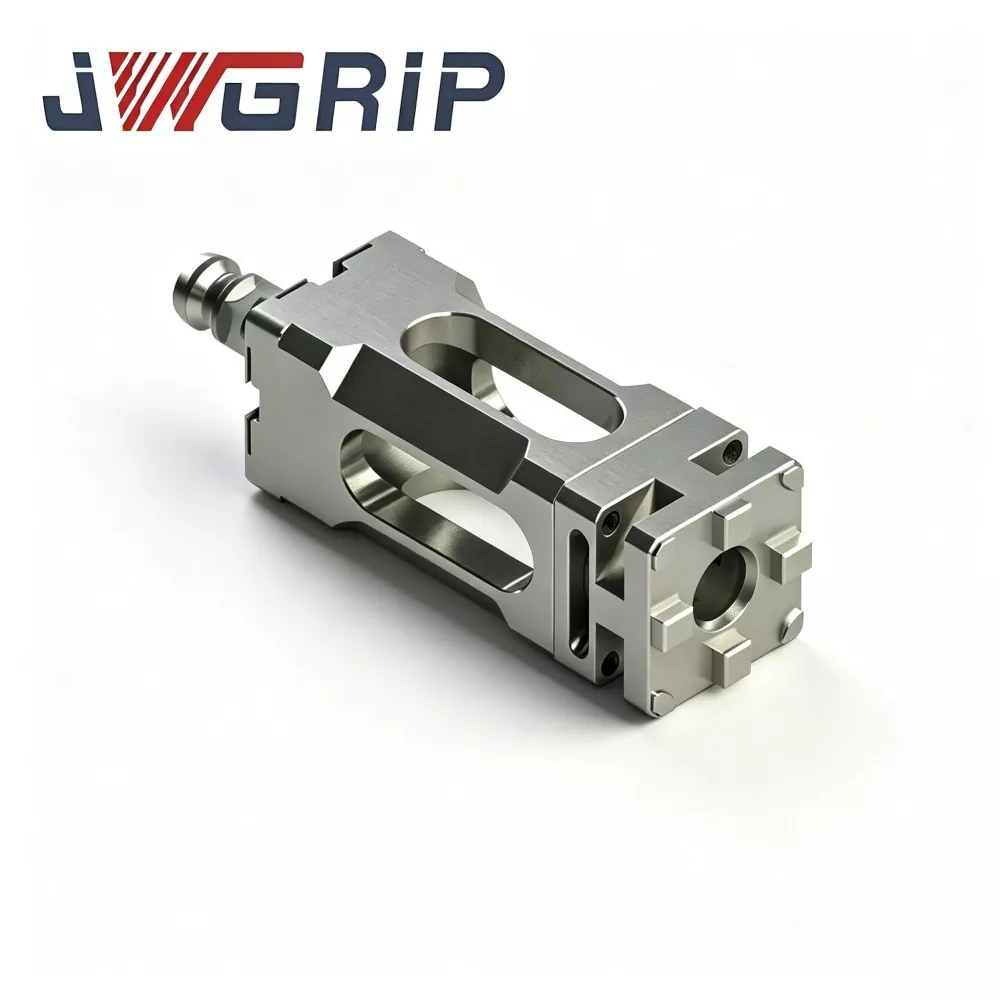
JWGRIP is a professional Wire EDM Fixture Accessories manufacturer and supplier in China. We warmly welcome you to wholesale high quality products at competitive price from our factory.
News Recommendations