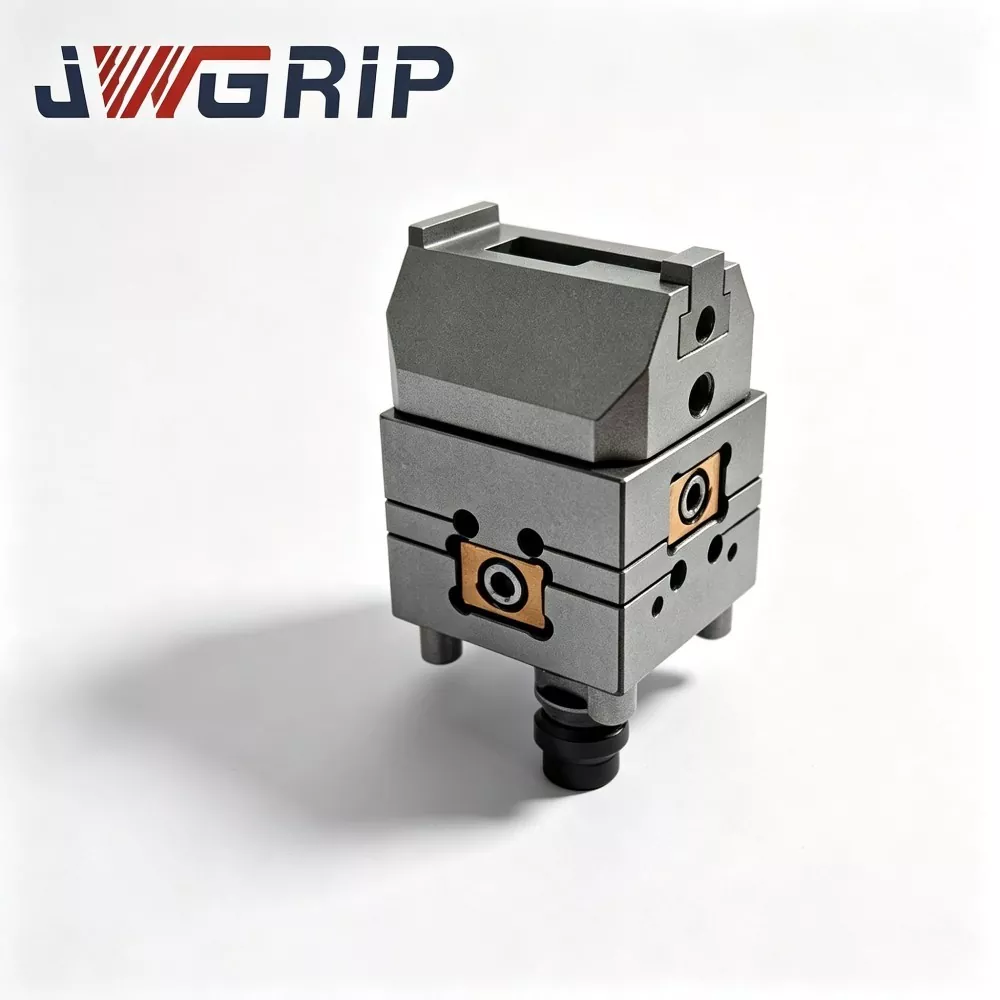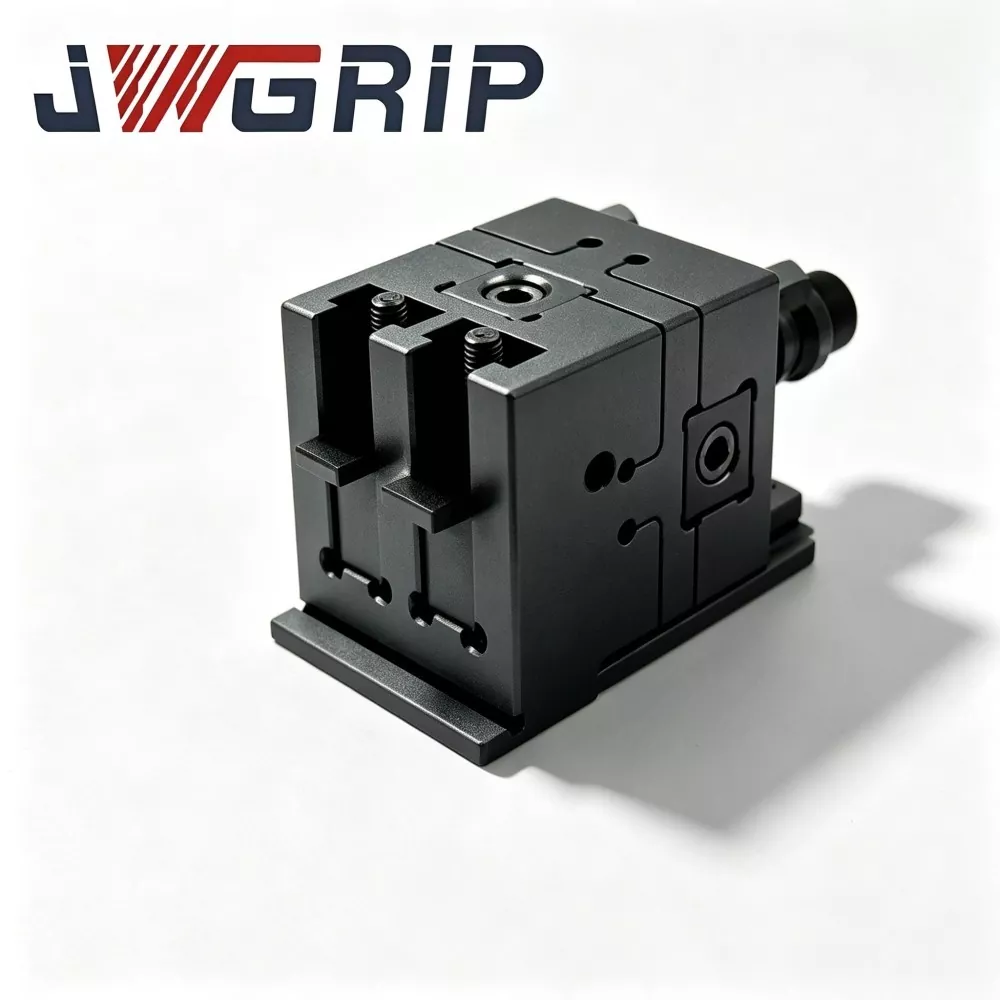
0-100mm Rotatable Wire EDM Vise
JWGRIP is the manufacturer and supplier of the Professional 0-100mm Rotatable Wire EDM Vise in China. It is high-precision workholding hardware purpose-engineered for multi-angle, taper-profile and spatial-inclined-cavity submerged wire-cut tasks. Made of thermally stabilized pre-hardened alloy steel, it adopts high-resolution rotary indexing platform and multi-point rigid position-locking mechanism, supporting continuous angular adjustment within 0-100mm clamping range. It firmly locks arbitrary rotary positions with high structural rigidity and maintains excellent angular repeatability under long-term dielectric fluid splashing and humid submerged conditions.
The 0-100mm Rotatable Wire EDM Vise addresses the drawbacks of traditional wire-EDM vises which only support fixed clamping angles. Traditional fixtures require tedious manual alignment and repeated dial testing for tapered or inclined workpieces and easily produce human-induced errors leading to unstable taper precision and inconsistent batch quality.
Equipped with high-precision rotary indexing and rigid locking structure, the thermally stabilized steel-body vise resists deformation and corrosion in harsh workshop environments and sustains long-term stable indexing accuracy. It improves machining flexibility and production efficiency and is widely applied in mold process-development laboratories and precision tool-making departments for complex spatial-angle submerged wire-EDM processing.
Real-world pain points
Many mold-process-development labs and precision tool-making departments frequently process complex work-pieces with spatial inclined surfaces, taper contours and non-orthogonal cavity features. Achieving stable repeatable angular datum inside submerged wire-EDM tanks remains a long-standing tricky technical problem.
· Most conventional work-holding hardware only offers orthogonal X/Y-axis positioning. When inclined features need machining, operators mostly adopt manual angle-plate fixtures. Ordinary manual angle-plates rely on external protractor reading for setting. After clamping-force loading or multiple tank thermal cycles, subtle angular drift occurs. Tiny angular deviation is invisible to naked eyes yet gets amplified on taper and inclined-wall surfaces and results in non-conforming part geometry. For prototype debugging jobs, repeated disassembly and dial-indicating consumes plenty of machine runtime and slows down process validation progress.
· Some market-available rotary vises are retrofitted from general-purpose milling-machine rotary components. They lack anti-pollution optimization dedicated for wire-EDM dielectric-fluid and fine sludge. After short-period submerged-tank operation, rotary clearance gets contaminated, indexing resolution drops and locking rigidity deteriorates.
R&D Orientation
JWGRIP 0-100mm Rotatable Wire EDM Vise is purpose-built to resolve angle-setting and repeat-reproduction bottlenecks for wire-EDM process-development scenarios. Different from milling-retrofitted rotary assemblies, its full set of rotary-indexing and locking mechanism is optimized for submerged-tank operating environments.
1. Drawing on abundant prototype-process data accumulated by JWGRIP as contract manufacturer for custom fixture projects, multiple prototype revisions complete combined rotary-locking aging test under simulated dielectric-fluid splash conditions before mass-production release.
2. Operators mount this vise onto wire-EDM machine worktable. Once angle indexing finishes, multi-point locking structure rigidly fastens rotary platform, and users can proceed with inclined-feature wire-cut machining.
3. Beyond standard configuration, JWGRIP can deliver custom structural adjustments for special process-development fixture-cell requirements.
Technical Bottlenecks
We sort out four frequent technical bottlenecks in wire-EDM angular-feature machining and illustrate how JWGRIP 0-100mm Rotatable Wire EDM Vise implements targeted improvements:
1. Poor angular repeatability of ordinary manual angle-plates Manual angle-plates depend on post-setup manual dial-indicating. Lock-in stress plus tank thermal fluctuation easily triggers angular drift. JWGRIP high-rigidity multi-point-locking rotary platform realizes mechanical indexing positioning, reduces reliance on manual calibration and improves angular-datum repeatability for prototype batches.
2. Rotary-mechanism contamination-caused failure under submerged-tank conditions General-purpose rotary units have no labyrinth anti-contamination barrier. Wire-cut sludge invades rotary clearance and brings indexing jitter and weakened-locking rigidity. This rotatable vise adds circumferential labyrinth-type sludge-proof barrier around rotary-indexing clearance and slows pollutant intrusion into internal rotary pairs.
3. Insufficient effective clamping range of many rotary vises Quite a number of rotary wire-EDM vises only provide narrow jaw opening and cannot accommodate medium-size prototype blanks. This model adopts 0-100 mm effective jaw clamping span and fits various blank dimensions for process-debugging work.
4. Cumulative time loss caused by repeated angular re-indicating Frequent disassembly and dial-indicating for multi-angle prototype samples occupies valid machine-hours. Its index-and-lock integrated structure cuts repeated teardown-and-indicating steps during process-development angle-switching.
Working Principle
JWGRIP 0-100mm Rotatable Wire EDM Vise consists of three core functional assemblies:
fixed base-body, rotary indexing platform and multi-point circumferential locking module.
① Fixed base-body mounts on wire-EDM worktable and maintains stable spatial-datum relation with machine table.
② Rotary indexing platform carries movable-jaw and fixed-jaw assemblies. Operators rotate platform to set target machining angle; scale marks plus reference reading edge offer visual angle auxiliary reference.
③ After angle adjustment completes, circumferential multi-point locking module acts synchronously, applying uniform pre-load around rotary-platform circumference to constrain rotary-platform degrees-of-freedom.
④ Labyrinth barrier between base-body and rotary-platform blocks most wire-cut sludge and dielectric-fluid splashes from entering inner rotary-pair clearance.
Functional Boundary & Main Application Scope
Important functional boundary statement: JWGRIP 0-100mm Rotatable Wire EDM Vise provides mechanical angular indexing and locking datum. It cannot eliminate angular deviation caused by workpiece-blank deformation or jaw-surface wear. After mechanical locking, probe-based angle verification and fine compensation are still mandatory before formal wire-cut processing.
Main application: process prototype debugging and small-batch production of inclined mold inserts, taper-type punches, spatial-angle gauge-components in submerged wire-EDM tanks.
Technical Characteristics
1.0-100 mm Wide-range Jaw-clamping Span Comparative application test shows:
JWGRIP 0-100mm Rotatable Wire EDM Vise covers more prototype-blank size specifications compared with narrow-opening rotary vises, satisfying multi-specimen mixed-debugging demands inside process-development laboratories.
2. Circumferential Labyrinth Anti-contamination Barrier for Rotary-pair
Under identical splash-pollution test conditions, labyrinth-barrier structure reduces sludge-particle invasion probability into rotary clearance by approx. 30 %, slowing rotary-pair wear and indexing-performance degradation under submerged-tank conditions.
3. Multi-point Synchronous Circumferential Locking Mechanism
Multi-point distributed locking pre-load improves rotary-platform rigidity after locking and lowers risk of local-angular micro-tilt induced by single-point locking stress-concentration.
4. Thermally-stabilized Pre-hardened Alloy-steel Main-structure
Main-base and rotary-platform go through multi-stage thermal-stabilization aging. Within 14-32 ℃ workshop-temperature range, structural datum-plane flatness variation ≤0.0029 mm, mitigating thermal-deformation influence over angular datum.
5. Hardened Jaw-clamping Surfaces plus Whole-unit Anti-rust Passivation
Jaw working-surfaces receive local surface-hardening treatment; full-vise passivation anti-corrosion finish adapts dielectric-fluid-splashing tank-working environments.
6. Flexible Custom-built Realization
As contract manufacturer, JWGRIP supports custom-built modification for rotary-indexing resolution, jaw-clamping stroke and bottom-mounting-interface according to special fixture-cell process-development requirements.
7. Whole-unit Serial-number Traceability
Every finished JWGRIP 0-100mm Rotatable Wire EDM Vise carries laser-etched unique serial number. Complete inspection records covering angular repeatability, locking-rigidity and datum-flatness are archived for laboratory-asset-management purposes.
Operation Norms
1. Before mounting JWGRIP 0-100mm Rotatable Wire EDM Vise onto wire-EDM worktable, fully clean machine-table datum-plane and vise-base bottom-datum; remove wire-cut sludge and chip residues. Foreign particles trapped between mating-surfaces cause vise-base tilt and undermine subsequent angular-datum reliability.
2. Tighten base-mounting bolts following recommended torque-value. Excessive torque triggers base-body micro-warping; insufficient torque creates potential vise-shift risk under clamping reaction-force.
3. Release multi-point locking unit; rotate platform to target-angle position and engage multi-point circumferential locking module. After locking completes, perform probe-based angle-verification before clamping workpieces. Visual scale reading is auxiliary reference and cannot replace probe-measurement.
4. Clamp work-pieces inside jaw operating range; avoid workpiece overhang beyond allowable jaw span. Do not apply excessive jaw-clamping torque, which will generate invisible platform micro-distortion.
5. Prior to formal prototype-part wire-cut, run angular-repeatability test through multiple unlock-rotate-re-lock cycles.
6. After tank-production completes: release locking mechanism, purge labyrinth-barrier groove with dry compressed-air, clean jaw-surfaces, fully dry all mating-surfaces before storing inside tool-case.
FAQ
Q1: Does JWGRIP 0-100mm Rotatable Wire EDM Vise fully eliminate probe-angle-verification procedures?
A: It supplies repeatable mechanical angular indexing and locking datum. Visual scale reading serves only as auxiliary reference. Probe-based angle fine-verification and compensation cannot be skipped for formal prototype-part wire-cut processing, to offset jaw-wear, mounting-deviation and tiny rotary-pair clearance error.
Q2: Is clamping allowed for heavy work-pieces with large overhang beyond jaw effective span?
A: Excessive workpiece overhang brings extra moment-load onto rotary-platform and triggers invisible micro-distortion, degrading angular accuracy. Main clamping zone of workpiece must stay within 0-100 mm jaw effective clamping span. Auxiliary external supporting structures shall be configured for special overhang-part tasks.
Q3: My project requires non-standard rotary resolution or special bottom-mounting-interface, can you deliver custom-built solution?
A: Yes. Please submit complete technical-drawings with clear requirements for rotary-indexing resolution, jaw-clamping span, mounting-interface dimension and tolerance specs. Our engineering-department will finish manufacturability assessment and issue formal quotation feedback within 12 working-days.
Q4: Which failure conditions fall under product-warranty scope?
A: JWGRIP 0-100mm Rotatable Wire EDM Vise is high-precision
submerged-tank rotary work-holding fixture. Warranty covers manufacturing-origin defects upon delivery such as out-of-spec angular-repeat-accuracy and datum-flatness non-conformity. Damages from heavy-impact collision, over-range clamping torque, sludge-erosion without maintenance and normal cyclic-usage-wear are excluded from warranty terms.
Hot Tags: 0-100mm Rotatable Wire EDM Vise, China, Manufacturer, Supplier, Factory
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.