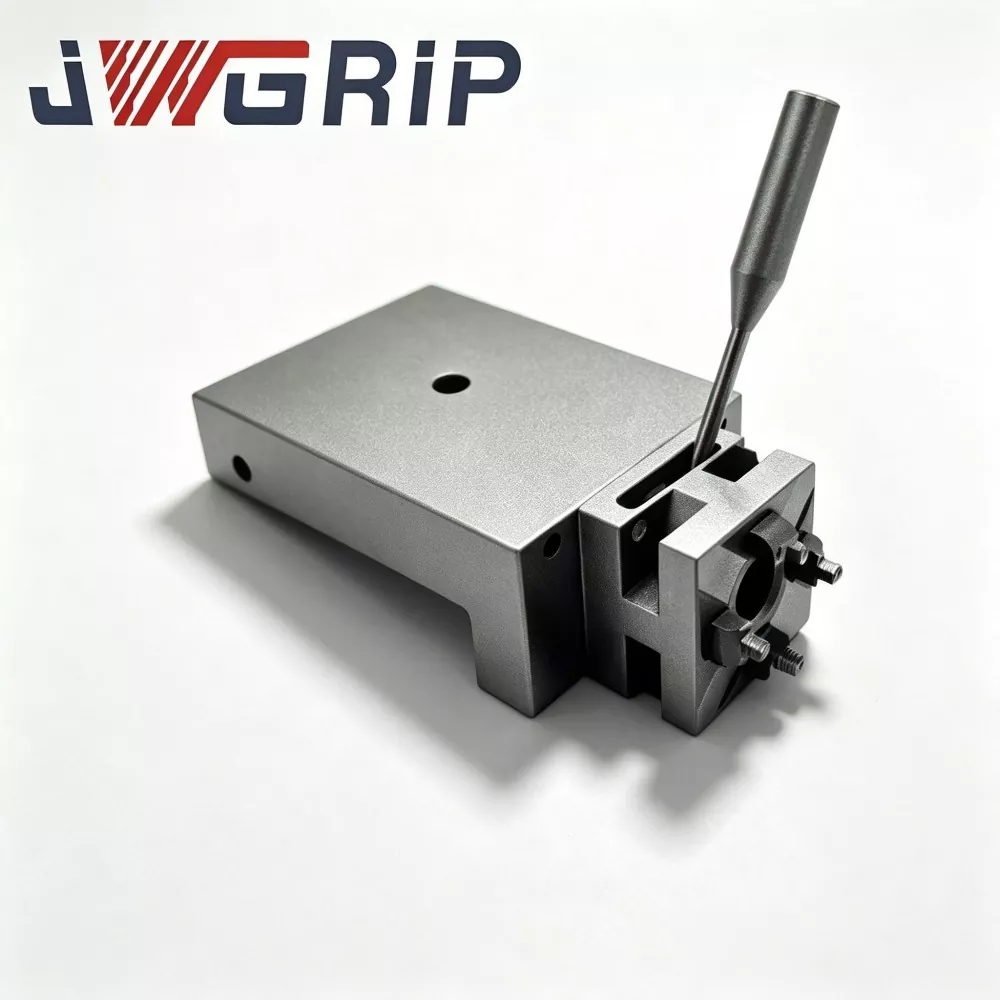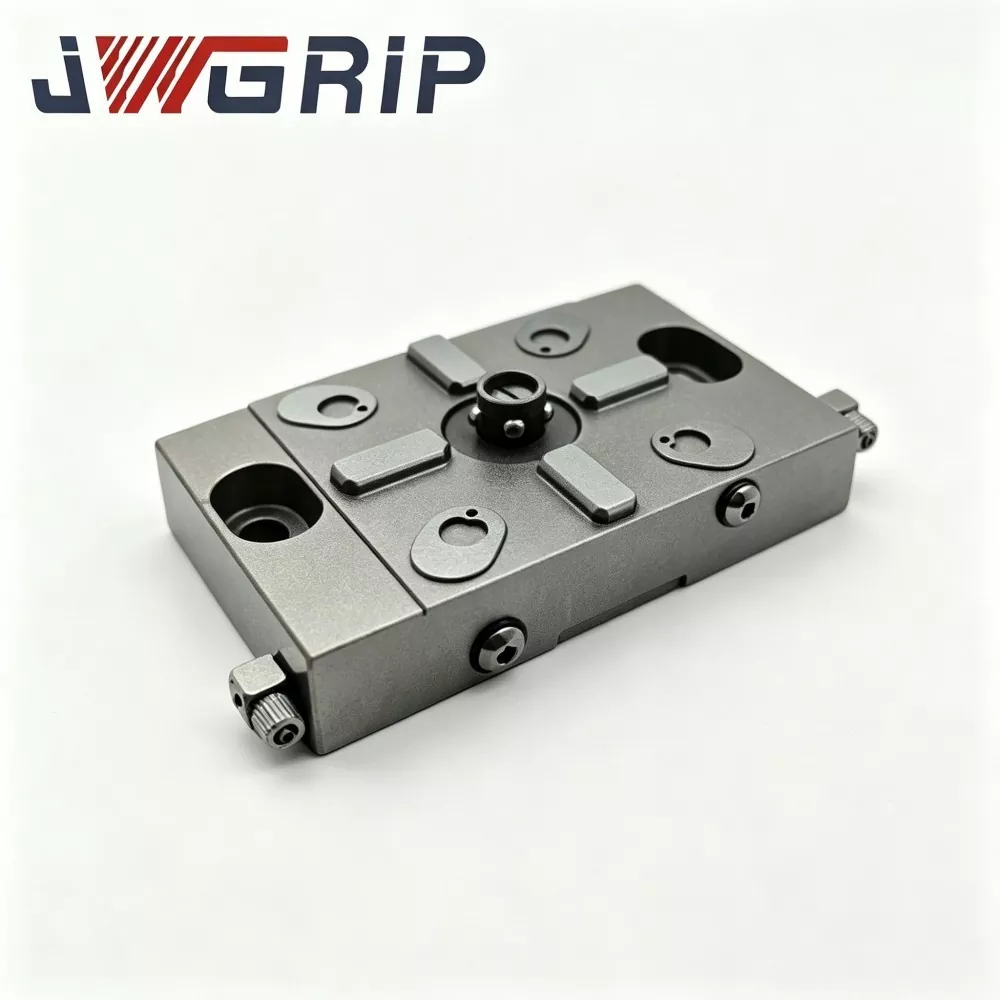
Pneumatic Chuck for Wire EDM Workholding
JWGRIP is the professional manufacturer and supplier of Pneumatic Chuck for Wire EDM Workholding in China, providing Factory Direct supply and Customized OEM structural modification for global automated submerged wire-cut production lines. It is a professional anti-corrosion integrated pneumatic clamping fixture specially designed for fully submerged wire EDM unmanned machining scenarios. It integrates exclusive air-channel anti-contamination structure and high-stability pneumatic locking performance into a single device, eliminating the common defects of ordinary dry-type pneumatic chucks such as fluid infiltration, piston jamming and clamping force attenuation in underwater environments.
This high-reliability Wire EDM Pneumatic Chuck is constructed from premium cryogenically treated pre-hardened alloy steel, with optimized internal air-channel anti-contamination architecture and professional sealing protection structure. Through strict submerged pollution aging simulation testing, it effectively resists dielectric fluid penetration, wire-cut sludge accumulation and internal component corrosion during long-term fully submerged operation. Pneumatic Chuck for Wire EDM Workholding maintains steady and consistent clamping force output in continuous automatic clamping and releasing cycles, avoiding positioning drift and machining instability caused by medium erosion and environmental corrosion.
Different from ordinary general-purpose pneumatic chucks that are only suitable for dry working conditions and prone to early failure underwater, it greatly reduces equipment maintenance frequency and batch workpiece scrap risks. It significantly cuts repetitive manual clamping operations, improves repeat positioning accuracy and unmanned production continuity. Widely applicable to automated wire-cut precision mold and tool blank batch processing, it supports standard mass supply and personalized OEM adjustment of air-port layout, jaw stroke and mounting interface, delivering high-efficiency and long-service-life workholding solutions for modern lights-out wire EDM workshops.
Failure Risks
Automated lights-out wire-EDM production raises throughput for mold-and-tool factories. Even so, pneumatic clamping units installed inside dielectric-fluid tanks bring a set of easily-overlooked hidden failure risks.
· Most off-the-shelf general-purpose pneumatic chucks are originally designed for dry-environment automation equipment. When deployed inside submerged wire-EDM tanks, fine wire-cut sludge and dielectric fluid seep into inner piston chambers through tiny clearance gaps.
· Contaminants build-up around seal rings and moving-piston surfaces. After hundreds of auto clamp-release cycles, sealing performance slowly degrades and clamping-force drifts without early warning signals.
· For high-precision stamping-die inserts with ±0.004 mm tolerance, invisible clamping-force attenuation induces micro-shift during wire-cut processing and leads to batch-part scrap. Many mold-shop technicians report such intermittent faults are hard to reproduce during offline inspection and increase troubleshooting difficulty.
Clamping solution
JWGRIP Pneumatic Chuck for Wire EDM Workholding is purpose-built to solve clamping-failure pain-points caused by medium contamination for automatic wire-EDM workholding.
Different from general-automation pneumatic chucks only validated via dry-bench lab tests, our R&D team collects massive real-world field-failure case data. Every generation of prototype passes simulated submerged-pollution aging testing before mass-production launch.
① Operators may mount this chuck onto wire-EDM machine worktables or custom fixture bases. Standard jaw-stroke fits mainstream small-medium precision-blank dimensions.
② Beyond standard versions, JWGRIP OEM service implements structural adjustments for retrofitting special automated wire-EDM fixture-cell projects.
Working principle
JWGRIP Pneumatic Chuck for Wire EDM Workholding is air-actuated automatic clamping fixture dedicated for submerged wire-EDM workstations. Clean dry compressed air enters internal sealed piston cavity through reserved air-ports, pushing piston assemblies to drive wedge-cam linkage mechanism and achieve synchronous inward-clamping / outward-releasing of movable jaws.
Its core differentiated design is built-in labyrinth-type anti-infiltration structure surrounding piston-shaft outlet. Multi-barrier channels block wire-cut sludge and dielectric fluid from invading air chambers.
Critical environmental difference note: conventional industrial pneumatic chucks work in dry atmosphere, while wire-EDM-special models endure continuous liquid splashing and partial immersion. If labyrinth barriers get clogged by debris, anti-pollution performance will decline. This chuck cannot replace compressed-air-source pretreatment. Moisture, oil mist and solid particles from air supply still accelerate wear of inner components.
Core Performance Characteristics
1. Multi-stage Labyrinth Anti-infiltration Architecture Comparative submerged-aging lab test shows: under identical splash-pollution cycles, JWGRIP pneumatic chuck cuts pollutant-invasion probability by approximately 36 % versus ordinary non-labyrinth pneumatic chucks. It effectively delays seal-ring failure triggered by dielectric-fluid sludge.
2. Cryogenically-stabilized Alloy-steel Main-body After rough-machining, main-body undergoes cryogenic treatment plus multi-round stress-relief tempering. Within workshop temperature range 15-32 ℃, main-body structural-dimension drift ≤0.0029 mm, restraining thermal-deformation influence over clamping-force output.
3. Plasma-nitrided Cam-wedge Moving Components Cam and wedge-linkage key components adopt plasma nitriding hardening, surface hardness reaches HV830-940, improving wear-resistance under particle-contaminated submerged environments.
4. Integrated Air-port Pre-filter Mounting Interface Reserved threaded port allows installing miniature near-chuck air-filter cartridge, performing secondary purification for compressed-air before medium flows into inner cavity.
5. Jaw Parallelism Assurance Movable-jaw mating surfaces receive ultra-precision grinding. Jaw parallelism under rated air-pressure ≤0.0035 mm, securing consistent clamping condition for small-size precision blanks.
6. Standard Specs plus Flexible OEM Realization Standard jaw-stroke and mounting dimensions match mainstream wire-EDM automation-fixture layout. JWGRIP can modify air-port arrangement, jaw travel, mounting-interface and sealing-material grade per customer drawings for special automated wire-EDM-cell projects.
7. Full-lot Traceable Quality Archive Each finished JWGRIP chuck carries laser-etched unique serial number. Complete test datasets including jaw parallelism, clamping-force output curve and submerged-simulation aging-test records are archived for enterprise-level quality traceability.
Complete Manufacturing Workflow
1. Incoming raw-material composition & hardness inspection
2. CNC rough-milling for main-body and labyrinth-groove
3. Cryogenic stabilization treatment
4. Multi-step stress-relief tempering
5. Semi-finish machining
6. Cam-wedge component forming
7. Plasma nitriding hardening for moving parts
8. Ultra-precision grinding for jaw-mating surfaces
9. Air-port & auxiliary-thread-interface finishing
10. Seal-groove precision-machining
11. Manual assembly with certified sealing components
12. Airtightness inspection
13. Jaw-parallelism measurement
14. Rated-pressure clamping-force-curve acquisition
15. Simulated submerged-splash pollution aging test
16. Laser serial-number marking
17. Overall anti-rust passivation
18. Final comprehensive recheck
19. Finished-product warehousing
JWGRIP factory follows ISO 9001 quality-management-system standards. Core measuring instruments including clamping-force test-bench, air-leak detector and coordinate-measuring-machine receive regular metrological calibration. Each finished chuck comes with independent inspection report. For OEM orders, material certificates and partial third-party test records are available upon client request.
Quality Specification
Each production batch of JWGRIP Pneumatic Chuck undergoes multi-dimensional quality validation:
① Raw-material inspection, hardness spot-check
② Main-body geometric-dimension detection
③ Post-assembly airtightness test
④ Jaw-parallelism measurement
⑤ Clamping-force-output-curve acquisition
⑥ Simulated submerged-splash pollution aging test
⑦ Surface anti-corrosion inspection
All measuring devices stay under valid calibration cycle. Batch inspection reports are archived for traceability. For OEM modified chucks, additional customized-feature inspection items will be supplemented in accordance with customer drawing requirements before shipment.
Core Advantage
Most commercially-available automation-oriented pneumatic chucks adopt simple sealing construction without labyrinth anti-infiltration channels. Many manufacturers cut costs by omitting cryogenic-stabilization and plasma-nitriding procedures.
1. Anti-pollution performance: Ordinary chucks without labyrinth grooves allow pollutants to easily invade inner-cavity under submerged splash conditions; sealing parts fail within short cycles. JWGRIP multi-stage labyrinth layout slows sludge invasion and prolongs sealing-kit service life.
2. Thermal-stability performance: Many competing products skip cryogenic treatment; residual-stress releases with tank-temperature fluctuation and triggers dimension-drift which disturbs clamping-force. JWGRIP cryogenically-stabilized main-body controls thermal-deformation magnitude.
3. Moving-part wear-resistance: Competitors’ cam-wedge components only receive ordinary quenching and wear quickly under particle-polluted environments. JWGRIP plasma-nitrided key moving-parts deliver outstanding surface hardness and wear-resistance.
4. Test-coverage difference: Many suppliers only perform static airtightness inspection. Every JWGRIP finished chuck passes simulated submerged-splash aging test plus clamping-force-curve recording. Custom-OEM orders also get dedicated-feature validation.
5. Customization capacity: Plenty factories can only supply fixed-standard-size chucks. With mature OEM workflow, JWGRIP adjusts air-port layout, jaw-stroke and mounting-interface for special-purpose automated wire-EDM-cell projects.
Packaging & Shipment
Each qualified JWGRIP Pneumatic Chuck is fully cleaned, air-blown dry and coated with anti-rust protective oil, then placed inside moisture-proof shock-proof heavy-duty tool case. Outer carton is foam-filled for ocean or air international freight.
As OEM-capable manufacturer, JWGRIP cooperates with trusted international freight forwarders. Packing list plus copy of single-unit inspection report can either be enclosed inside cargo package or issued as PDF digital documents.
FAQ
Q1: Does labyrinth-structure realize 100 % zero-infiltration for wire-cut sludge and dielectric fluid?
A: JWGRIP multi-stage labyrinth-groove greatly lowers pollutant-infiltration risk, yet absolute zero-penetration cannot be guaranteed under extreme heavy-sludge impact. Operators must maintain qualified compressed-air source and execute periodic labyrinth-channel purging maintenance. Regular inspection cannot be omitted for unattended lights-out production.
Q2: Can this chuck work without air-dryer and air-filter unit?
A: Not recommended. Even with near-chuck auxiliary filter thread interface, water-vapor and oil-mist from upstream air-supply accelerate seal-ring aging. Complete air-treatment assembly (dryer + filter) is mandatory for long-term submerged wire-EDM automatic operation.
Q3: If non-standard air-port layout, special jaw-stroke and modified mounting-interface are needed, can you deliver OEM production?
A: Yes. Please submit complete technical drawings with clear requirements covering air-port arrangement, jaw travel, mounting-interface dimension and tolerances. Our engineering team will finish manufacturability assessment and issue formal quotation feedback within 12 working-days.
Q4: What failure modes fall under product-warranty scope?
A: JWGRIP Pneumatic Chuck for Wire EDM Workholding belongs to high-precision submerged automatic workholding component. Warranty covers manufacturing-origin defects upon delivery such as out-of-spec jaw parallelism, unqualified airtightness and non-conforming main-body dimension. Damages caused by contaminated air-source, over-rated air-pressure, sludge-impact pollution and normal fatigue-wear of sealing parts are excluded from warranty terms.
Hot Tags: Pneumatic Chuck for Wire EDM Workholding, China, Manufacturer, Supplier, Factory
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.