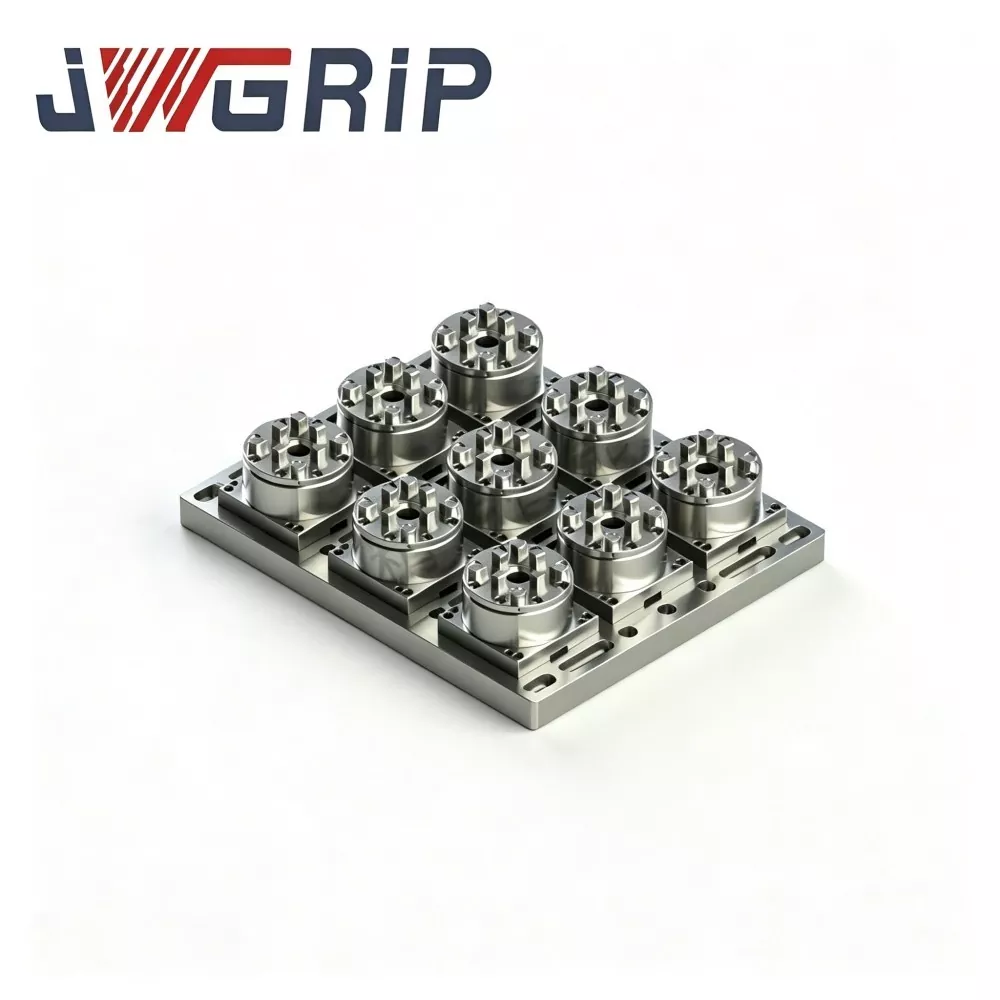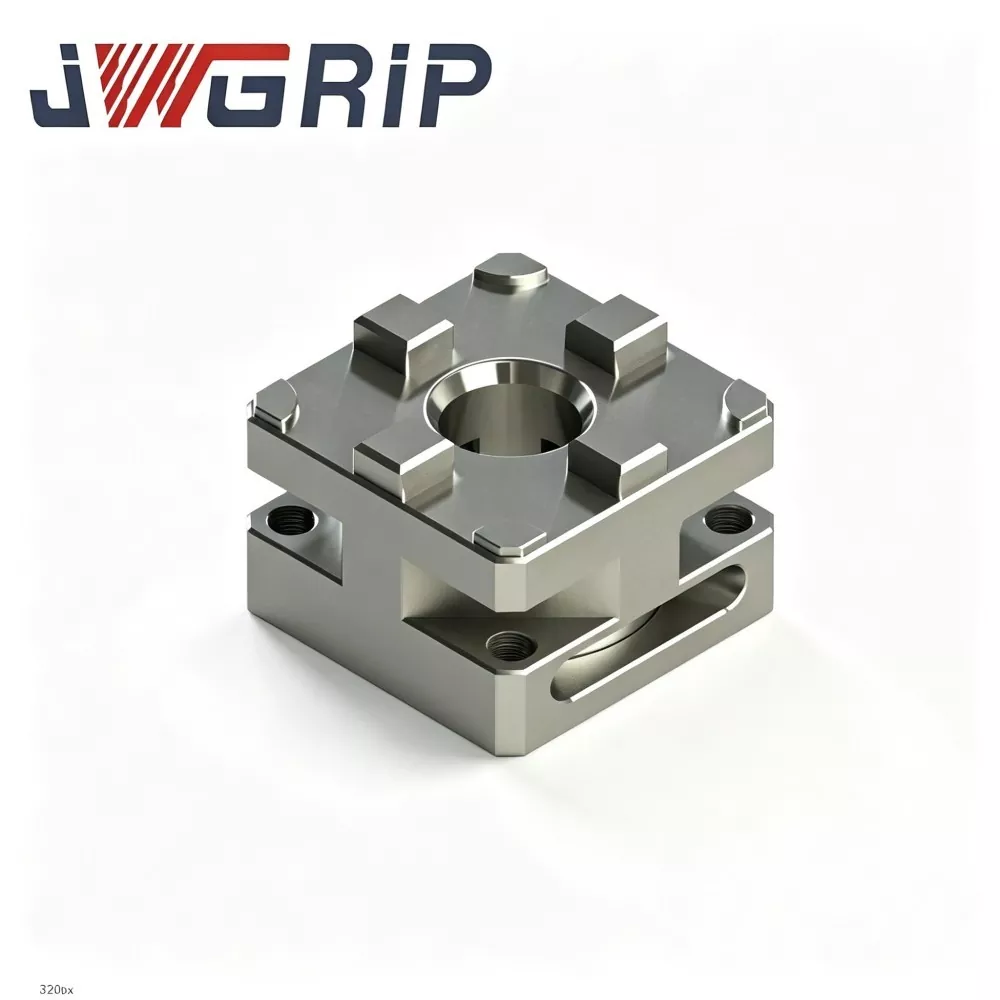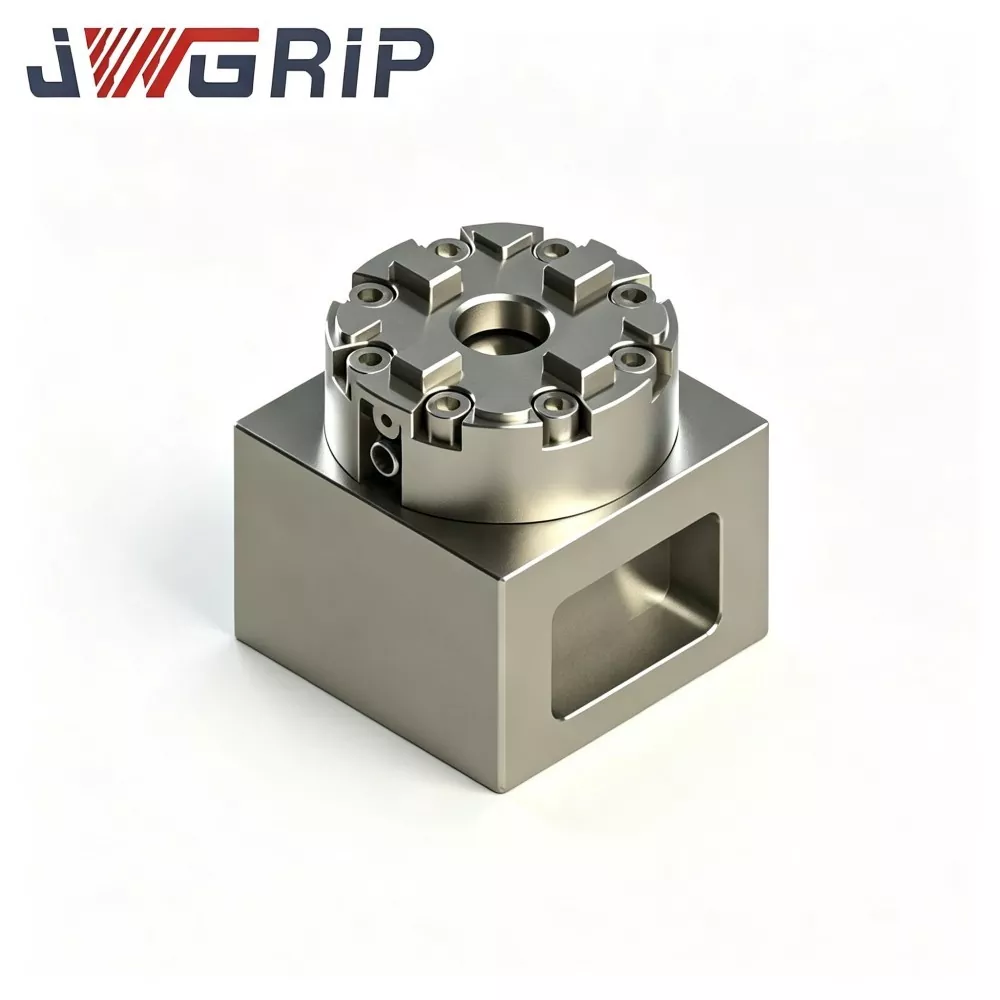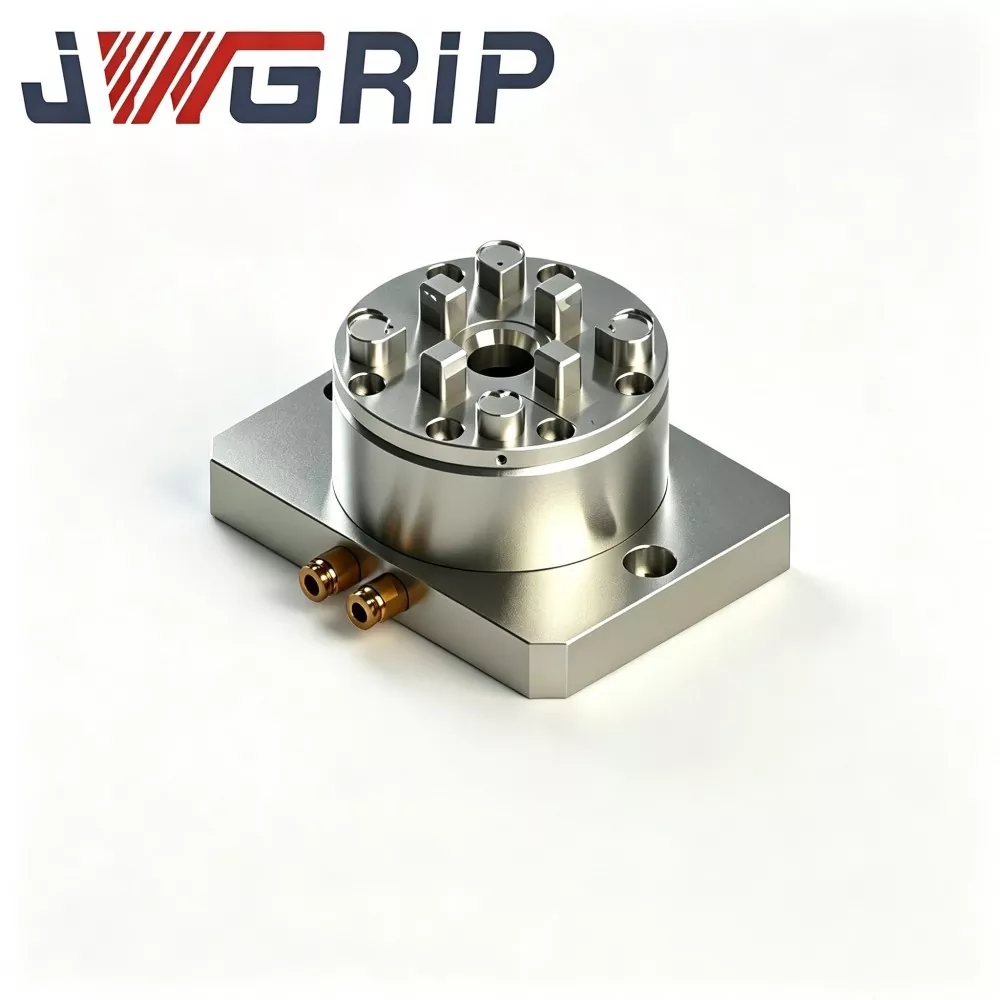
R-Type D150 Pneumatic EDM Chuck
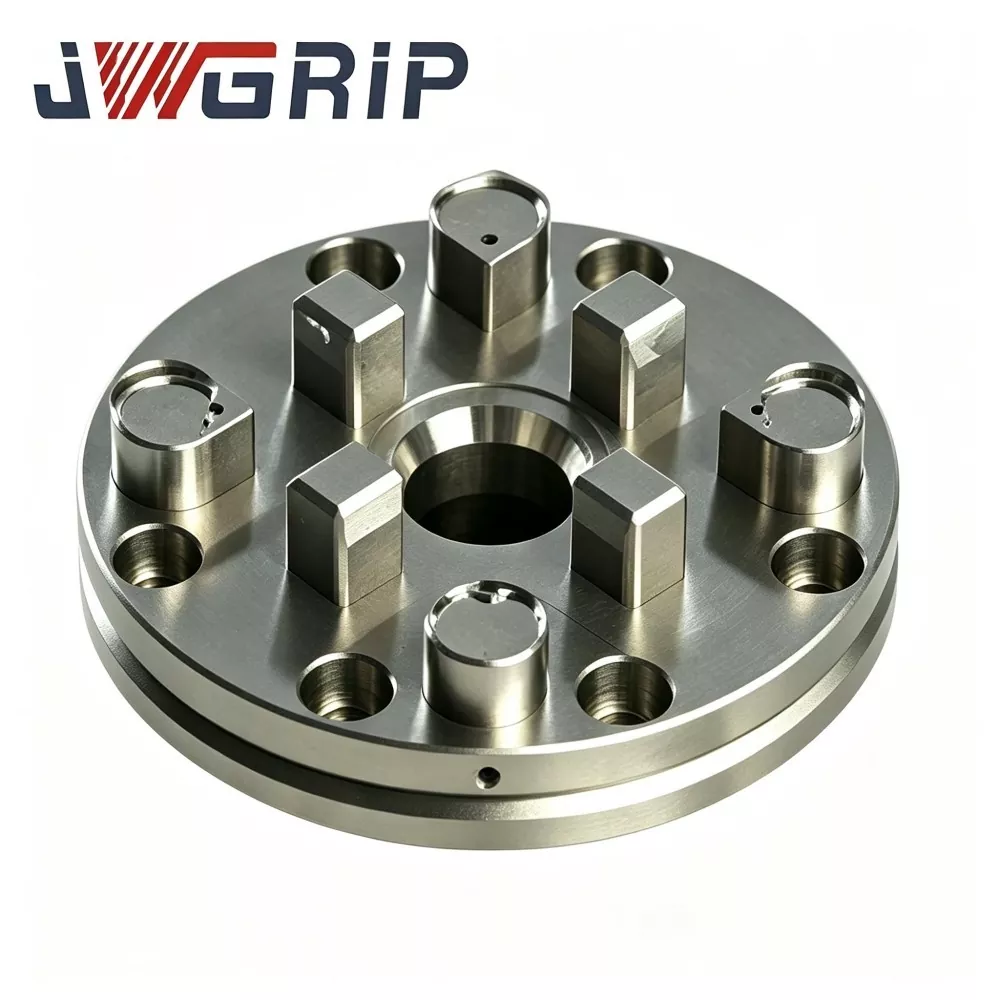
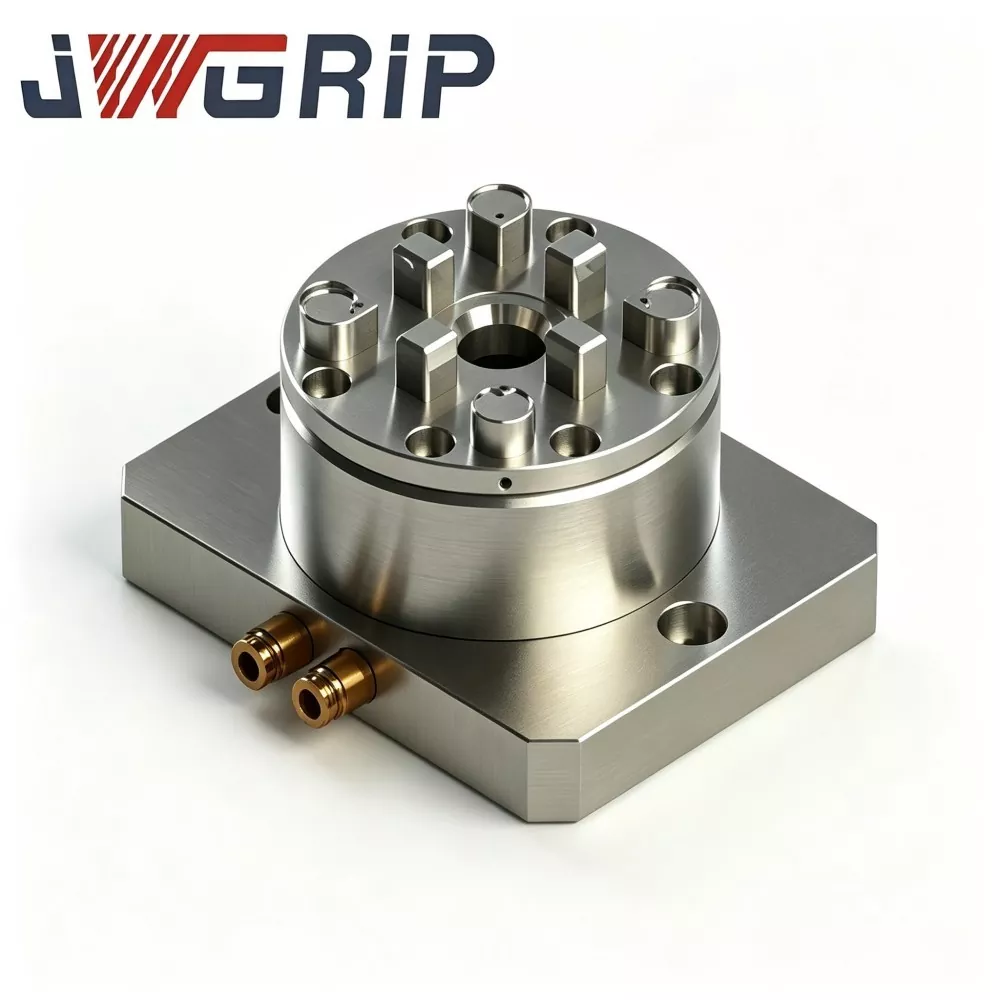
JWGRIP is the Professional manufacturer and supplier of R-Type D150 Pneumatic EDM Chuck in China, with standard specifications fully in Stock to support global framework agreement cooperation and consignment order deployment. It is a high-efficiency integrated pneumatic clamping fixture professionally customized and developed for die-sinker EDM, wire-cut EDM and precision mold electrode machining scenarios. It integrates optimized internal air circuit structure and high-precision positioning clamping unit into a single device, eliminating tedious manual alignment and repeated calibration procedures required by traditional fixtures.
This high-performance R-Type D150 Pneumatic EDM Chuck is made of high-grade quenched alloy steel, featuring ultra-stable clamping force, excellent concentricity and outstanding long-term anti-fatigue performance under continuous pneumatic cycling. Core positioning reference surfaces adopt one-time clamping integral machining technology, and key matching components are precisely ground after quenching treatment to ensure consistent fitting clearance and assembly accuracy. The optimized internal air circuit effectively reduces pressure loss during repeated pneumatic actions, maintaining stable clamping status for long-term continuous cyclic operation and avoiding clamping force fluctuation and concentricity drift.
R-Type D150 Pneumatic EDM Chuck supports offline presetting and rapid replacement of electrodes, greatly cutting auxiliary debugging time and reducing manual positioning deviation. It can also be connected with automatic robot handling modules to realize unmanned electrode swapping. Widely applicable to precision mold EDM processing, it provides reliable high-precision clamping solutions for mold manufacturers, EDM processing subcontractors and automated production enterprises.
Clamping Solution
In real-world mold-making workshops, electrode clamping is a major bottleneck restricting EDM processing efficiency:
· Conventional manual fixtures require repeated clamping, dial-gauge alignment and position calibration for every electrode replacement. Auxiliary time cost is high, and positioning accuracy depends heavily on on-site operator experience.
· For complex molds requiring continuous swap of multiple electrode groups, frequent re-setup significantly extends overall production lead-time.
· Many commercial low-cost pneumatic chucks generate pressure fluctuation after thousands of cycles. Clamping force and concentricity drift will damage final mold cavity surface forming quality.
JWGRIP optimizes product structure to tackle above-mentioned issues:
1. Core positioning reference surfaces adopt one-clamping complete-machining process. After quenching treatment, critical matching parts go through precision grinding to guarantee consistent fitting clearance.
2. Optimized inner air-circuit reduces pressure loss during repeated pneumatic actuation, maintaining stable clamping state for long-duration cyclic work.
3. Offline electrode presetting is supported. Operators finish electrode installation and debugging outside EDM equipment. Rapid swap after docking avoids positioning error from repeated manual adjustment.
4. Compatible with robot automatic loading-unloading modules to realize unmanned electrode changeover, supplying reliable high-precision clamping for die-sinker EDM, wire-cut EDM and mass mold-electrode processing.
Internal Architecture
JWGRIP R-Type D150 Pneumatic EDM Chuck applies built-in closed air-driven wedge-type clamping architecture:
1. Workshop compressed air flows into inner air chamber through side-mounted air inlet port. Air pressure pushes wedge sliding block and creates radial driving force to drive multiple clamping jaws for centering clamping towards central datum.
2. When air supply is released, built-in return spring pushes wedge block backward, clamping jaws open for electrode shank or fixture disassembly.
Key structural design highlights:
· All core locating datum surfaces are finished via one-time high-precision grinding, minimizing accumulated assembly tolerance.
· Air channels are integrated inside chuck main-body instead of exposed external pipelines, preventing collision damage under EDM oil-immersed environment.
· Reinforced inner ribs spread clamping stress evenly across chuck shell to avoid local stress concentration under long-term cyclic clamping. Stable concentricity and clamping performance hold true for both framework-agreement batch-use sites and consignment-order end-user workshops.
· Internal sealing components adopt special oil-resistant rubber material, custom-made for dielectric oil bath working conditions to slow sealing aging during continuous spark-erosion machining.
Core Technical Performance
1. Superior Centering & Repeat-Positioning Capability Key locating surfaces go through multi-pass precision grinding. Concentricity ≤0.003 mm and repeat positioning accuracy ≤0.005 mm. No accumulated positioning deviation even after thousands-time continuous clamping cycles, satisfying strict tolerance requirements for complex multi-cavity mold electrode machining.
2. High-grade Anti-fatigue Alloy-steel Main-body Main-body adopts premium 40CrNiMo alloy steel with integral quenching & tempering heat-treatment, surface hardness HRC 52-56. Great anti-impact, anti-deformation and oil-corrosion-resistant performance fits long-term cyclic clamping under EDM dielectric-oil immersion. Widely trusted among high-end mold-making enterprises.
3. Significant Pneumatic Quick-swap Productivity Gain After one-time datum calibration on EDM machine table, electrode-holder replacement only costs 5-10 seconds by manipulating pneumatic control valve. Manual screw tightening and repeated dial-gauge tramming are eliminated. Non-cutting auxiliary time drops sharply, lifting EDM machine utilization for multi-variety small-batch mold orders and large-scale electrode processing projects.
4. Full Adaptability to Oil-immersed EDM Working Scenario Optimized custom oil-resistant sealing assembly is specially designed for spark-erosion dielectric oil environment. Concealed integrated air-circuit avoids pipeline damage caused by electrode collision or mold-part handling. Stable long-time oil-soaked operation without frequent maintenance for air-pipe joints.
5. Complete Industrial Compliance & Batch Inspection Each production batch undertakes dimension check, concentricity test, cyclic clamping fatigue test and air-tightness inspection. CE and ISO9001 test documents can be supplied for enterprise clients signing framework-agreement centralized procurement contracts.
Assessment Checklist
Complete following pre-assessment before purchasing JWGRIP R-Type D150 Pneumatic EDM Chuck to prevent on-site application obstacles:
1. Confirm installation available space of EDM machine work-table. Measure vertical & horizontal reserved space to avoid mechanical interference between chuck shell, spindle and moving axes.
2. Verify stable compressed-air supply. Working air pressure shall keep stable within 0.4-0.6 MPa. Air source must be equipped with oil-water separator to filter moisture and impurities.
3. Check daily-processed electrode shank diameter range, ensure real electrode dimension falls within rated clamping scope of this chuck.
4. Pay attention to EDM dielectric-oil immersion depth. Air-inlet joint must stay above liquid level to prevent oil back-flow entering internal air-circuit.
5. For enterprise framework-agreement clients or consignment-order distributors, submit full on-site environment parameters and performance requirements in advance for correct product configuration matching.
Quality Inspection
All JWGRIP R-Type D150 Pneumatic EDM Chucks are manufactured and inspected inside our China-based fixture workshop following multi-phase standardized workflow:
1. Raw-material incoming inspection: 40CrNiMo alloy steel bar for chemical composition analysis and hardness test; full material certification attached. Disqualified raw materials get rejected directly.
2. Rough CNC machining: rough-process outer contour, inner wedge-block cavity, air-channel passages and pre-mount holes, leaving finishing allowance for all locating-related functional surfaces.
3. Quenching & tempering heat-treatment: precisely control heating, holding and cooling curve to achieve target hardness HRC 52-56 and release internal stress. This step is essential for anti-fatigue performance against long-term cyclic clamping force.
4. Fine CNC machining: machine central locating hole, wedge-block mating surfaces, air-inlet thread port and mounting holes. Key dimension tolerance controlled within ±0.006-0.010 mm.
5. Multi-run precision grinding for core locating datum planes to satisfy concentricity and flatness requirements.
6. Component assembly & air-circuit commissioning: install wedge-block group, return springs, special oil-resistant seals and clamping jaws. Repeated open-close cyclic test plus full air-tightness inspection remove assembly burrs and verify stable pneumatic driving.
7. Comprehensive final inspection: test dimension, hardness, concentricity, repeat-positioning accuracy, clamping-force stability and air-circuit leak-proof performance. Every unit obtains exclusive traceability serial number. Non-conforming goods go for rework instead of packaging.
8. Anti-rust cleaning, surface anti-corrosion treatment and shock-resistant plywood-case export-grade packaging.
Why Select Us As Your Partner
1. Real Factory Source JWGRIP is self-owned fixture manufacturer instead of pure trading middleman. Entire production for R-Type D150 Pneumatic EDM Chuck is completed in-house. Our mechanical engineering team owns more than 11-year experience in EDM workholding R&D and fully understands mold-making workshop practical pain-points.
2. Flexible Cooperation Modes plus OEM Customization OEM modification options include clamping-range adjustment, special interface conversion and client-brand logo marking. Small-lot trial purchase, customized OEM development, long-term enterprise framework-agreement and distributor consignment-order projects are all acceptable business patterns.
3. Transparent & Traceable Pricing We offer clear price lists according to product configuration, modification complexity and different cooperation types, without hidden extra costs emerging during project execution.
4. Complete Quality-guarantee Mechanism Each chuck carries unique traceability serial number. Two-year warranty covers manufacturing-caused defects under rated air-pressure and correct-installation conditions. Technical team supplies installation guidance document and common-fault troubleshooting tips. Worn sealing consumable parts are excluded from warranty coverage.
5. Reliable & Predictable Delivery Schedules Standard-spec products follow fixed production cycles. For framework-agreement batch delivery or consignment-order stocking demand, we provide periodic production progress feedback to guarantee stable supply rhythm.
FAQ
Q1: Are you manufacturer or trading supplier for R-Type D150 Pneumatic EDM Chuck?
A1: JWGRIP is genuine fixture manufacturer based in China. All production workflows are finished in-house. We provide OEM development, framework-agreement supporting service and consignment-order cooperation rather than working as simple middleman trader.
Q2: Can this pneumatic chuck sustain stable performance under long-term EDM dielectric-oil immersion?
A2: Standard unit adopts special oil-resistant sealing components designed for EDM oil-bath environment. Please strictly follow installation specification to prevent dielectric-oil back-flow into air-circuit for longer service lifespan.
Q3: What are concentricity and repeat-positioning accuracy of standard R-Type D150 Pneumatic EDM Chuck?
A3: Standard-product concentricity ≤0.003 mm, repeat positioning accuracy ≤0.005 mm. Higher-precision variants can be realized through OEM technical adjustment.
Q4: Which damages are excluded from warranty scope?
A4: Two-year warranty applies for manufacturing-caused defects under rated air-pressure and correct-installation. Damage induced by air-pressure overload, hard mechanical collision, sealing-part natural aging and improper manual maintenance is not covered.
Q5: Can I obtain official price-list documents?
A5: Yes. Please contact JWGRIP sales department. We prepare formal price-list based on product configuration, purchasing volume and cooperation modes including framework-agreement or consignment-order projects.
Hot Tags: R-Type D150 Pneumatic EDM Chuck, Supplier, Manufacturer, Factory
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.