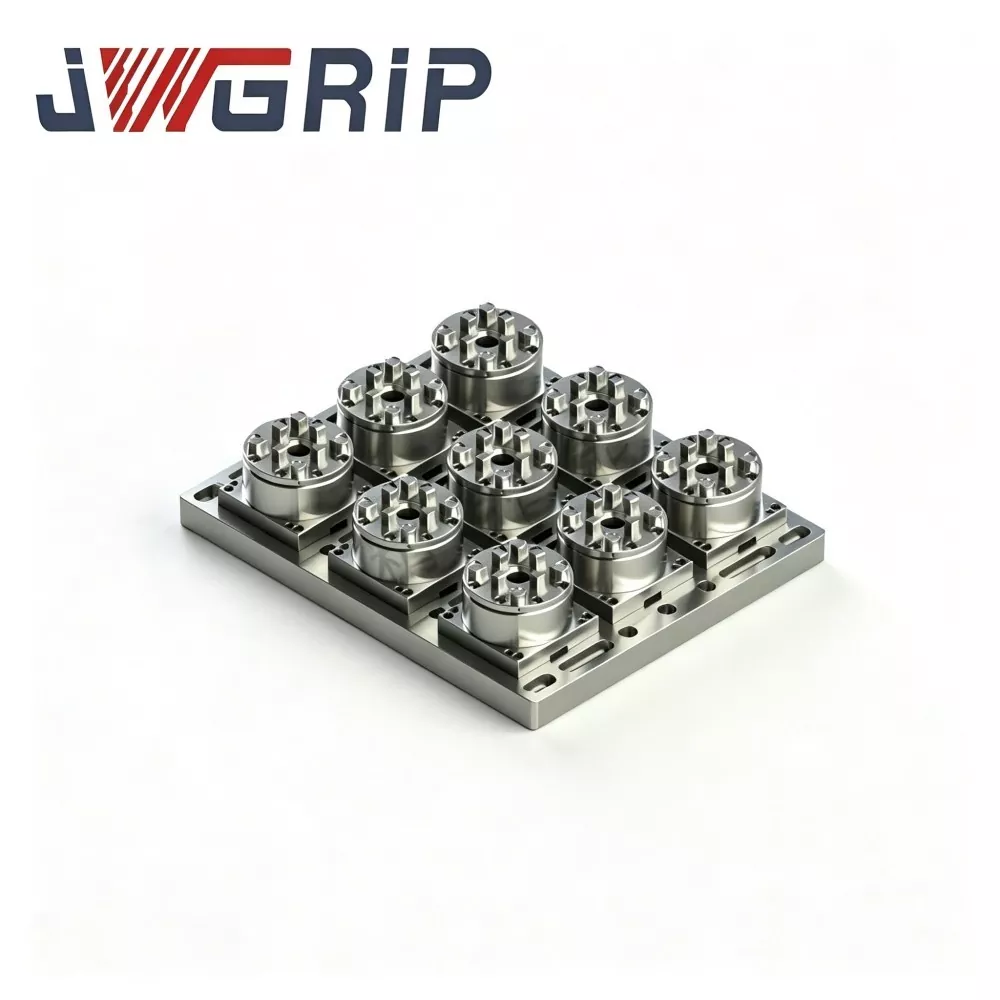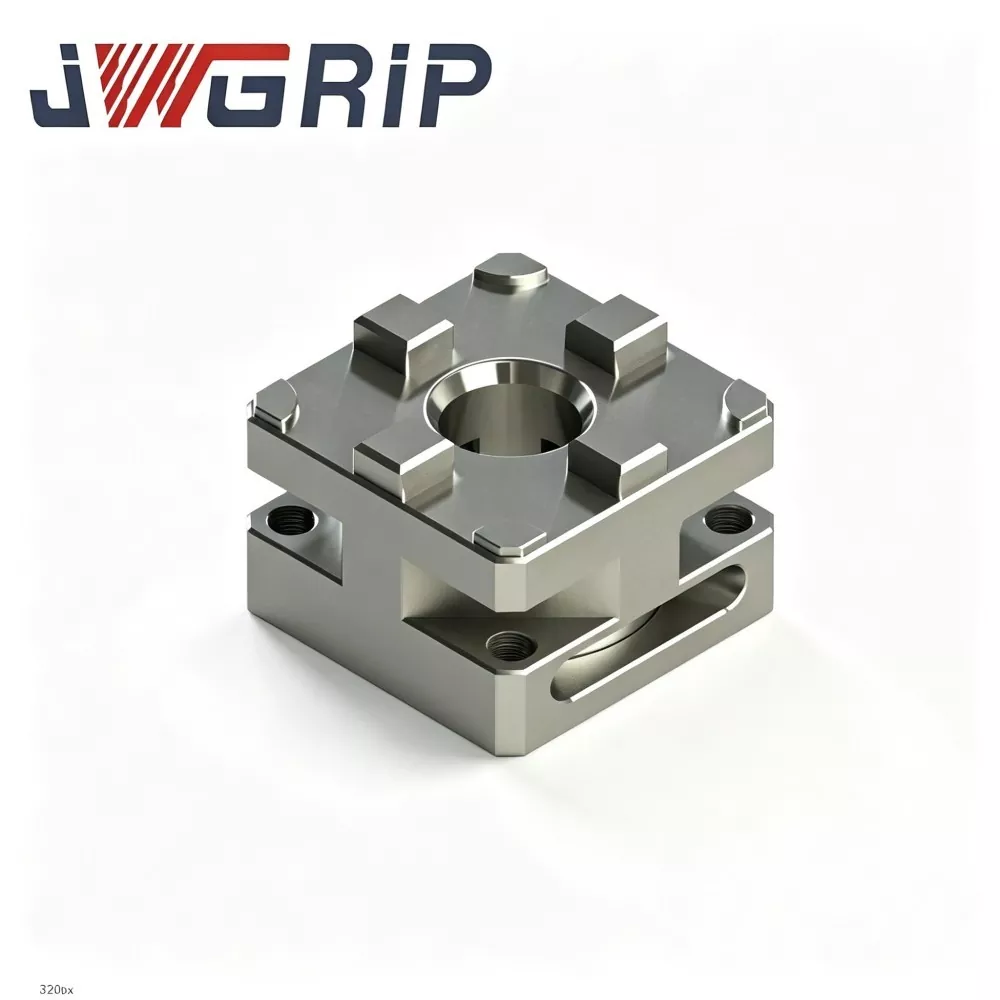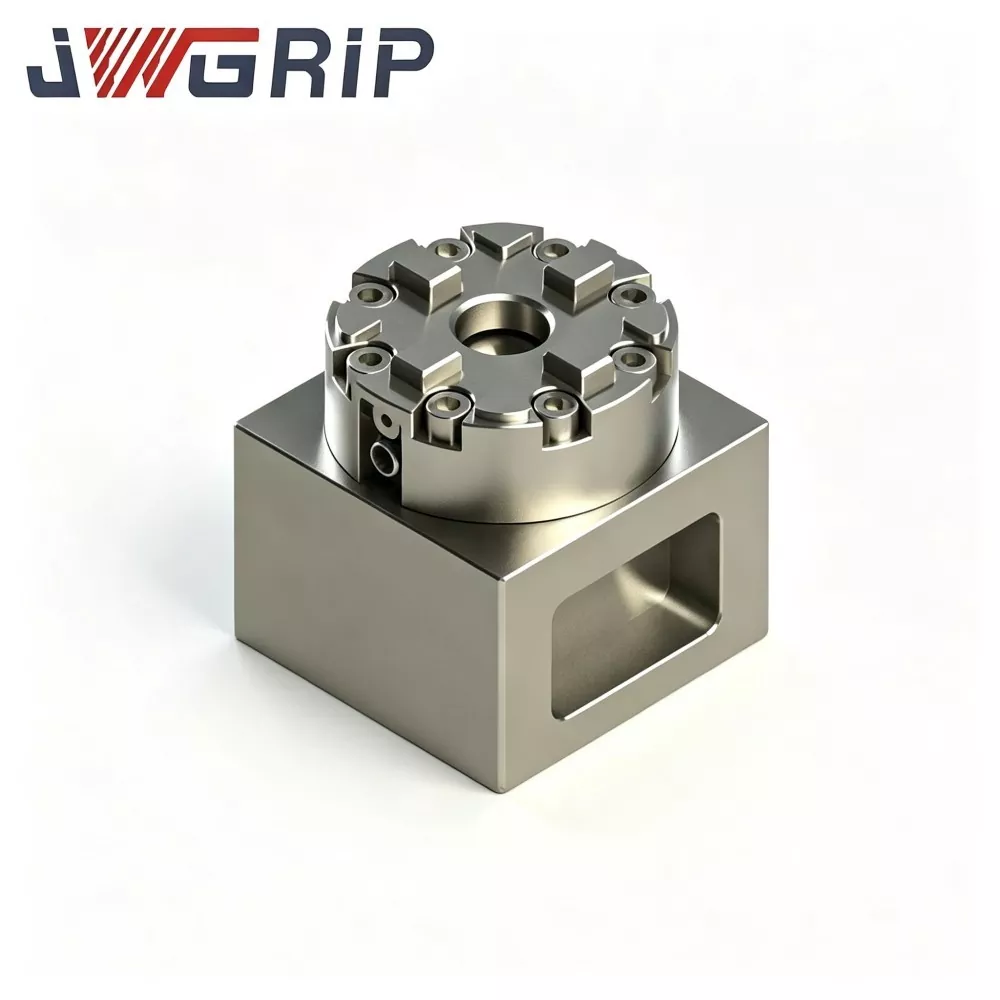
R-Type D75 MacroStd CNC Manual EDM Chuck
JWGRIP is the professional manufacturer and supplier of Customized R-Type D75 MacroStd CNC Manual EDM Chuck in China, providing Factory Direct supply to support global volume bidding projects and spot consignment business. It is a high-precision integrated manual clamping fixture complying with MacroStd dimensional standards, specially engineered for sinker EDM, wire-cut EDM and professional mold electrode manufacturing workshops. Integrating anti-corrosion hardened steel structure and unified precision positioning benchmark into a single compact unit, it eliminates tedious repeated dial indicator calibration and cumulative positioning errors of traditional clamping tools.
This high-performance R-Type D75 MacroStd CNC Manual EDM Chuck adopts fully hardened anti-corrosion alloy steel material, featuring stable mechanical clamping force, ultra-low concentricity deviation and excellent long-term wear resistance under frequent manual locking cycles. All key clamping reference surfaces are processed by ultra-precision machining technology to ensure consistent positioning accuracy in long-term cyclic clamping operations.
Different from ordinary manual chucks with easy precision attenuation, it effectively avoids electrode offset and mold cavity texture unevenness caused by accuracy drift. It greatly reduces non-processing auxiliary calibration time, optimizes electrode replacement efficiency, and stabilizes the overall production rhythm of mold workshops. With reliable and repeatable clamping performance, it is widely applicable for small and medium batch mold processing, providing stable and high-precision manual clamping solutions for global mold manufacturers, EDM subcontractors and machine tool system integrators.
Addressing the pain points
Traditional screw-type manual clamping brings multiple headaches for mold electrode workshops:
· Simple screw-based clamping solutions force operators to spend massive time adjusting screw torque and correcting datum every time electrodes get swapped.
· Manual operation heavily depends on operator skill. Uneven tightening torque may trigger electrode slip, concentricity drift and unstable repeat accuracy, especially for mixed-variety small-batch electrode orders.
· Common low-cost manual chucks on market cannot sustain stable concentricity after long-time cyclic clamping. Minor electrode offset leads to uneven mold-cavity texture and finished-part rejects.
JWGRIP optimizes the R-Type D75 MacroStd manual chuck against above-mentioned pain-points:
1. Strict MacroStd standard locating-datum structure is adopted. After one-time datum calibration on EDM machine platform, electrode-holder locking and release can be finished with manual torque wrench, without repeated dial-gauge readjustment.
2. Cross-machine datum transfer is realized for electrodes and mold inserts, effectively cutting non-processing auxiliary time for EDM equipment.
3. Full-hardened anti-corrosion alloy-steel main-body plus ultra-precision-machined clamping reference surfaces eliminate cumulative positioning errors caused by repeated manual setup. Stable repeatable clamping accuracy is guaranteed for long-run small-and-medium-batch mold processing.
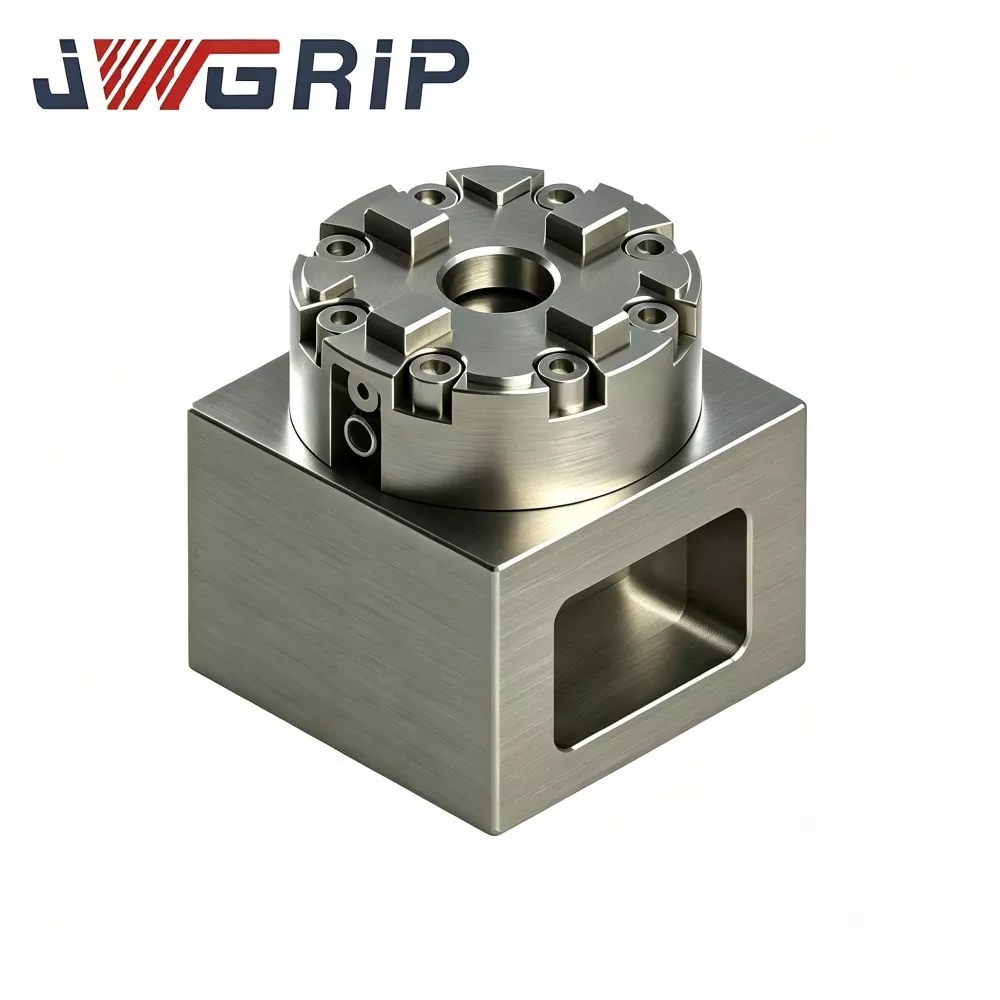
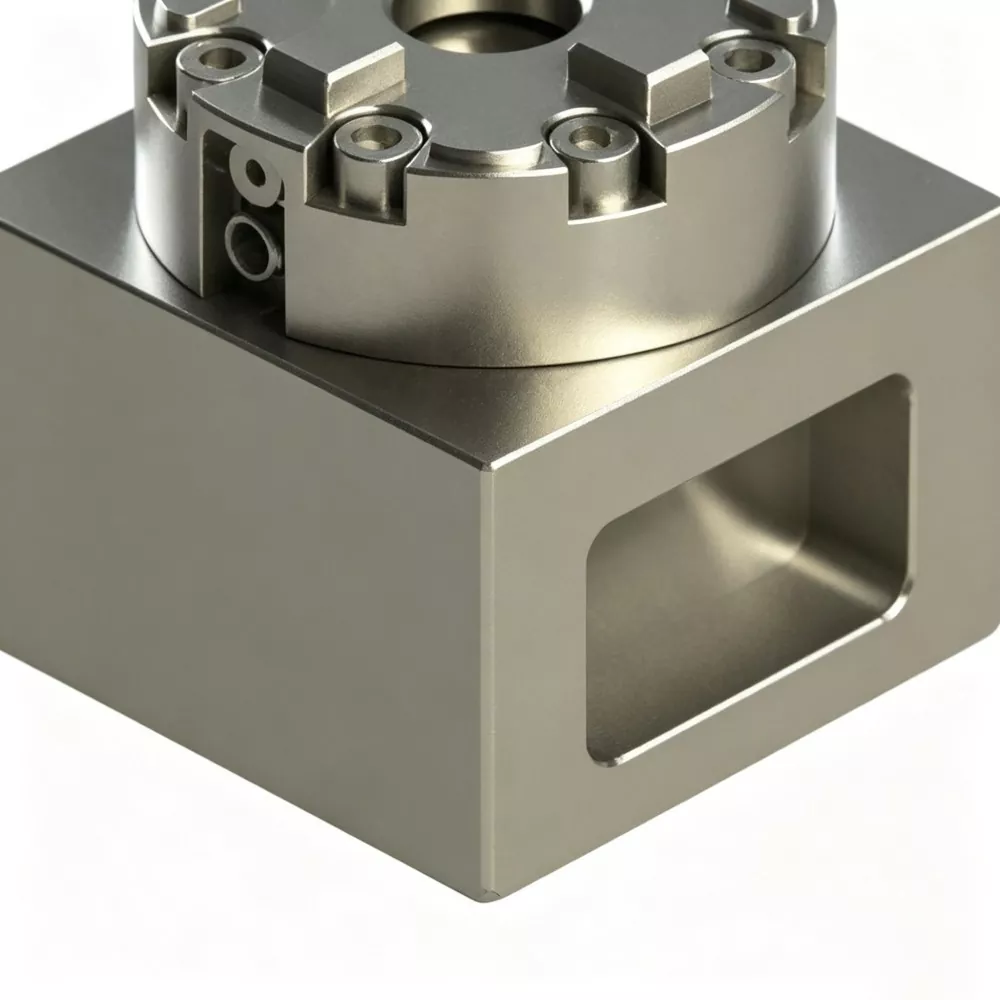
Working Logic
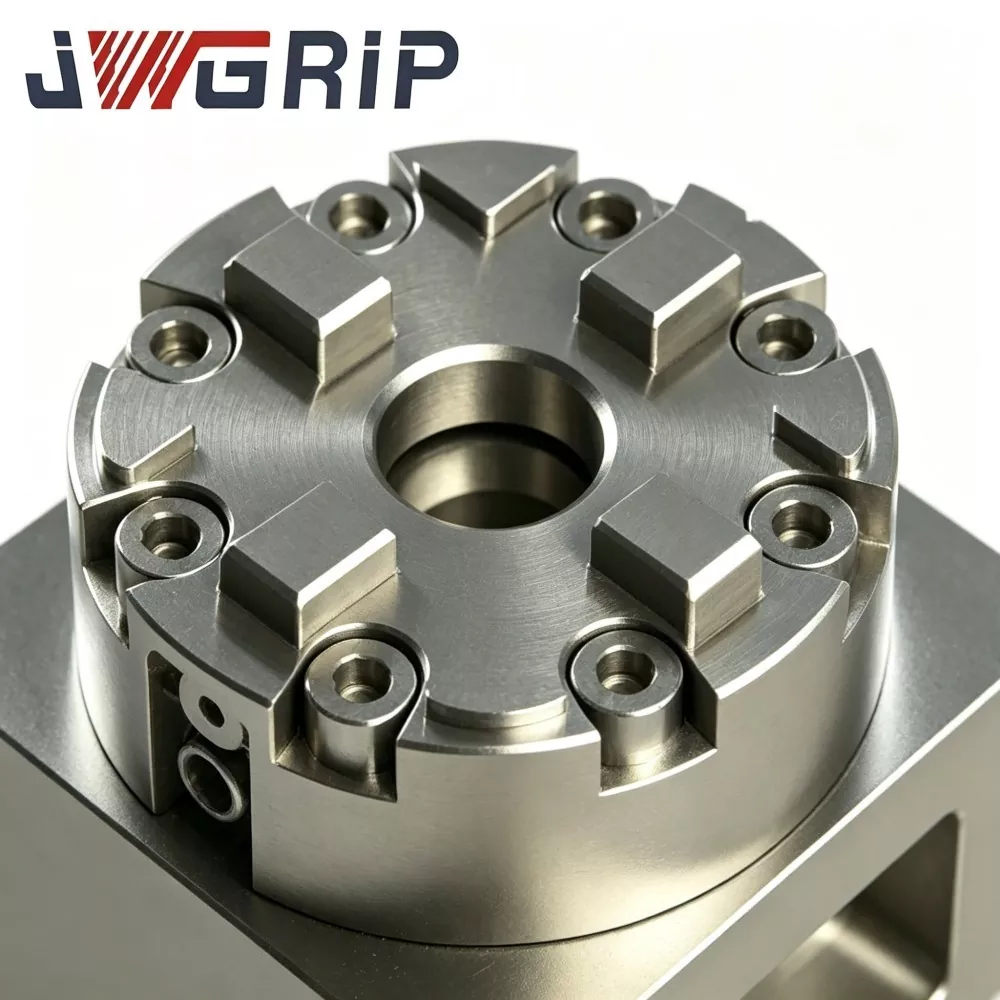
JWGRIP R-Type D75 MacroStd CNC Manual EDM Chuck uses multi-jaw centering clamping architecture complying with MacroStd specifications:
1. Bottom mounting datum strictly follows D75 outer-dimension benchmark; it can mount directly to EDM work-table or pair with transitional adapter plates.
2. Movable clamping jaws are driven by internal wedge-cam mechanical transmission set. Operators apply standardized torque through external manual torque wrench. Wedge-cam components push jaws radially toward central locating hole for centering clamping of electrode shanks or MacroStd-standard holders.
3. Reversing wrench rotation releases wedge-cam pre-load; clamping jaws open so fixtures or electrodes can be disassembled.
Key structural design highlights:
· All core locating reference planes are finished with one-clamp multi-pass precision grinding, lowering assembly-caused accumulated tolerance.
· Reinforced inner-shell ribs evenly spread manual-torque-generated clamping stress across the chuck shell, avoiding stress concentration at partial jaw-mount positions and enhancing anti-deformation performance during long-term cyclic manual locking. The design maintains stable concentricity and repeat-positioning performance both for volume-bidding production sites and spot-consignment end-user mold workshops.
· Jaw moving-contact surfaces receive special anti-wear surface treatment to slow abrasion induced by carbon sediment contamination from spark-erosion oil-bath working environment.
Core Technical Performance
1. Trustworthy Centering & Repeat-Positioning Capability Key locating functional surfaces undergo repeated precision-grinding. Concentricity ≤0.004 mm and repeat positioning accuracy ≤0.003 mm. No positioning deviation accumulates even after thousands-time manual lock-unlock cycles, satisfying strict tolerance requirements for multi-cavity mold electrode manufacturing.
2. High-Strength Wear-Resistant Alloy-Steel Main-body Main-body adopts premium 41Cr4 alloy steel with integral quenching-and-tempering heat-treatment, surface hardness reaches HRC 53-57. It delivers excellent impact-resistance, anti-deformation and dielectric-oil corrosion-resistance, adapting to long-time cyclic manual clamping in EDM oil-immersed conditions. Well-accepted among cost-conscious high-end mold-making enterprises.
3. Torque-regulated Stable Manual-Clamping Experience Operators lock with standard torque wrench, recommended tightening torque: 5-7 Nm. Constant-torque operation prevents fluctuating clamping-force caused by inconsistent hand-applied force. After one-time machine-table datum calibration, re-tramming workload during electrode swap drops sharply. EDM machine effective utilization rises for frequent-variant small-batch mold orders and repetitive electrode-processing assignments.
4. MacroStd-Compliant Broad Compatibility D75 outer dimension and inner locating dimensions fully follow MacroStd industrial benchmark. Compatible with most mainstream MacroStd-series electrode holders, locating pallets and fixture adapters on global tooling market. Drawing-based structural modification is available for special-height needs, reserved avoidance cut-outs and non-standard mounting-hole layout to satisfy personalized technical requirements from volume-bidding projects.
5. Authorized Industrial Compliance & Batch Inspection Each production lot carries out dimension inspection, hardness testing, cyclic wear simulation and concentricity-stability test. CE and ISO9001 inspection-report documents can be supplied for enterprise clients completing volume-bidding formal procedures.
Evaluation Checklist
1. Measure available installation dimensions of EDM machine work-platform. Confirm vertical and horizontal reserved clearance; prevent mechanical interference between chuck shell and machine-tool spindle or moving axes.
2. Prepare matched standard torque wrench for manual locking. Excessive torque will lead to permanent jaw deformation; insufficient torque creates electrode-slippage risk during spark-erosion cutting.
3. Check dimensional standard of existing electrode holders. Confirm whether current tooling follows MacroStd benchmark. Non-standard modified holders require extra transitional adapter components.
4. Keep appropriate distance between main mounting-screw positions and dielectric-oil liquid level, to reduce sediment accumulation on threaded parts.
5. For enterprise volume-bidding clients or spot-consignment dealers, submit complete on-site environment parameters and performance requirements in advance to achieve accurate product-configuration matching.
Maintenance points
While operating JWGRIP R-Type D75 MacroStd CNC Manual EDM Chuck, pay attention to misuse hazards and routine-maintenance guidelines below:
1. Strictly follow recommended tightening-torque range of 5-7 Nm. Excessive wrench force will cause permanent jaw deformation. Insufficient torque creates electrode-slippage risks in spark-erosion processing.
2. Avoid carbon-sediment accumulation inside jaw guide-grooves. Carbon-particle contaminants abrade moving mating surfaces and degrade positioning accuracy. Establish fixed periodic-cleaning work flow for on-site operators.
3. Protect central locating hole and clamping-jaw working surfaces against heavy mechanical collision. Hard impact damages datum precision and directly impairs concentricity performance.
4. Regularly inspect mounting-screw-hole thread status; clear rust and oil sediment. Apply a small amount of anti-rust grease for long-term non-working storage.
5. For volume-bidding tender-project clients, unify on-site operation-tool configuration requirements of different branch-workshops during early-phase technical communication.
6. For spot-consignment dealers, implement regular mutual stock-taking to synchronize bilateral inventory quantity data.
FAQ
Q1: Are you manufacturer or trading supplier for R-Type D75 MacroStd CNC Manual EDM Chuck?
A1: JWGRIP is genuine fixture-manufacturer located in China. All production procedures are completed in-house. We provide drawing-driven modification support, volume-bidding tender-document matching service and spot-consignment cooperation instead of working as simple middleman trader.
Q2: Can this manual-type chuck maintain stable performance under long-time EDM dielectric-oil immersion?
A2: Standard-version moving-matching-surfaces receive anti-wear surface-treatment adapted for EDM oil-bath environment. Please strictly perform periodic carbon-sediment cleaning maintenance to extend overall service-life.
Q3: What are concentricity and repeat-positioning accuracy of standard-spec R-Type D75 MacroStd CNC Manual EDM Chuck?
A3: Standard-product concentricity ≤0.004 mm, repeat positioning accuracy ≤0.003 mm. Higher-precision variants can be realized by drawing-driven technical modification.
Q4: Which damages are excluded from warranty-coverage scope?
A4: Two-year warranty covers manufacturing-caused defects under rated-torque and correct-installation conditions. Damage caused by over-torque operation, hard mechanical collision, abrasive-particle wearing and improper manual-maintenance is not covered. Clamping jaws belong to consumable wearing-parts.
Q5: Can I obtain formal commercial-quotation documents for tender usage?
A5: Yes. Please contact JWGRIP sales department. We prepare formal commercial-quotation documents based on product configuration, order scale and specific-business-mode including volume-bidding tender-project or spot-consignment cooperation.
Hot Tags: R-Type D75 MacroStd CNC Manual EDM Chuck, Supplier,Manufacturer
Related Category
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.