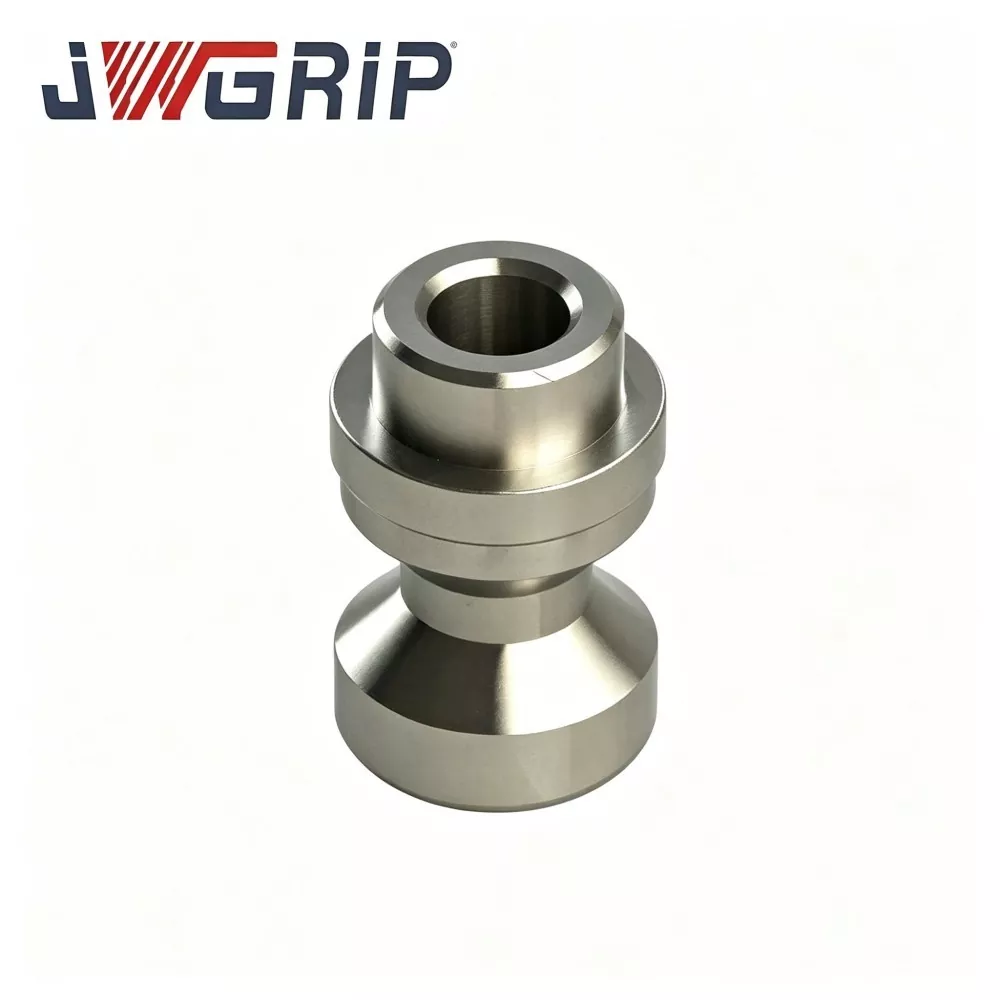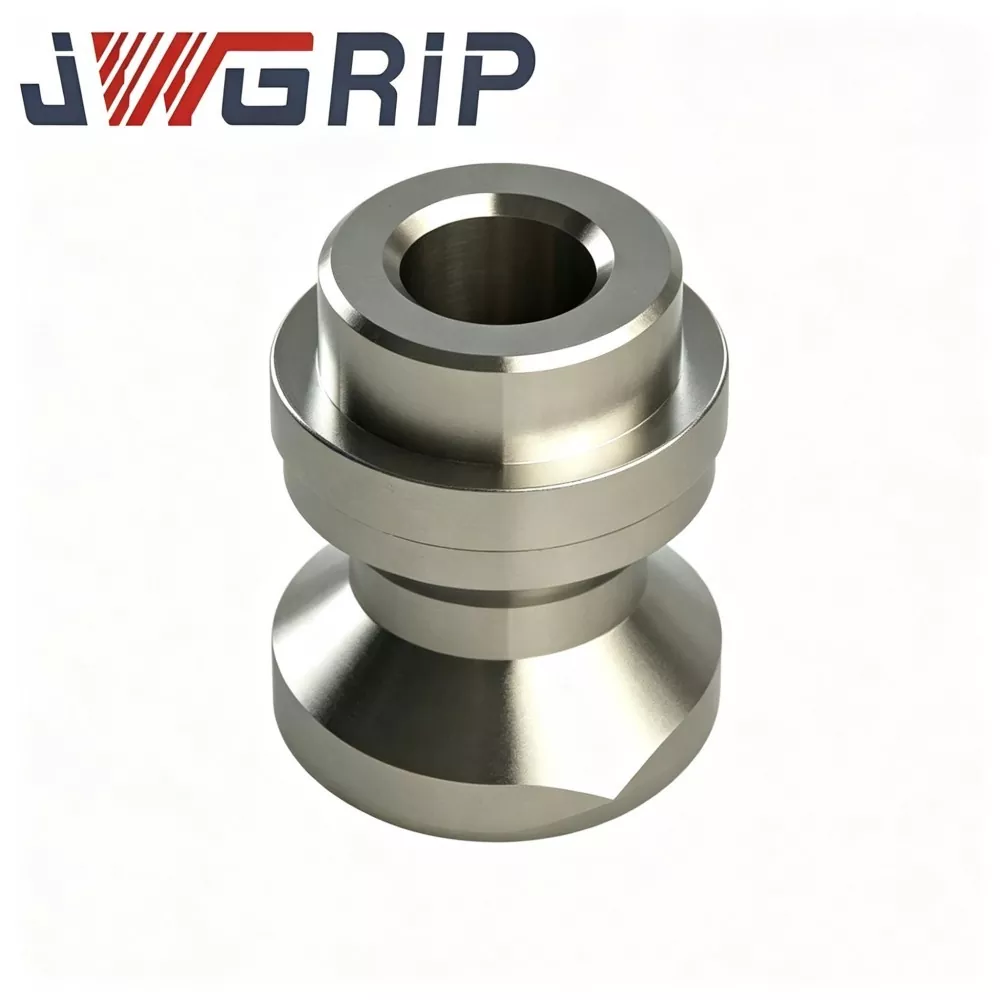
Precision D20 Zero Point Pull Stud for CNC Fixture
JWGRIP is the professional manufacturer and supplier of Precision D20 Zero Point Pull Stud for CNC Fixture in China, providing Factory Direct sales service with standard models fully in Stock to serve global fixture integrators, CNC machine shops and tooling maintenance departments. It is a high-performance core load-bearing positioning component specially designed and matched for D20 series zero-point clamping tooling systems. Integrating benchmark positioning, locking force transmission and anti-rotation constraint functions into a single optimized structural unit, it perfectly adapts to high-speed milling, drilling and multi-axis composite cutting processes.
Precision D20 Zero Point Pull Stud for CNC Fixture adopts high-strength alloy steel blank, processed through professional hot forging, multi-step tempering and spherical surface carburizing and quenching treatment. Different from ordinary bar stock processed pull studs without structural optimization, it optimizes internal metal fiber distribution along the force transfer path, effectively reducing spherical spalling, shoulder deformation and thread fatigue damage under long-term heavy-load cyclic clamping conditions. With ultra-stable geometric tolerance retention after massive repeated clamping cycles, the durable component fully meets CE mechanical safety standards for machine tool auxiliary parts.
Every batch undergoes strict raw material spectral inspection, forging flaw screening, hardness grading, spherical precision grinding and cyclic clamping simulation tests to ensure consistent quality. It is widely applicable for new fixture supporting assembly and replacement maintenance of aged & deformed pull studs on production lines. Supporting small-batch trial production and large-volume batch ordering, as well as OEM and personalized customization of shoulder size, thread specification and surface strengthening technology, it provides reliable high-precision zero-point positioning solutions for modern CNC flexible machining production.
Functional Analysis
Zero-point fixture technology drastically shortens fixture-change-over time for multi-variant CNC machining and has become mainstream tooling for 3-axis and 5-axis machining-centers. The D20 zero-point pull-stud is fastened underneath fixture-plate bottom face and cooperates with D20 clamping-collet inside zero-point base. It realizes fast locking and high-precision repeated positioning for fixture plates.
Typical failure-chain caused by defective pull-stud:
① Spherical-surface spalling / indentation → positioning datum deviation
② Shoulder plastic-deformation → decline of perpendicularity
③ Thread wear / damage → insufficient pre-tightening force
④ Final result:fixture-plate positioning drift, unstable clamping force, batch-part dimensional fluctuation, hidden safety-risk under high-speed cutting.
Core function
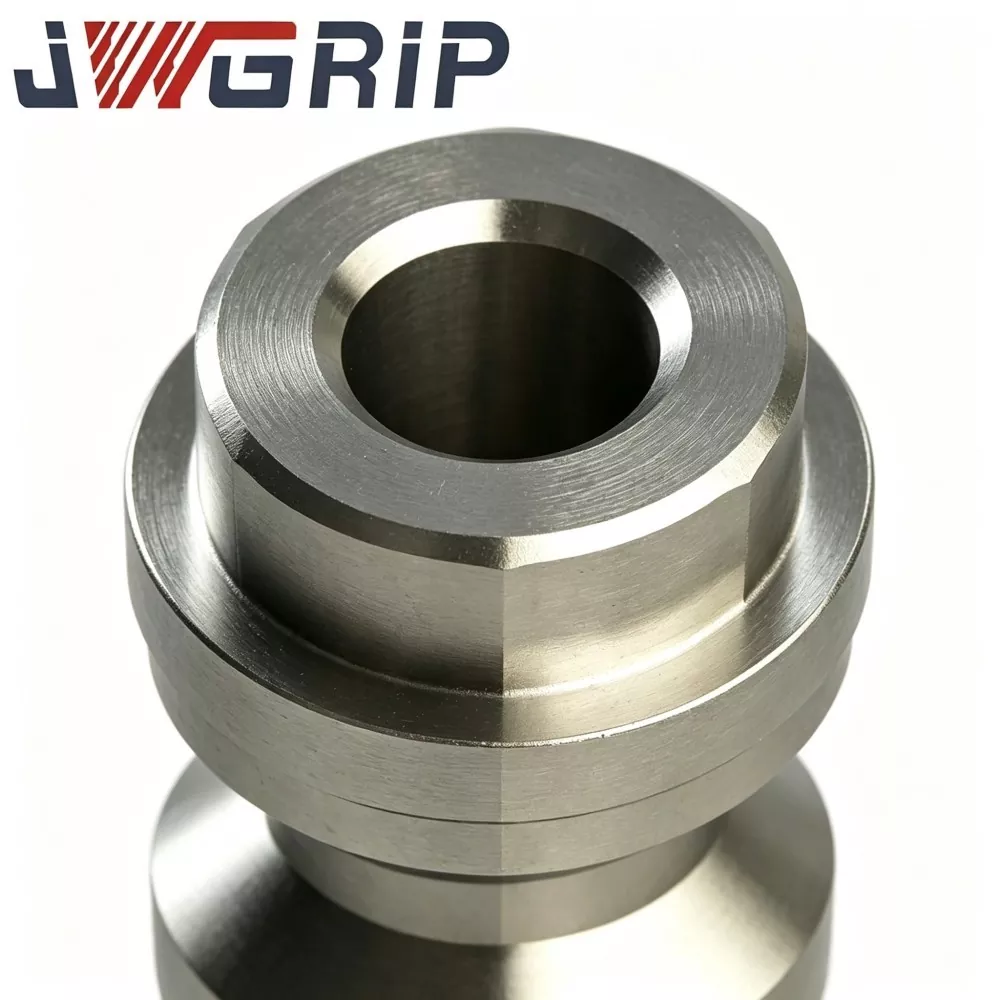
Precision Precision D20 Zero Point Pull Stud for CNC Fixture is divided into three core functional sections:
1. Threaded connecting segment
Fastens whole pull-stud onto fixture-plate bottom surface; transmits partial axial pre-tension torque. Thread machining precision directly determines perpendicularity between spherical locating-head and fixture-plate datum plane.
2. Reference shoulder segment
Serves as mounting reference face when screwing pull-stud into fixture-plate; bears partial axial pre-tension force. Shoulder flatness and perpendicularity are critical indexes for overall fixture repeat-positioning-accuracy.
3. Spherical locating-head segment
Core mating working zone, contacts and cooperates with clamping-collet inside zero-point base; undertakes pull-down locking-force and forms geometric positioning-benchmark. Spherical-surface suffers high local contact-pressure during every clamping-unclamping cycle.
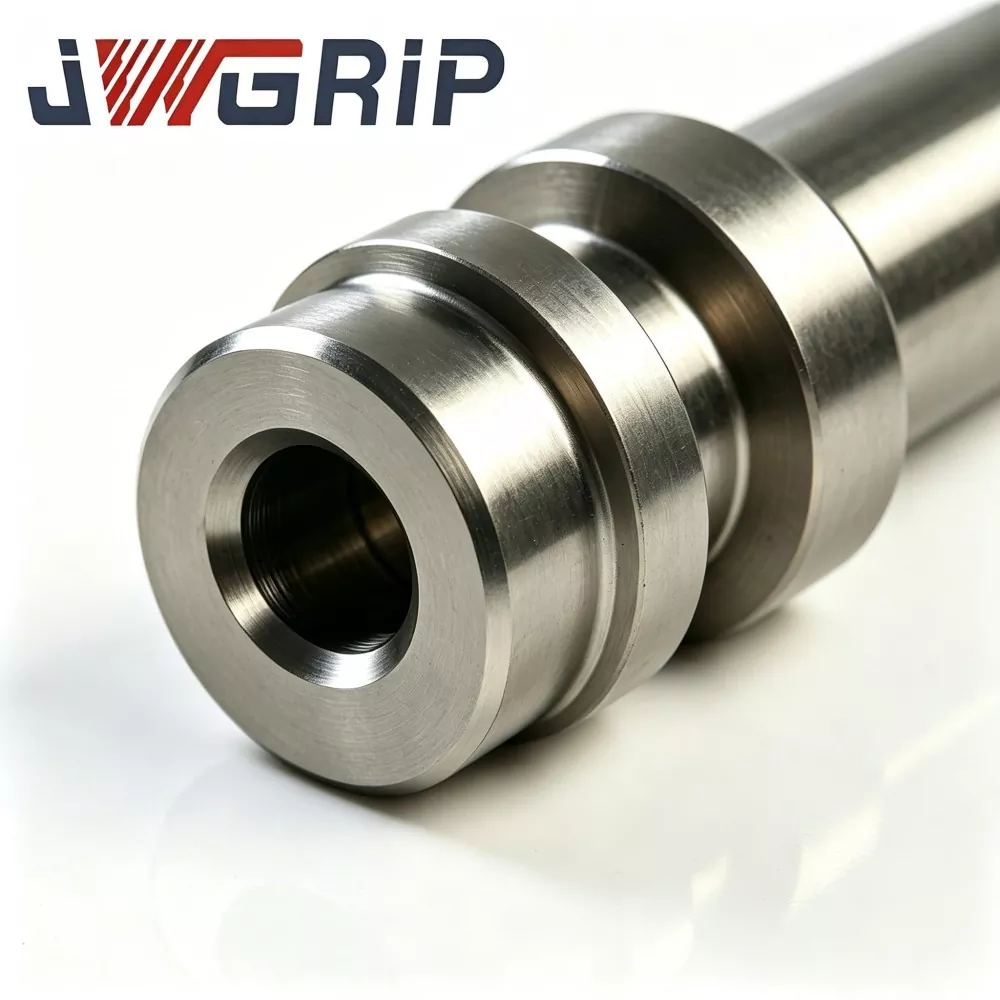
production risks:
1. Spherical locating-head bears cyclic high contact-stress in each clamping-loop, high risk of contact-fatigue damage.
2. Reference-shoulder may generate micro-deformation risk under excessive installation-torque.
3. Thread segment bears combined tension plus vibration-load during cutting processes.
Market-common low-cost pull-studs only adopt bar-stock turning without hot-forging; metal-fiber flow is cut off, anti-fatigue performance drops sharply under heavy-load repeated-clamping. JWGRIP adopts hot-forged blank, making metal-fiber distribute continuously following force-transfer direction. When fixture-plate thickness or load-level differs from standard specifications, OEM custom-order can adjust dimension of each segment and material configuration.
Production Quality
Every batch of JWGRIP Precision D20 Zero Point Pull Stud for CNC Fixture executes multi-stage quality-control workflow before delivery:
1. Raw-material spectral-composition inspection, verify alloy-steel material grade compliance.
2. Hot-forging forming, non-destructive forging-defect screening.
3. Multi-step tempering heat-treatment, hardness grading test.
4. Semi-finish turning for thread, shoulder and spherical-head pre-forming.
5. Spherical-surface carburizing-quenching surface-strengthening treatment.
6. Ultra-precision spherical-surface grinding and thread finishing.
7. Sampling simulated cyclic-clamping fatigue test, verify anti-fatigue performance under rated-load.
Only pull-studs passing full-item inspection will enter finished-goods stock for shipment. Non-conforming products are rejected and will not flow to customers.
Typical On-Site Fault-Diagnosis Reference
|
Fault Phenomenon |
Possible Cause |
Suggested Countermeasure |
|
Fixture repeat-positioning accuracy drifts |
Spherical-head spalling / indentation; zero-point collet inner-cavity scratch; pull-stud shoulder deformation |
Check pull-stud appearance; inspect zero-point collet; replace damaged components |
|
Pull-stud loosens on fixture-plate |
Thread damage; insufficient tightening torque; hole misalignment during installation |
Check thread condition; apply recommended torque; guarantee hole coaxiality when assembling |
|
Obvious vibration occurs during cutting |
Foreign-body clamped between spherical-head and collet; pull-stud loose |
Disassemble, clean contact surface; retighten pull-stud following torque specification |
Installation Reminders
1. Strictly follow official recommended tightening-torque value when mounting pull-stud onto fixture-plate. Excessive torque will produce permanent shoulder-deformation; insufficient torque leads to thread loosening under cutting vibration.
2. Keep spherical-head locating-surface completely dry and clean; never apply grease or oil onto spherical mating-area.
3. Inspect pull-stud appearance regularly during mass-production: check spherical-head for indentation, spalling, crack; inspect shoulder and thread for deformation or wear.
4. Replace pull-stud immediately once spherical-head shows visible damage, or repeat-positioning-accuracy cannot recover after thorough cleaning. Do NOT continue production with defective pull-stud.
5. For custom-dimension pull-studs, strictly comply with engineering drawing requirements on fixture-plate counter-bore depth, hole coaxiality and flatness.
After-Sales Services
1. Warranty statement:Under correct installation, torque-compliant assembly and rated-clamping-cycle working-conditions, non-consumable main-body enjoys 1-year warranty. Damage caused by overload-clamping, wrong tightening-torque, foreign-body abrasive-wear, man-made collision and chemical-corrosion beyond specification is excluded from warranty scope.
2. Remote online-technical guidance for installation and fault-analysis support. Global customers may submit technical-inquiry by email; engineers reply within 24 working-hours.
3. Complete dimensional drawings and material-performance documentation provided for each order.
4. Engineering-level technical consultation for OEM custom-projects: shoulder-size adjustment, thread-spec modification, spherical-tolerance optimization, special surface-treatment etc.
5. Spare-part batch supply for repeat-purchase of standard or custom pull-studs.
Procurement Selection Reference
Core value of JWGRIP Precision Precision D20 Zero Point Pull Stud for CNC Fixture:
hot-forged continuous metal-fiber structure, multi-step heat-treatment plus spherical-surface carburizing-quenching, strict multi-stage incoming-&-process-quality-control, compatible with mainstream D20 zero-point-system, supports OEM dimension / surface-treatment customization.
It solves common accessory-side bottlenecks of zero-point fixture system:spherical-surface spalling, shoulder deformation, thread fatigue failure, short service-life of bar-stock-turned low-cost pull-studs.
Selection reminders:
1. Confirm matching zero-point-system specification, verify mounting-dimension compatibility before ordering.
2. Clarify fixture-plate thickness, actual maximum clamping-load and workshop cutting-environment (ordinary / high-corrosion) to decide whether standard or custom version shall be adopted.
3. Standard stocked versions realize short lead-time; adopt OEM custom-engineering service for special shoulder size, thread or surface-strengthening-requirements.
FAQ
Q1: Can standard D20 pull-stud directly replace pull-studs from other-brand zero-point-systems?
Standard-version only fits D20-spec zero-point-system with fully-matched dimensions. If dimensions differ, OEM customized pull-stud shall be adopted.
Q2: How to judge when pull-stud needs to be replaced?
Replace immediately if spherical-head has visible indentation, spalling or crack; or repeat-positioning-accuracy cannot be restored after thorough cleaning.
Q3: Can I apply grease onto spherical locating-head for lubrication?
No. Spherical contact-surface must stay dry and clean. Grease will adsorb metal chips and create clamping-failure risks.
Q4: What is the essential difference between forged pull-stud and ordinary bar-stock-turned pull-stud?
Hot-forged blank forms continuous internal metal-fiber flow, improving anti-contact-fatigue-performance under massive repeated-clamping cycles. Simple bar-stock turning cuts off metal-fiber, leading to shortened service-life under long-term cyclic-working-conditions.
Hot Tags: Precision D20 Zero Point Pull Stud for CNC Fixture, China, Manufacturer, Supplier, Factory
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.