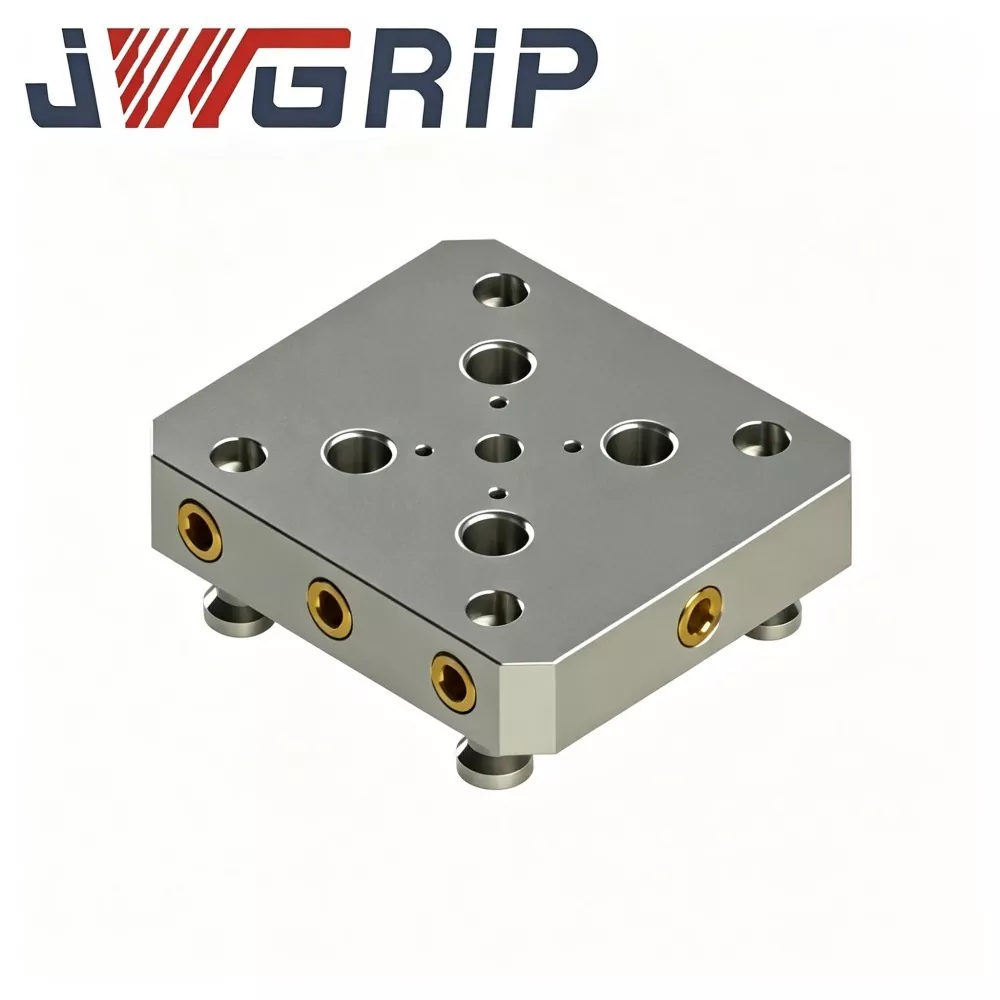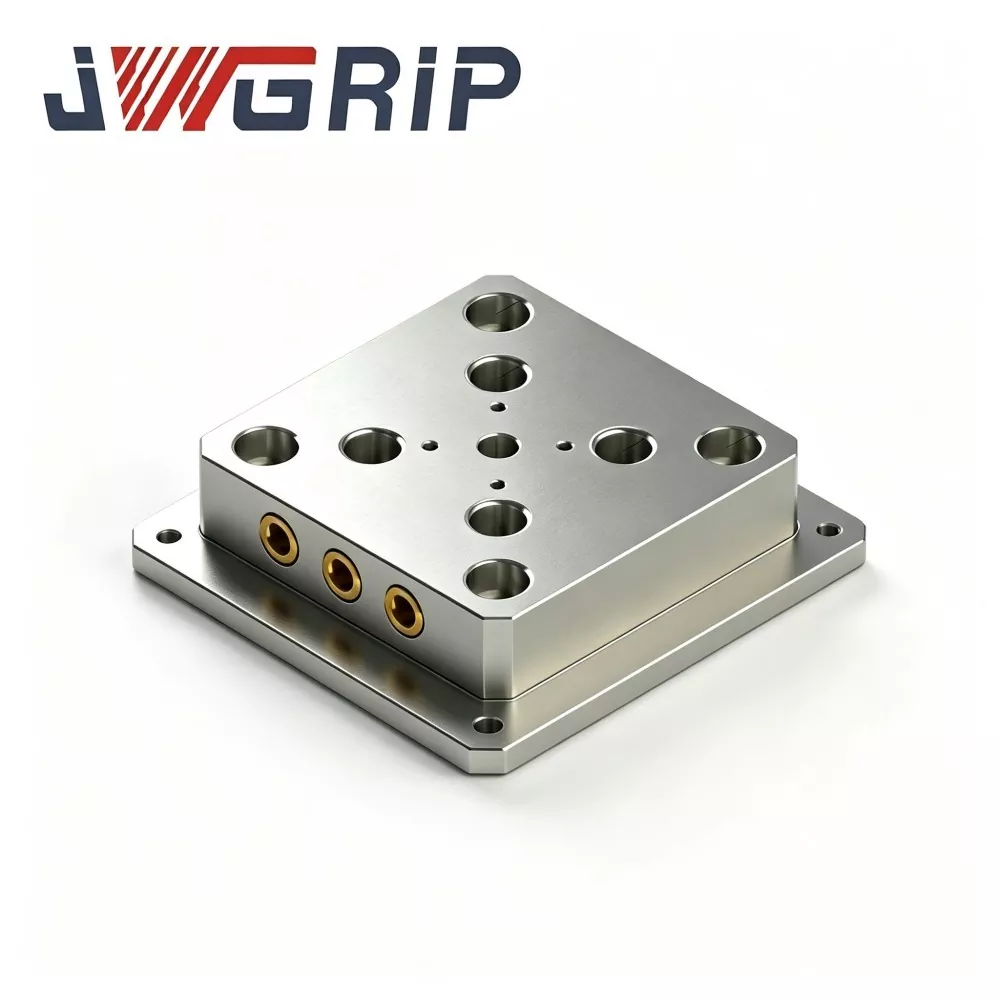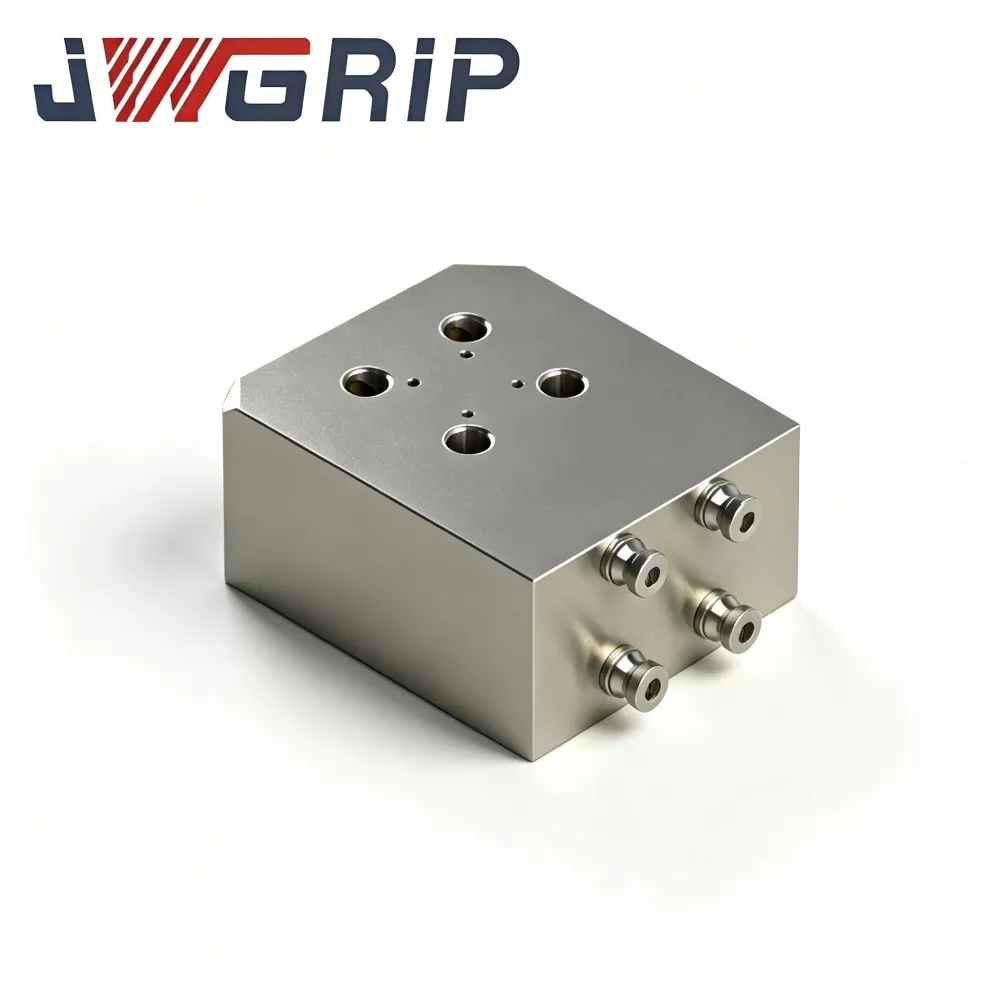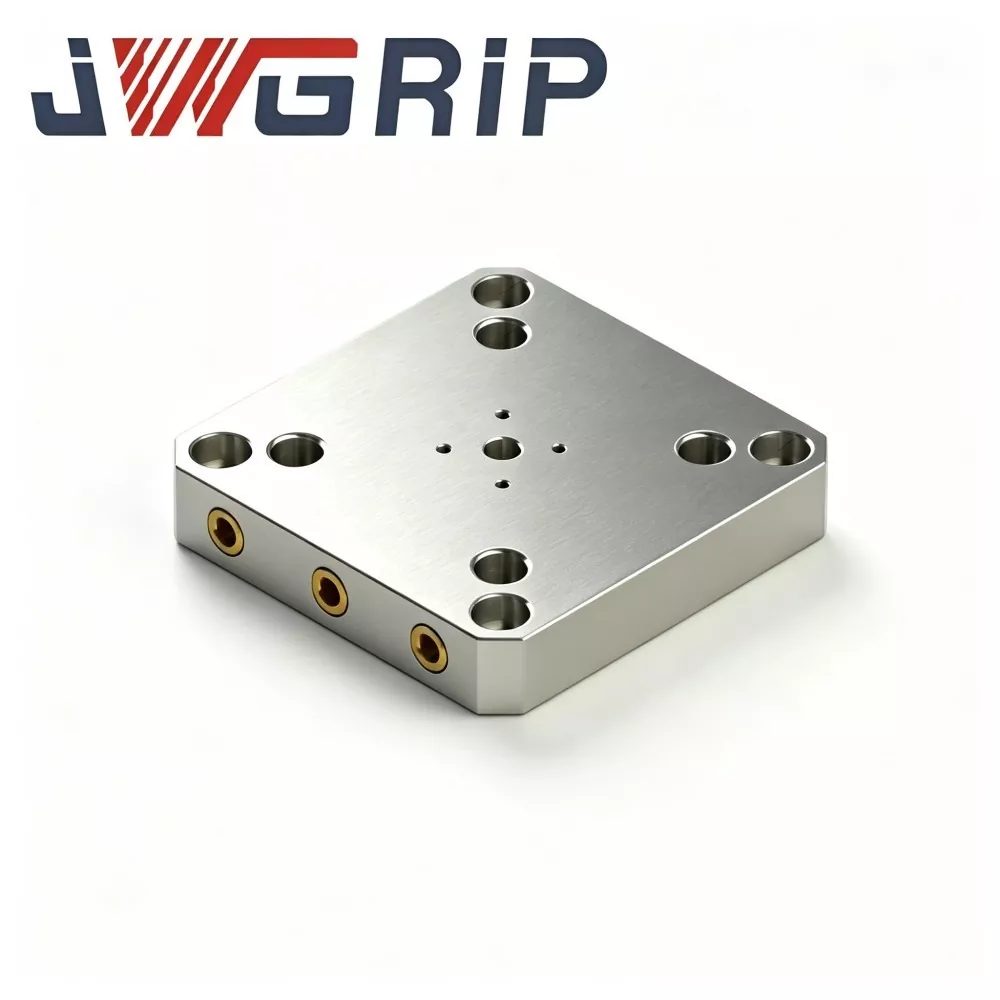
96 Quick Change Fixture Plate for CNC Workholding
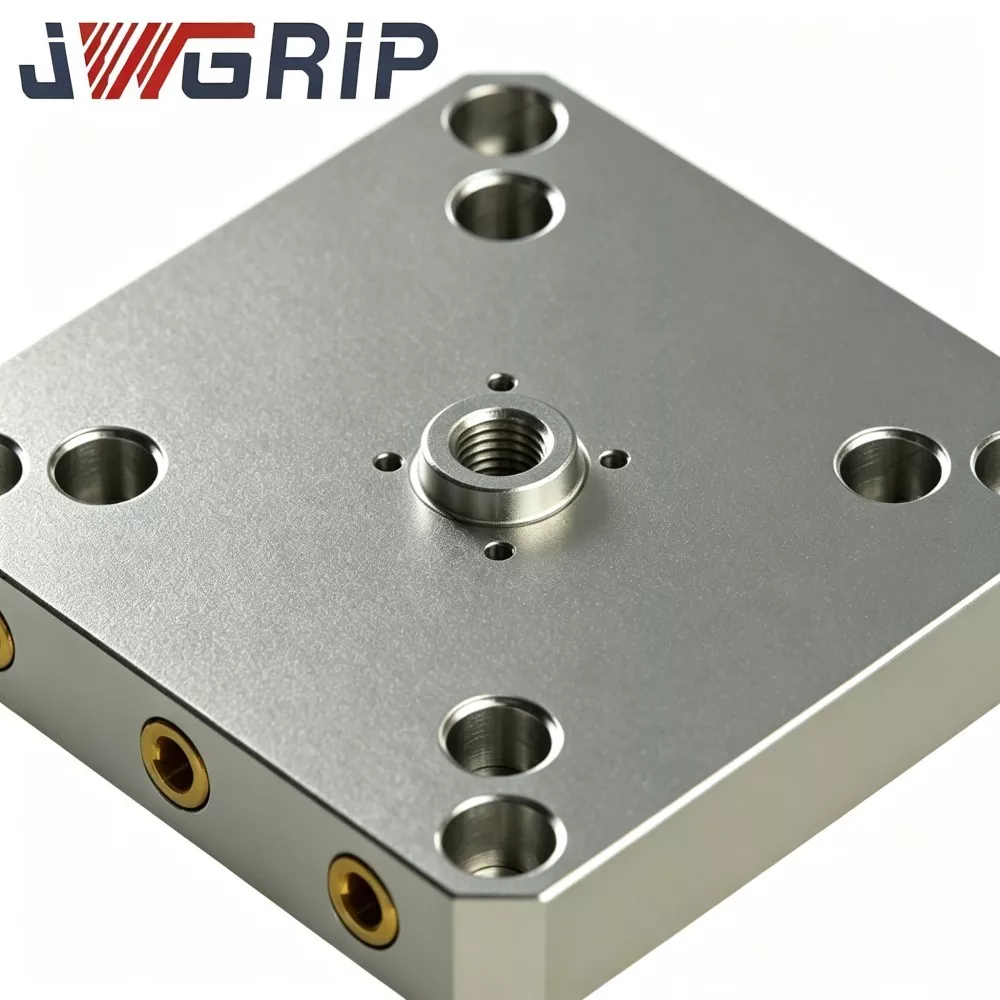
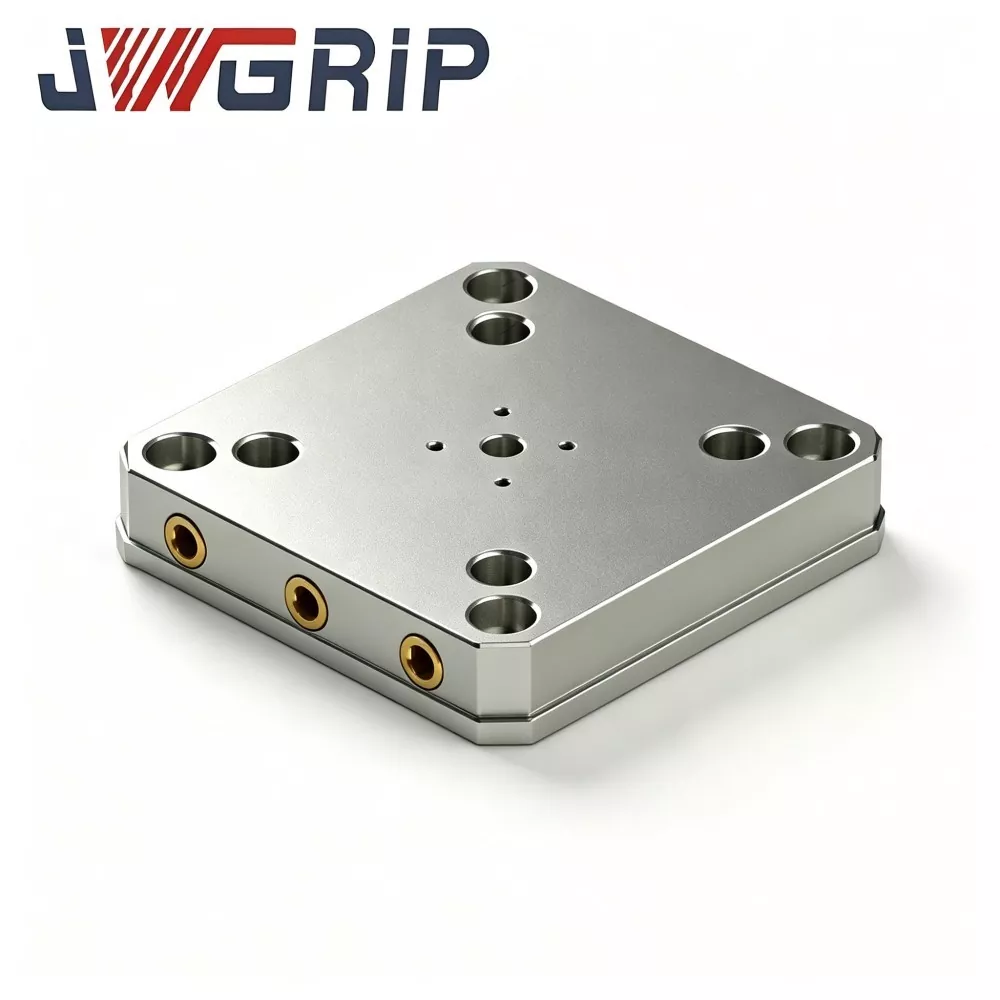
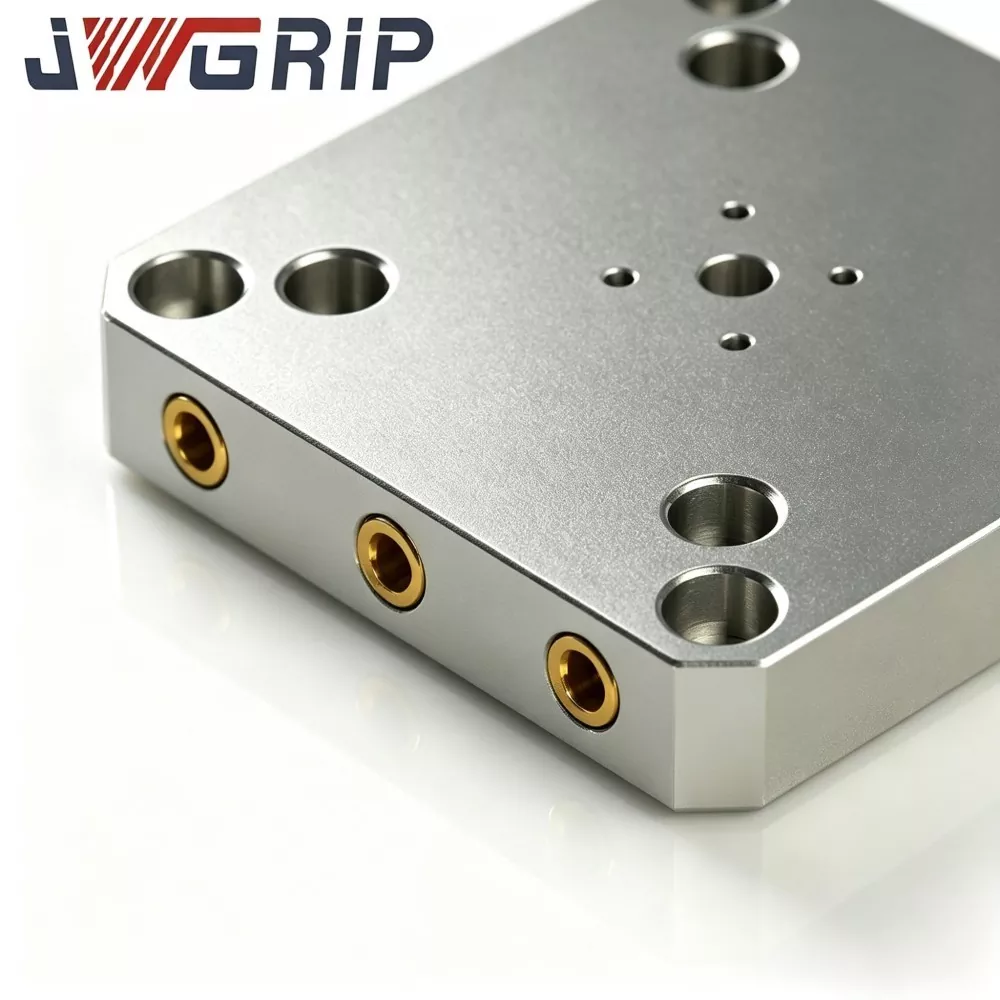
JWGRIP is the professional manufacturer and supplier of 96 Quick Change Fixture Plate for CNC Workholding in China, providing Factory Direct service with standard models fully in Stock to support global tender procurement and project cooperation. It is a high-efficiency integrated upper tooling plate specifically designed for modern CNC milling, five-axis machining and mold manufacturing workshops. It integrates a standardized 96-series pull-stud mounting pattern, a high-rigidity load-bearing plate body and a grid top workpiece-mounting interface into a single unit, eliminating repeated dial-indicator calibration and extra transitional spacer plates.
This high-performance 96 Quick Change Fixture Plate for CNC Workholding is manufactured from premium 42CrMo hardened alloy steel, featuring outstanding repeat-positioning accuracy, ultra-robust structural rigidity and long-term stable mechanical performance. All key positioning reference surfaces adopt strict one-clamping integral machining technology to ensure high overall datum consistency. After rough machining, the alloy-steel blanks undergo complete stress-relieving aging treatment to thoroughly eliminate internal residual stress and avoid structural deformation caused by long-term alternating cutting loads.
Critical mating surfaces — the bottom locating face that sits on the 96 chucks and the top workpiece-mounting datum — are finished by ultra-precision grinding, delivering stable and reliable mating performance. Supporting offline fixture presetting and rapid on-machine locking/swapping, it effectively reduces manual alignment workload, shortens fixture setup time and lowers non-cutting downtime. Widely applicable to mold processing, multi-axis precision milling and automated production lines, it provides a solid, standardized and high-efficiency modular clamping platform for global industrial machining workshops.
Why Choose JWGRIP
Conventional fixture plates create many troubles in daily mold and multi-axis machining workshops:
· Frequent fixture replacement requires repeated installation, alignment and manual calibration. Setup quality heavily depends on operator skill, yielding unstable positioning results and wasting valid production hours.
· Homemade ordinary fixture plates lack a standardized pull-stud pattern and datum machining. Sustained alternating cutting loads produce stress concentration and subtle plate deformation, gradually ruining positioning accuracy and batch-part dimensional consistency.
JWGRIP improves the product from raw-material processing to finished-part grinding:
All critical positioning reference surfaces adopt one-clamping complete-machining strategy.
Hardened 42CrMo alloy-steel blanks go through full stress-relief aging after rough machining to remove internal residual stress.
The bottom locating face and top workpiece datum are precision-ground to secure stable seating on 96-series zero-point chucks.
The standard 96-series pull-stud pattern enables offline fixture presetting. Operators build vises and sub-fixtures on the plate outside the machine; the complete plate is then seated onto the 96 chucks and locked in seconds, cutting manual alignment workload.
Custom & OEM services support special-size workpieces and unique machine-table installation needs, offering a reliable modular clamping platform for mold processing, multi-axis precision milling and automated production lines.
Core Mechanism
The JWGRIP 96 Quick Change Fixture Plate is the upper tooling plate that mates with 96-series zero-point chucks mounted on the machine table:
The bottom locating face conforms to the 96-series zero-point pattern. Tapped holes on the bottom receive matched 96-pattern pull studs, which screw in from below and engage the internal clamping collets of the 96 chucks.
The bottom locating surface sits flat on the chuck reference faces; once the chucks clamp, the whole plate is pulled down and radially/axially located on one repeated-positioning datum.
The top surface uses an industry-standard grid layout of threaded holes and dowel-pin holes for mounting vises, sub-fixtures or workpieces directly.
Side datum edges are precision-milled for on-machine edge-finding and repeat loading.
Key mechanical design highlights:
All positioning reference points — bottom locating face, pull-stud hole pattern and top datum — are machined on a single plate body. Assembled spacer parts are minimized to avoid accumulated tolerance drift during repeated swap cycles.
The reinforced pocketed/ribbed structure spreads dynamic cutting force over the whole plate instead of concentrating stress on local pull-stud holes, improving durability under heavy-cutting conditions.
Locating reliability stays stable for continuous shift-based production, whether used for tender-procurement workshop projects or high-frequency changeover sites.
Technical Performances
Stable repeat-positioning accuracy: Critical datum surfaces receive multi-pass precision grinding. Repeat-positioning accuracy ≤0.010 mm after hundreds of fixture swaps. Position tolerance of the pull-stud hole pattern is strictly controlled within ±0.006 mm to prevent cumulative positioning deviation in multi-setup part machining.
42CrMo high-strength hardened alloy-steel body: Integral quenching & tempering heat-treatment delivers surface hardness HRC 54–58. Good anti-impact and anti-deformation performance resists chip scratch, cyclic clamping pressure and intermittent heavy-cutting load. Widely adopted by mold workshops, auto-component factories and aerospace processing plants.
Obvious tooling-change efficiency gain: After the 96 chucks are one-time installed on the machine table, a fixture-plate swap takes only 8–12 seconds. No repeated dial-indicator tramming is needed. Non-productive setup time drops significantly, lifting overall equipment effectiveness both for mass production and for prototype orders with frequent changeover.
Broad compatibility plus custom-OEM support: The standard pull-stud pattern fits mainstream commercial 96-series zero-point chucks. The top grid layout accommodates standard vises, sub-plates and locating jigs. The JWGRIP factory provides OEM & custom service: outer dimensions, grid hole layout, pull-stud pattern, avoidance cut-outs and mounting-boss height can all be adjusted. Customized versions satisfy special demands for tender-procurement projects and automation-line transformation.
Complete industrial certification & batch inspection: Every batch undergoes dimension check, hardness test, flatness/parallelism inspection and positioning-stability verification. ISO9001 inspection reports can be provided for tender-procurement formal-document submission.
Production & Quality-control
All JWGRIP 96 Quick Change Fixture Plate for CNC Workholding is manufactured and inspected inside our Chinese factory following a standardized multi-phase workflow:
1. Raw-material incoming inspection: 42CrMo steel bar goes through chemical-composition analysis and hardness test; material certificates attached. Unqualified raw materials are rejected directly.
2. Rough CNC milling: rough-machine outer contour, pocket/rib structure and pre-holes; leave finishing allowance on all positioning-related surfaces.
3. Quenching & tempering heat-treatment: precisely control heating, holding and cooling curves to reach HRC 54–58 target hardness and release internal material stress. This step is mandatory for anti-deformation performance under long-term dynamic cutting.
4. Stress-relief aging: further release residual stress introduced by rough machining and heat-treatment.
5. Finish CNC machining: machine the bottom pull-stud tapped holes, bottom locating face, top grid holes, side datum edges and auxiliary features; critical dimension tolerance controlled within ±0.007–0.012 mm.
6. Multi-run precision surface grinding of the top and bottom datum planes to guarantee flatness and parallelism.
7. Thread-gauge verification and pull-stud mounting simulation: confirm every tapped hole mates with the matched 96-pattern pull stud without interference.
8. Final comprehensive inspection: dimension, hardness, flatness, parallelism, pull-stud hole-position accuracy and repeat-positioning performance on a 96 chuck. Each product receives a unique traceability serial number. Non-conforming plates go for rework rather than packaging.
9. Anti-rust cleaning, black-oxide surface treatment and shock-resistant plywood-case packaging.
Mis-operation Risks
When deploying the JWGRIP 96 Quick Change Fixture Plate, watch these misuse points to avoid equipment crash or positioning failure:
Evaluate overall height in advance. The combined height of the fixture plate plus upper vises/sub-fixtures may trigger spindle crash. Run simulation measurement before formal mass cutting.
Distinguish static bearing capacity from dynamic cutting load. Even with a high static-pressure test value, users must follow the official rated dynamic-load parameters under real cutting impact.
Prevent chip accumulation on the bottom locating face and inside the pull-stud tapped holes. Iron-chip residues scratch the locating face and create positioning deviation. Implement regular on-site cleaning maintenance.
Tighten pull studs only to the specified torque. Over-torque distorts the tapped holes and plate datum; under-torque loosens under cutting vibration.
For tender-procurement projects: confirm certification format, inspection-report content and serial-number traceability requirements at the early communication phase.
Packaging
Every JWGRIP fixture plate goes through complete cleaning, anti-rust-oil spraying and anti-rust-paper wrapping, then is packed into a foam-filled shock-resistant plywood wooden case to avoid collision and vibration damage during sea freight, air freight or land transport.
Available Logistics Options
Multiple logistics selections for different order scenarios:
Sea freight: large-volume tender-procurement project shipments
Air freight: time-urgent inventory replenishment
International express: small-volume trial-sample delivery
FAQ
Q1: Are you manufacturer or trading supplier for the 96 Quick Change Fixture Plate for CNC Workholding?
A1: JWGRIP is a real fixture manufacturer based in China. All production workflows are finished in-house. We provide OEM development and tender-procurement supporting service rather than working as a middleman trader.
Q2: Can this fixture plate be adapted for non-standard modified 96-series chucks?
A2: The standard version matches industry-general 96-pattern zero-point chucks. If your chucks are heavily modified non-standard units, please send drawings or photos for technical assessment before ordering.
Q3: What is the repeat-positioning accuracy of the standard fixture plate?
A3: The standard JWGRIP 96 Quick Change Fixture Plate reaches repeat-positioning accuracy ≤0.010 mm. Higher-precision custom versions can be developed according to special technical requirements.
Q4: What is the warranty coverage scope?
A4: Two-year warranty against manufacturing-caused defects under rated-load and correct-installation conditions. Damage caused by overload, chip corrosion, mechanical collision or improper maintenance falls outside the warranty scope.
Q5: Can I get a formal quotation and price-list documents?
A5: Yes. Please contact the JWGRIP sales team. We prepare a price-list or formal commercial quotation based on product configuration, order scale and business requirements.
Hot Tags: 96 Quick Change Fixture Plate for CNC Workholding, China, Manufacturer, Supplier, Factory
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.