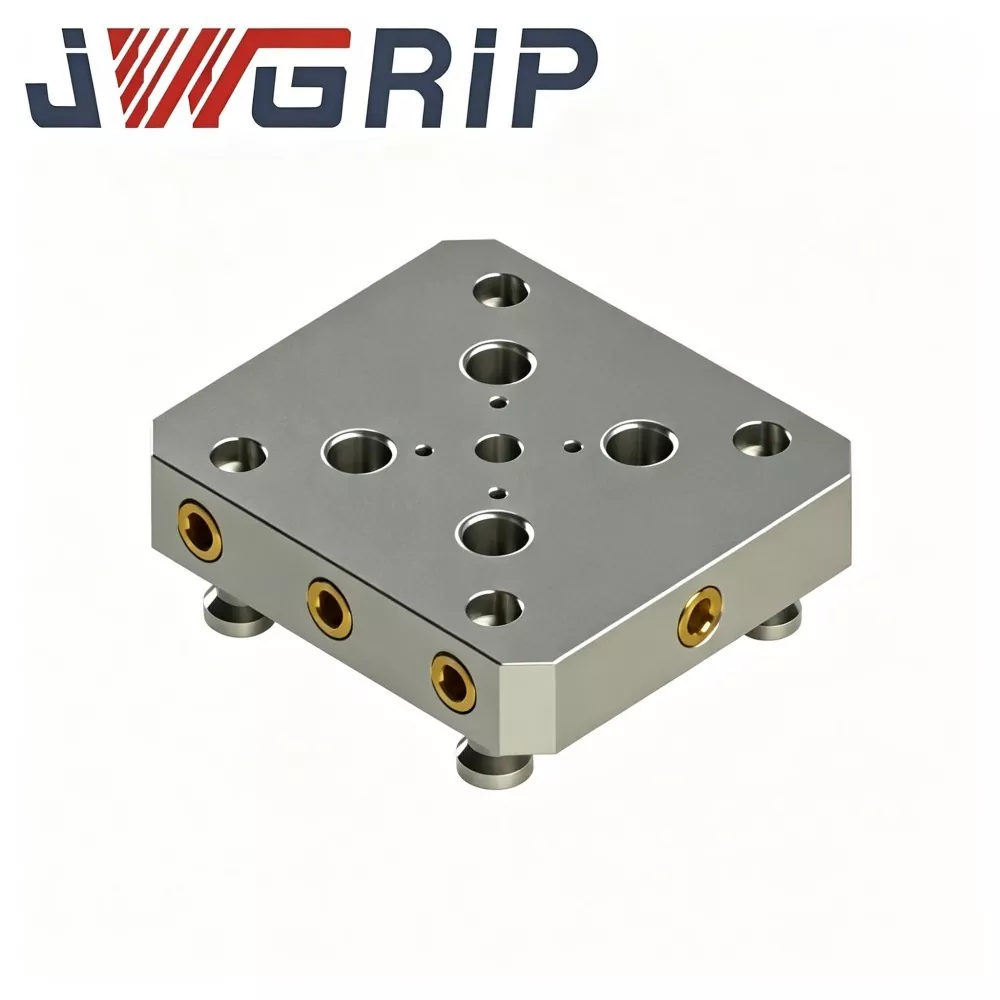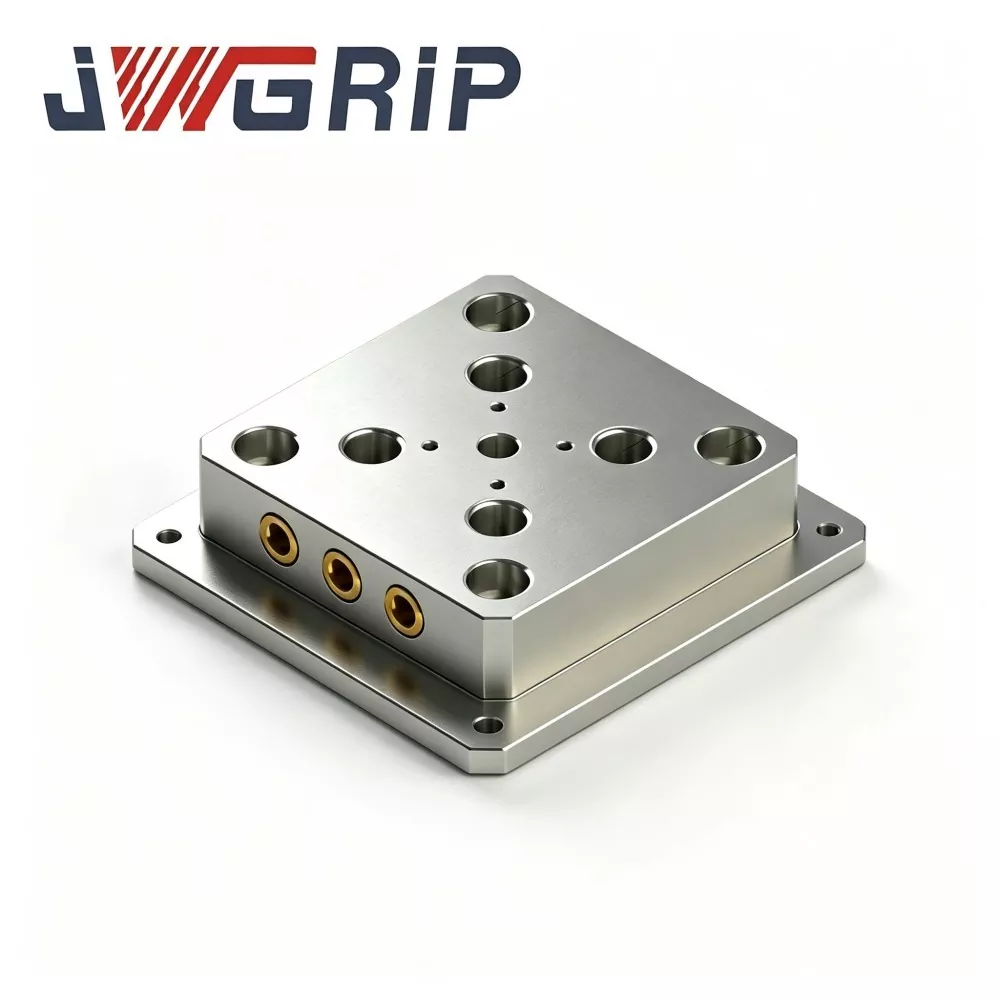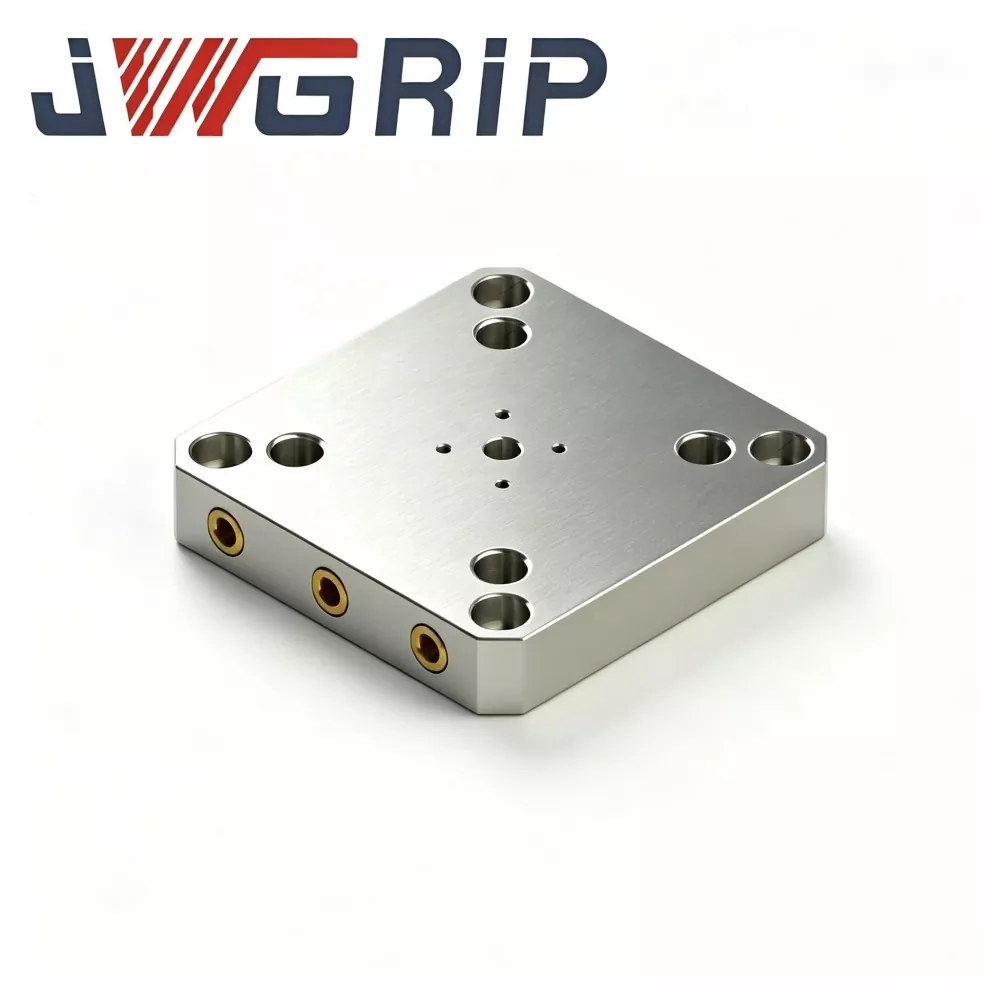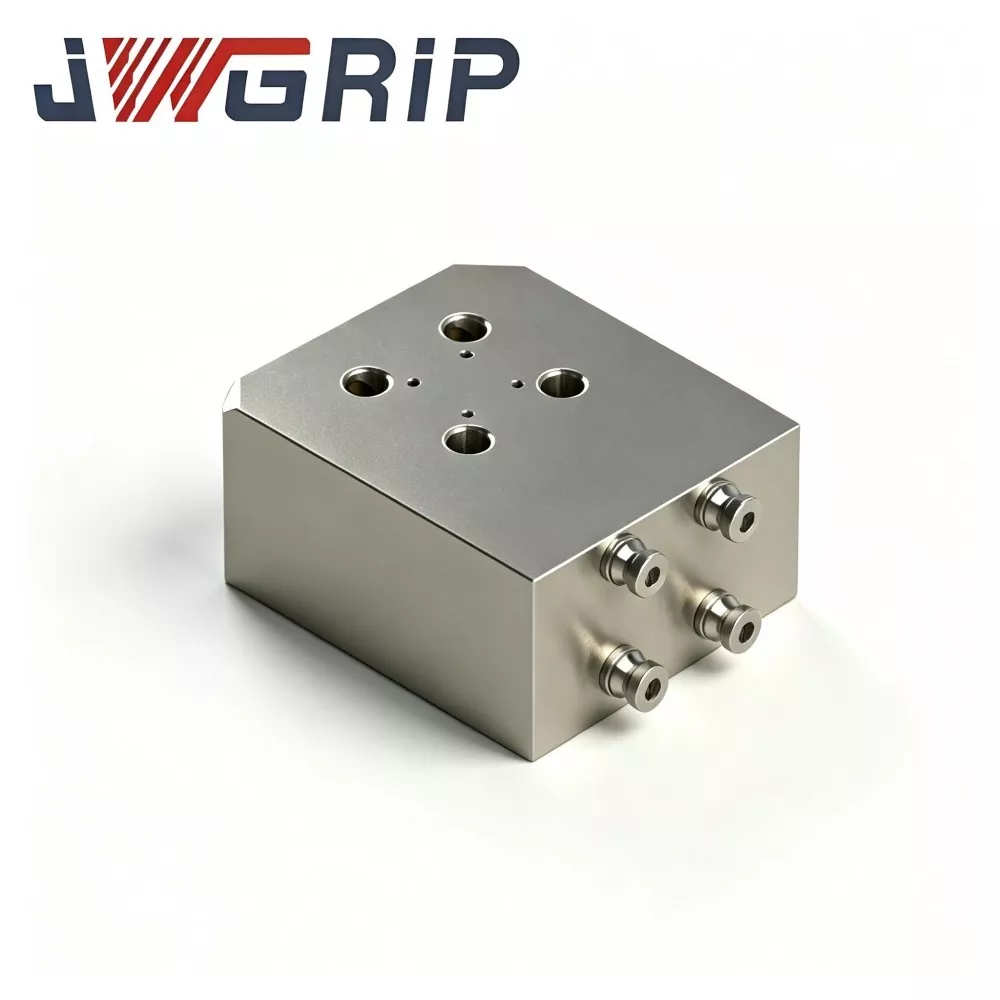
Double-Sided Swivel Quick Change Fixture Base
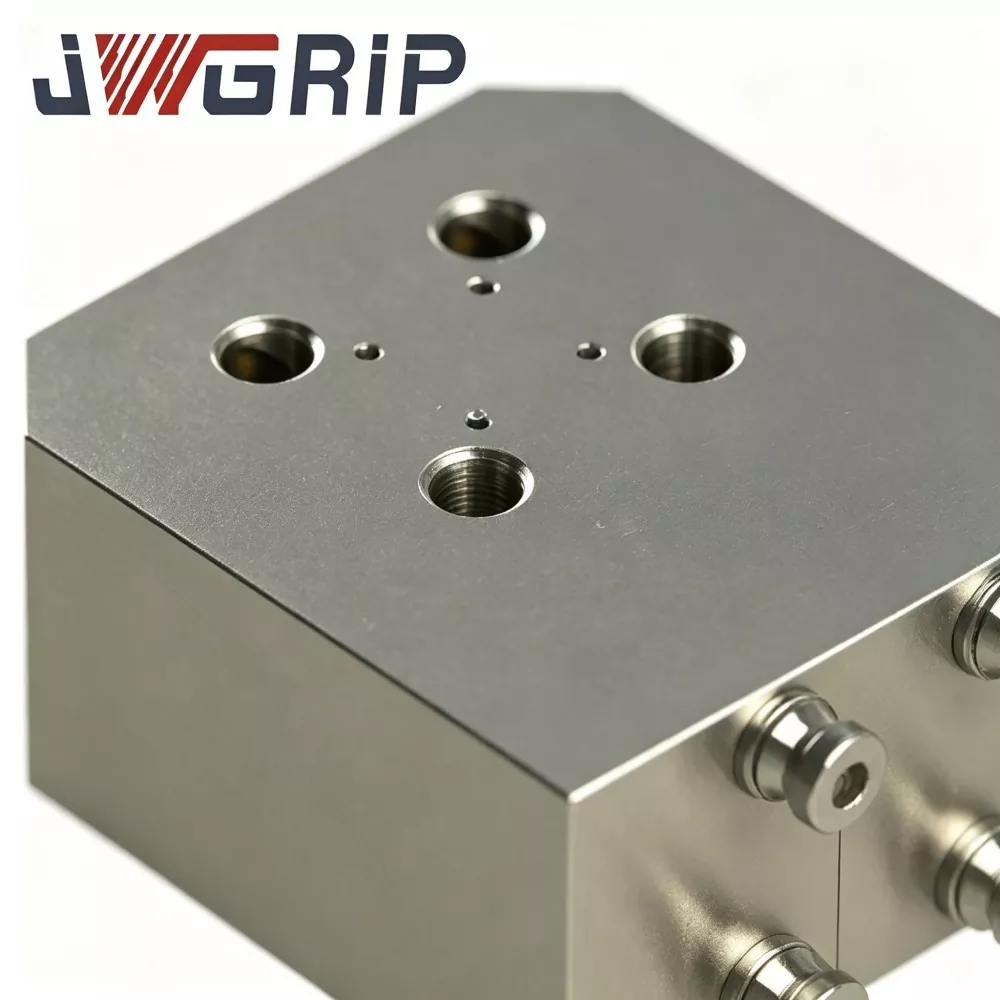
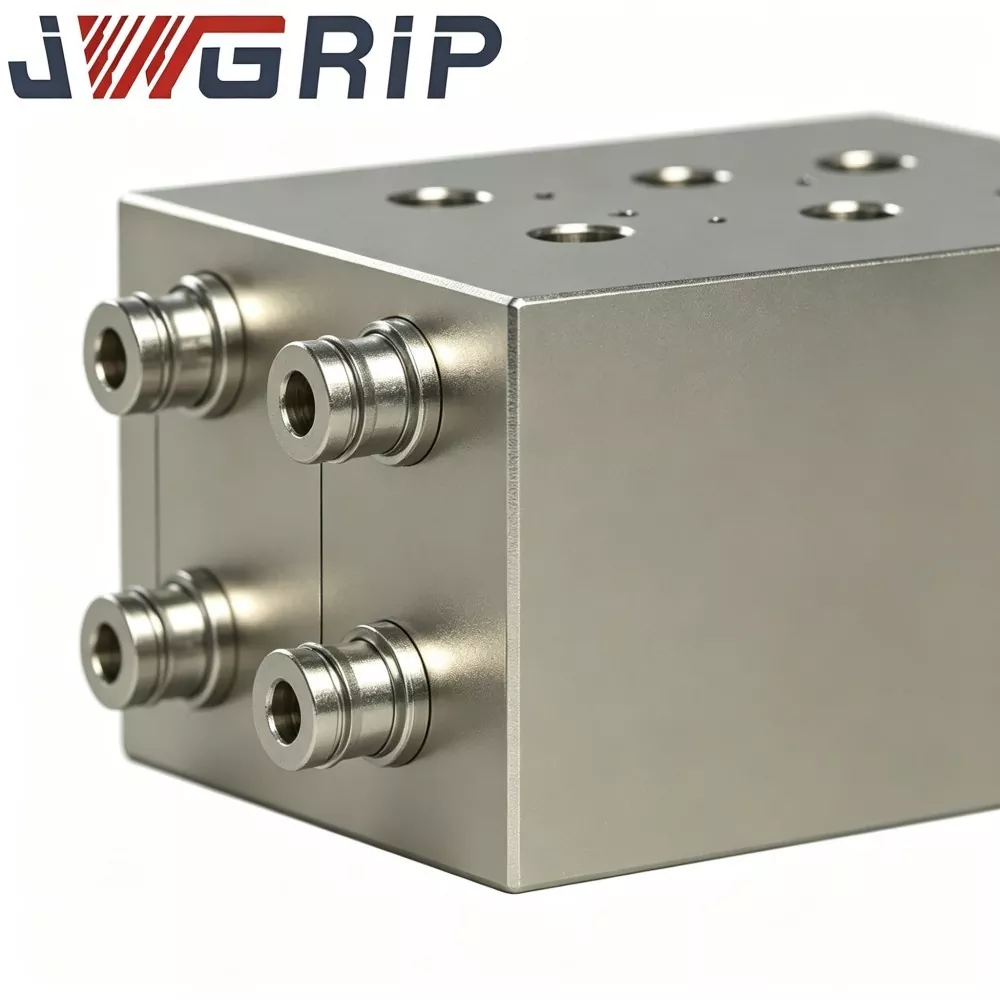
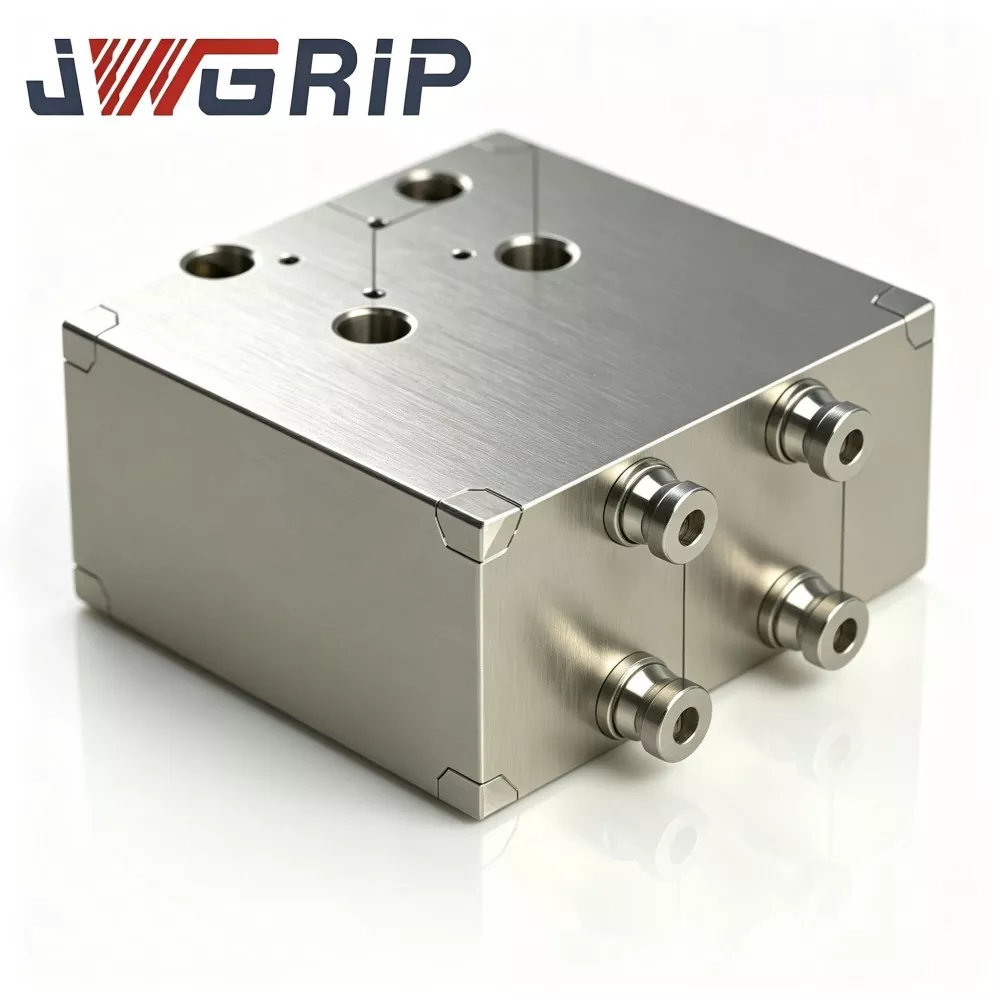
JWGRIP is the trusted wholesaler and exporter of Double-Sided Swivel Quick Change Fixture Base in China, supporting Factory Direct procurement with standard products fully in Stock to meet global industrial project demands. It is a high-performance integrated rotary positioning fixture base specially optimized for multi-process and multi-surface CNC machining scenarios. It integrates double-sided mounting function and 360-degree free rotation capability into a single unit, adopting integral hardened alloy steel structure and integrated quick-change positioning design. It eliminates repeated disassembly and re-alignment work for the base, and can be directly installed and fixed on CNC machine tool worktables, supporting OEM and customized modification to adapt to special workpiece sizes and machine tool installation interfaces.
This advanced double-sided swivel fixture base features durable mechanical structure, stable clamping performance and excellent repeat positioning accuracy. All key rotating mating surfaces undergo strict stress-relieving aging treatment and precision grinding processing, effectively avoiding clearance looseness and accuracy attenuation caused by long-term cyclic rotation. The unique double-sided mounting layout allows simultaneous installation of two sets of workpieces or sub-fixtures, realizing 360-degree angle adjustment without removing the fixture base from the machine table.
Double-Sided Swivel Quick Change Fixture Base greatly simplifies multi-surface machining procedures, shortens non-cutting auxiliary clamping time, reduces human-induced positioning deviation, and significantly improves overall equipment efficiency and batch machining consistency. Widely applicable to CNC milling, turning and five-axis composite machining of auto parts, aerospace components and electronic hardware parts, it provides flexible, efficient and high-precision clamping solutions for high-mix and low-volume production workshops worldwide.
Core Functional Logic
Multi-surface machining often requires multiple clamping re-positioning operations. Traditional fixture solutions need manual disassembly, removal and re-alignment of fixtures, which brings long auxiliary time and human positioning errors. The Double-Sided Swivel Quick Change Fixture Base integrates rotary indexing mechanism, double-sided fixture mounting interface and zero-point quick-change positioning unit as one complete assembly.
After the base is fixed on the CNC machine worktable, operators can complete angle indexing and locking on-machine. Two groups of sub-fixtures or workpieces can be installed on two opposite mounting sides. When one-side workpiece completes machining, the rotary unit drives the platform to rotate to switch working stations, without removing the whole base from machine tool.
Typical failure transmission path caused by abnormal swivel fixture base:
1. Rotation mating surface wear / insufficient locking force → indexing angle deviation
2. Double-sided mounting datum deformation → parallelism & perpendicularity error between two stations
3. Final result:Unstable workpiece dimension, batch size fluctuation, hidden safety risk during high-speed cutting.
JWGRIP standard Double-Sided Swivel Quick Change Fixture Base keeps compatible installation dimension with mainstream zero-point quick-change systems. It can be used for new-build fixture project assembly as well as replacement of aging rotary fixture bases on running production lines. OEM custom engineering modification service is supported for non-standard table size, special rotation-locking torque, large-load-bearing requirement and corrosion-resistant working environment. Both small-batch trial purchase and large-volume fixture-matching bulk orders are acceptable.
Key Functional Segments
JWGRIP Double-Sided Swivel Quick Change Fixture Base consists of five key functional sections, each undertaking different mechanical stress in repeated rotation-locking cycles.
1. Machine-table mounting base segment
Bottom fixed support body, installed and locked onto CNC machine tool worktable or zero-point positioning chuck. It bears total cutting composite load. Mounting datum flatness directly determines overall fixture base positioning stability.
2. Precision rotary bearing assembly segment
Core rotating kinematic pair, supports 360° free rotation of upper double-sided platform. Adopts high-precision heavy-load bearings. Rotation clearance is strictly controlled after pre-loading, to avoid angular drift under cutting vibration. It belongs to high-fatigue-risk friction pair.
3. Hydraulic / Pneumatic indexing locking segment
Power locking unit for angle positioning. After target rotation angle is in-place, the locking mechanism acts to rigidly lock rotary platform, resisting cutting impact force. Locking force determines anti-vibration performance during machining.
4. Double-sided fixture mounting working platform
Two opposite high-precision datum planes for installing sub-fixtures, vises or direct workpiece clamping. Both sides are equipped with standard grid threaded holes and positioning pin holes. The parallelism and flatness of double-sided datum are critical indexes for batch machining consistency.
5. Quick-change positioning interface segment
Built-in zero-point quick-change positioning structure, allows fast swapping of double-sided platform module. It supports rapid replacement of different mounting platforms without disassembling bottom base body.
Many low-cost market-supplied rotary fixture bases adopt common-grade bearings without stress-relief treatment. Rotation clearance becomes larger after short-term cyclic operation, indexing angle drifts easily under cutting impact. JWGRIP adopts integral hardened alloy-steel base body, full stress-relief aging for all rotary mating surfaces, and pre-loaded heavy-duty bearing configuration to improve rotation repeatability and anti-vibration performance. OEM custom orders can adjust platform outline size, locking power mode, bearing grade and double-sided hole-layout according to customer-specific load and fixture requirements.
Quality-Control System
Every production batch of JWGRIP Double-Sided Swivel Quick Change Fixture Base completes sequential multi-item inspection before ex-factory. Non-conforming components are rejected and will not flow to customers.
1. Raw-material spectral composition inspection, verify alloy-steel material-grade compliance.
2. Integral forging / casting forming, non-destructive defect-screening for internal cracks and inclusions.
3. Multi-stage stress-relief aging heat-treatment, eliminate internal residual stress.
4. Precision machining for machine-table base, rotary mating surface and double-sided mounting platform preprocessing.
5. Surface hardening treatment for rotary friction contact surfaces and mounting datum planes.
6. Ultra-precision grinding for double-sided fixture-mounting datum and rotary matching surfaces.
7. Sampling bench test: actual locking-force measurement, 360° indexing repeat-positioning test and thousands-time rotation-locking cyclic fatigue verification.
Fault-Diagnosis Reference Table
|
Fault Phenomenon |
Probable Root Cause |
Recommended Disposal Measure |
|
Indexing angle deviation after rotation locking |
Bearing wear; insufficient locking force; residual chips on rotary mating surface |
Clean rotary mating surface; check locking power source; inspect bearing pre-load status; replace worn components |
|
Poor parallelism between double-sided mounting datum |
Platform datum surface dent / deformation; uneven stress release of base body |
Check flatness of double-sided datum; re-grind or replace platform if over-tolerance |
|
Intermittent vibration chatter during cutting |
Insufficient locking rigidity; bearing clearance enlarged; foreign particles inside rotary pair |
Re-adjust locking-force parameter; clean rotary assembly; maintain or replace bearing assembly |
|
Slow or incomplete locking action |
Pneumatic / hydraulic source pressure abnormal; internal sealing element aging |
Check power source pressure; inspect seal parts; replace aging sealing components |
Assembly Guidelines
1. During base installation, thoroughly clean CNC machine-tool worktable or zero-point chuck datum surface. Remove chips, oil residue and foreign particles before mounting the fixture base. Foreign contaminants will cause installation tilt and positioning error.
2. Strictly follow official torque specification to fasten mounting bolts. Prevent base-body deformation caused by over-torque, or loose installation caused by insufficient torque.
3. Keep rotary mating surfaces and double-sided mounting datum clean during daily production; avoid hard impact hitting on mounting datum planes.
4. Regularly inspect fixture-base performance in mass-production workshops: monitor indexing repeat-positioning accuracy, locking-force stability and cutting vibration status. Maintain or replace wearing parts timely once performance degrades obviously.
5. Do NOT operate fixture base continuously exceeding rated bearing load and rated locking-force. Overload condition will aggravate bearing and locking-mechanism wear and shorten service-life sharply.
6. For OEM custom-size fixture base, strictly follow assembly-dimension requirement of customer installation drawing.
Packaging
JWGRIP Double-Sided Swivel Quick Change Fixture Base. Standard stocked items support fast global spare-part order dispatch.
1. Each single fixture base receives independent anti-rust protection treatment and separate inner packaging. Key precision datum surfaces are attached with protective film.
2. Small-quantity orders: anti-rust plastic bag plus reinforced paper carton with corner protection.
3. Bulk export orders:fumigation-free shock-resistant solid-wood crate with inner separating buffer padding, avoid scratch and deformation of precision datum surfaces during long-distance sea-and-land transportation.
4. OEM custom-modified orders follow mutually-confirmed project lead-time.
Corresponding batch-inspection report documents are enclosed for each shipment lot.
After-Sales Support Services
1. Warranty statement:Under correct assembly and rated-load cyclic-working-conditions, non-wearing main-structure enjoys 1-year warranty. Damage caused by overload-operation, foreign-body abrasive-wear, wrong-assembly, man-made impact and chemical-corrosion out-of-spec is excluded from warranty scope.
2. Remote online-technical-guidance for fixture-base installation and on-site fault-diagnosis support. Global customers may submit technical-inquiry by email, engineers reply within 24 working-hours.
3. Complete dimension drawings and batch inspection-records are provided for each purchasing-order.
4. Engineering-level technical consultation for OEM custom-projects: platform outline adjustment, locking-mode selection, double-sided hole-layout modification, special surface-strengthening-treatment etc.
5. Stable repeat-order spare-part supply for both standard-spec and custom-spec fixture-base wearing components (bearings, sealing parts, locking assemblies).
Procurement & Technical Assessment
Integral hardened alloy-steel base body, full stress-relief aging treatment, pre-loaded heavy-duty rotary bearing, double-sided high-precision mounting datum, built-in quick-change positioning interface, strict batch-wise factory inspection, supports OEM structural customization.
It solves common fixture-system accessory-side painpoints: Time-consuming multi-clamping re-alignment, indexing angle drift, poor parallelism between double working stations, insufficient anti-vibration rigidity during heavy-cutting, short service-life of low-cost ordinary rotary fixtures.
Assessment reminders:
1. Confirm machine-table installation dimension, maximum bearing load and required rotation-locking torque before ordering, verify dimensional interchangeability.
2. Clarify actual working cutting-load magnitude and production-cycle frequency, select standard or custom-reinforced version.
3. Standard stocked versions realize short lead-time; adopt OEM custom-engineering for special platform size, locking-mode or surface-strengthening-demands.
FAQ
Q1: Can standard-spec Double-Sided Swivel Quick Change Fixture Base match mainstream zero-point chucks from other brands?
Standard version is interchangeable only when bottom mounting dimensions are fully matched. If dimension difference exists, OEM custom-manufactured fixture base is required.
Q2: How to judge whether swivel fixture base needs maintenance or part replacement?
Carry out maintenance or replace wearing parts in time if indexing repeat-positioning accuracy obviously drifts, locking force becomes unstable, or obvious vibration chatter occurs during cutting, even after thorough cleaning of all mating surfaces.
Q3: Can we apply heavy-viscosity grease in large quantity onto rotary mating surfaces?
Use anti-wear grease in accordance with maintenance manual, excessive high-viscosity grease will trap metal chips and accelerate abrasive wear. Keep rotary mating assembly clean, regularly clean chip residues.
Q4: What is the advantage of stress-relieved integral-hardened fixture base compared with ordinary rotary fixture?
Integral hardened alloy-steel base with full stress-relief aging eliminates residual internal stress. It maintains stable indexing accuracy and double-sided datum flatness under thousands-time rotation-locking cycles. Ordinary rotary fixtures without stress-relief treatment are prone to gradual datum deformation and angle drift after long-time cyclic cutting load.
Hot Tags: Double-Sided Swivel Quick Change Fixture Base, China, Manufacturer, Supplier, Factory
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.