Automated Zero Point Pallet with Power Chuck
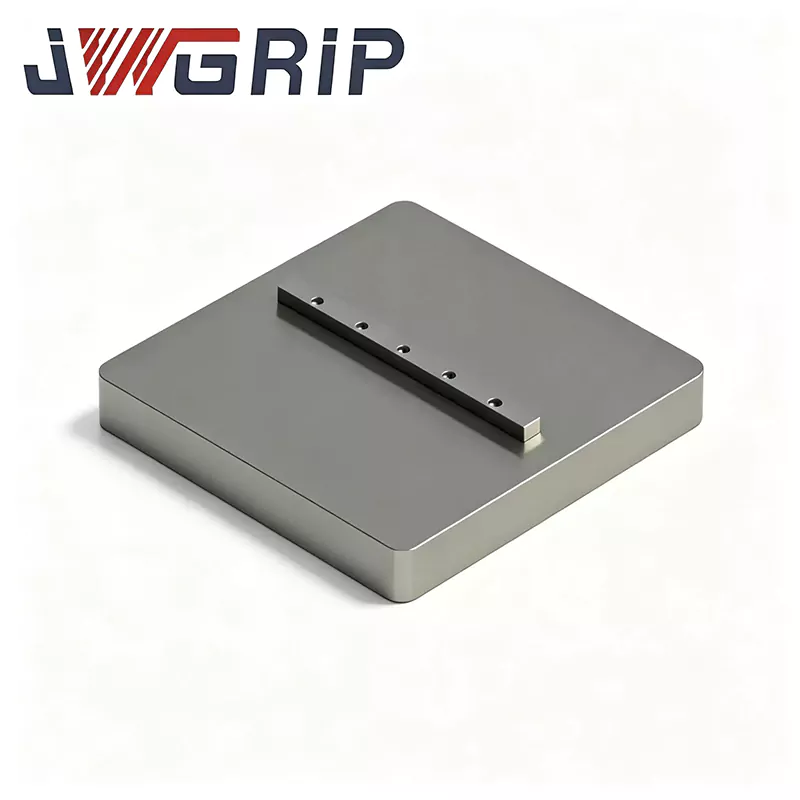
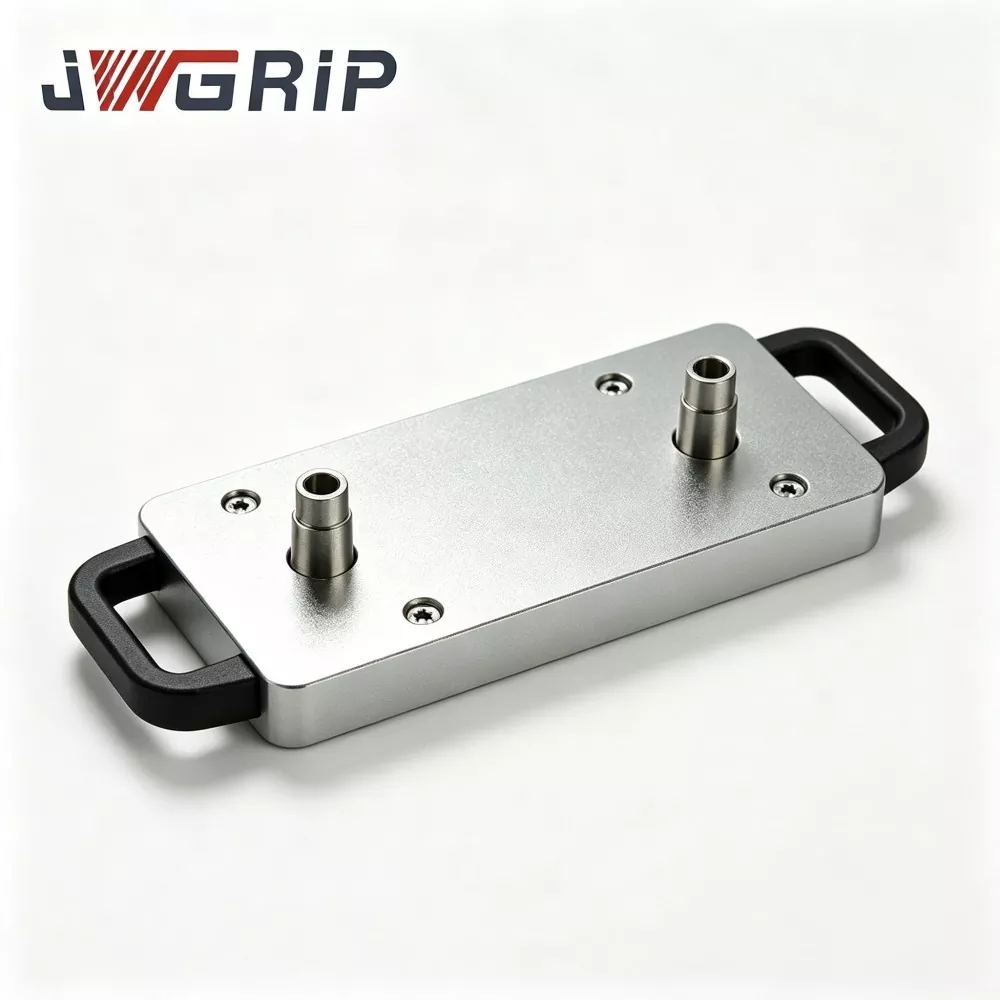
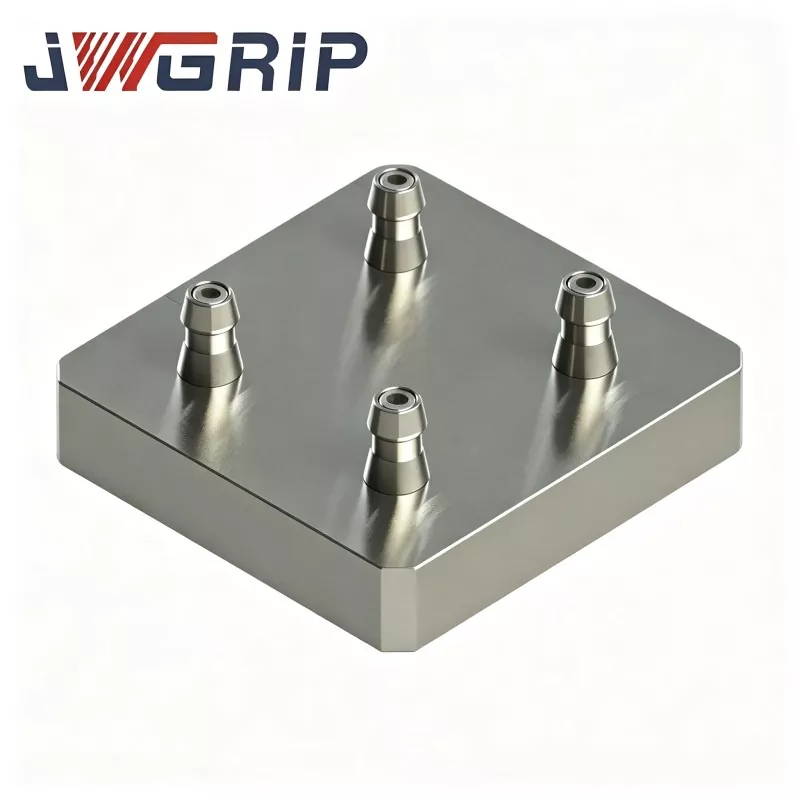
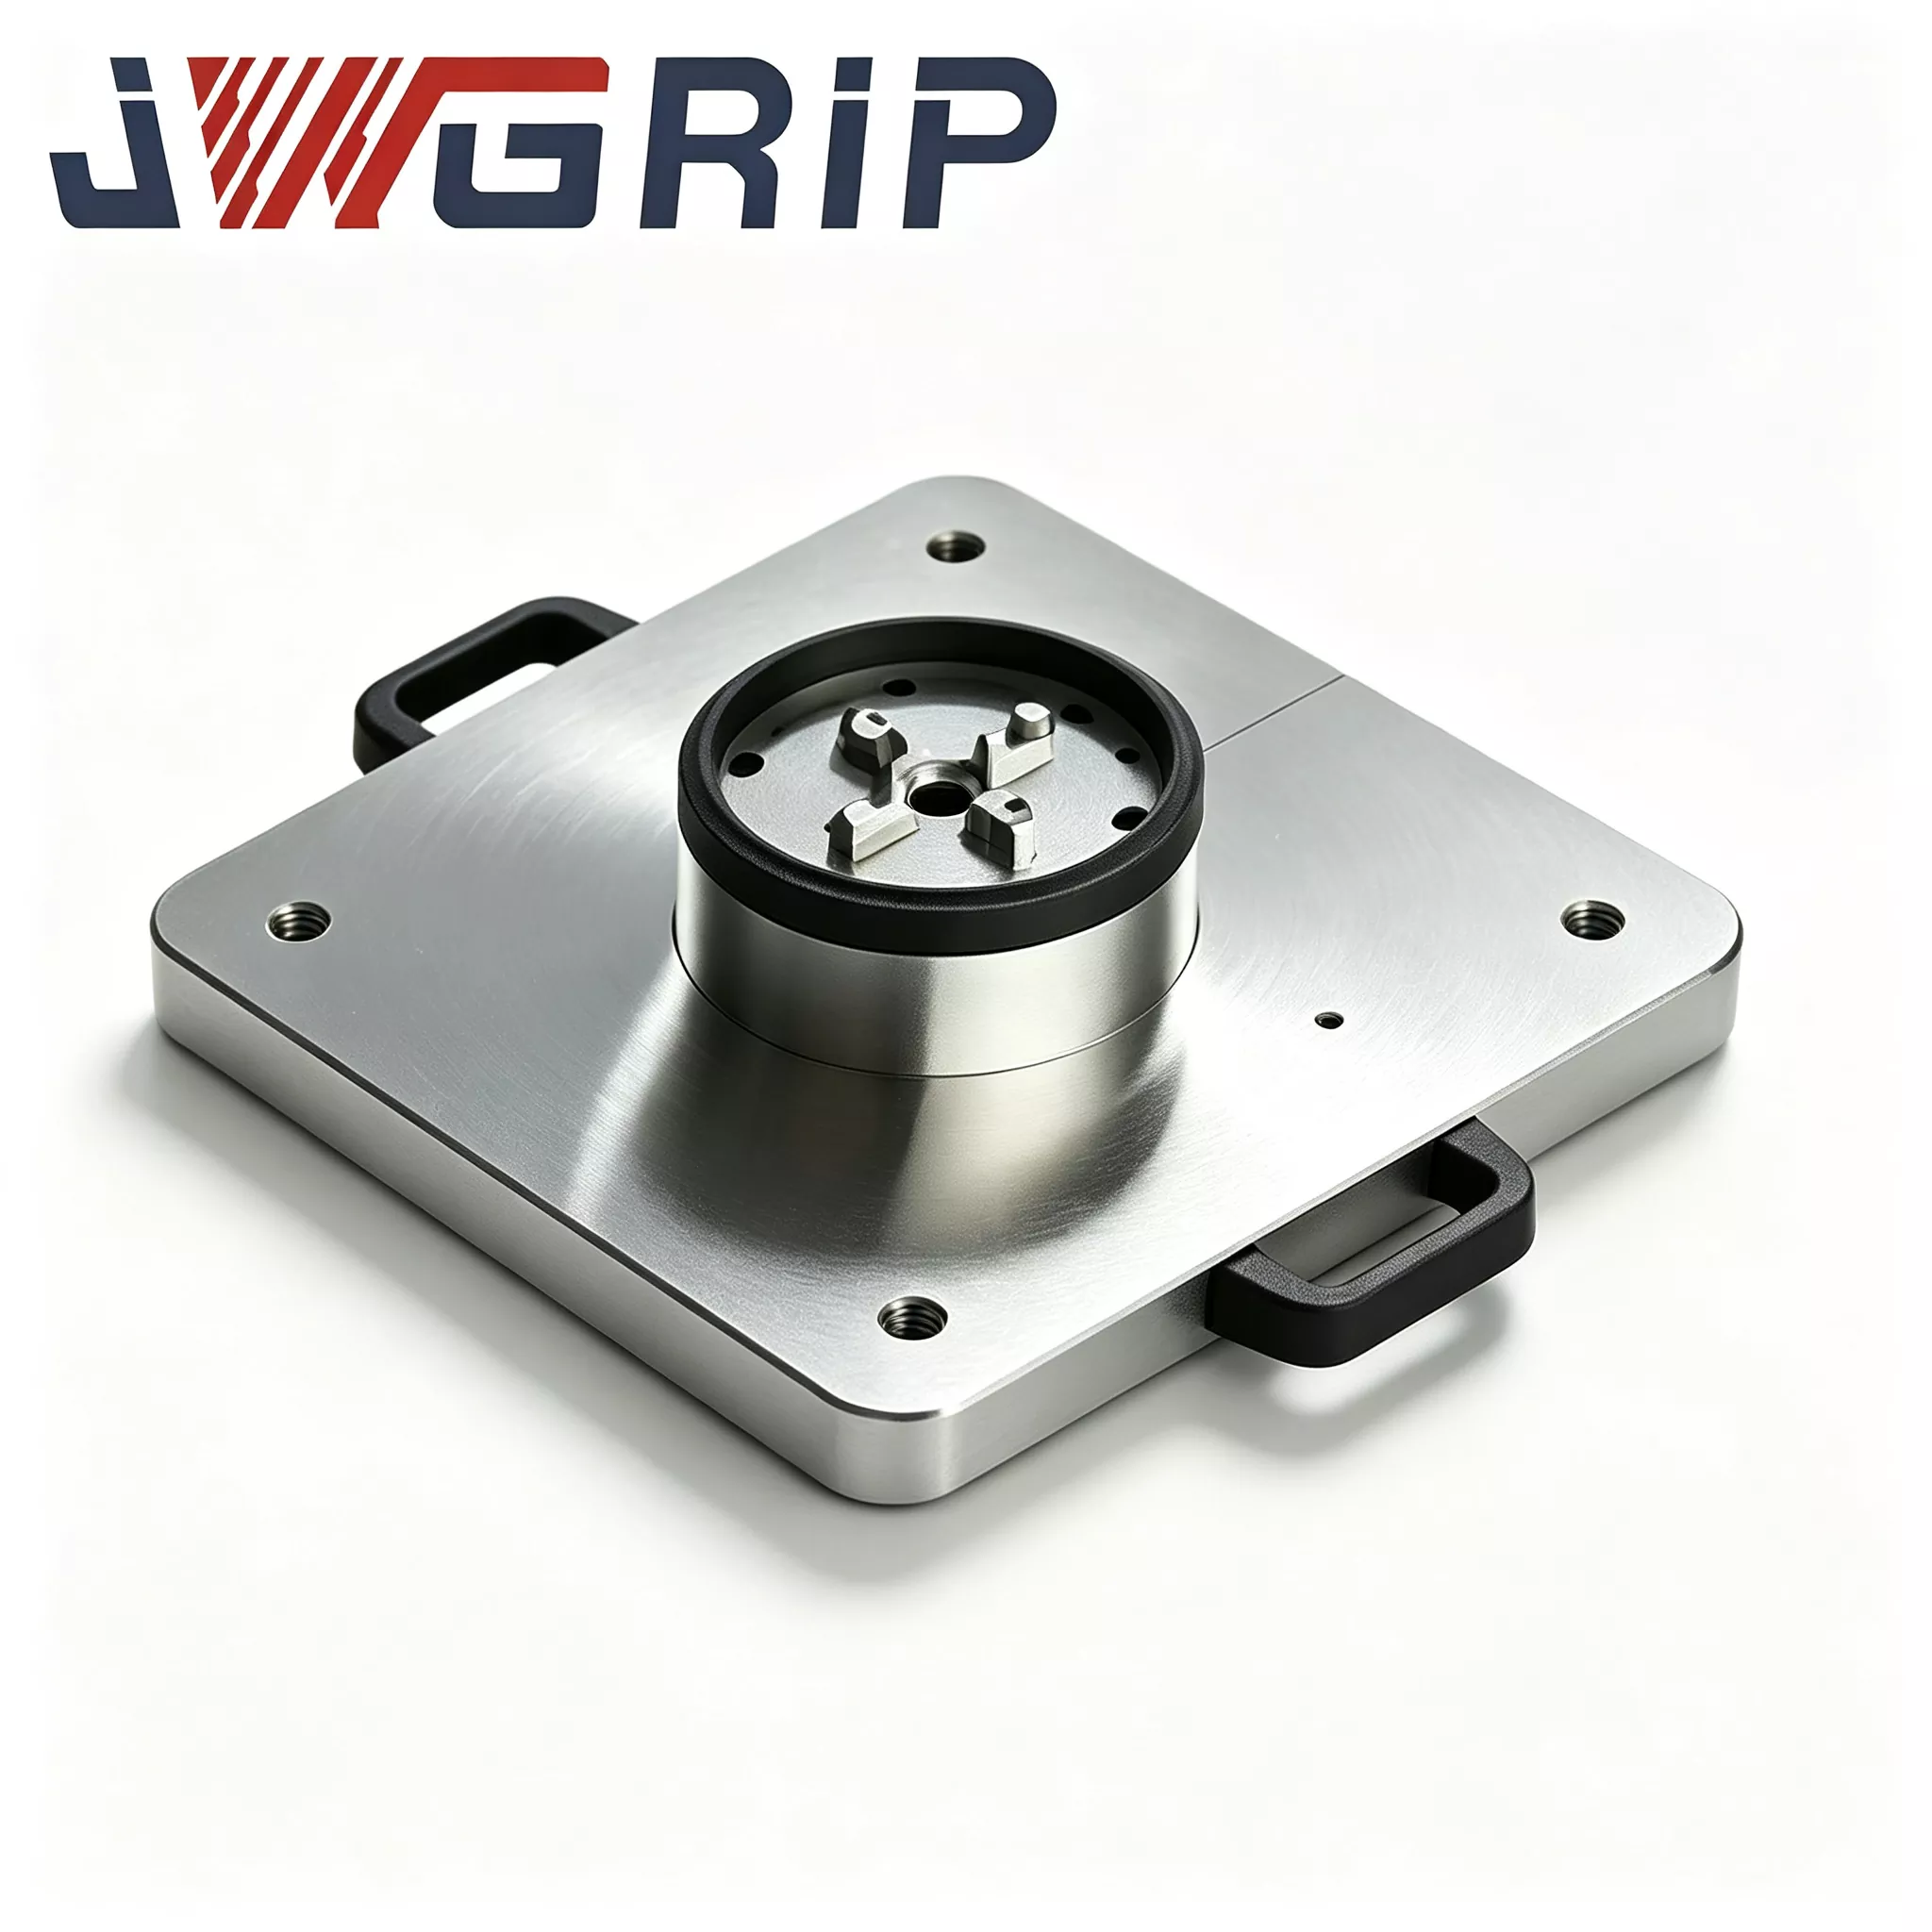
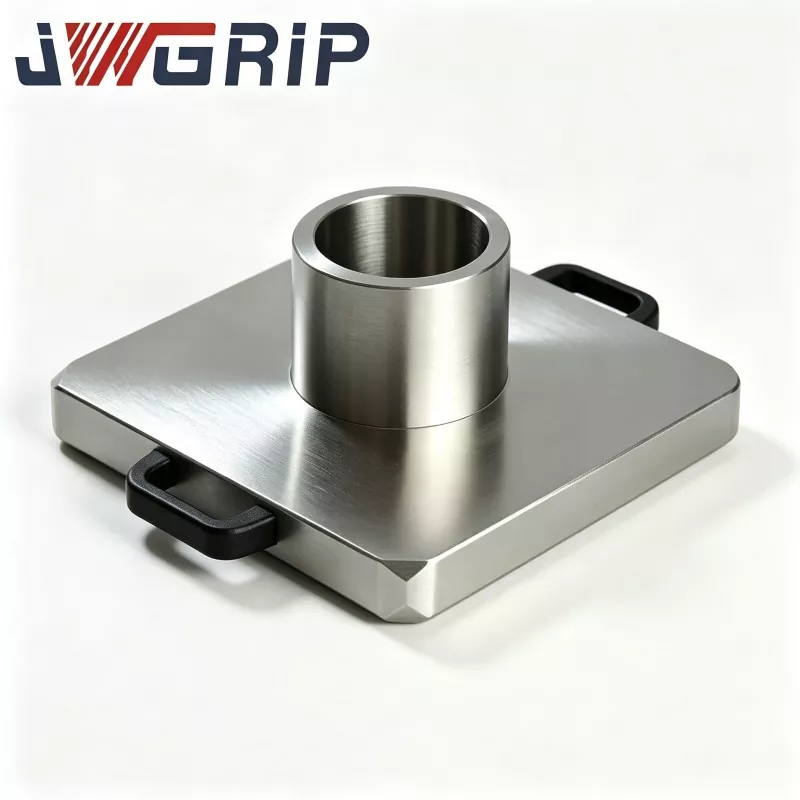
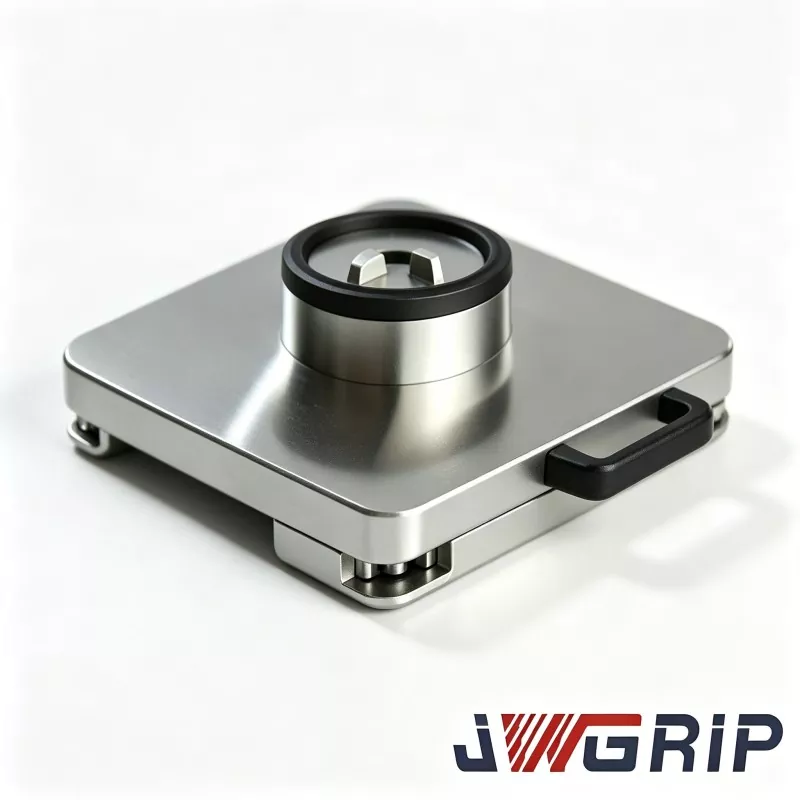
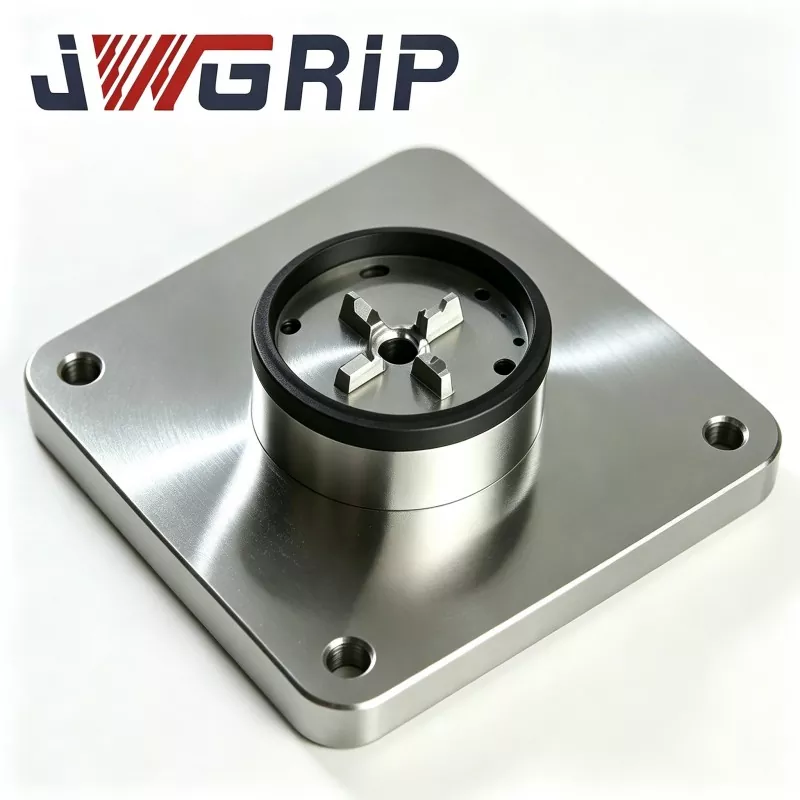
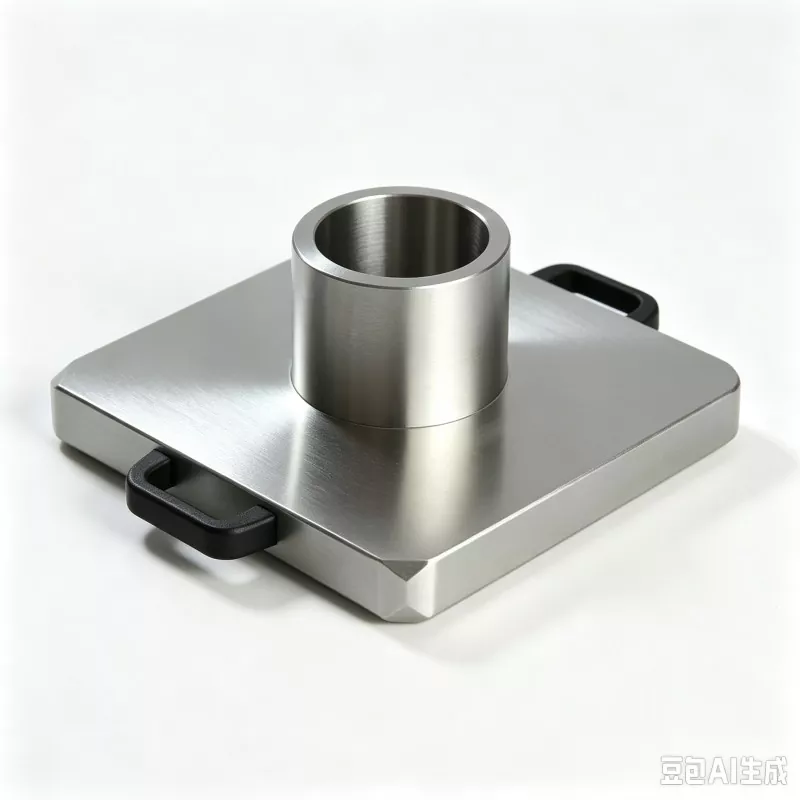
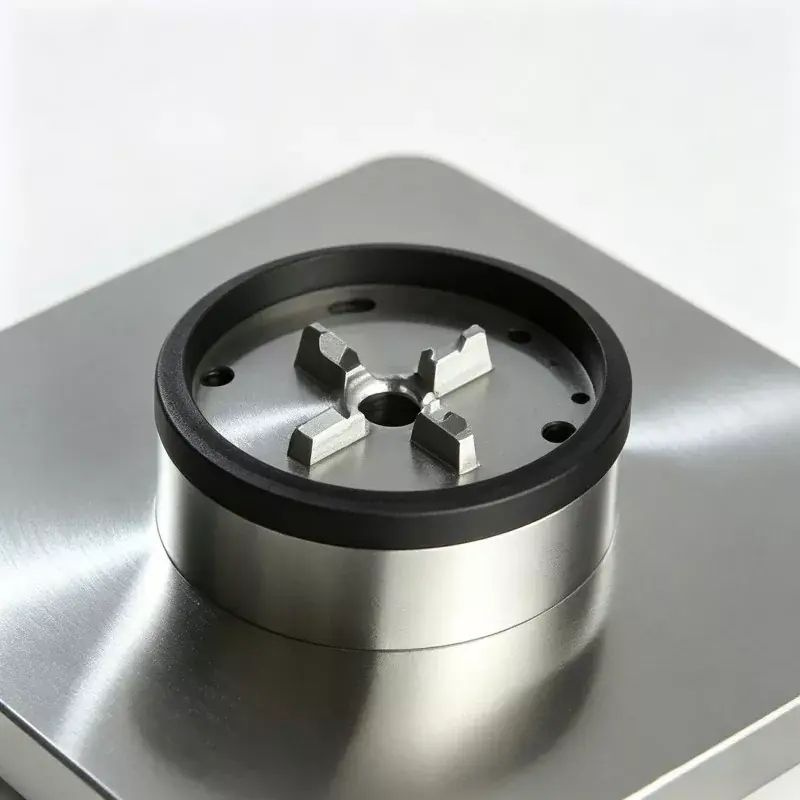
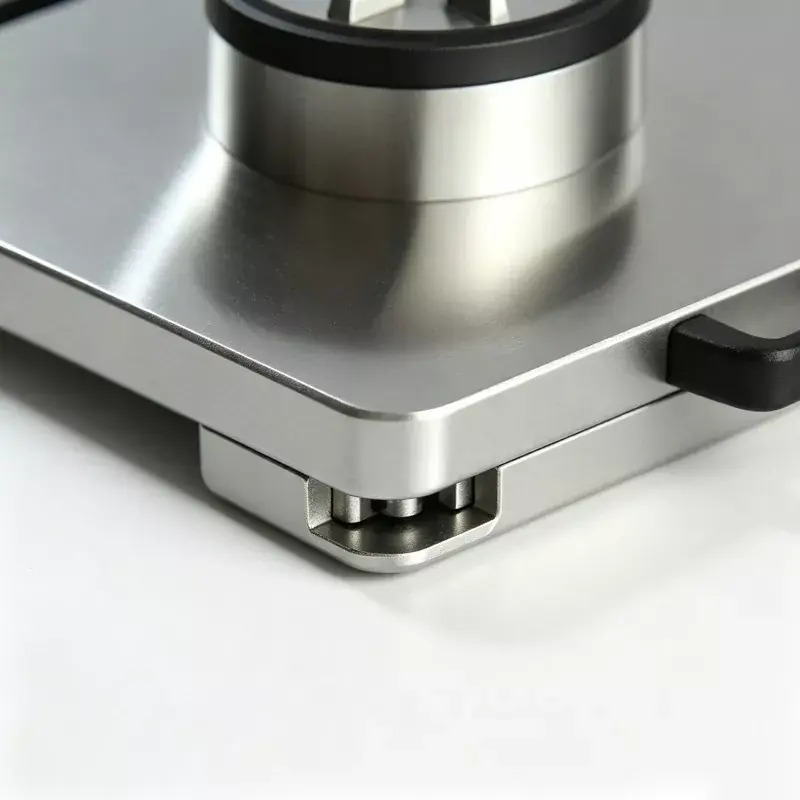
JWGRIP is the manufacturer and supplier of the Professional Automated Zero Point Pallet with Power Chuck in China. It is an integrated zero-point positioning fixture specifically designed for flexible unmanned CNC production lines. It integrates the zero-point positioning reference component and the power pneumatic chuck locking unit into a single device, eliminating the need to purchase additional multi-layer adapter plates or separate chuck attachments. It can be directly installed and fixed on the machine tool worktable and connected to industrial robot grippers.
The Automated Zero Point Pallet with Power Chuck can achieve automatic positioning, automatic clamping, and automatic release after the workpiece is clamped. It has been widely used in the processing of automotive aluminum alloy die-cast parts, large-scale production of metal structural components for 3C consumer electronics, and automatic graphite electrode processing units in mold workshops.
Product Composition and Work Flow
The Automated Zero Point Pallet with Power Chuck belongs to the Zero Point Pallet series. It is mainly composed of four core components: the pallet base body, the high-precision zero-point positioning sleeve assembly, the pneumatic drive module, and the synchronous power chuck fixture.
The complete work flow is as follows: The industrial robot picks up the fixture base of the loaded workpiece and places it on the reference plane of the pallet. The zero-point positioning sleeve completes the initial positioning. When the built-in sensor detects the position accurately, it sends a signal to the PLC control system.
The PLC starts the pneumatic circuit, and the built-in pneumatic unit drives the power chuck fixture to move synchronously inward, achieving uniform radial clamping of the fixture base.
After clamping is completed, an electrical confirmation signal is sent to the CNC machine tool, and the cutting processing cycle begins.
When the processing program ends, the machine tool sends a completion signal, and the pneumatic circuit releases the pressure. The chuck fixture synchronously opens, and the robot takes out the completed workpiece along with the fixture, preparing for the next cycle of loading.
The entire process does not require manual tightening of bolts or manual indication and alignment.
Process Advantages
The base plate blank is made of forged alloy steel and undergoes two complete stress-relieving heat treatment processes to eliminate the internal residual stress generated during the CNC machining process.
Many low-cost competitors will omit this crucial step. If the internal residual stress in the base material is significant, repeated clamping operations in the workshop and changes in temperature due to day-night cycles may cause microscopic deformations that are invisible to the naked eye on the reference benchmark plane.
This will lead to continuous size deviations in the machined workpieces and result in a large amount of waste loss.
Each piece of raw material in our factory strictly completes the complete annealing process. This standard is derived from over ten years of practical engineering experience and serves numerous CNC automated fixture projects. The positioning bushing is made of high wear-resistant bearing steel, undergoes quenching and tempering treatment, and is combined with internal hole fine grinding and ultra-fine processing to minimize the gap between the positioning surfaces and ensure stable positioning performance even after countless replacement cycles.
Core Advantages
1. Integrated One-Piece Structural Design
The integrated one-piece design saves mounting space on the machine tool worktable and eliminates accumulated assembly errors caused by multi-layer adapter plates. Traditional split-type solutions require stacking zero-point pallets, adapter base plates, and independent chucks, where stacking 2–3 plates can generate an extra 3–5μm of accumulated positioning deviation. Our monolithic integrated design avoids these error sources, reduces the number of purchased accessories, and lowers spare parts management costs for end customers.
2. Repeat Positioning Accuracy
The pallet delivers stable repeat positioning accuracy of ±2μm. Inner bores of positioning bushings are processed via honing super-finishing. Every pallet undergoes 100% full-item accuracy inspection before delivery, and each unit is shipped with a hard-copy original inspection report that can be supplied for verification upon overseas buyers' request.
3. Native Automation Integration
Standardized pneumatic ports and NPN electrical signal output interfaces are reserved, making the pallet compatible with multiple mainstream industrial robot brands on the market. It genuinely supports unattended night-shift production. According to real retrofit data from one domestic auto parts end-user, fixture changeover cycle time dropped from the original manual 12–15 minutes down to within 45 seconds after deploying our pallets, with no operator required to stay on-site during night shifts.
4. High Clamping Force Output
The built-in power pneumatic chuck unit supplies a maximum clamping force of up to 45kN, capable of withstanding cutting impact generated by heavy-feed machining of mold steel and cast-aluminum workpieces, effectively reducing the risk of fixture shifting and loosening during cutting operations.
5. Convenient Maintenance and Controllable Spare Part Cost
Chuck jaw assemblies can be disassembled and replaced individually without removing the entire pallet from the machine tool worktable. When jaws suffer abrasion or damage, customers only need to purchase corresponding spare parts rather than replacing the entire pallet set, effectively reducing long-term equipment maintenance investment.
Real Customer Cases
The Automated Zero Point Pallet with Power Chuck is mostly applied in three categories of production lines: unmanned-CNC production lines for automotive components, mass-production lines for 3C metal structural parts, and flexible automated graphite-electrode machining cells inside mold factories.
Case 1: One large-scale domestic auto-parts manufacturer retrofitted two flexible CNC automated production lines with total 16 sets of Automated Zero Point Pallet with Power Chuck for aluminum die-casting machining. Before retrofit, operators needed manual indicating and alignment for every fixture change-over, consuming roughly 13 minutes per batch. After deployment of our zero-point automated pallets, robot completes all loading-unloading, positioning and clamping work. Single change-over cycle shortens to 42-50 seconds. Unattended night-shift is realized. According to three-month continuous production statistics, monthly workshop-level production capacity rises by 22 percent. Dimensional consistency across workpiece batches improves obviously and reject-scrap rate drops significantly.
Case 2: One large-scale mold-making enterprise located in Pearl River Delta installs multiple sets of this automated pallet inside graphite-electrode automated-machining cells. All electrode bases adopt unified standard dimensions. Operators no longer repeat manual indicating for every electrode-machining task. Dimensional consistency of finished electrodes improves greatly and repetitive labor intensity for mold-shop staff decreases. Suggested image positions: on-site photos taken inside our own processing workshop, real-shot pictures of customer-site automation workstation, exploded-view detail photos of pallet body, photos captured during factory-outlet accuracy-QC inspection.
Manufacturing Process
All automated pallets go through full-flow production including forging, CNC machining, heat-treatment, grinding and assembly within our in-house CNC-fixture workshop. No complete-unit OEM outsourcing is adopted.
Complete production workflow:
alloy-steel blank forging → rough machining → first stress-relief aging → semi-finishing → secondary stress-relief aging → super-precision grinding → bushing press-fitting → general assembly → multi-item accuracy-&-performance inspection → air-tightness pressure test → anti-rust protection → export-grade packing.
Quality Control & Certifications
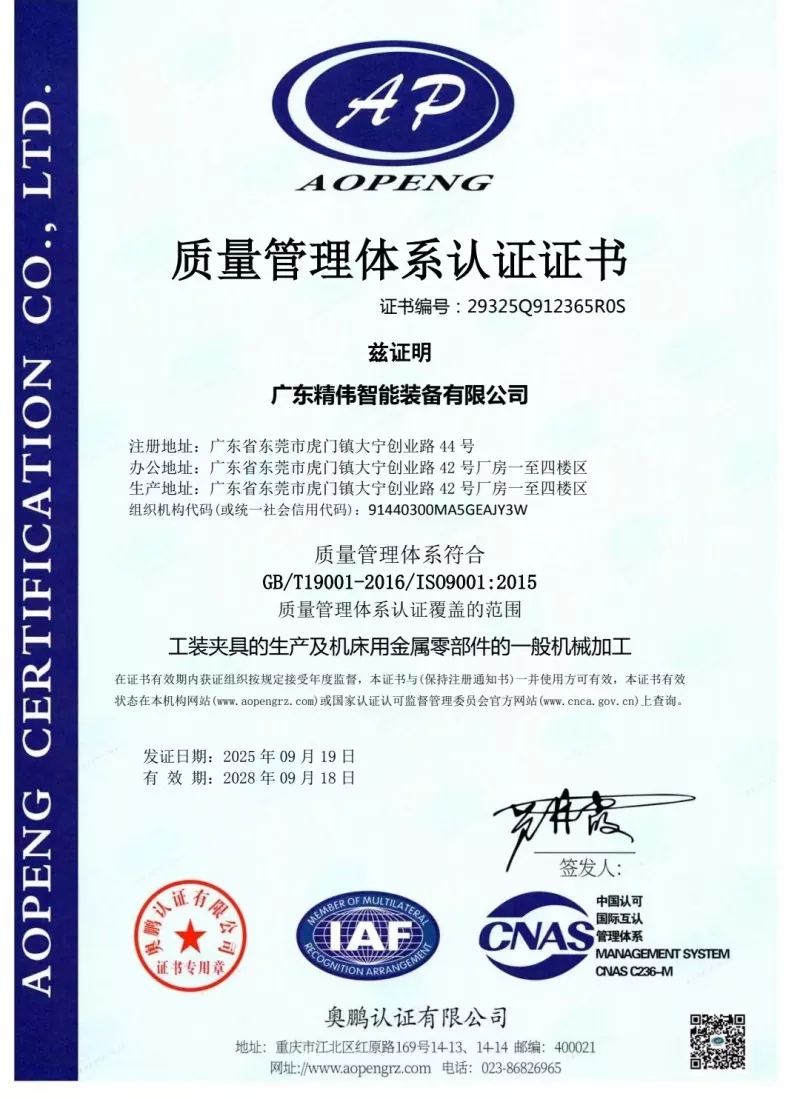
Mandatory pre-delivery inspection items for every unit: repeat-positioning-accuracy test, actual chuck-clamping-force measurement, air-tightness pressure-holding test (max. allowable pressure drop ≤0.02 MPa within 5-minute holding duration), electrical-signal-logic integrity test. Each unit is delivered with unique factory-inspection data sheet. Our factory holds ISO 9001 quality-management-system certification. Material certificates are available for key metal components. Third-party laboratory inspection designated by customers is acceptable.
Selection Guide
Firstly, confirm actual outer dimension of customer-site fixture carrier to match pallet clamping-range specification.
Secondly, check workshop air-source condition. Compressed-air pressure must stably stay within 0.5-0.7 MPa. If air-source pressure fluctuates heavily, pressure-regulating filter triple assembly is strongly recommended.
Thirdly, for automation-project procurement, clarify IO communication protocol between robot and PLC control system. We supply complete electrical-interface-documentation free-of-charge.
Fourthly, provide maximum workpiece weight if heavy workpieces are processed. Our technical staff will conduct assessment and judge whether reinforced customized-version pallet is required.
Installation, Commissioning & Operation Notes
While mounting pallet onto machine-tool worktable, fasten bolts strictly following torque values specified in manual. Violent over-torque tightening is forbidden to avoid pallet-body deformation. Oil-water filter must be installed at front-end of compressed-air inlet to prevent moisture and metal debris from entering chuck and causing internal-component rusting or jaw jamming. Every 80-100 cumulative working hours, spray dry-lubricant spray onto sliding friction surfaces inside chuck.
Liquid engine oil is prohibited, as liquid oil attracts massive aluminum and iron chips and triggers jaw-jamming failures. During production, avoid heavy chip accumulation on pallet reference datum plane. Operators must blow and clean locating holes and datum planes with compressed-air at every shift change. Never run unit exceeding maximum clamping-force listed on specification sheet. Overload operation causes permanent plastic deformation of chuck jaws and permanently destroys pallet positioning accuracy.
Packing, Lead Time & After-sales Service
Export-grade shock-proof solid-wood packing cases with thick foam inner buffer protection are adopted to safeguard precision datum surfaces against collision damage during long-distance ocean-shipping transportation. Standard lead-time: 12-18 working days. Certain standard items are kept in-stock for shorter delivery.
12-month full-unit warranty covers manufacturing defects not induced by human mis-operation; free repair or spare-part replacement is provided. Remote online technical-guidance for installation and commissioning is available. Paid on-site-commissioning service can be offered for bulk-order projects.
Customized modification service is supported, including clamping-range adjustment, pneumatic-circuit layout alteration and signal-output-form change. Free sample is available for customer evaluation test; freight cost for samples shall be undertaken by buyers.
FAQ
Q1: Can Automated Zero Point Pallet with Power Chuck be compatible with zero-point fixtures from other third-party brands?
A: Datum dimension of standard-version matches our native zero-point system. If compatibility with other-brand zero-point fixtures is required for your project, notify technical requirement before order placement, customized datum-dimension machining can be realized.
Q2: Will unstable air-source pressure influence clamping safety and reliability?
A: It will bring direct impact. Insufficient air-source pressure reduces actual chuck clamping force and creates workpiece-loosening risk during cutting. Pressure-regulating filter assembly is strongly suggested to stabilize pressure within 0.5-0.7 MPa.
Q3: What are primary causes for degraded repeat-positioning accuracy after long-time operation?
A: Three frequent root-causes: first, chip contaminants accumulated on reference locating surfaces; second, normal wear of internal sliding components; third, pallet-body deformation caused by external heavy impact. Prioritize cleaning and maintenance. Worn-out components can be replaced by separate spare-parts instead of full-pallet renewal.
Q4: Can this pallet be applied on 5-axis CNC machine tools?
A: It is compatible with 5-axis machines. Total assembled fixture height must be calculated to prevent collision during 5-axis spindle tilting. Supply machine-tool model at selection phase and we will assess interference risk for you.
Hot Tags: Automated Zero Point Pallet with Power Chuck Supplier, Manufacturer, Wholesale
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.