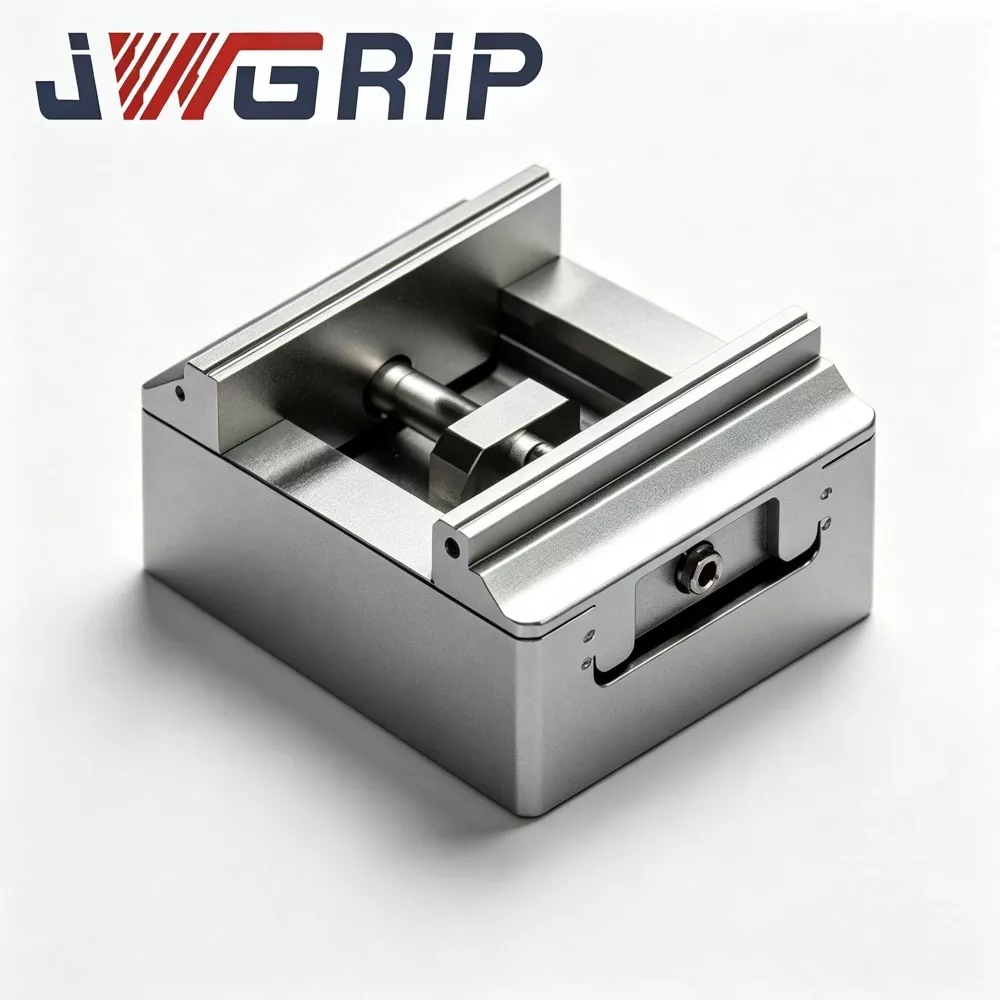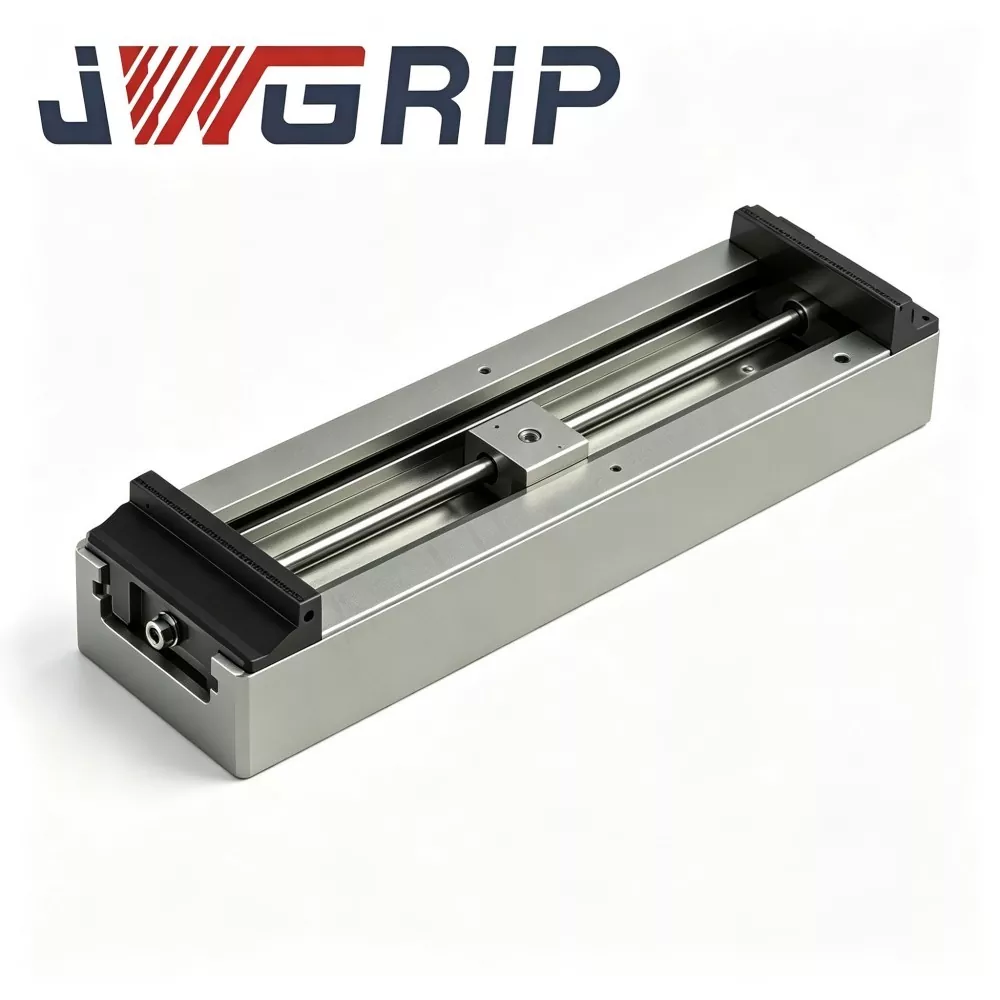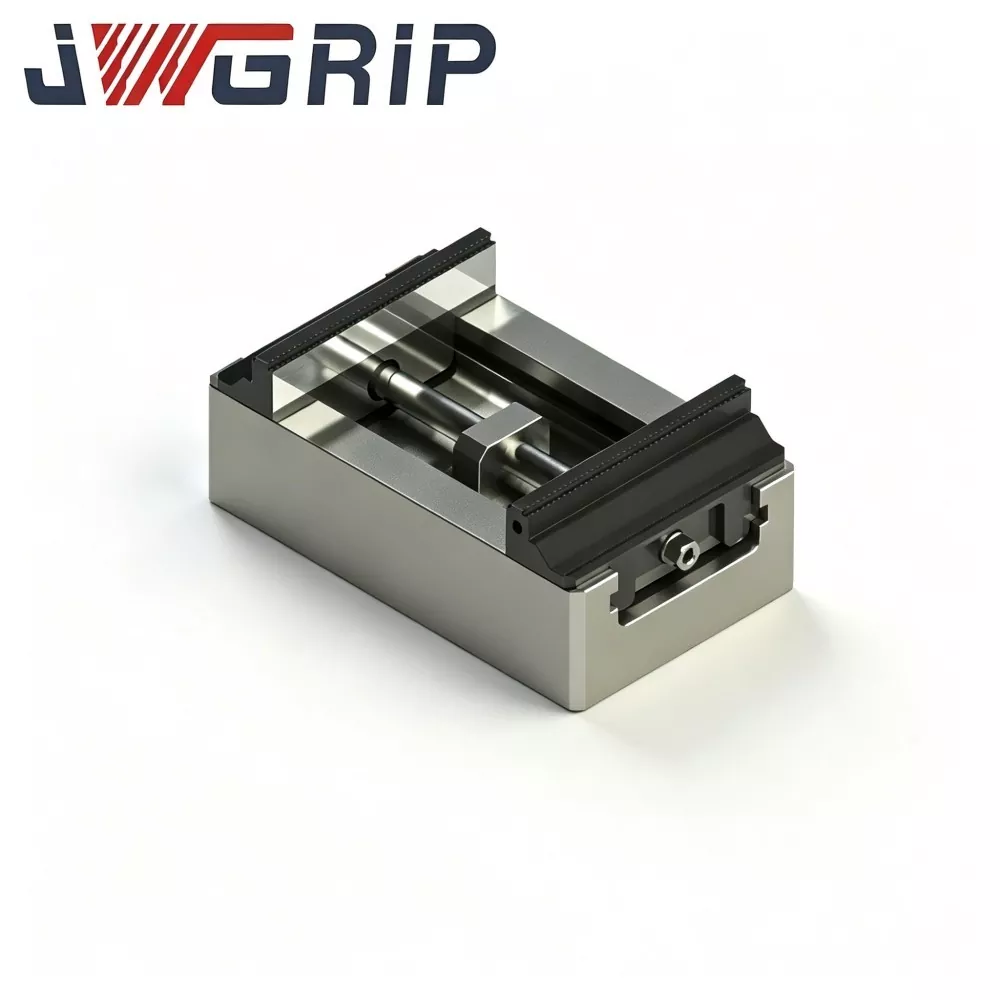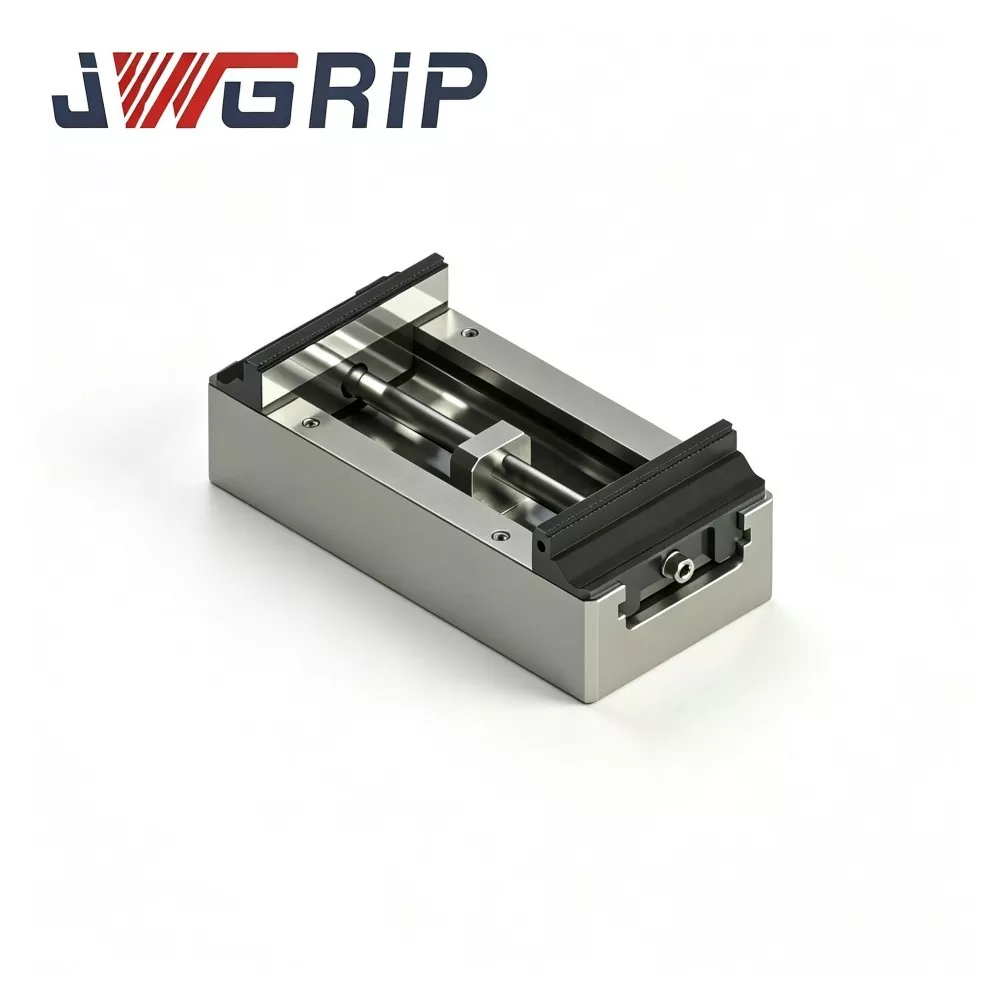
Extended Travel Heavy-Duty Self-Centering Zero Point Vise with Hard Jaws
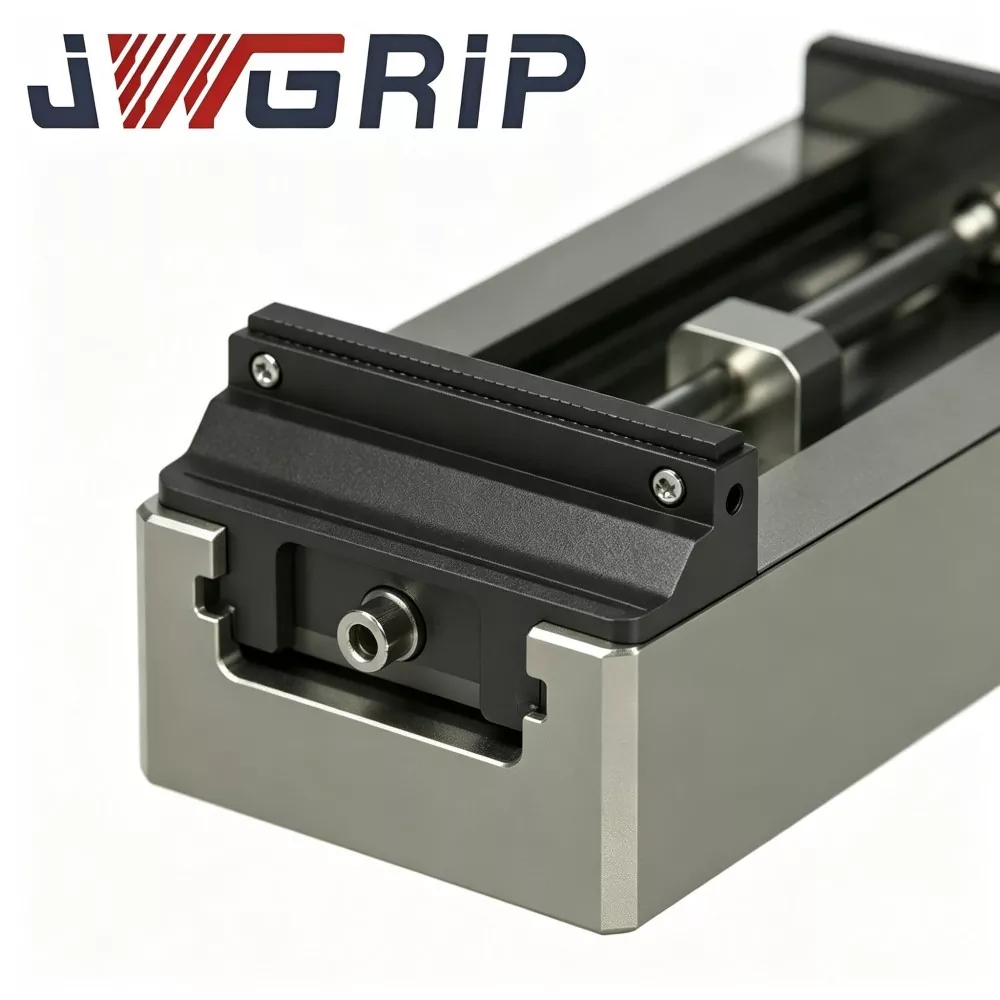
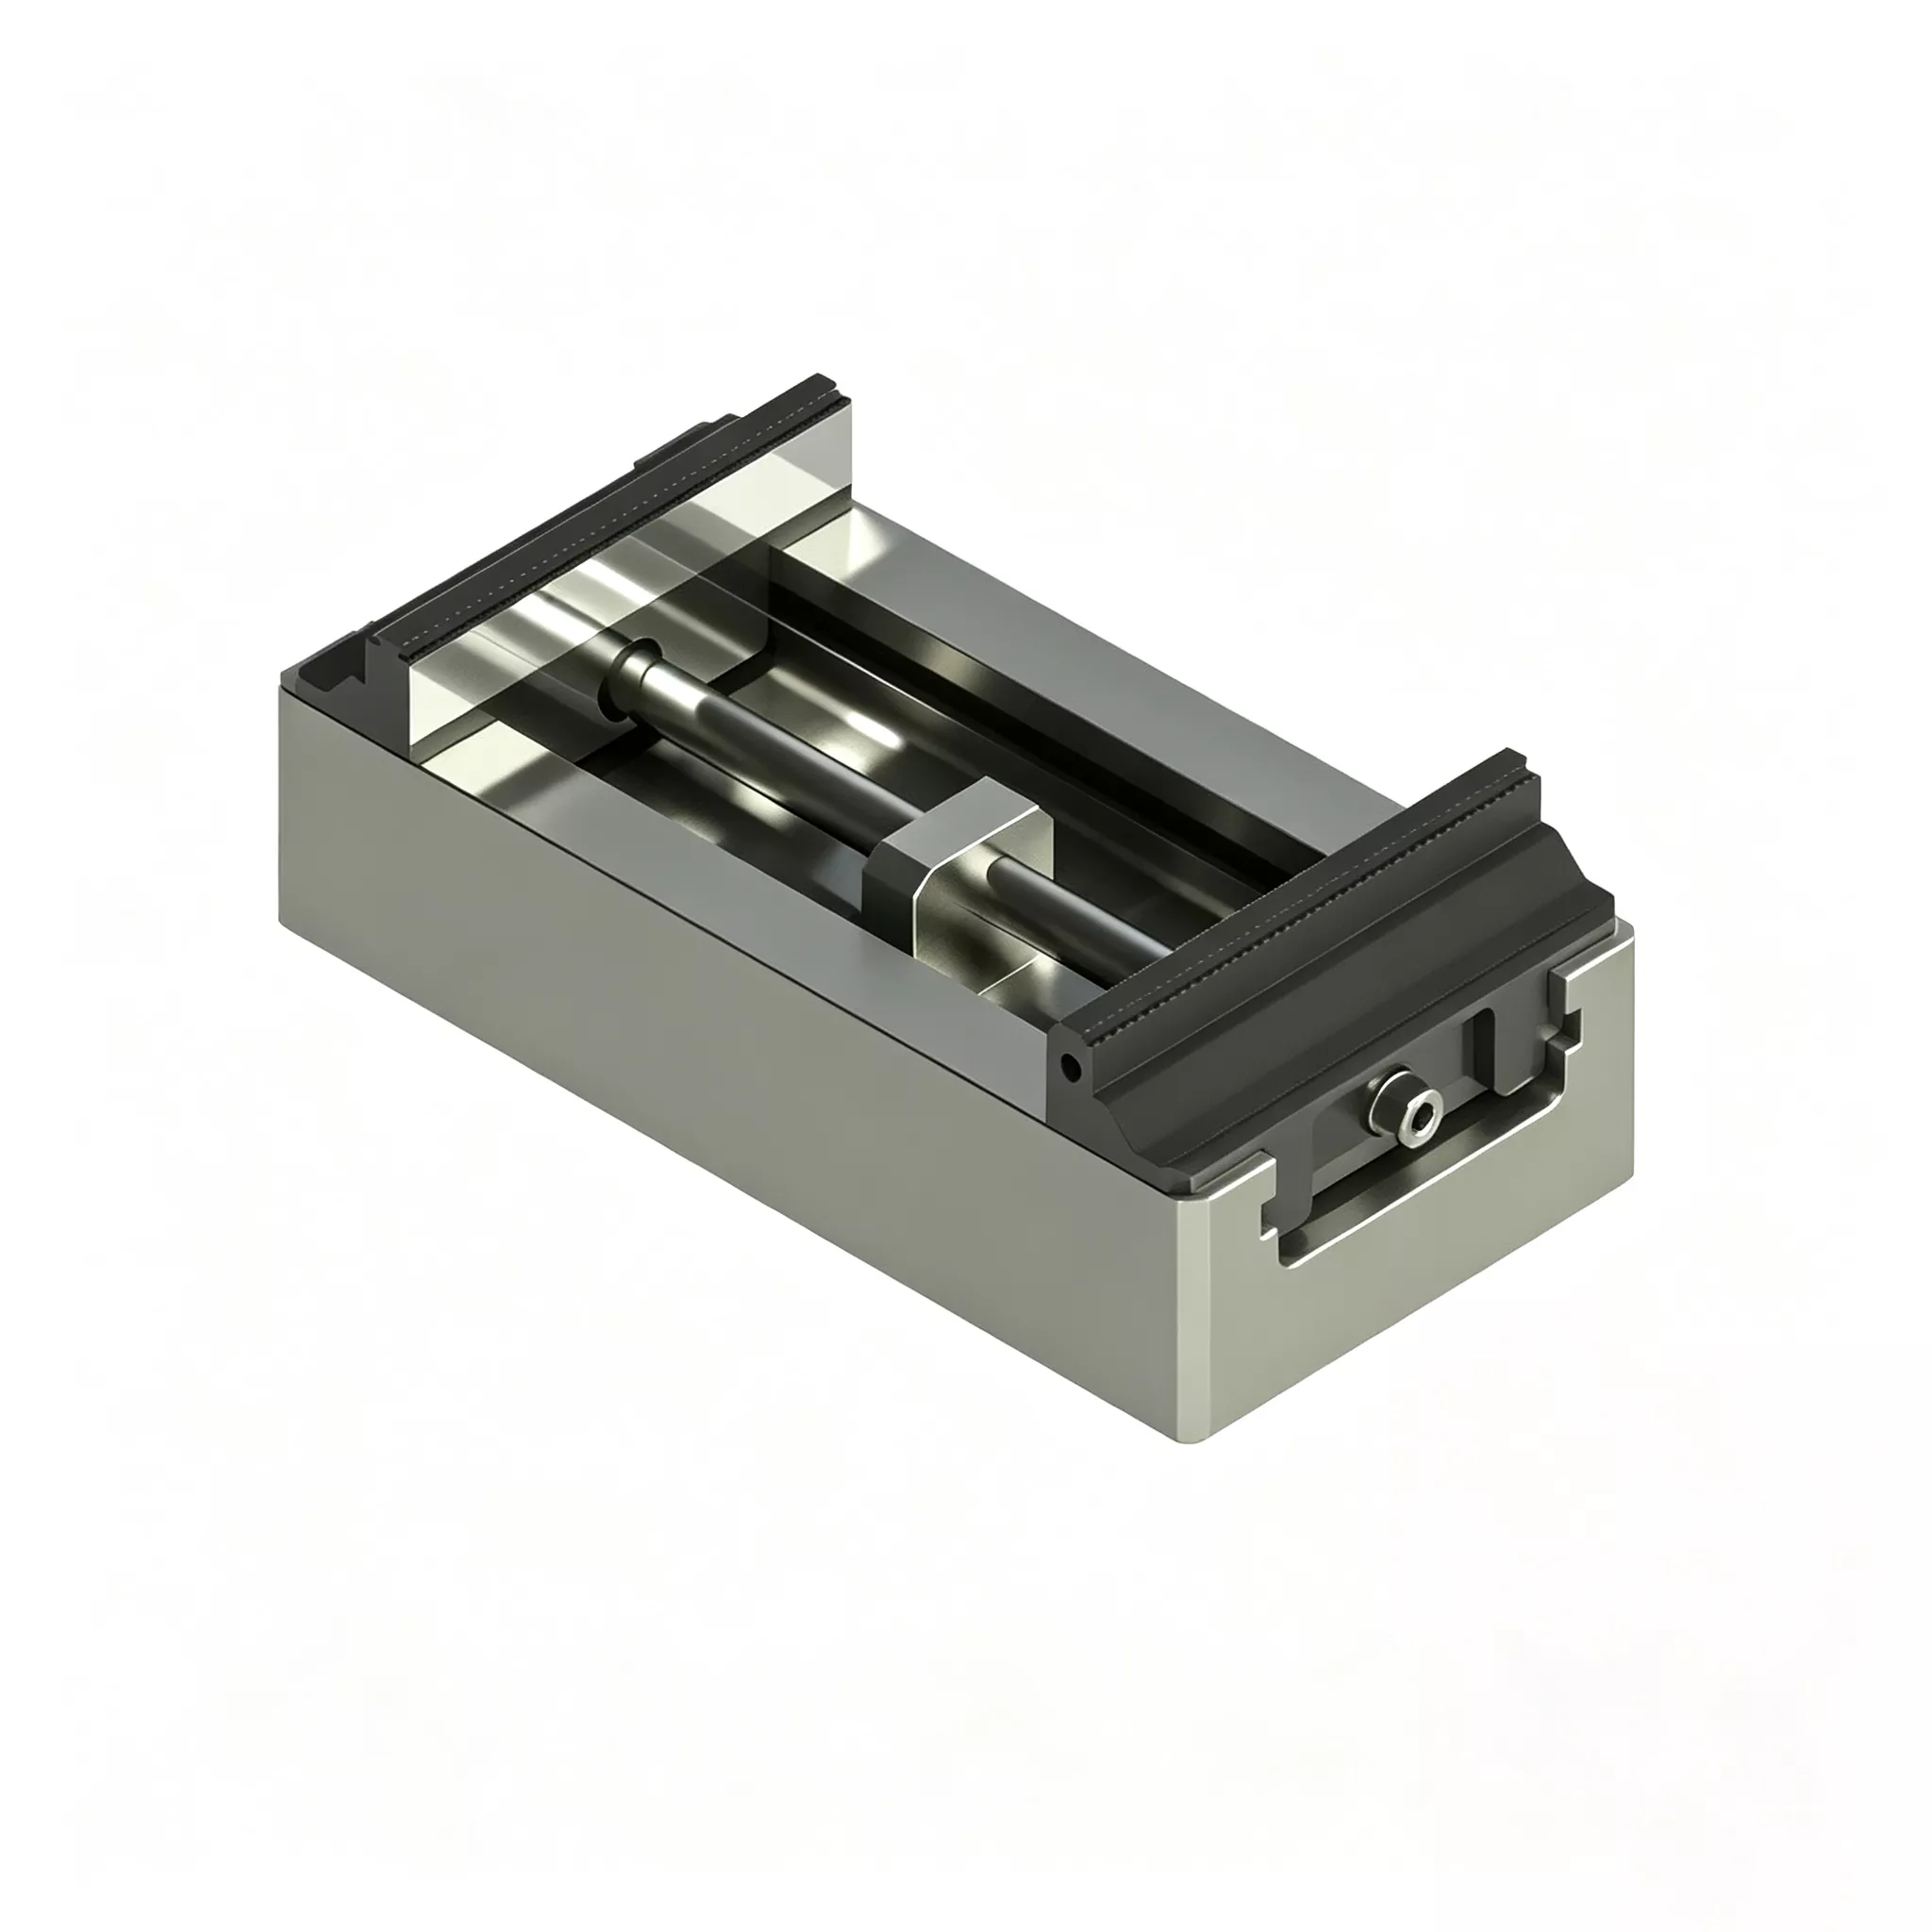
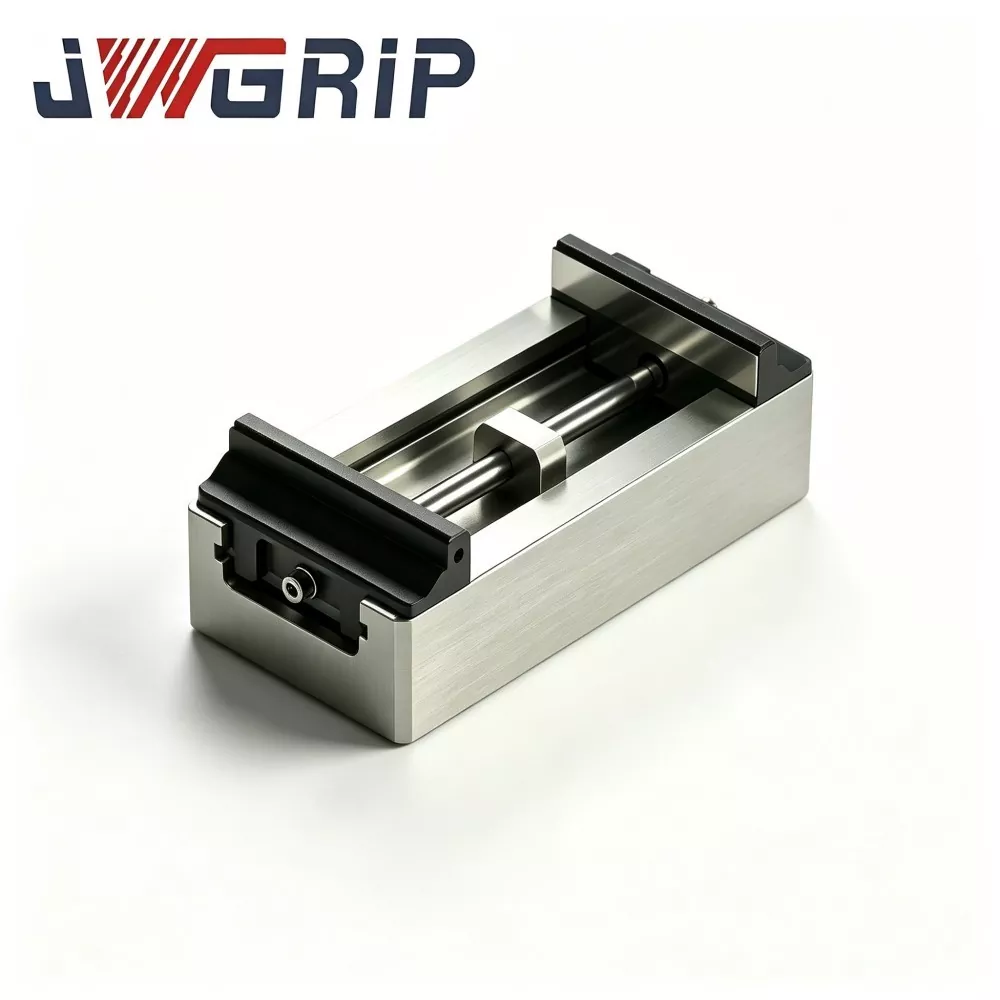
JWGRIP is the professional manufacturer and supplier of Factory Direct Extended Travel Heavy-Duty Self-Centering Zero Point Vise with Hard Jaws in China, with standard products fully in Stock for rapid global delivery. It is a newly upgraded integrated zero-point positioning clamping fixture specially designed for vertical CNC machining centers, 4-axis and 5-axis linkage processing equipment. Adopting brand-new structural craftsmanship and manufactured in strict accordance with high-grade industrial standards, the fixture integrates optimized long-travel transmission structure and standard zero-point quick-change docking unit as a complete integrated device.
Featuring upgraded structural optimization and high-strength alloy steel construction, this heavy-duty long-travel zero point vise delivers outstanding mechanical stability, efficient machining adaptability, ultra-long service life and easy daily maintenance. All main body and internal transmission components undergo professional stress-relief aging treatment and precision grinding processing to ensure excellent structural rigidity and clamping stability under heavy-load rough milling conditions. The optimized internal transmission layout achieves an extended effective clamping range, perfectly adapting to the processing of large-size blanks and irregular workpieces.
Equipped with a built-in integrated zero-point quick-change interface, Extended Travel Heavy-Duty Self-Centering Zero Point Vise with Hard Jaws support efficient offline workpiece presetting and fast fixture swapping, greatly improving workshop production efficiency and repeat positioning accuracy. Widely applicable to mold manufacturing, auto parts, aerospace components, new energy structural parts and general hardware processing fields, this high-quality Made-in-China fixture provides standardized, stable and reliable precision clamping solutions for global industrial manufacturing enterprises.
Limitations:
● Short clamping travel forces frequent fixture change-over or auxiliary block adding when processing large-size blanks.
●Insufficient structural rigidity under heavy-load rough-milling triggers tiny workpiece offset and inconsistent dimensional tolerances.
●Poor-matched zero-point docking leads to low repeat-positioning accuracy and time-consuming manual dial-indicator alignment.
JWGRIP extended-travel heavy-duty self-centering zero-point vise optimizes inner transmission layout to achieve longer effective clamping range.
●Main body and transmission components adopt high-strength alloy steel, completed with in-house stress-relief aging and precision grinding
●Integrated zero-point quick-change interface supports offline presetting and rapid fixture swap
Extended Travel Heavy-Duty Self-Centering Zero Point Vise with Hard Jaws solves classic pain-points of traditional vises: insufficient clamping stroke, weak clamping rigidity, workpiece shifting under heavy loads, poor zero-point positioning performance and limited adaptability for irregular-shape workpieces.
Widely deployed for mold manufacturing, auto-parts, aerospace components, new-energy structural parts and general-hardware processing. It delivers reliable standardized fixture solutions for global industrial manufacturers.
Production Bottlenecks
1. Limited clamping travel requires secondary clamping for long-size and large-format workpieces, which brings unavoidable re-positioning errors.
2. Many ordinary extended-travel vises adopt lightweight construction. Micro-deformation and workpiece vibration occur under heavy cutting loads, generating tool chatter marks and out-of-spec dimensions.
3. Most off-the-shelf vises have no built-in zero-point positioning structure. Time-intensive manual calibration is required for every fixture swap and greatly lowers machine-tool utilization rate.
4. Deficient sealing allows cutting fluid and metal chips to penetrate inner transmission assemblies, resulting in mechanical jamming, accuracy decay and shortened fixture service life.
JWGRIP Extended-Travel Heavy-Duty Self-Centering Zero-Point Vise with Hard Jaws targets all above-mentioned bottlenecks via four core design measures: extended clamping-stroke design, heavy-duty reinforced vise body, integrated zero-point positioning interface and full-enclosed protective sealing structure.
Module Composition
JWGRIP extended-travel heavy-duty self-centering zero-point vise consists of six core functional modules:
· Stress-relieved heavy-duty vise body
· Extended-travel synchronous rack-and-pinion transmission assembly
· Quenched wear-resistant hard-jaw set
· Integrated zero-point positioning base
· Full-enclosed sealing & protection system
· Precision locking fine-tuning mechanism
Inner Operating Principle
The vise body is integrally forged alloy-steel and undergoes multi-round stress-relieving treatments to eliminate built-in structural stress. It resists deformation under long-term heavy-cutting impact.
High-precision rack-and-pinion synchronous transmission delivers fully symmetrical synchronized opening-closing motion for two hard jaws. Automatic workpiece centering removes manual positioning errors. Stable clamping datum is maintained even for long-size and irregular-shaped blanks.
Fully-quenched hard-jaws feature high hardness, outstanding wear-resistance and strong clamping friction force. They firmly grip steel, cast-iron and other hard workpieces and prevent sliding and vibration during heavy-duty milling.
The bottom-integrated zero-point positioning interface is fully compatible with mainstream industrial zero-point systems. Extended Travel Heavy-Duty Self-Centering Zero Point Vise with Hard Jaws enables fast fixture swap and repeat positioning without repeated manual calibration, greatly boosting efficiency for high-mix fast-iteration production. Independent positioning-clamping architecture balances quick-change performance and heavy-cutting mechanical rigidity.
Core Technical Strengths
1.Expanded Effective Clamping Travel
Much-enlarged clamping stroke adapts to long-profile parts, large frame-shaped workpieces and irregular structural components. Secondary clamping operations are avoided, and repeated-clamping-induced machining errors are eliminated.
2.Heavy-Duty Forged-Body Rigidity
Integrally forged high-strength steel body plus complete stress-relieving process resists deformation and vibration under powerful cutting force. It supports combined heavy rough-milling and high-precision finish-milling within one fixture.
3.Fully-Quenched Replaceable Hard-Jaw Performance
Precision-ground and full-quenched hard-jaws deliver excellent wear-resistance and impact-resistance. Long-term clamping accuracy is sustained, and frequent jaw maintenance is reduced. Hard-jaws can be replaced separately without discarding the whole vise.
4.Built-In Zero-Point Fast-Positioning Interface
Native standard zero-point docking enables fast fixture swap and repeat positioning. It saves over 80 % of fixture setup-and-debug time and maximizes CNC machine-tool output capacity.
5.Full-Enclosed Contaminant-Isolation Protection
Totally-sealed inner cavities isolate cutting fluid, metal chips and workshop dust. Inner transmission parts are protected against corrosion and jamming, significantly extending the whole-service life of the vise.
6.Wide-Range Equipment Compatibility
Optimized outer-dimension layout fits vertical CNC machining centers, 4-axis and 5-axis linkage machines. It covers most typical precision-milling, drilling and boring application scenarios.
Installation & Commissioning Procedures
1.Clean machine-tool worktable surface and vise-base positioning reference surface thoroughly before mounting. Remove chips, coolant residues and oil contamination. Foreign particles will tilt the vise and cause dimensional deviations.
2.Align zero-point positioning interfaces, place the vise properly and tighten fixing bolts according to torque values stated in the official manual. Make sure the vise sits firmly without shaking.
3.Adjust clamping force properly according to workpiece material and processing technology. Avoid excessive clamping force that may deform thin-wall workpieces.
4.Perform idle-stroke test and trial-cut validation. Simulate actual machining movement and confirm no workpiece shifting or vibration before starting formal batch-production runs.
5.When integrated with robot-automation systems, calibrate robot grabbing center against vise centering center to prevent mechanical collision.
Maintenance Regimen
1.Clean jaw clamping surfaces and sweep away chips and processing residues immediately after each machining shift.
2.Lubricate inner synchronous transmission assemblies on a regular schedule to keep jaw opening-closing smooth.
3.Carry out positioning-accuracy calibration every quarter.
4.Replace worn-out hard-jaws independently when performance degrades; the modular design removes the necessity of replacing the complete vise unit.
5.Protect vise-base datum surfaces from impact and scratches during handling and storage. Apply anti-rust coating for long-term idle storage.
Issue Diagnosis & Resolution
Symptom 1: Workpiece dimensional deviation after cutting
Troubleshooting: Insufficient clamping force; transmission lacking lubrication; hard-jaw wear; loose base bolts
Solution: Adjust clamping force; replenish lubricant; grind or replace worn hard-jaws; retighten base bolts to standard torque.
Symptom 2: Jaw jamming and unsmooth movement
Troubleshooting: Chips / coolant penetrate sealing cavity; insufficient grease supply; internal transmission-part wear
Solution: Disassemble and clear internal contaminants; add lubricating grease; inspect and swap heavily worn components.
Symptom 3: Poor repeat-positioning accuracy after vise re-mounting
Troubleshooting: Dirty zero-point contact faces; locating-pin wear; incomplete base locking
Solution: Fully clean zero-point mating surfaces; replace worn locating-pins; re-torque vise-base fixing bolts.
Symptom 4: Workpiece shift under heavy-load rough-milling
Troubleshooting: Inadequate locking torque; chip debris stuck on jaw contact faces
Solution: Increase locking torque moderately; thoroughly clean hard-jaw clamping surfaces.
Packaging & Shipment Arrangement
1.Standard stocked items support fast global shipment.
2.Every unit passes comprehensive precision inspection before dispatch, with inspection-report documentation enclosed.
3.Single-unit order: pearl-cotton buffer wrapping plus heavy-duty carton package.
4.Bulk export orders: fumigation-free shock-resistant solid-wood crates with partition padding, safeguarding precision datum surfaces against ocean-transport collision damage.
5.OEM & custom-modified orders follow mutually-agreed lead-time.
After-Sales Support Services
① Remote online technical guidance covering installation, commissioning and on-site fault diagnosis.
② Complete operation-maintenance documents are provided for every purchase order.
③ Custom-project technical consulting for stroke modification, special-profile jaw design and non-standard mounting-hole adjustment.
④ Spare-part supply for wearable components such as hard-jaws for independent field replacement.
FAQ
Q1: Will extended clamping travel reduce overall clamping rigidity?
No. The heavy-duty reinforced forged vise-body maintains ultra-high structural rigidity while delivering extended clamping travel. It is fully qualified for heavy-load cutting of steel and cast-iron workpieces.
Q2: Do I need to replace the whole vise once hard-jaws are worn?
No. Hard-jaws are independent replaceable spare-parts. Only worn jaws need to be swapped, which lowers overall maintenance expenditure.
Q3: Is it compatible with mainstream industrial zero-point positioning systems?
Standard-version interfaces fit most mainstream zero-point positioning bases. Custom-adaptation service can be provided for special-spec zero-point plates.
Q4: Can Extended Travel Heavy-Duty Self-Centering Zero Point Vise with Hard Jaws be deployed for 5-axis machining tasks?
Yes. Optimized compact outline avoids rotary-motion interference. It fully adapts to multi-angle tilting and flipping processing of 4-axis and 5-axis machine-tools.
Q5: Does JWGRIP accept large-batch OEM custom orders?
Yes. We deliver professional non-standard OEM customization services to satisfy mass-production and special-process requirements from global clients.
Hot Tags: Extended Travel Heavy-Duty Self-Centering Zero Point Vise with Hard Jaws, China, Manufacturer, Supplier, Factory
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.