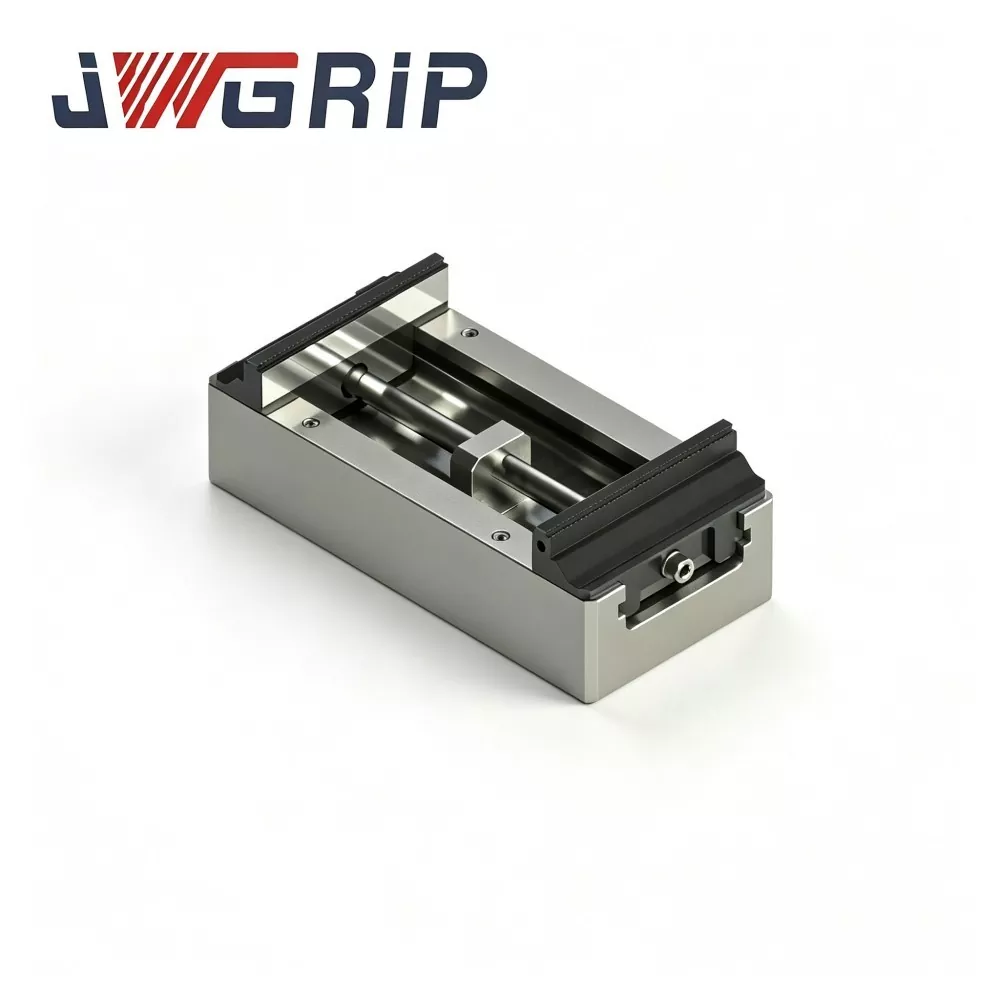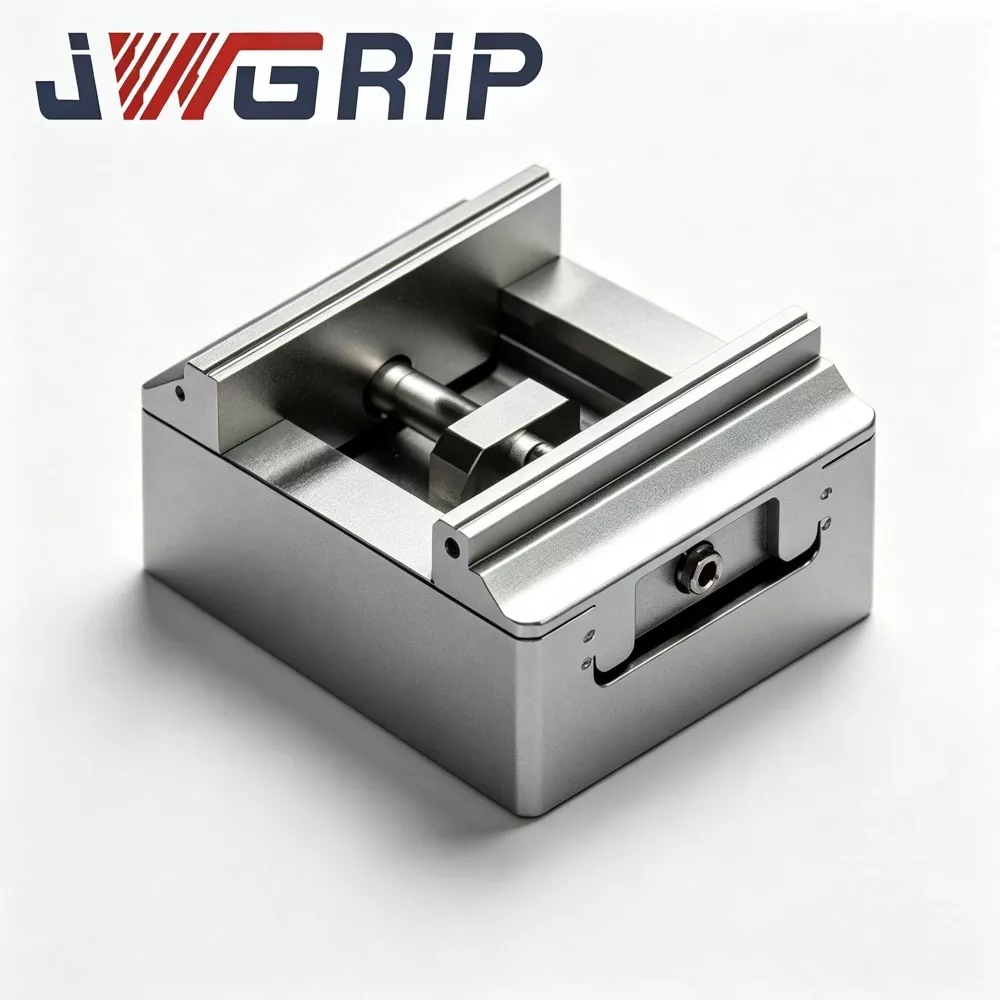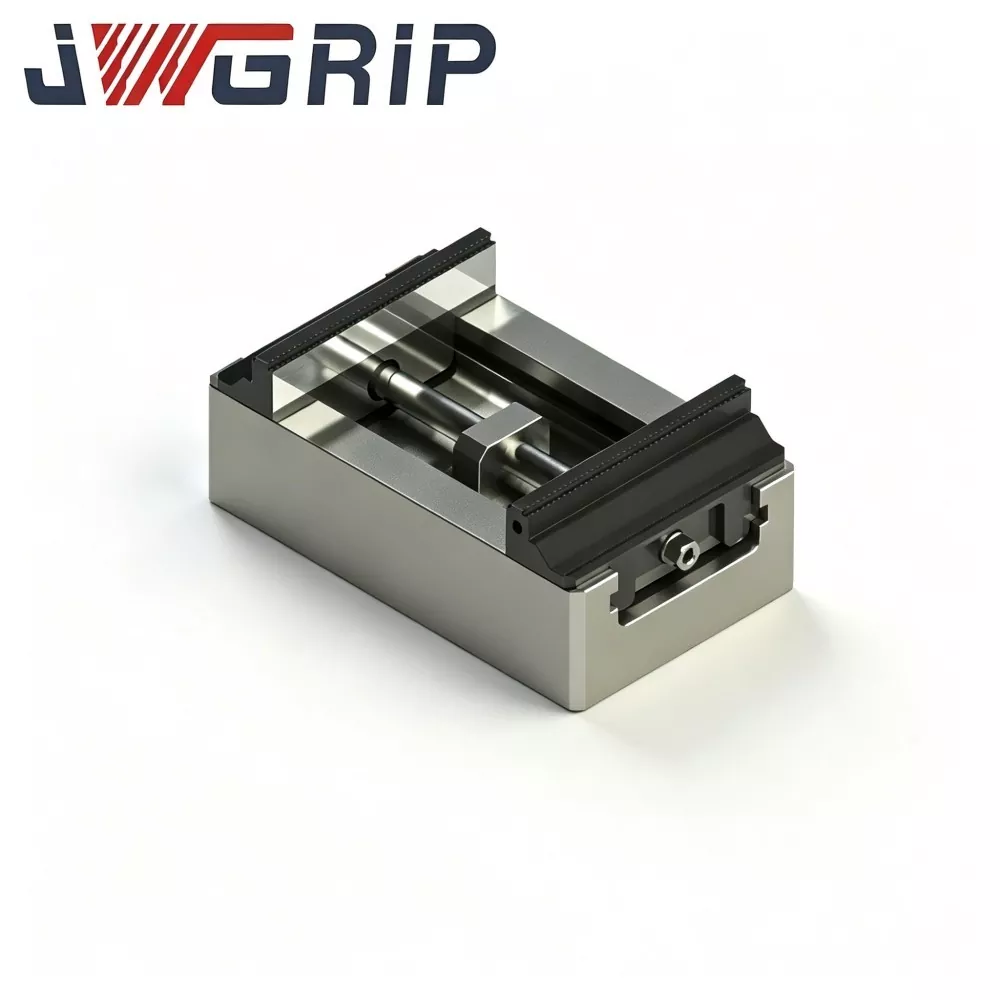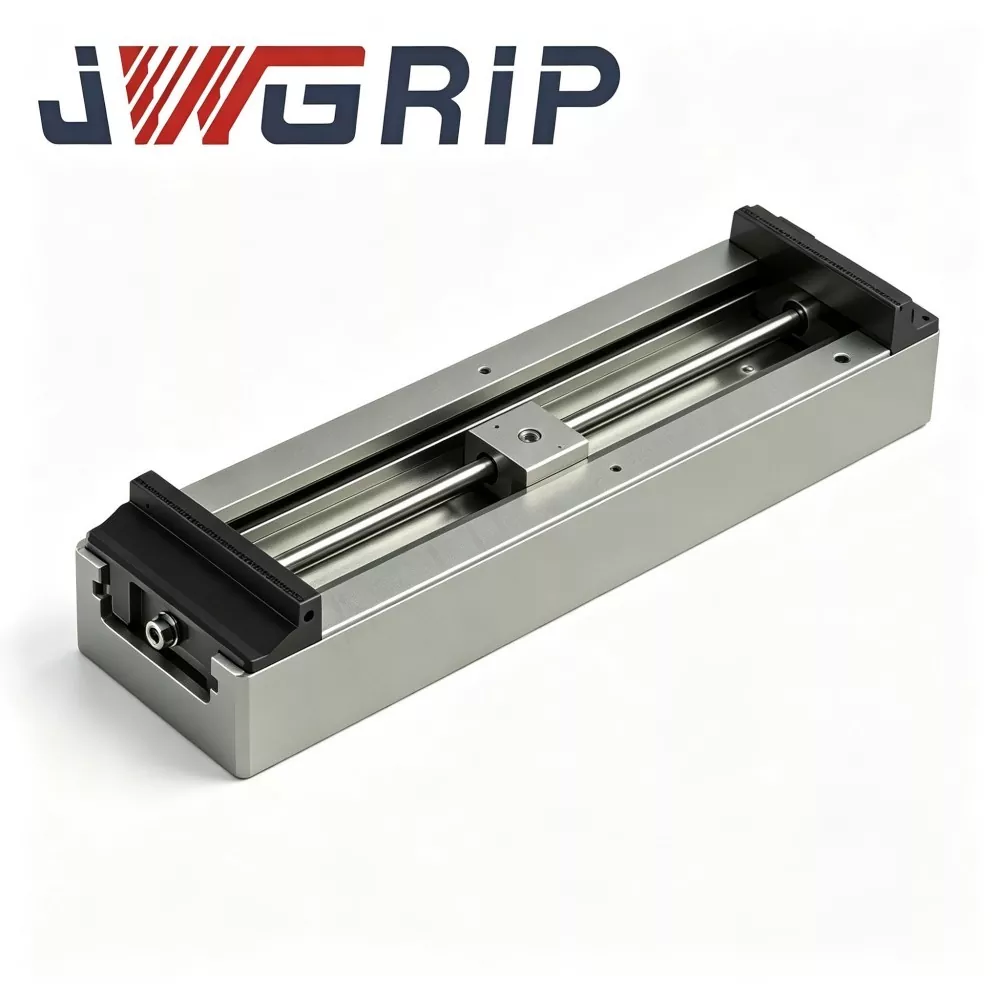
Large Travel Heavy-Duty Self-Centering Vise with Hard Jaws for Large Workpiece Machining
JWGRIP is the professional manufacturer and supplier of Customized Large Travel Heavy-Duty Self-Centering Vise with Hard Jaws for Large Workpiece Machining in China, with standard specifications fully in Stock for timely project delivery. It is a purpose-built integrated precision clamping fixture specially designed for oversized, long-dimension and large-size workpiece processing in modern CNC workshops. Adopting high-quality material configuration and standardized integrated structural design, it integrates extended clamping stroke and high-rigidity bearing structure into one single device, eliminating the need for combined assembly of multiple separate fixtures and repeated datum calibration.
This high-performance heavy-duty self-centering vise features high structural rigidity, stable clamping performance and easy-maintainable modular construction. The main frame is made of high-strength cast alloy and undergoes multiple stress-relief aging treatments to completely eliminate internal residual stress and avoid structural deformation under long-term heavy cutting loads. Key transmission and jaw matching surfaces are processed by ultra-precision grinding technology, ensuring accurate and synchronous centering effect and uniform clamping force distribution during continuous heavy-load operation.
Effectively avoiding jaw wear and workpiece position deviation caused by uneven stress, the fixture greatly saves non-cutting auxiliary time and improves workshop overall productivity. Large Travel Heavy-Duty Self-Centering Vise with Hard Jaws for Large Workpiece Machining is widely applicable to mold manufacturing, heavy machinery component processing, new energy large structural parts, aerospace structural assemblies and heavy equipment component production, providing robust and reliable professional clamping solutions for large-size workpiece milling, drilling, boring and multi-face machining processes.
Unique Clamping Challenges
Processing large-dimension workpieces creates special clamping difficulties that ordinary fixed-stroke vises cannot resolve.
1.Forced segmented / secondary clamping
Most conventional vises are designed for small-to-medium-size parts with limited travel. When handling long plates, large frame assemblies, oversized mold inserts, heavy castings and large structural profiles, one-shot full clamping is impossible. Segmented clamping or re-fixturing introduces new positioning errors, damaging dimensional tolerance, flatness and positional accuracy. For die steel, high-strength cast iron and thick aluminum-alloy blocks, secondary-clamping deviation raises reject rates of large-size components.
2.Body micro-deformation under heavy-cut loads
Many commercially-available extended-travel vises adopt thin-wall lightweight construction. To achieve longer travel, wall-thickness and structural rigidity are sacrificed. Under heavy rough-milling, high-feed and high-torque cutting, vise-body micro-deformation occurs; gear-rack transmission clearance drifts and self-centering datum shifts. Workpiece micro-slip and vibration generate chatter marks and poor surface finish. Even tiny fixture deformation can cause severe out-of-tolerance for large-size parts.
3.Uneven clamping-force distribution
If jaws cannot maintain fully synchronous movement across full large travel, clamping pressure concentrates on partial workpiece zones. Thin-walled large-size components risk clamping-induced distortion. Many generic vises use soft jaws or low-hardness inserts. Jaw wear accumulates during continuous heavy-load production, requiring frequent grinding or replacement and raising workshop operating costs.
4.Poor sealing against harsh workshop contaminants
Large-part machining generates massive metal chips and splashing coolant. Inadequate sealing allows debris and fluid to invade inner transmission assemblies, leading to jamming, corrosion and progressive accuracy decay, shortening fixture service life.
5.Long setup time for large blanks
Without purpose-optimized structures, operators spend excessive time on datum alignment, dragging down machine-tool utilization for large-batch heavy-component projects.
JWGRIP Large-Travel Heavy-Duty Self-Centering Vise with Hard Jaws is engineered against above-mentioned bottlenecks. Through large-travel structural layout, heavy-duty stress-relieved cast body, high-hardness quenched hard-jaws, reinforced synchronous transmission and optimized sealing architecture, it delivers reliable clamping for oversized workpieces while preserving high rigidity, precise centering and long-term operational stability.
Product Design Positioning
Large Travel Heavy-Duty Self-Centering Vise with Hard Jaws for Large Workpiece Machining is positioned as a dedicated clamping solution for large-dimension workpieces. It is NOT a simply scaled-up version of small-size standard vises. Every structural dimension, material grade and transmission ratio is re-engineered for heavy-load, long-travel clamping conditions.
Core design goals:
● Realize one-time complete clamping for large-size blanks and eliminate secondary-re-fixturing errors
● Keep consistent centering accuracy across the full stroke
● Maintain high structural rigidity under heavy-cutting impact
We adopt the Custom-Engineered Tooling project-oriented development concept:
● Standard models cover mainstream large-workpiece processing requirements
● Engineering-level modification is available for special workpiece dimensions, special machine-table interfaces and custom clamping requirements
The whole product is iterated based on real-world feedback from mold factories, heavy-equipment manufacturers and new-energy component plants. It balances large-travel capability, heavy-duty rigidity, clamping precision and service-friendliness. Hard-jaw configuration is selected for continuous heavy-load production scenarios to reduce frequent jaw-maintenance workload for large-part manufacturing.
Overall Assembly
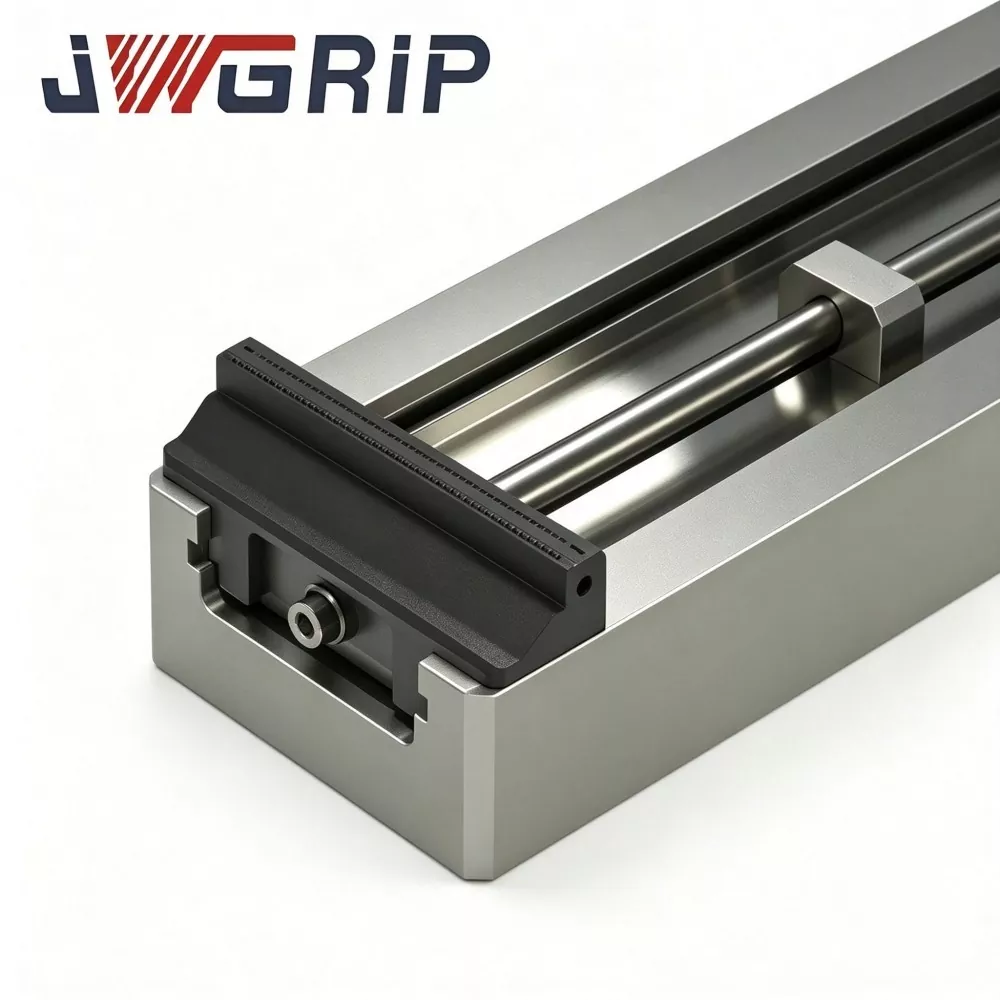
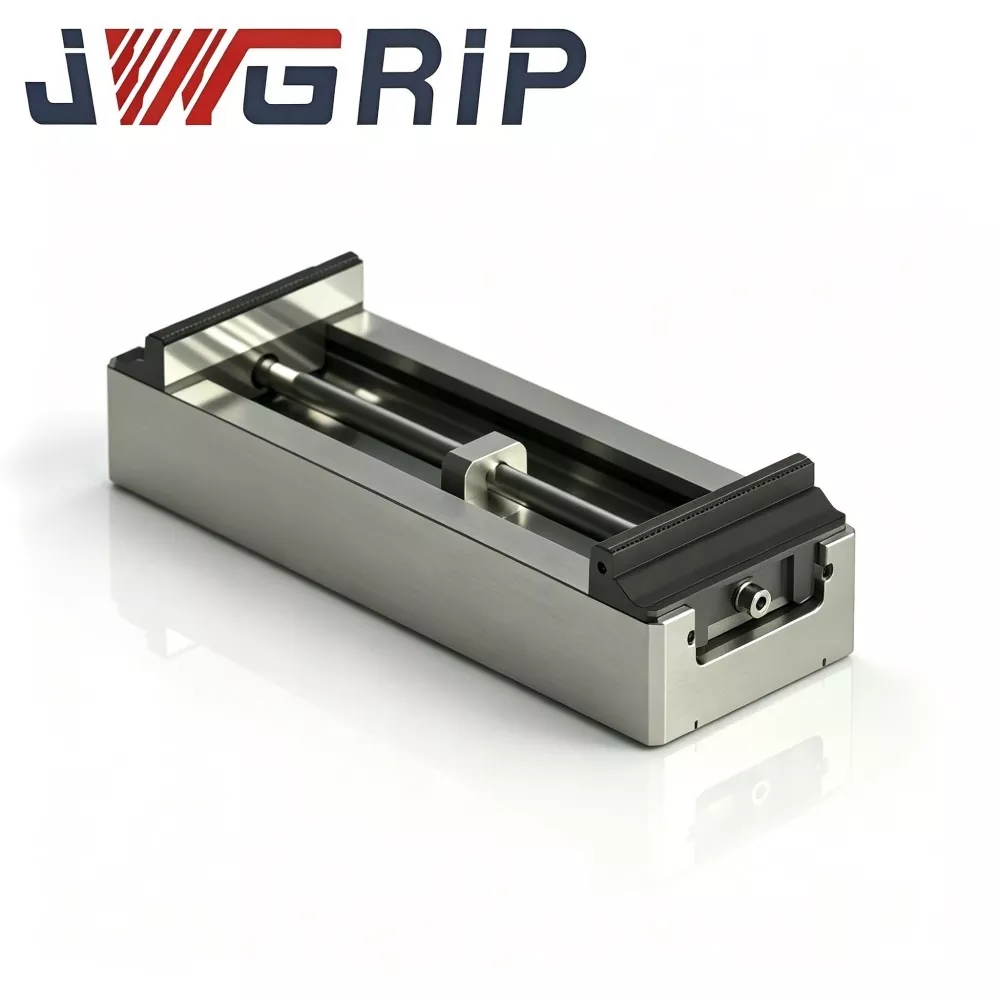
JWGRIP Large-Travel Heavy-Duty Self-Centering Vise with Hard Jaws for Large-Size Workpiece Machining includes five major core assemblies:
· Stress-relieved heavy-duty vise body
· High-precision long-travel rack-and-pinion synchronous transmission module
· Quenched high-hardness hard-jaw assembly
· Reinforced base mounting platform
· Full-enclosed chip-proof & coolant-resistant sealing system
Working Principle
The vise body is integrally forged from high-strength alloy steel and goes through multiple natural-aging plus artificial stress-relieving treatments to fully release residual stress from forging and machining. This is critical for large-travel vises: even when jaws open to maximum stroke for extra-large blanks, the main body resists bending and twisting under heavy-cutting impact.
Long-travel rack-and-pinion synchronous transmission adopts precision paired-grinding technology, keeping transmission clearance within micrometer level. Left-right hard jaws deliver perfectly symmetrical synchronous movement across the full large stroke. Workpieces placed between jaws realize automatic centering without manual fine-adjustment. Centering datum remains stable even for long, oversized blanks and removes human-induced setup deviations.
Hard-jaw assemblies are manufactured from premium tool steel, fully quenched-and-tempered followed by precision surface grinding. High surface hardness brings excellent wear-resistance and friction performance. Firmly grips die steel, cast iron, thick aluminum alloy and structural-steel workpieces, resisting cutting vibration and workpiece sliding during heavy-duty milling.
Full-enclosed sealing housing blocks metal chips, cutting fluid and workshop dust out of inner transmission cavities and protects transmission parts against jamming and corrosion. The base platform is equipped with reinforced mounting holes compatible with common CNC machine-tool worktables. Modular design enables separate replacement of worn hard-jaws; there is no need to replace the complete vise unit.
Core Competitive Strengths
1.Large-stroke one-shot clamping for oversized blanks
Realize single-setup clamping for long and large-dimension workpieces. Eliminate segmented clamping and secondary re-fixturing. Reduce accumulated positioning errors, improve dimensional consistency of large-size components and shorten overall project processing cycles for big-part production.
2.Heavy-duty stress-relieved body, anti-deformation at maximum opening
Different from thin-walled extended-travel vises on market. Forged stress-relieved body maintains high rigidity even when jaws are fully opened. Resists bending and micro-deformation in heavy rough-milling for large workpieces. Centering datum stays stable throughout complete machining workflows.
3.Quenched high-hardness modular hard-jaw assembly for heavy-duty continuous runs
Precision-ground fully-quenched hard-jaws provide superior wear-resistance. Jaw wear rate drops greatly during continuous large-size heavy-load processing. Stable clamping friction prevents workpiece slip under high cutting torque. Modular-jaw structure supports independent replacement upon wear.
4.Consistent high-precision synchronous performance over full travel range
Pair-ground rack-and-pinion system sustains synchronous-movement accuracy across the whole stroke. Whether clamping small-medium-size parts or maximum-size large blanks, centering reference does not drift. No datum offset occurs even at extreme jaw-opening positions.
5.Full-enclosed sealing suited for harsh large-part-machining environments
Large-workpiece processing produces abundant chips and coolant splash. Fully-sealed structure keeps contaminants away from transmission assemblies, lowering failure rate, extending fixture service life and reducing regular-maintenance workload.
6.Project-oriented Custom-Engineered Tooling adaptability
Standard units satisfy most large-workpiece-processing demands. Engineering-level modifications are available: travel adjustment, special-jaw geometry, custom mounting-hole layout, machine-tool-interface adaptation, to satisfy unique requirements from different manufacturing workshops.
Multi-Industry Application Coverage
1.Large-size mold manufacturing
Machining of oversized mold cores, large mold inserts and big-frame mold components. One-time clamping avoids re-fixturing errors, accelerates mold-development cycles and improves surface quality plus dimensional consistency for mold parts.
2.Heavy-duty mechanical-equipment component production
Large castings, heavy structural frames and large base plates for industrial machinery. Delivers stable clamping during heavy-load milling, drilling and boring for heavy mechanical parts.
3.New-energy large-scale structural-part fabrication
Large battery-housing components, big heat-dissipation profiles and large-size chassis frames for new-energy equipment. Large-travel clamping enables single-setup processing for bulky new-energy blanks.
4.Aerospace large-dimension structural-assembly manufacturing
Large aluminum-alloy blanks and long aerospace frame components. High-precision centering and rigid clamping satisfy strict dimensional-tolerance specifications for aerospace structural parts.
5.General heavy-duty hardware & casting processing
Oversized cast blanks, large steel structural profiles and heavy-duty metal blanks for general machinery. Suitable for both rough-machining and finish-machining of large-size workpieces.
6.Custom-Engineered special-project manufacturing
The Large Travel Heavy-Duty Self-Centering Vise with Hard Jaws for Large Workpiece Machining can be re-configured via our Custom-Engineered Tooling service to match special workpiece geometry and unique machine-tool set-ups for non-standard projects.
Operation & Maintenance Specifications
1.Daily routine maintenance
After finishing each production shift, clean jaw surfaces and vise exterior. Remove accumulated chips and coolant residues to keep clamping surfaces free of debris and preserve centering accuracy.
2.Periodic lubrication maintenance
Apply special high-temperature-resistant lubricating grease to internal rack-and-pinion transmission components on a regular cycle. Maintain smooth jaw-opening-closing motion and stable transmission clearance for large-stroke operation.
3.Quarterly precision inspection & calibration
Check self-centering accuracy and mounting-datum condition every quarter. Detect minor precision drift in advance and prevent large-size-workpiece out-of-tolerance accidents.
4.Wear-part replacement management
Periodically inspect hard-jaw wear condition. When surface wear degrades clamping performance, replace hard-jaw inserts independently. Full-vise replacement is not required.
5.Long-term idle-storage protection
If the vise remains idle for a long period, fully clean all surfaces. Apply anti-rust coating over metal surfaces and datum planes. Store in dry, dust-proof surroundings.
6.Forbidden-operation rules
Never use over-stroke or over-load clamping. Avoid heavy-tool impact striking against vise-body and jaws to prevent structural deformation and inner-transmission damage.
Fault Diagnosis & Handling
Fault 1: Large-size workpiece dimensional deviation after machining
Possible causes: insufficient clamping force; transmission lack-of-lubrication; hard-jaw wear; loose base-mounting bolts
Solutions: Appropriately raise clamping-force; replenish special-purpose lubricant; grind or replace worn hard-jaws; retighten base bolts with standard torque.
Fault 2: Jaw jamming and unsmooth opening-closing movement
Possible causes: Chips / coolant invade sealed-cavity; insufficient grease supply; inner-transmission-component wear
Solutions: Disassemble and clear internal contaminants; replenish lubricating grease; inspect and replace heavily-worn transmission-parts.
Fault 3: Centering-accuracy drop after vise re-installation
Possible causes: Dirty mounting-datum surfaces; mounting-bolt loose; local jaw-surface wear
Solutions: Thoroughly clean vise-base and machine-table mating-surfaces; re-torque mounting-bolts; inspect and replace worn hard-jaw inserts.
Fault 4: Workpiece micro-slip during heavy-load large-part rough-milling
Possible causes: Insufficient locking torque; chips stuck on hard-jaw clamping-faces
Solutions: Increase locking torque moderately; fully clean jaw contact surfaces before clamping workpieces.
Procurement & Selection Reference
Core value of JWGRIP Large Travel Heavy-Duty Self-Centering Vise with Hard Jaws for Large Workpiece Machining lies in large-stroke single-setup clamping capacity, heavy-duty anti-deformation forged body, full-travel consistent centering-precision, quenched wear-resistant hard-jaws and project-oriented Custom-Engineered Tooling capability. It addresses typical pain-points in large-size-workpiece CNC machining: forced segmented clamping, insufficient rigidity under heavy-cut loads, jaw fast-wear and high setup-time consumption.
Selection reminders:
1. Compare maximum workpiece outer dimension against vise effective clamping-stroke, reserve adequate safety margin.
2. For heavy-cut processing of steel, cast-iron and thick-alloy blanks, prioritize hard-jaw configuration.
3. Evaluate machine-table mounting-hole layout to match vise base mounting specification. Contact our engineering team for non-standard machine-table adaptation requirements.
4. Standard stocked versions enable fast delivery; turn to Custom-Engineered Tooling service for extra-large blanks or special project-demands.
Factory-direct from JWGRIP. This vise is an ideal upgrade fixture for workshops undertaking mold, heavy-equipment, new-energy and aerospace large-size-component milling-drilling-boring jobs.
FAQ
Q1: Will large-travel design reduce vise-body structural rigidity?
No. This vise adopts heavy-duty forged stress-relieved body and re-optimized structural layout for large-stroke scenarios. It maintains high anti-deformation performance even at maximum jaw opening and can sustain heavy-load cutting of large-size workpieces.
Q2: Do I need to replace the whole vise after hard-jaws wear out?
No. Hard-jaw inserts are modular independent spare-parts. Only worn jaw inserts require replacement, which lowers workshop long-term maintenance costs.
Q3: Can this vise work with 4-axis rotary tables for multi-face machining of large-size workpieces?
Yes. Optimized outer-body contour fits 4-axis rotary-table installation conditions and supports multi-face indexing-machining for large-size blanks.
Q4: Is Custom-Engineered Tooling modification available for special-dimension workpieces?
Yes. Our engineering team can adjust clamping-stroke, custom-build special-profile jaws and modify mounting-structure to match unique workpiece-specifications and machine-tool requirements.
Q5: Can it handle both rough-milling and finish-milling for large-size workpieces?
Yes. Heavy-duty stress-relieved body and high-precision synchronous-transmission satisfy both heavy-load rough-milling and high-accuracy finish-milling requirements for large-dimension blanks.
Hot Tags: Large Travel Heavy-Duty Self-Centering Vise with Hard Jaws for Large Workpiece Machining, Manufacturer, Supplier, Factory
Send Inquiry
Contact Info
-
Address
No. 44, Daning Entrepreneurship Road, Humen Town, Dongguan City, Guangdong Province, China
-
Tel
-
Email
Welcome to send inquiry to JWGRIP. Our professional technical and sales team will provide free fixture selection, customized solution design and accurate quotation.